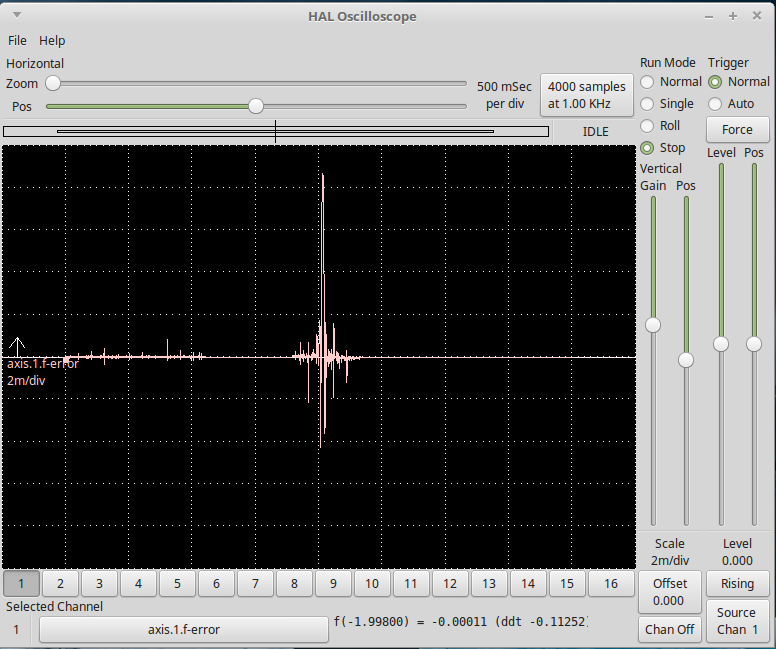
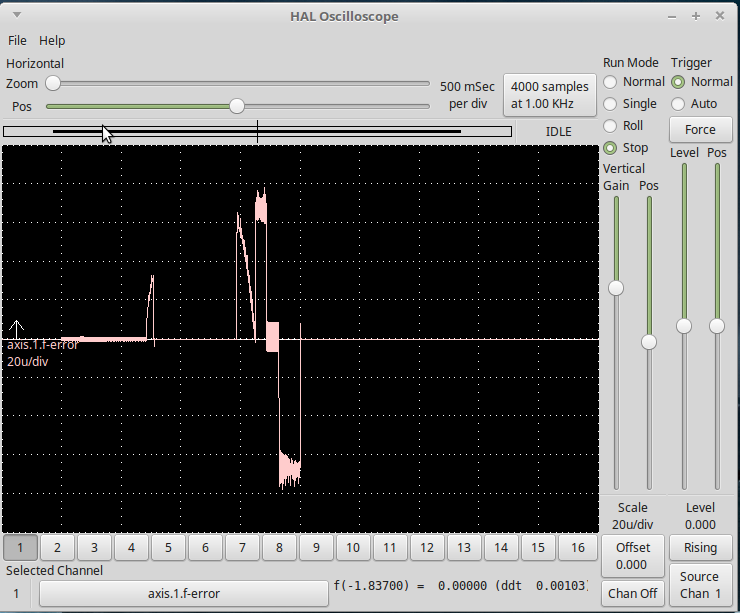
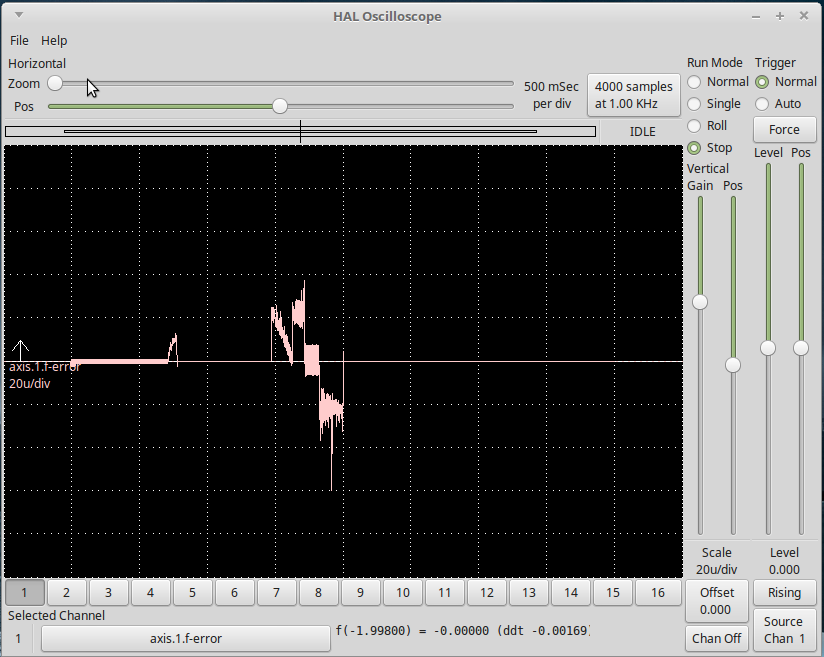
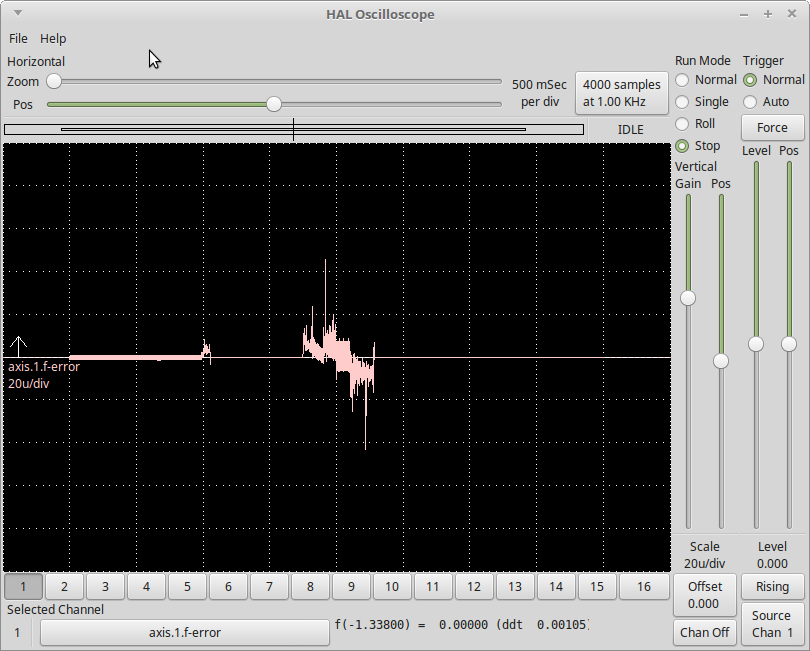
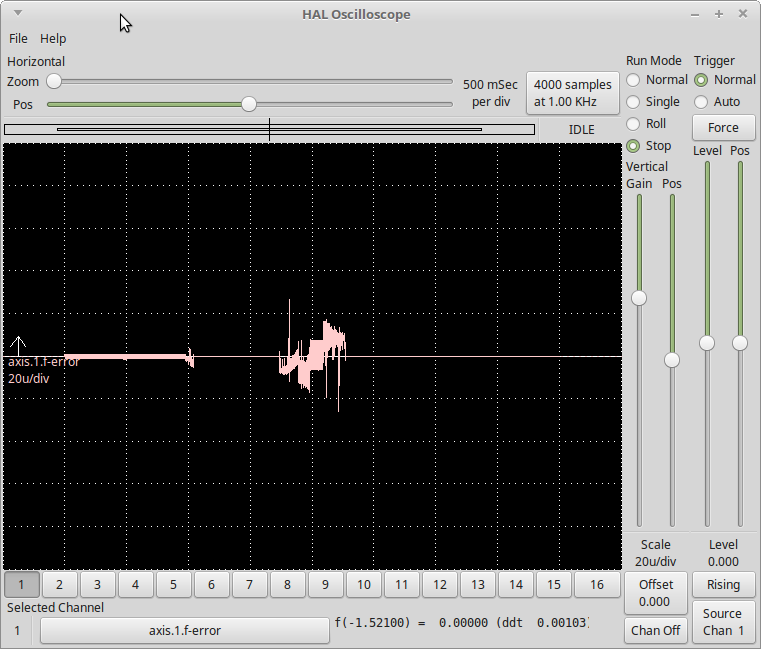
Just for interest, here's the differences I'm seeing with the various fixes and tweaks in place.
The G-code running on the mill during these scope captures is just the standard 'LinuxCNC' logo test program that loads on Axis startup. The large spike in each of the traces is the Y-axis Following Error as it rapids between the end of cutting the lower-case 'n' in 'LinuxCNC' to the start of the dot above the 'i'. This is where I found the biggest deviation while running this particular G-code.
Without any fixes or tweaks. Largest peak on the FErr spike is about 9 millis:
With PCW's 'latch all stepgen counts...' HAL fix. Largest peak is down to +/-80 micros:
With PCW's HAL fix plus the addition of FF2 = 0.00015 and PID max_error = 0. Largest peak is down to +40/-60 micros:
G0 rapids on my machine are 3200mm/min during these tests.