
- Posts: 175
- Thank you received: 14

Please Log in or Create an account to join the conversation.

Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
I would consider it "hopeless".Please Log in or Create an account to join the conversation.
I doubt it can be done in a meaningful way
I was surfing and found this link (post # 7)
www.cnczone.com/forums/benchtop-machines...speeds-feed-doc.html
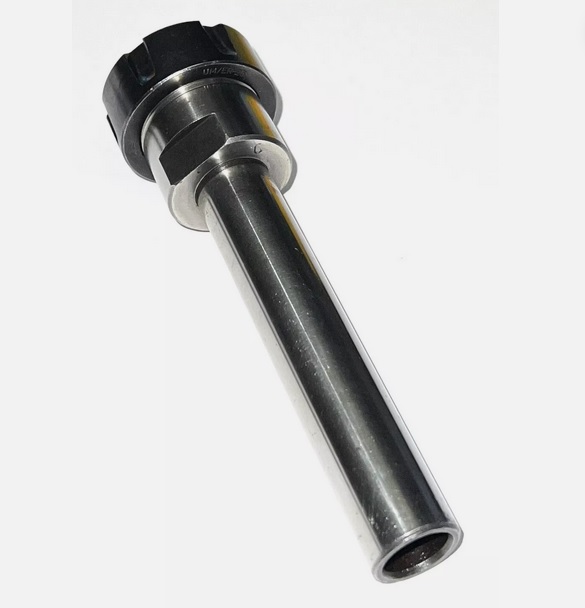
I bought a cylindrical ER25 toolholder from Rego-Fix (Swiss made) and NSK P4 angular contact bearings and made my own direct coupled spindle.
I did the lathe work myself. While its not perfect I am still pretty proud of it. It takes about 15 minutes to swap between the highspeed spindle and
my high torque 'grunter'.
It cuts steel like a DEMON!!!! The problem is that my mill is not really a stiff as I had thought.....but still I can cut as much steel or stainless steel as
I can offer up to the spindle.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.