

- Posts: 19311
- Thank you received: 4655
G-code to engrave numbers on cylinders
13 years 12 hours ago - 8 years 2 months ago #40497
by andypugh
G-code to engrave numbers on cylinders was created by andypugh
[edit 30/8/18: I added tick marks, see
forum.linuxcnc.org/20-g-code/27169-g-cod...ders?start=10#116888
]
I wrote this G-code to engrave angles on a lathe part. It might be handy for other things. It uses a sub for each digit, then computed-calls to call the right one.
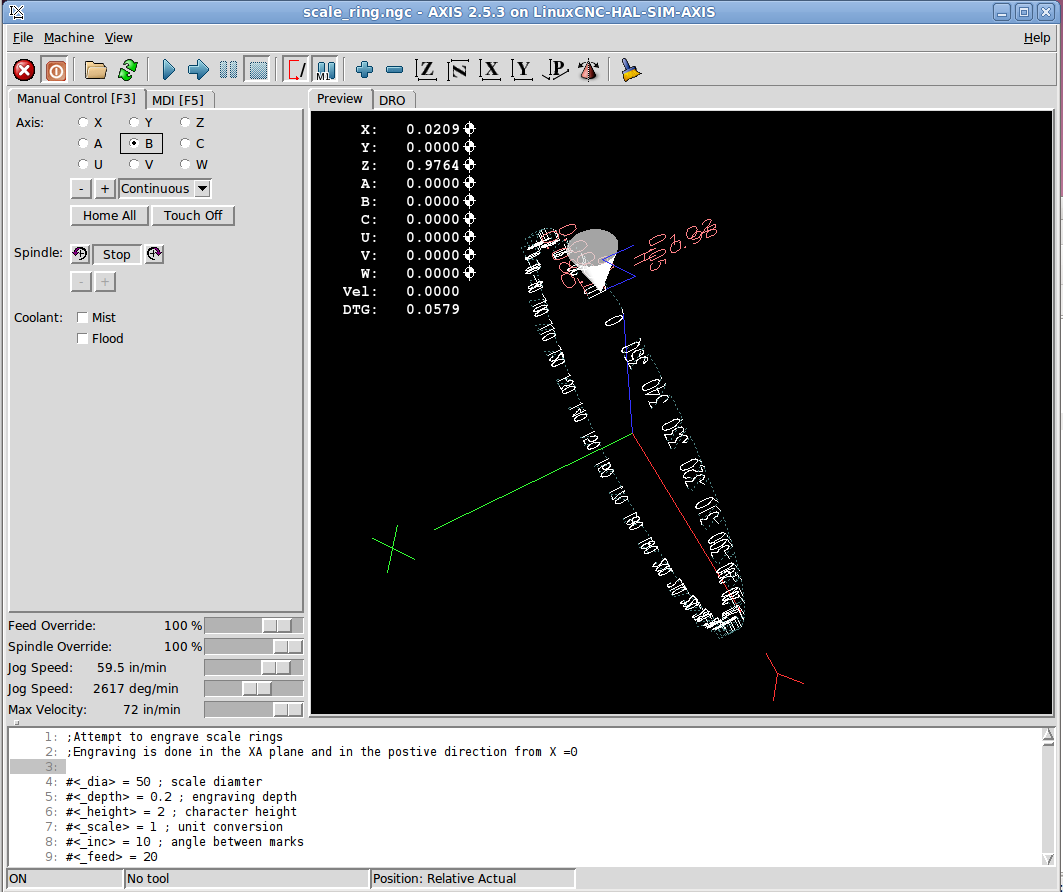
I wrote this G-code to engrave angles on a lathe part. It might be handy for other things. It uses a sub for each digit, then computed-calls to call the right one.
Code:
;Attempt to engrave scale rings
;Engraving is done in the XA plane and in the postive direction from X =0
#<_dia> = 50 ; scale diamter
#<_depth> = 0.2 ; engraving depth
#<_height> = 2 ; character height
#<_scale> = 1 ; unit conversion
#<_inc> = 10 ; angle between marks
#<_feed> = 20
G21
F #<_feed>
#41 = [180 / [#<_dia> * 3.14159] * #<_height>]
#42 = #<_height>
(debug, #41 #42)
O0 sub
G92 A0 X0
G0 A0 X0 Z[#<_dia> / 2 + 1]
G1 Z[#<_dia> / 2 - #<_depth>]
A[0.2357 * #41] X[0.0976 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.3333 * #41] X[0.6667 * #42]
A[0.2357 * #41] X[0.9024 * #42]
A[0.0000 * #41] X[1.0000 * #42]
A[-0.2357 * #41] X[0.9024 * #42]
A[-0.3333 * #41] X[0.6667 * #42]
A[-0.3333 * #41] X[0.3333 * #42]
A[0.0000* #41] X[0.0000 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O0 endsub
O1 sub
G92 A0 X0
G1 Z[#<_dia> / 2 - #<_depth>]
A[0.0000 * #41] X[1.0000 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O1 endsub
O2 sub
G92 A0 X0
G0 A[0.3333 * #41] X[0.000 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[-.3333 * #41] X[0.0000 * #42]
A[0.0000 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.4310 * #42]
A[0.3333 * #41] X[0.6666 * #42]
A[0.2357 * #41] X[0.9024 * #42]
A[0.0000 * #41] X[1.0000 * #42]
A[-.2357 * #41] X[0.9024 * #42]
A[-.3333 * #41] X[0.6667 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O2 endsub
O3 sub
G92 A0 X0
G0 A[-.3333 * #41] X[0.3333 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[-.2357 * #41] X[0.0976 * #42]
A[0.0000 * #41] X[0.0000 * #42]
A[0.2357 * #41] X[0.0976 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.5690 * #42]
A[0.0000 * #41] X[0.6667 * #42]
A[0.3333 * #41] X[1.0000 * #42]
A[-.3333 * #41] X[1.0000 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O3 endsub
O4 sub
G92 A0 X0
G0 A[0.2357 * #41] X[0.000 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[0.2357 * #41] X[1.0000 * #42]
A[-.3333 * #41] X[0.3333 * #42]
A[0.3333 * #41] X[0.3333 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O4 endsub
O5 sub
G92 A0 X0
G0 A[-.3333 * #41] X[0.3333 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[-.2357 * #41] X[0.0976 * #42]
A[0.0000 * #41] X[0.0000 * #42]
A[0.2357 * #41] X[0.0976 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.5690 * #42]
A[0.0000 * #41] X[0.6667 * #42]
A[-.3333 * #41] X[0.6667 * #42]
A[-.3333 * #41] X[1.0000 * #42]
A[0.3333 * #41] X[1.0000 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O5 endsub
O6 sub
G92 A0 X0
G0 A[-.3333 * #41] X[0.0333 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia> / 2 - #<_depth>]
A[-.2357 * #41] X[0.5690 * #42]
A[0.0000 * #41] X[0.6667 * #42]
A[0.2357 * #41] X[0.5690 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.0976 * #42]
A[0.0000 * #41] X[0.0000 * #42]
A[-.2357 * #41] X[0.0967 * #42]
A[-.3333 * #41] X[0.3333 * #42]
A[-.2357 * #41] X[0.9024 * #42]
A[0.0000 * #41] X[1.0000 * #42]
A[0.2357 * #41] X[0.9024 * #42]
G0Z [#<_dia> / 2 + 1]
G92.1
O6 endsub
O7 sub
G92 A0 X0
G0 A[-.2357 * #41] X[0.0000 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[0.3333 * #41] X[1.0000 * #42]
A[-.3333 * #41] X[1.0000 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O7 endsub
O8 sub
G92 A0 X0
G0 A[0.2357 * #41] X[0.5690 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia> / 2 - #<_depth>]
A[-.2357 * #41] X[0.5690 * #42]
A[-.3333 * #41] X[0.3333 * #42]
A[-.2357 * #41] X[0.0976 * #42]
A[0.0000 * #41] X[0.0000 * #42]
A[0.2357 * #41] X[0.0976 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.5690 * #42]
A[0.3333 * #41] X[0.6667 * #42]
A[0.2357 * #41] X[0.9024 * #42]
A[0.0000 * #41] X[1.0000 * #42]
A[-.2357 * #41] X[0.9024 * #42]
A[-.3333 * #41] X[0.6667 * #42]
A[-.2357 * #41] X[0.5690 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O8 endsub
O9 sub
G92 A0 X0
G0 A[-.3333 * #41] X[0.3333 * #42] Z[#<_dia> / 2 + 1]
G1 Z[#<_dia>/2 - #<_depth>]
A[-.2357 * #41] X[0.0976 * #42]
A[0.0000 * #41] X[0.0000 * #42]
A[0.2357 * #41] X[0.0976 * #42]
A[0.3333 * #41] X[0.3333 * #42]
A[0.3333 * #41] X[0.6667 * #42]
A[0.2367 * #41] X[0.9024 * #42]
A[0.0000 * #41] X[1.0000 * #42]
A[-.2357 * #41] X[0.9024 * #42]
A[-.3333 * #41] X[0.6667 * #42]
A[-.2357 * #41] X[0.4310 * #42]
A[0.0000 * #41] X[0.3333 * #42]
A[0.2357 * #41] X[0.4310 * #42]
A[0.3333 * #41] X[0.6667 * #42]
G0 Z[#<_dia> / 2 + 1]
G92.1
O9 endsub
; Start Engraving
G92.1
#3 = 0
O100 while [#3 LT 360]
#4 = [#3 * #<_scale>]
(DEBUG, #4)
O101 if [#4 LT 10]
G0 A#3 X0 Z[#<_dia> / 2 + 1]
O[FIX[#4]] call
O101 else if [#4 LT 100]
G0 A[#3 - #42 * 0.5] X0 Z[#<_dia> / 2 + 1]
O[FIX[#4 / 10]] call
G0 A[#3 + #42 * 0.5] X0
O[FIX[#4 mod 10]] call
O101 else if [#4 LT 1000]
G0 A[#3 - #42 ] X0 Z[#<_dia> / 2 + 1]
O[FIX[#4 / 100]] call
G0 A#3 X0
O[FIX[[#4/10] mod 10]] call
G0 A[#3 + #42 ] X0
O[FIX[#4 mod 10]] call
O101 endif
#3 = [#3 + #<_inc>]
O100 endwhile
M2
Last edit: 8 years 2 months ago by andypugh.
The following user(s) said Thank You: BigJohnT, Dimitrios, biqut2, RotarySMP, jo_key, clunc, Boltonbrass
Please Log in or Create an account to join the conversation.

12 years 11 months ago #40509
by BigJohnT
Replied by BigJohnT on topic G-code to engrave numbers on cylinders
That's pretty slick Andy.
JT
JT
Please Log in or Create an account to join the conversation.
12 years 11 months ago - 12 years 11 months ago #41130
by andypugh
Replied by andypugh on topic G-code to engrave numbers on cylinders
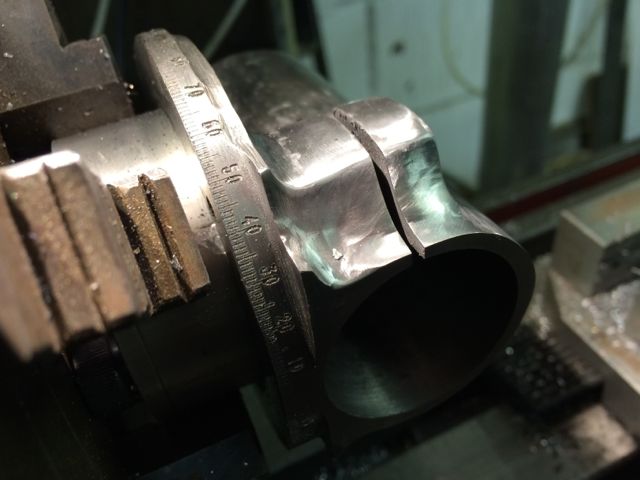
The fonts are based on two octagons, and straight lines, but the results don't show it.
Last edit: 12 years 11 months ago by andypugh.
Please Log in or Create an account to join the conversation.
- Kirk_Wallace
- Offline
- New Member
-

Less
More
- Posts: 19
- Thank you received: 0
11 years 9 months ago #55453
by Kirk_Wallace
Replied by Kirk_Wallace on topic G-code to engrave numbers on cylinders
Andy, thank you for replying to my IRC query. My setup -- 10.04, 2.5, stock sim_axis9 and stock sim.ini and your g-code above --- produces a tool that only moves in X and Z. It appears that the DROs change appropriately, but not the display. If it is convenient, could you let me know if you there are any configuration or other changes I should look at?
Please Log in or Create an account to join the conversation.
11 years 9 months ago #55458
by andypugh
I just tried it in the stock sim/axis-9-axis config and it was as you describe.
I changed GEOMETRY to ABCXYZYVW and then on restart the display looked as-shown in the picture above.
Replied by andypugh on topic G-code to engrave numbers on cylinders
Kirk_Wallace wrote: If it is convenient, could you let me know if you there are any configuration or other changes I should look at?
I just tried it in the stock sim/axis-9-axis config and it was as you describe.
I changed GEOMETRY to ABCXYZYVW and then on restart the display looked as-shown in the picture above.
Please Log in or Create an account to join the conversation.
- Kirk_Wallace
- Offline
- New Member
-
Less
More
- Posts: 19
- Thank you received: 0
11 years 9 months ago #55460
by Kirk_Wallace
Replied by Kirk_Wallace on topic G-code to engrave numbers on cylinders
Crud, I tried:
[TRAJ]
AXES = 9
COORDINATES = A B C X Y Z U V W
HOME = 0 0 0 0 0 0 0 0 0
LINEAR_UNITS = inch
ANGULAR_UNITS = degree
CYCLE_TIME = 0.010
DEFAULT_VELOCITY = 1.0
DEFAULT_ANGULAR_VELOCITY = 45.0
POSITION_FILE = position9.txt
MAX_LINEAR_VELOCITY = 1.2
MAX_ANGULAR_VELOCITY = 90.0
No joy. (using LinuxCNC 2.6.5 on Wheezy)
[TRAJ]
AXES = 9
COORDINATES = A B C X Y Z U V W
HOME = 0 0 0 0 0 0 0 0 0
LINEAR_UNITS = inch
ANGULAR_UNITS = degree
CYCLE_TIME = 0.010
DEFAULT_VELOCITY = 1.0
DEFAULT_ANGULAR_VELOCITY = 45.0
POSITION_FILE = position9.txt
MAX_LINEAR_VELOCITY = 1.2
MAX_ANGULAR_VELOCITY = 90.0
No joy. (using LinuxCNC 2.6.5 on Wheezy)
Please Log in or Create an account to join the conversation.
Time to create page: 0.111 seconds