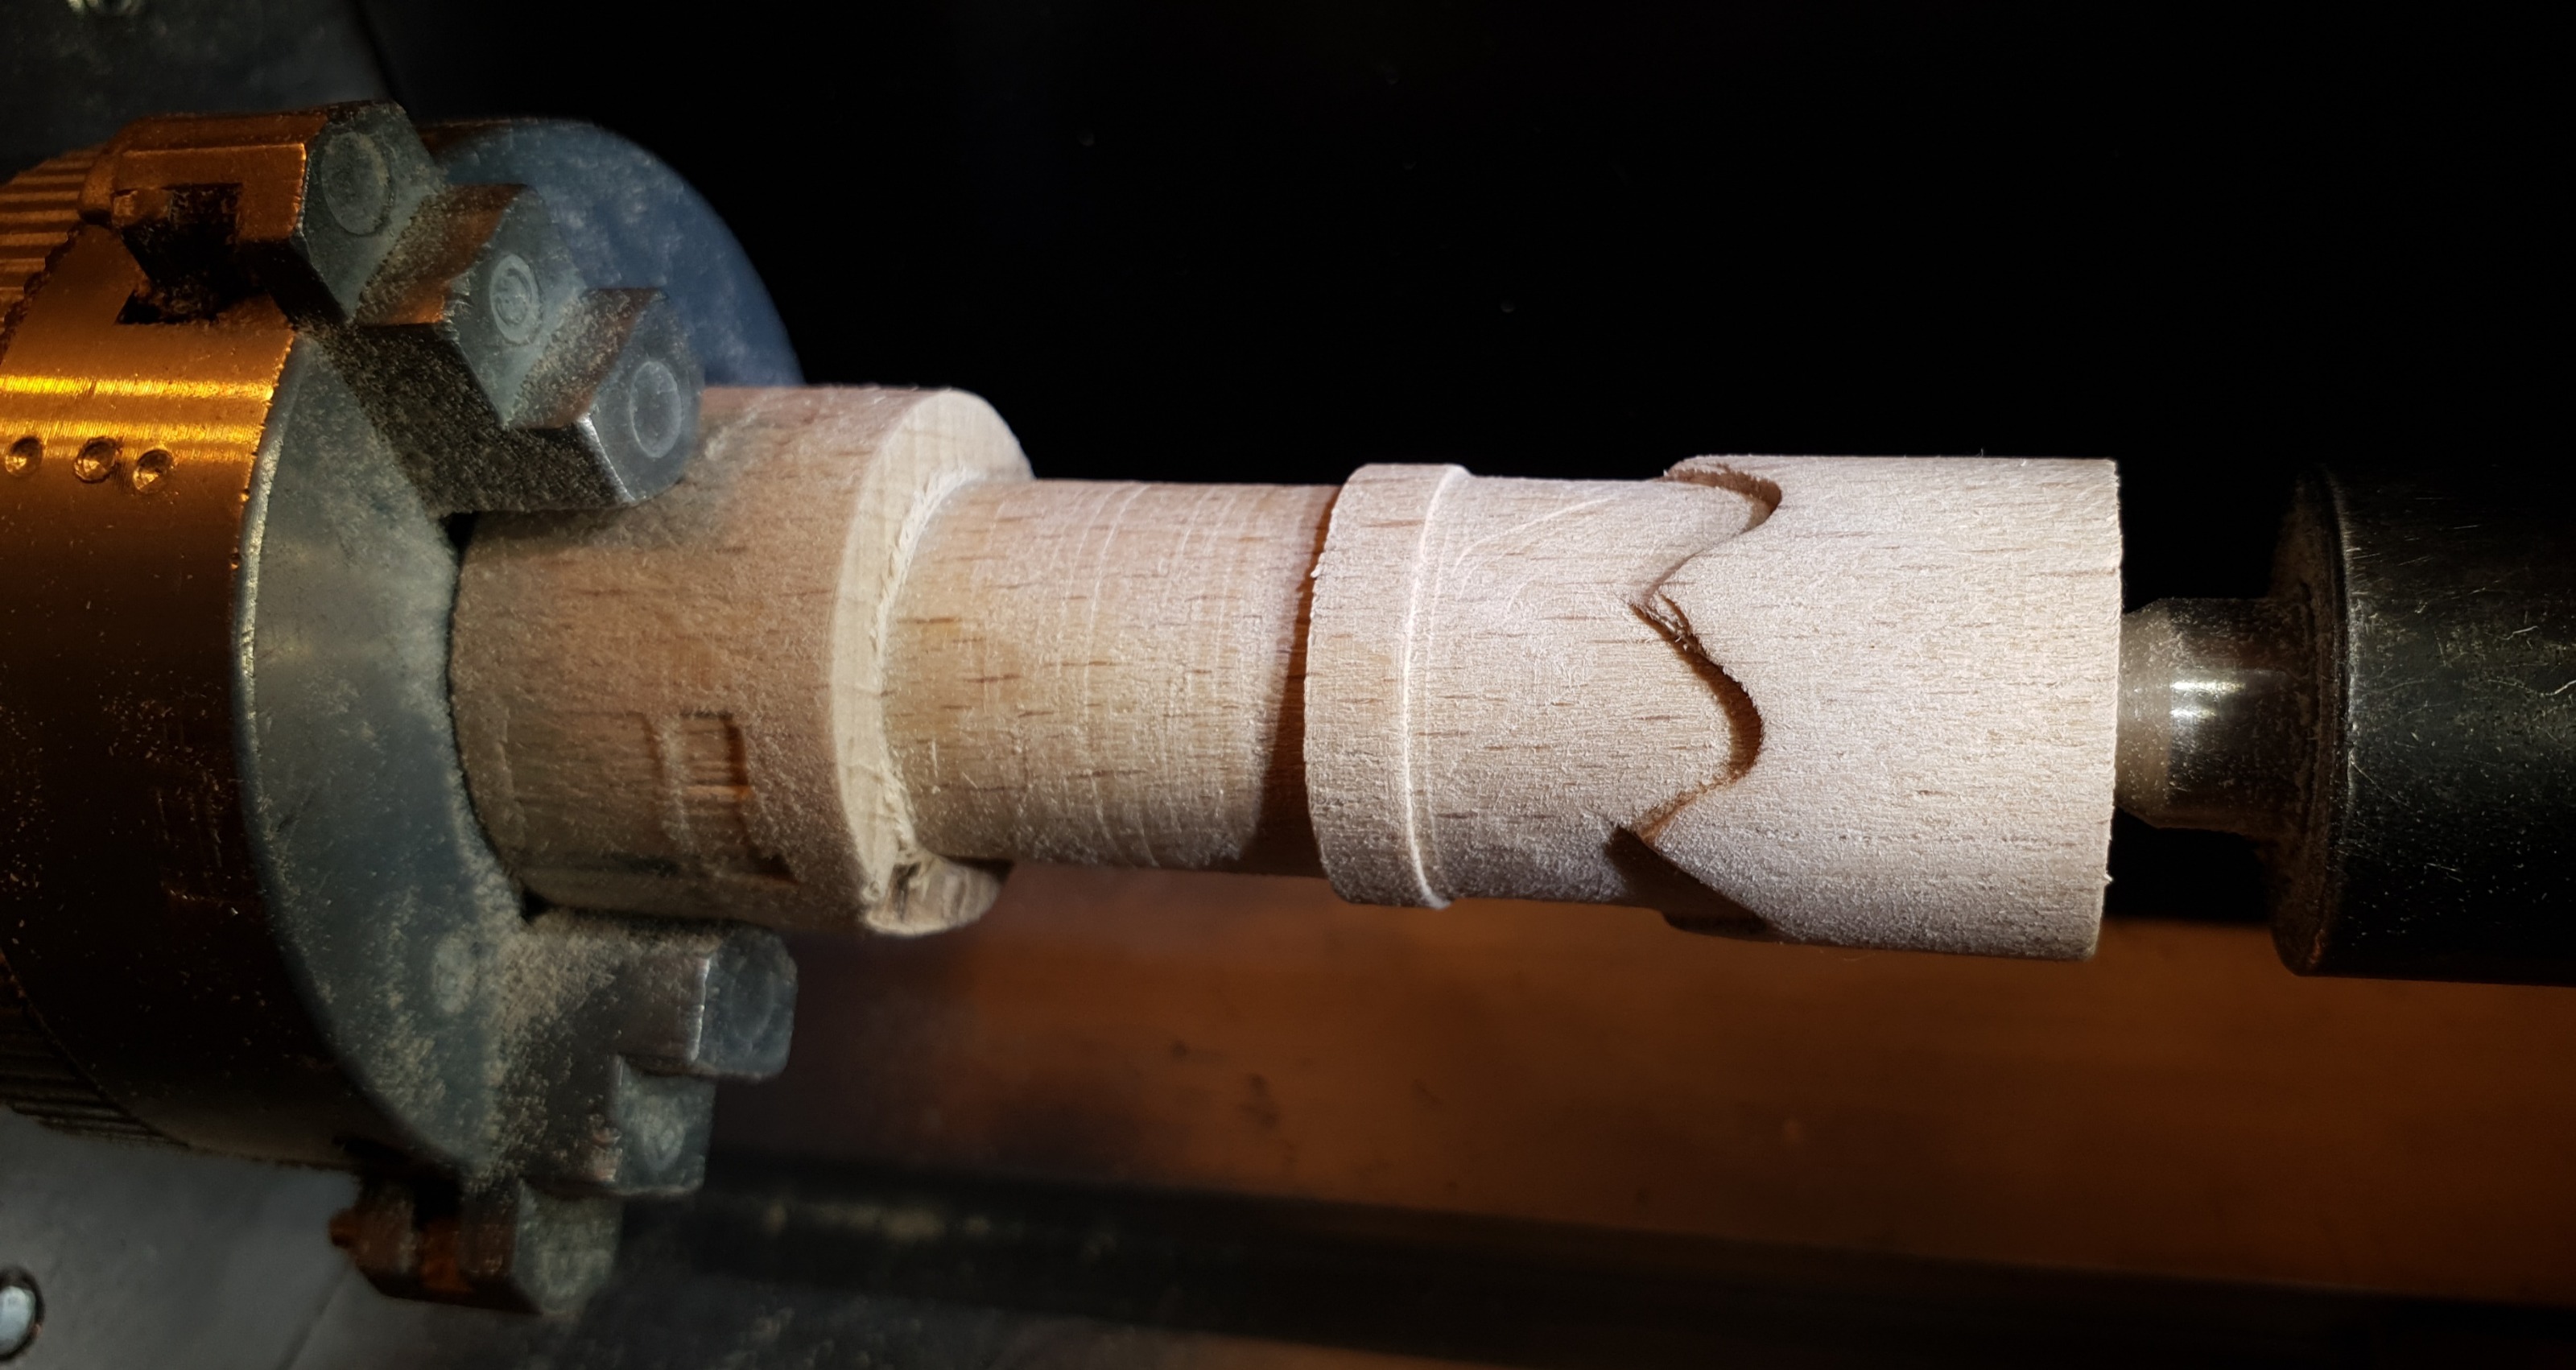
I have cleaned up the kinematics file, the ini config, and the machine with some axis being stuck.
- Now u,v,w are again free to be used as normal tool offsets.
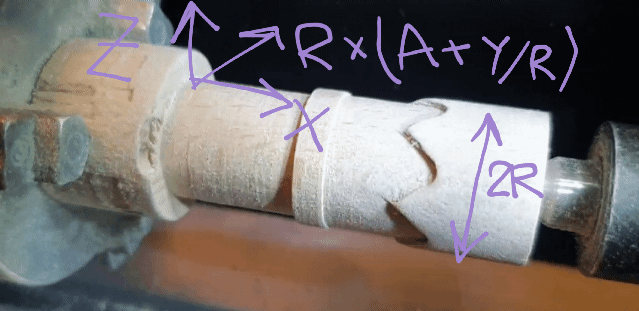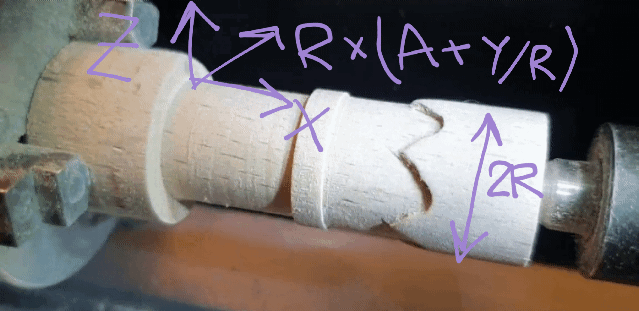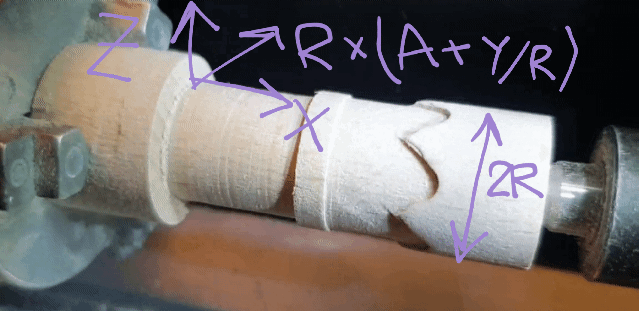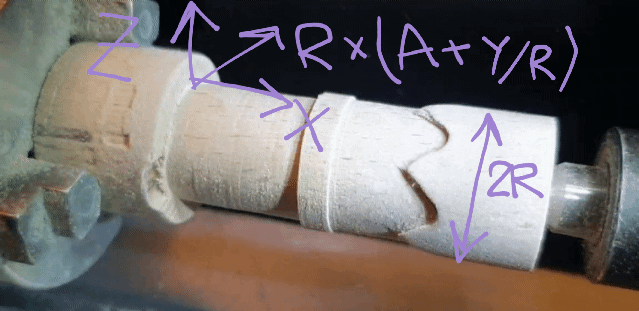
- Machine Y is mapped on B axis.- A axis is rotation as normal.- The cylinder radius is stored in axis C.
- Machine Y is moved prior to call gcode, using joint4. When cylinder axis lines up with the cutter, G92 B0 will do the job.
- A is used like a tool offset, applied to rotate the part to starting point, like using X. Then G92 X0 A0 Z0 sets the part origin.
All together simple enough to remember in front of the machine. Attached a sample ngc that will cut some periodic zig zag pattern. My machine is far from high-end, but code is running fine. Hopefully I can cut some nice chess figures from hard wood.