lathe tool sensor setup , who's done it ?

More
3 years 4 months ago #273945 by smc.collins
the lathe tool sensor has 4 inputs and has 4 offsets 1 per input. so that's why a hal component is needed, lcnc only allows for a single probe input and it's not specifically designed to be a lathe tool sensor.
The following user(s) said Thank You: spumco

Please Log in or Create an account to join the conversation.
More
3 years 4 months ago #273966 by spumco
@GuiHue

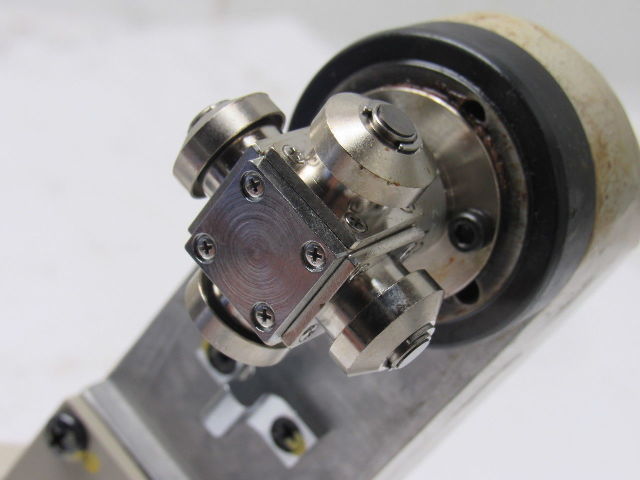
Some lathe tool probes are basically a spindle probe with square sides (instead of a ball stylus).

However, some are 4-sided jobs.


Some (older) machines required the operator to lower the probe arm manually (or bolt it on).  Newer machines generally deploy the arm automatially... meaning up sensor and deployed sensors, plus safety logic in case it doesn't make it down all the way.

Pretty sure you could do everything in M-codes, but it'd get messy and hard to follow or debug.  A dedicated comp to handle all of the backstage stuff would be sweet.

Please Log in or Create an account to join the conversation.

More
3 years 3 months ago #275537 by endian
hello gentelmen,

I am hooking up pin for this topic because I am curently tring to solve same problem.
  1. Where to place metrol probe to flatbed lathe - small free space volume
  2. how to start probing - by some marco from MDI screen probably
I am owner of this stuff  knuth vturn 410 1000  converted to CNC by analog kollmorgen servopacks. I bought  metrol stuff  for tool probing purpose. 

I found some ways of putting it on lathe, placement connection and probing subroutine but feedback from real user should be better then my own dreams. Have anybody experiences with implementation of that and what should do and what avoid please?

Regards F.

Please Log in or Create an account to join the conversation.

More
3 years 2 months ago #278733 by JR1050
This is my tool setting macro. 
od tool 12 oclock P12
front of any tool 3 oclock P3
id tool 6 oclock P6
left hand tool 09 oclocl P9
 set tool about .2 from the probe
Probe front of any tool 
M275 P3 in MDI
G54 is ALWAYS machine zero, #101, #102 ect are the variables you have to figure out. #101 would be the difference from the triggered probe to the center of your spindle. #104 in my case is the distance from the front of the chuck to the face of the probe.

o<m275> sub
G90G49G54
(PROBE OD TURNING TOOL-THISONE WORKS)
o101 if[#<P> EQ 12]
#102=-1.7501
G49G94
G91
G38.2 X-.2 F5.
G0X.15
G38.2 X-.2 F5.
#101=[[#5061+#102]*2]
G0X.2
G90G49
G10 L1 P#5400 X#101
G49

(PROBE ID TOOL)
o101 elseif[#<P> EQ 6]
#103=-.1585
G49G94
G91
G38.2 X.2 F5.
G0X-.15
G38.2 X.2F5.
#101=[[#5061+#103]*2]
G0X-.2
G90G49
G10 L1 P#5400 X#101


(PROBE FRONT OF ANY TOOL)
o101 elseif[#<P> EQ 3]
#104=-9.6783
G49G94
G91
G38.2 Z-.2F5.
G0Z.15
G38.2 Z-.2F5.
#101=[#5063+#104]
G0Z.2
G90G49
G10 L1 P#5400 Z#101

(PROBE LEFT HAND TOOL)

o101 elseif[#<P> EQ 9]
#105=-4.674 
G49G94
G91
G38.2 Z.2F5.
G0Z-.2
G38.2 Z.2F5.
#101=[#5063+#105]
G0Z-.2
G90G49
G10 L1 P#5400 Z#101
o101 endif

#<P>=0 

o<m275> endsub
M30
The following user(s) said Thank You: spumco, endian

Please Log in or Create an account to join the conversation.

More
2 years 9 months ago #292061 by endian
hello,

Ive already create dry program for my manual toolchange 4 direction tool probe... but not yet tested because I am out off the shop.. should it be working from you point of view?
Code:
o<m275> sub (master tool number) #<_toolNumberMaster> = 0 (axis reference number) #<_xAxisNumber> = 1 (#<_yAxisNumber> = 2) #<_zAxisNumber> = 3 (etc...) (tool orientation for probing directions) #<_toolOrientation1> = 1 #<_toolOrientation2> = 2 #<_toolOrientation3> = 3 #<_toolOrientation4> = 4 #<_toolOrientation5> = 5 #<_toolOrientation6> = 6 #<_toolOrientation7> = 7 #<_toolOrientation8> = 8 #<_toolOrientation9> = 9 (default probing stroke) #<_probingStrokeDefault> = 50.0 (calibration move off stroke) <_calibrationMoveOffStroke> = 0.5 (move off probe stroke) #<_moveOffProbeStroke> = 5.0 (reference value of axis - for lathe 1/2 of wanted value - X10 == D20) #<_xReference> =  24.0 (#<_yReference> = number here) #<_zReference> = 0.0 (tool orientation low limit) #<_toolOrientationLowLimit> = 1 (feed of probing) #<_roughtProbingSpeed> = 500.0 #<_finalProbingSpeed> = 10.0 (tool number) #<_toolNumber> = #5400 (tool orientation 1 - 9) #<_toolOrientation> = #5413 (axis in which probing) #<_probingAxis> = #<P> (aproximation lenght of probing stroke in UU) #<_probingStroke> = #<Q> (actual coordination system) #<_actualCoordSystem> = #5220 (probing order M275 P1 - Xprobing in default lenght uu) (probing order M275 P1 Q150 - Xprobing in 150uu) (probing order M275 P3 q80 - Zprobing in 80uu)          o108 if[#<_probingStroke> LE 0]         #<_probingStroke> = #<_probingStrokeDefault>     o108 endif              o110 if[#<_probingAxis> EQ #<_xAxisNumber> OR #<_probingAxis> EQ #<_zAxisNumber>]    (check if your probing order is right)         o120 if[#<_toolOrientation> GE #<_toolOrientationLowLimit>]    (check right configuration of tool table)                      G94             G91             G49             #<_actualCoordSystem> = #5220                           o130 if[#<_toolOrientation> EQ #<_toolOrientation1> OR #<_toolOrientation> EQ #<_toolOrientation2> OR #<_toolOrientation> EQ #<_toolOrientation6> OR #<_toolOrientation> EQ #<_toolOrientation5]                 #<_probingStroke> = #<_probingStroke>                 <_calibrationMoveOffStroke> = <_calibrationMoveOffStroke>             o130 elseif[#<_toolOrientation> EQ #<_toolOrientation3> OR #<_toolOrientation> EQ #<_toolOrientation4> OR #<_toolOrientation> EQ #<_toolOrientation8> OR #<_toolOrientation> EQ #<_toolOrientation7]                 #<_probingStroke> = -#<_probingStroke>                 <_calibrationMoveOffStroke> = -<_calibrationMoveOffStroke>             o130 else                 (#########################################call error for the lathe setup)                 #<P>=0                  #<Q>=0                  M2             o130 endif                                       o200 if[#<_toolNumber> GT #<_toolNumberMaster>] (check which number of tool are already inserted)                 o300 if[#<_probingAxis> EQ #<_xAxisNumber>](other tools then master)                     G38.2 X-#<_probingStroke> F#<_roughtProbingSpeed>                     G1 X<_calibrationMoveOffStroke>                     G38.2 X-#<_probingStroke> F#<_finalProbingSpeed>                     G0 X#<_moveOffProbeStroke>                     #<probingSuccesfull> = #5070                     o350 if[#<probingSuccesfull> EQ 1]                         #<axisActualProbeOffset> = #5061                         #<axisOffet> = [[#<axisActualProbeOffset> + #<_xReference>] * 2]                         G90                         G49 $                        G10 L1 P#<_toolNumber> X#<axisOffet>                     o350 else                         (#########################################call an error of probing )                                             (MSG,Probing in X direction error.)                         #<P>=0                          #<Q>=0                          M2                     o350 endif                 o300 elseif[#<_probingAxis> EQ #<_zAxisNumber>]                     G38.2 Z-#<_probingStroke> F#<_roughtProbingSpeed>                     G1 Z<_calibrationMoveOffStroke>                     G38.2 Z-#<_probingStroke> F#<_finalProbingSpeed>                     G0 Z#<_moveOffProbeStroke>                     #<probingSuccesfull> = #5070                     o360 if[#<probingSuccesfull> EQ 1]                                             #<axisActualProbeOffset> = #5063                         #<axisOffet> = [#<axisActualProbeOffset> + #<_zReference>]                         G90                         G49 $                        G10 L1 P#<_toolNumber> Z#<axisOffet>                     o360 else                         (#########################################call an error of probing )                                             (MSG,Probing in Z direction error.)                         #<P>=0                          #<Q>=0                          M2                     o360 endif                 o300 endif                                              o200 else                 o400 if[#<_probingAxis> EQ #<_xAxisNumber>]                (master tool reference setup for T0 - find to where probe is located)                     G38.2 X-#<_probingStroke> F#<_roughtProbingSpeed>                     G1 X<_calibrationMoveOffStroke>                     G38.2 X-#<_probingStroke> F#<_finalProbingSpeed>                     G0 X#<_moveOffProbeStroke>                     #<probingSuccesfull> = #5070                     o450 if[#<probingSuccesfull> EQ 1]                             G90                         G49                         G4 P0.5                         #<axisOffet> = [#<_xReference> * 2] $                        G10 L2 P#<_actualCoordSystem> X#<axisOffet>                     o450 else                         (#########################################call an error of probing )                                             (MSG,Probing in X direction error.)                         #<P>=0                          #<Q>=0                          M2                     o450 endif                                      o400 elseif[#<_probingAxis> EQ #<_zAxisNumber>]                     G38.2 Z-#<_probingStroke> F#<_roughtProbingSpeed>                     G1 Z<_calibrationMoveOffStroke>                     G38.2 Z-#<_probingStroke> F#<_finalProbingSpeed>                     G0 X#<_moveOffProbeStroke>                     #<probingSuccesfull> = #5070                     o460 if[#<probingSuccesfull> EQ 1]                                                 G90                         G49                         G4 P0.5                         #<axisOffet> = #<_zReference> $                        G10 L2 P#<_actualCoordSystem> Z#<axisOffet>                     o460 else                         (#########################################call an error of probing )                                             (MSG,Probing in Z direction error.)                         #<P>=0                          #<Q>=0                          M2                     o460 endif                                      o400 endif                 o200 endif         o120 else             (#########################################call an error of wrong configuration of tool table)             (MSG,Probing error. Wrong tool setup in the tooltable.)             #<P>=0              #<Q>=0              M2         o120 endif     o110 else         (#########################################call an error of wrong configuration of #<P> parameter in the macro MDI call)         (MSG,Probing error. Wrong macro call configuration.)         #<P>=0          #<Q>=0          M2     o110 endif #<P>=0  #<Q>=0  o<m275> endsub M30

I do no know have many conditions should be in the row or in the single expresion ... do you know it please?

regards
The following user(s) said Thank You: smc.collins

Please Log in or Create an account to join the conversation.

Time to create page: 0.353 seconds
Powered by Kunena Forum
