Kitamura Mycenter 0 ATC ARM Help

More
6 years 8 months ago #156772 by drimaropoylos
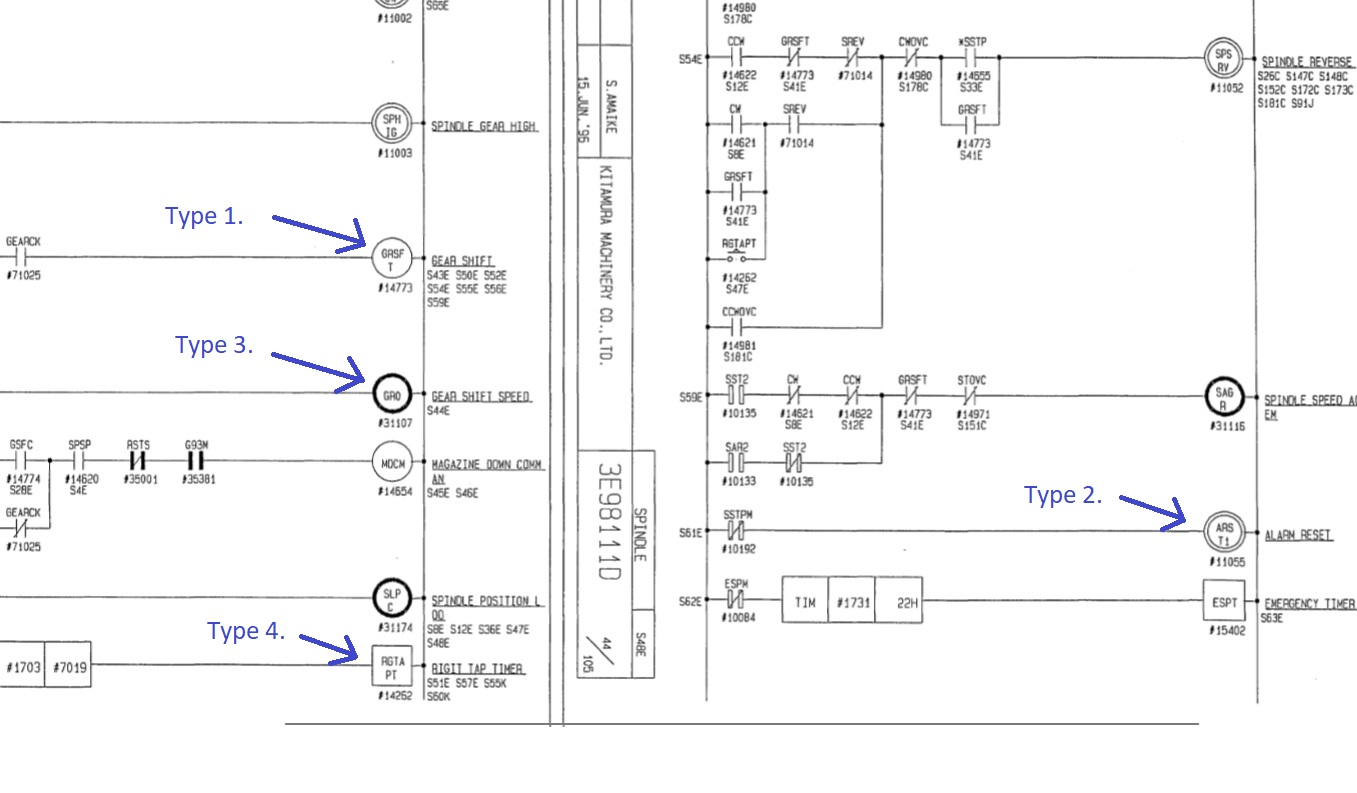
A few thing that may help you. They are different types of “relays” in the ladder schematics
1. ladder internal relays to build the logic
2. output relays for control components of the machine
3. output relays witch they are inputs to the cnc controller
4. the square stuff witch they are timers

Please Log in or Create an account to join the conversation.
More
6 years 8 months ago #156774 by drimaropoylos
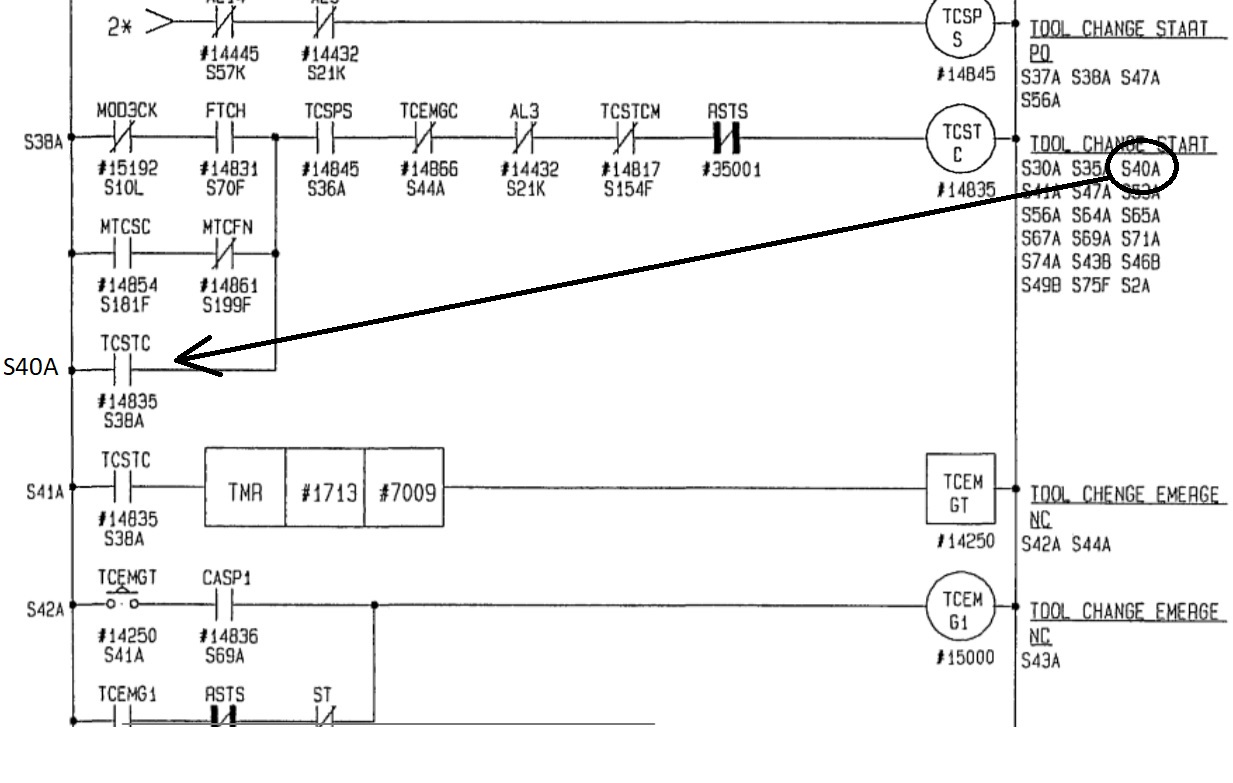
Every relay has a number and the numbers below the description of the relay is the place of the contacts of that relay.
The following user(s) said Thank You: DaOne

Please Log in or Create an account to join the conversation.

More
6 years 8 months ago #156778 by drimaropoylos
10044 tells the plc to slow down the arm because is close to the tool holder
10040 tells the plc that the tool holder is clamped and it is ok to proceed to relise the tool and continue with the rest of the arm movement
10081 tells the plc that the arm is in home position and the program may continue
John
The following user(s) said Thank You: DaOne, tommylight

Please Log in or Create an account to join the conversation.

More
6 years 8 months ago #156782 by DaOne
John, thank you! For the most part I figured out the way to read the ladder logic. (Just hard for my mind to follow it) I do need to figure out the timer blocks however. I am thinking I might just start putting this whole thing into classic ladder and watch how its working. I am worried that timing is super critical. The actual tool change on this machine is super fast. Under .8 of a second.

Things I am still trying to figure out...
*Does it only go in one direction or does it change direction in some point of the cycle? Trying to understand why there is a CW and a CCW?
*Does it use the timers in the later logic as delays for the proximity sensors?
*The timer blocks.. What does the first and 2nd value actually mean? I have the values but no idea what the represent. On delay off delay?
*In classic ladder fast enough to handle timings like this if thats whats required?

Please Log in or Create an account to join the conversation.

More
6 years 8 months ago #156788 by drimaropoylos
The arm can only go CW from the home position to the holder, and can only go CCW from the holder to the home position, so both way are needed. The swap of the tools can be done CW or CCW.
John

Please Log in or Create an account to join the conversation.

More
6 years 8 months ago - 6 years 8 months ago #156790 by drimaropoylos
They are a lot of use for a timer in ladder , In S41A the timer counts the time it takes for the tool change to complete and if it is not complete in a certain amount of time then it stops the tool change.
Last edit: 6 years 8 months ago by drimaropoylos.

Please Log in or Create an account to join the conversation.

Time to create page: 0.156 seconds
Powered by Kunena Forum