

- Posts: 18
- Thank you received: 7
Avon 3000 Mill retrofit
11 months 1 week ago #339217
by zoeper
Replied by zoeper on topic Avon 3000 Mill retrofit
I could not get Linuxcnc to launch on Mint. This could have been due to me not setting up the Hal and ini files correctly. I switched back to my old installation and it now seems stable. PNCConf was the key to get me up and running, Thanks!
Please Log in or Create an account to join the conversation.
11 months 1 week ago #339220
by zoeper
Replied by zoeper on topic Avon 3000 Mill retrofit
I spent a lot of time studying the machine schematics and have a decent grasp of the workings thereof.
I removed the old Anilam GXM control, screen and manual control panel. The MESA 7i77 connected up to the encoders and I can read XYZ in the DRO screen. I can plot W in the HAL Scope, but it does not show on the DRO yet. (I think I selected encoder as rotary axis in PNCConf and will sort this out later.)
I now want to start connecting the limit switches and other IO's but have some things I am not clear on.
On the schematic attached:
D_A/18 and EXP/18 (37) would connect to V-Field on TB2
D_A/17 and EXP/17 (00) would connect to Ground on TB2
D-A/21, D-A/24, D-A/26, EXP/22 can be ignored for now. Was only pulled high to prevent fault condition for axis not in use on GXM
D-A/23 (83) is a input to indicate E-Stop active when not high.
D-A/25 (62) is a input to indicate Lubrication unit fail. (Feed Hold/ External Stop)
D-A/22 (820) is a input to indicate no axis overtravel and E-stop out.
D-A/26 (87) X Positive vector (Input)
D-A/24 (88) X Negative vector (Input)
D-A/23 (89) Y Positive vector (Input)
D-A/25 (90) Y Negative vector (Input)
D-A/19 (91) Z Positive vector (Input)
D-A/21 (92) Z Negative vector (Input)
D-A/09 (81) E-Stop Out and Reset Pressed (Input)
D-A/02 (72) M8 Coolant Off (Output, Drain)
D-A/08 (69) M5 Spindle Stop(Output, Drain)
D-A/04 (71) M7 Coolant On (Output, Drain)
D-A/12 (67) M3 Spindle Forward (Output, Drain)
D-A/10 (68) M4 Spindle Reverse (Output, Drain)
D-A/06 (70) M6 Tool Override (Output, Drain)
EXP/10 (236) "M Strobe" (Output, Drain)
EXP/20 (230) "Fin" (Output, Drain)
EXP/14 (235) "S Strobe" (Output, Drain)
EXP/06 (2311) "T Strobe" (Output, Drain)
Once I can get the limits and E-Stop circuits connected, I should be able to connect the motors and start tuning them.
Any thoughts or comments welcome.
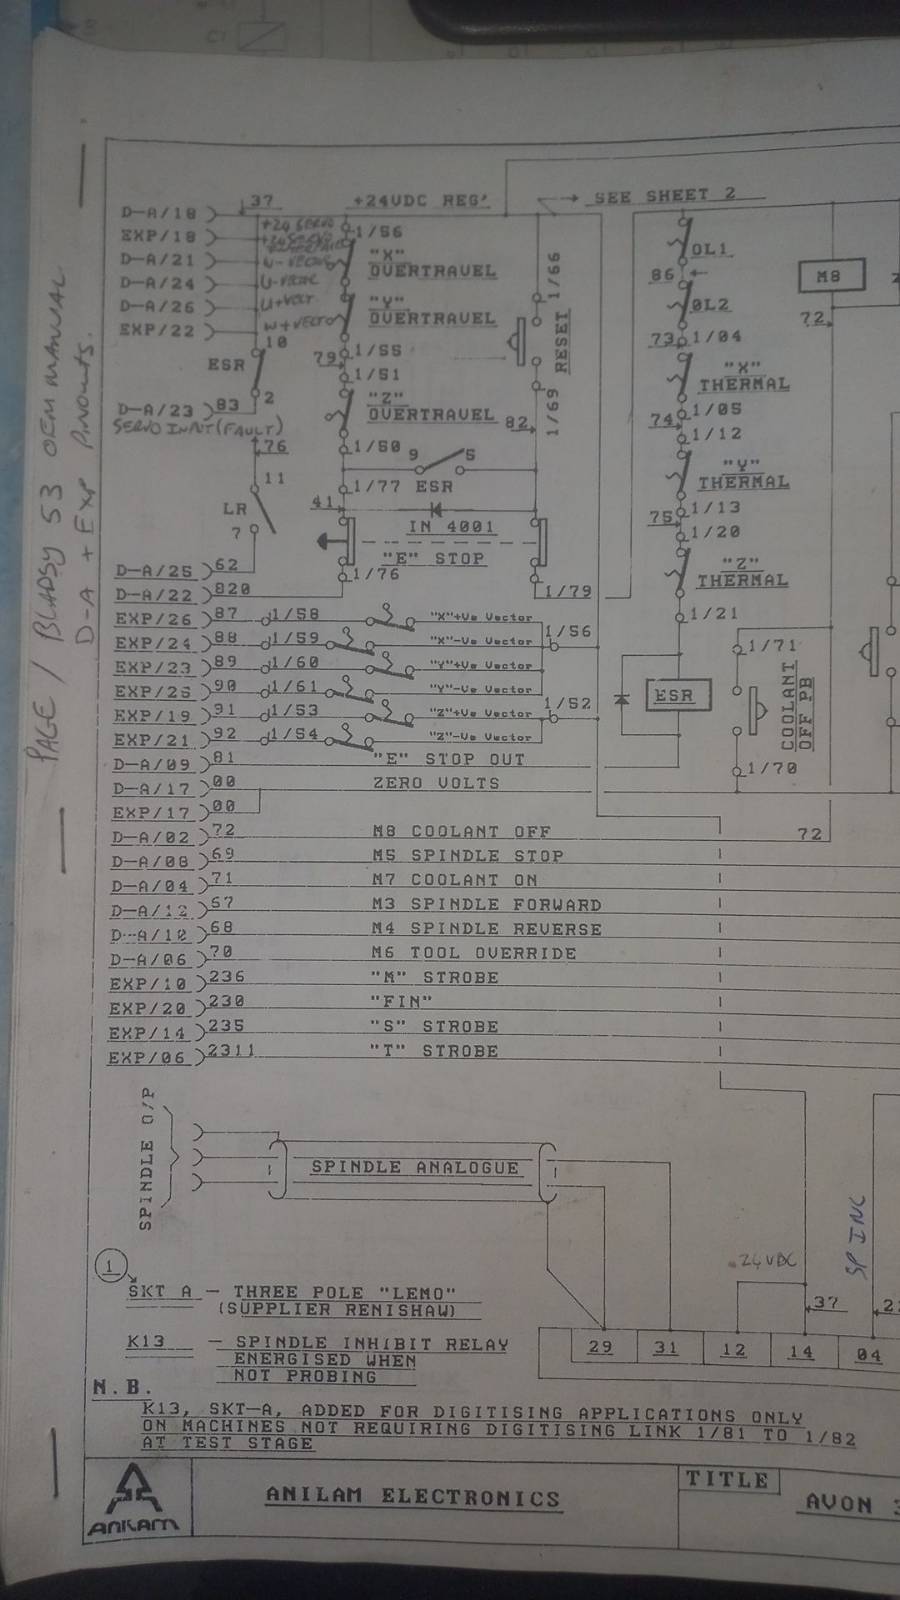
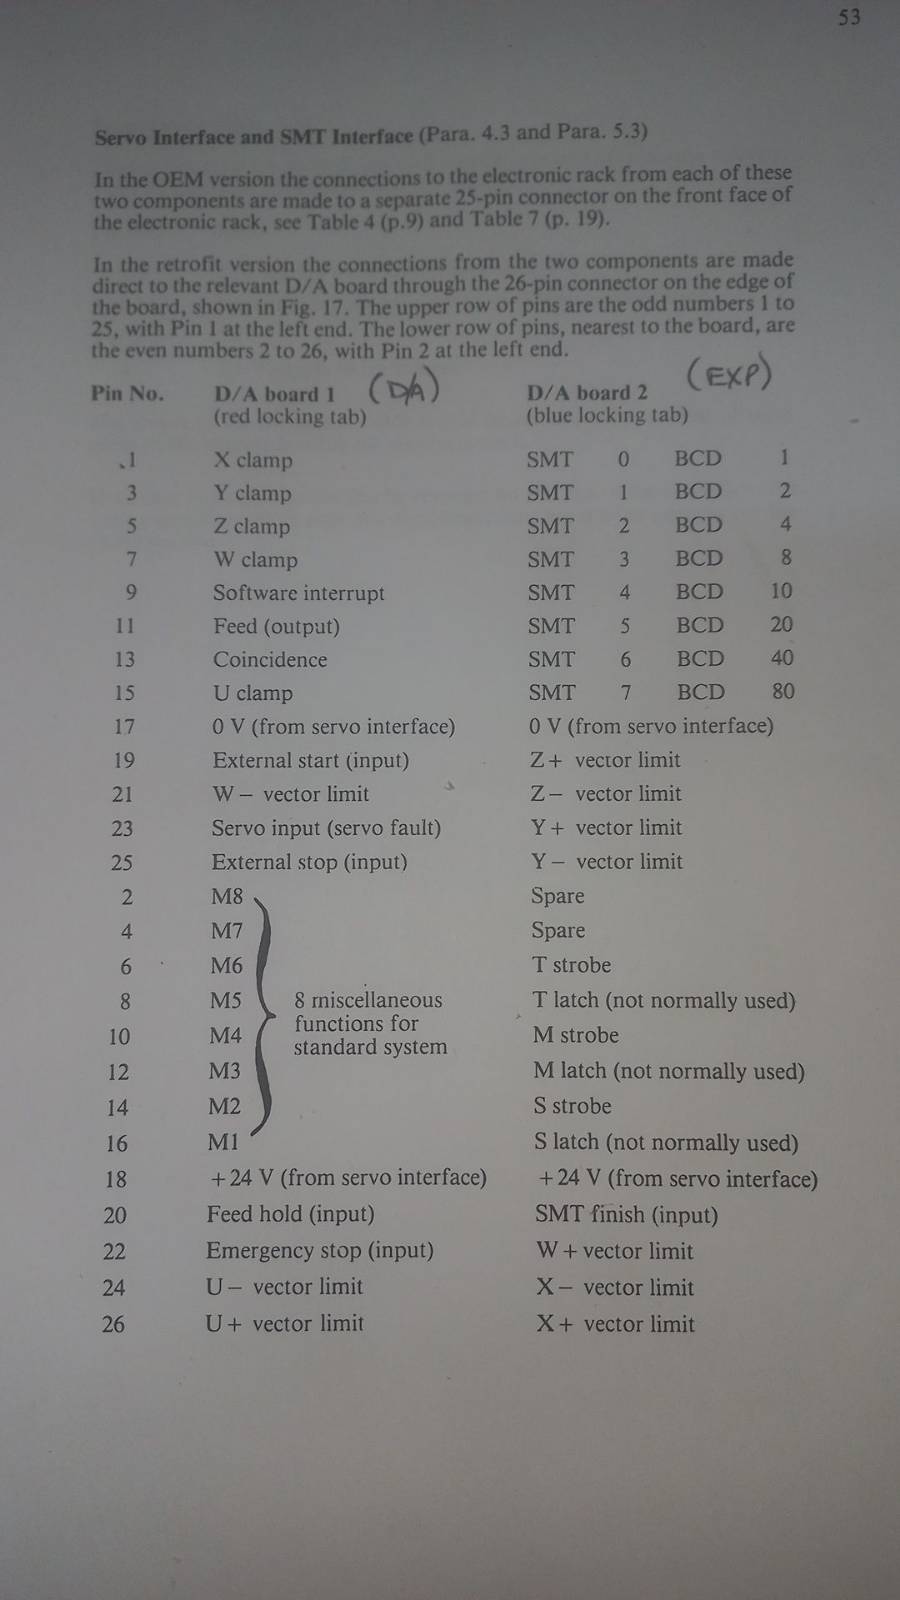
I removed the old Anilam GXM control, screen and manual control panel. The MESA 7i77 connected up to the encoders and I can read XYZ in the DRO screen. I can plot W in the HAL Scope, but it does not show on the DRO yet. (I think I selected encoder as rotary axis in PNCConf and will sort this out later.)
I now want to start connecting the limit switches and other IO's but have some things I am not clear on.
On the schematic attached:
D_A/18 and EXP/18 (37) would connect to V-Field on TB2
D_A/17 and EXP/17 (00) would connect to Ground on TB2
D-A/21, D-A/24, D-A/26, EXP/22 can be ignored for now. Was only pulled high to prevent fault condition for axis not in use on GXM
D-A/23 (83) is a input to indicate E-Stop active when not high.
D-A/25 (62) is a input to indicate Lubrication unit fail. (Feed Hold/ External Stop)
D-A/22 (820) is a input to indicate no axis overtravel and E-stop out.
D-A/26 (87) X Positive vector (Input)
D-A/24 (88) X Negative vector (Input)
D-A/23 (89) Y Positive vector (Input)
D-A/25 (90) Y Negative vector (Input)
D-A/19 (91) Z Positive vector (Input)
D-A/21 (92) Z Negative vector (Input)
D-A/09 (81) E-Stop Out and Reset Pressed (Input)
D-A/02 (72) M8 Coolant Off (Output, Drain)
D-A/08 (69) M5 Spindle Stop(Output, Drain)
D-A/04 (71) M7 Coolant On (Output, Drain)
D-A/12 (67) M3 Spindle Forward (Output, Drain)
D-A/10 (68) M4 Spindle Reverse (Output, Drain)
D-A/06 (70) M6 Tool Override (Output, Drain)
EXP/10 (236) "M Strobe" (Output, Drain)
EXP/20 (230) "Fin" (Output, Drain)
EXP/14 (235) "S Strobe" (Output, Drain)
EXP/06 (2311) "T Strobe" (Output, Drain)
Once I can get the limits and E-Stop circuits connected, I should be able to connect the motors and start tuning them.
Any thoughts or comments welcome.
Please Log in or Create an account to join the conversation.
11 months 2 days ago #339528
by zoeper
Replied by zoeper on topic Avon 3000 Mill retrofit
I managed to make some progress this weekend.
I can now command all 3 axis. Motors are hunting a bit, but I will send time to tune them later. Servo drives/ motors have a high pitch noise when enabled, but I will live with that till I can upgrade to brushless DC servos at a later date.
Next would be to connect rest of the IO and get it to interact with linuxcnc.
Really happy to have things moving on command and grateful for the help from members here!
Good week to all
I can now command all 3 axis. Motors are hunting a bit, but I will send time to tune them later. Servo drives/ motors have a high pitch noise when enabled, but I will live with that till I can upgrade to brushless DC servos at a later date.
Next would be to connect rest of the IO and get it to interact with linuxcnc.
Really happy to have things moving on command and grateful for the help from members here!
Good week to all
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
10 months 4 weeks ago #339660
by zoeper
Replied by zoeper on topic Avon 3000 Mill retrofit
My ears have their own ring, so I get used to things like that easily. I would however love to dump the 30+ year old DC servos and Amps in favour of something more modern. Looking at the complexity of my electrical cabinet in comparison to modern systems makes me think there is room for improvement too. If I can get it up and running first, at least it can make some money to pay for its own upgrades. 
Please Log in or Create an account to join the conversation.
10 months 2 weeks ago - 10 months 2 weeks ago #340122
by zoeper
Replied by zoeper on topic Avon 3000 Mill retrofit
Hi All,
At some point the S-code could be used to command the spindle speed. The control sends an analog voltage to the LARRIOZ speed control card. The card reads a sensor that counts spindle revolutions and compares it to the commanded speed. The card can then switch relays, that in turn switch the contactors driving the motorized CVT transmission between spindle and spindle motor to increase/ decrease the spindle speed as required.
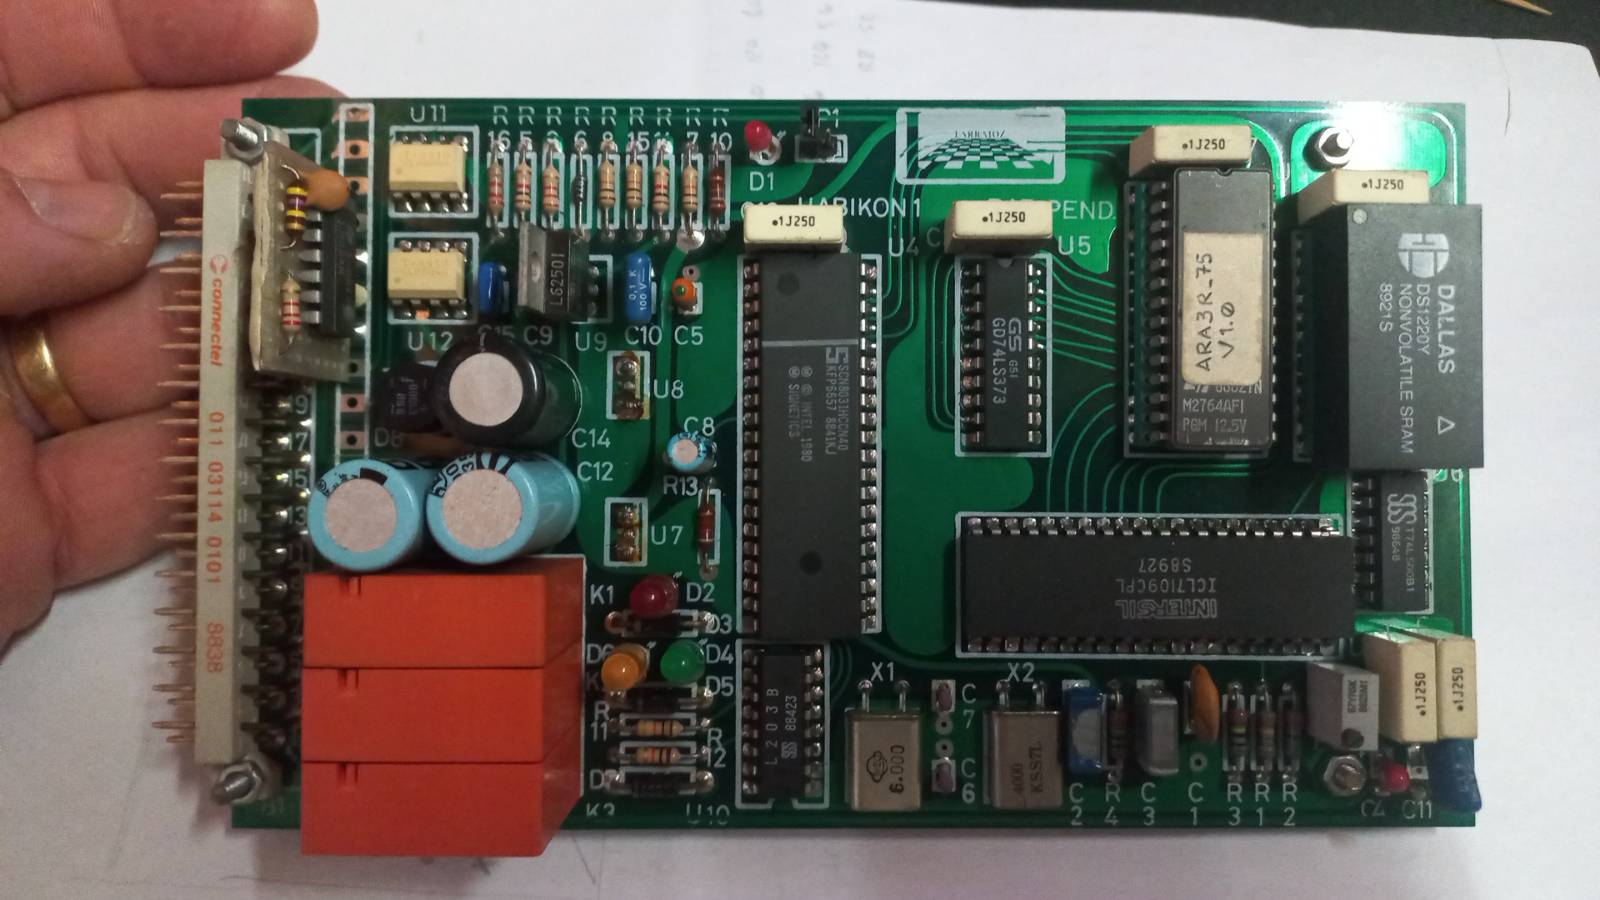
This never worked since I got the mill. I did at the time try to get it to work, but due to lack of knowledge and/ or documentation, I could not get working. I would think that the lithium battery in the Dallas non-volatile SRAM would be long gone, but I am not sure what would be stored in SRAM. I assume (While I know not to assume anything) that the firmware would live on the EPROM and the SRAM might hold parameters relating to the specific installation. Other than JP 1(Jumper), and P1 (Potentiometer) there is no other configuration or programming port on the LARRIOZ HABIKON1 board.
Although slow, I prefer this system, as I would not sacrifice low speed torque, as would be the case with using only a VFD for speed control.
I suppose it would be fairly easy with modern microcontrollers to get the system going again, but I would be happy to hear from others as to their experience or suggestions as to how I should proceed.
Regards
P
At some point the S-code could be used to command the spindle speed. The control sends an analog voltage to the LARRIOZ speed control card. The card reads a sensor that counts spindle revolutions and compares it to the commanded speed. The card can then switch relays, that in turn switch the contactors driving the motorized CVT transmission between spindle and spindle motor to increase/ decrease the spindle speed as required.
This never worked since I got the mill. I did at the time try to get it to work, but due to lack of knowledge and/ or documentation, I could not get working. I would think that the lithium battery in the Dallas non-volatile SRAM would be long gone, but I am not sure what would be stored in SRAM. I assume (While I know not to assume anything) that the firmware would live on the EPROM and the SRAM might hold parameters relating to the specific installation. Other than JP 1(Jumper), and P1 (Potentiometer) there is no other configuration or programming port on the LARRIOZ HABIKON1 board.
Although slow, I prefer this system, as I would not sacrifice low speed torque, as would be the case with using only a VFD for speed control.
I suppose it would be fairly easy with modern microcontrollers to get the system going again, but I would be happy to hear from others as to their experience or suggestions as to how I should proceed.
Regards
P
Last edit: 10 months 2 weeks ago by zoeper.
The following user(s) said Thank You: NWE
Please Log in or Create an account to join the conversation.

10 months 2 weeks ago #340145
by NWE
Replied by NWE on topic Avon 3000 Mill retrofit
Can you find any specs on the motor that drives the CVT adjuster? Maybe even a pic. of its nameplate. I suspect something should be available for it. Using a VFD for speed control a person can gain some low end torque using closed loop speed feedback and PID, but the CVT on my Wilton mill certainly has a lot more low speed torque than I was able get with just a vfd on another project.
Please Log in or Create an account to join the conversation.
Time to create page: 0.057 seconds