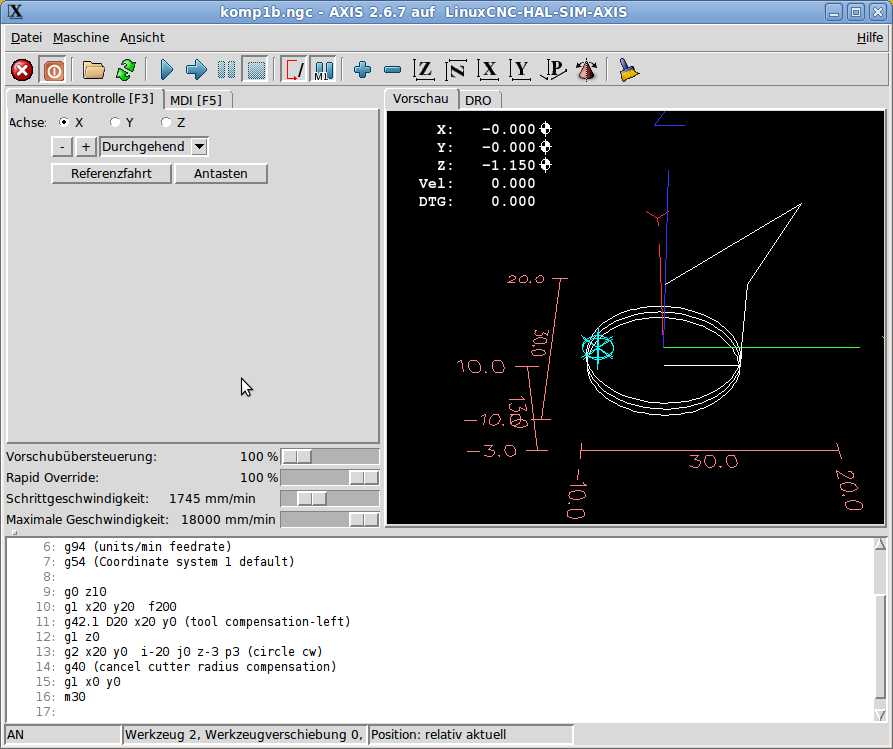
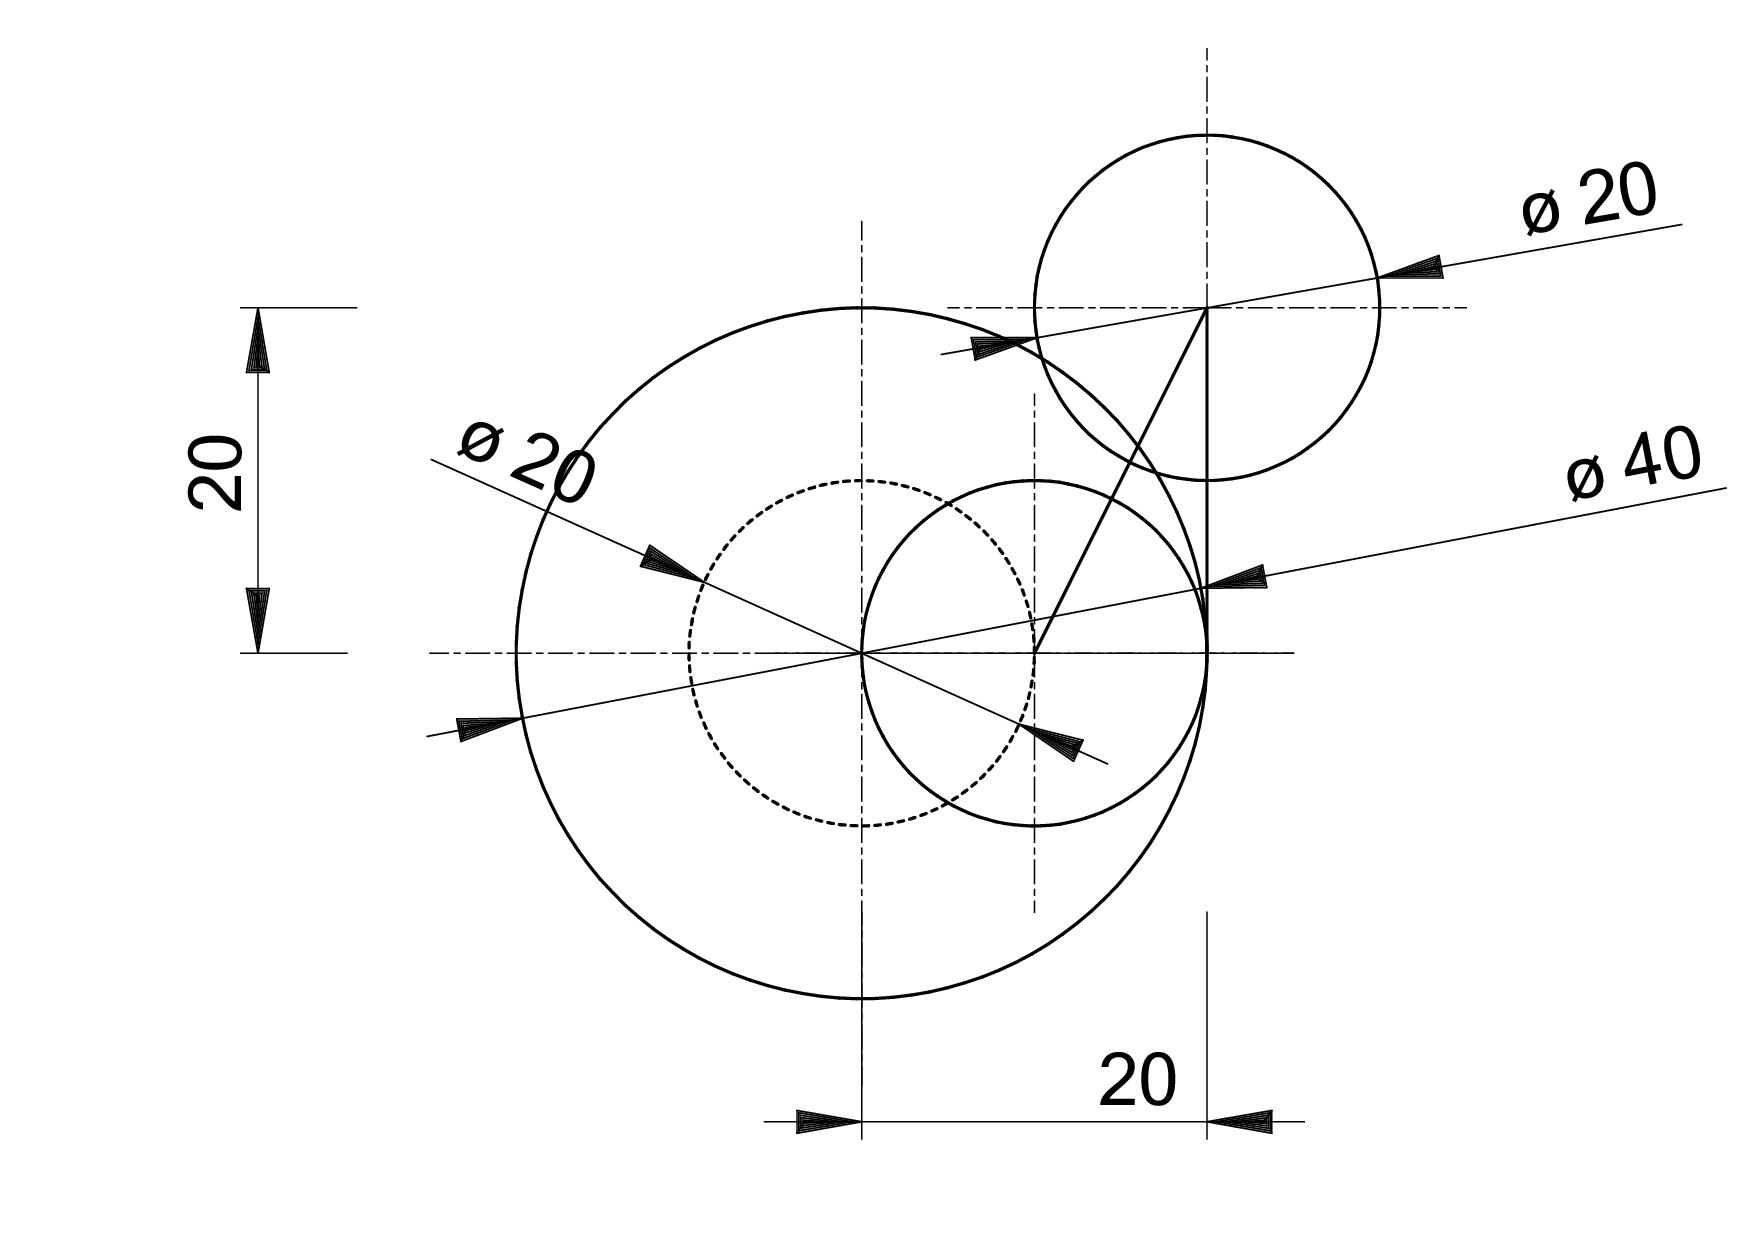
What is best practice for a linear initailal move if I want to make a round pocket. (tool diameter is greater then the pocket radius)
What I did:
Code:
g17 (xy plane)
g21 (mm)
g40 (cancel cutter radius compensation)
g49 (cancel tool lengthoffset)
g90 (absolute distance mode)
g94 (units/min feedrate)
g54 (Coordinate system 1 default)
g0 z10
g1 x20 y20 f200
g42.1 D20 x20 y0 (tool compensation-left)
g1 z0
g2 x20 y0 i-20 j0 z-3 p3 (circle cw)
g40 (cancel cutter radius compensation)
g1 x0 y0
m30
Question:
1. What is best practise for this move if the tool diameter is greater then the pocket radius?
2. Is there a way to make the compensation move complete inside the pocket?