Anyone with succesful Rack Type Tool Changer with Auto Tool length probe ?

More
7 years 6 months ago #131756 by marq_torque
Thanks for guidance,

If i am not wrong you suggesting me additional code for touch probe after tool change? If it is then i tried same method back time in mach 3 i issed M6T# and later M177 for tool touch. and at this time i am not able to get customised M code output in my cam system and also need it little simple so wanted to clup this touch probe routine in M6T# code. If any help ??

Regards,
Ankit

Please Log in or Create an account to join the conversation.
More
7 years 6 months ago #131770 by andypugh
The sample config is set up so that M6 calls a G-code subroutine.
(rack_change.ngc, linked to above)
You would modify that routine to also do a tool length probe, and to set the new calculated length in the tool table with an G10 command.
linuxcnc.org/docs/2.7/html/gcode/g-code.html#gcode:g10-l1
Note the different functions of G10 L1, G10 L2, G10 L10 and G10 L11.

I think that you would just make a probe move to the touch-plate then issue a G10 L10 Znn where nn is the known position of the touch plate (possibly in an otherwise unused coordinate system).

To allow for different slot locations, I think I would use the U,V colums of the tool table as the tool location.
The following user(s) said Thank You: marq_torque

Please Log in or Create an account to join the conversation.

More
7 years 6 months ago #131773 by marq_torque
Hello AndyPugh,

Thanks for responding, yes i m understanding what you suggested.

1) Can you explain how to activate Pneumatic cylinder using parallel port configuration to declamp tool how to setup output pin delay and all ? I m not able to find any details of output.

2) Also in last lines you said that tool table decides tool pocket Location, if i am using that tool table so what lines to remove in INI ? Or am i understanding wrong ?


Regards,
Ankit

Please Log in or Create an account to join the conversation.

More
7 years 6 months ago #131774 by marq_torque
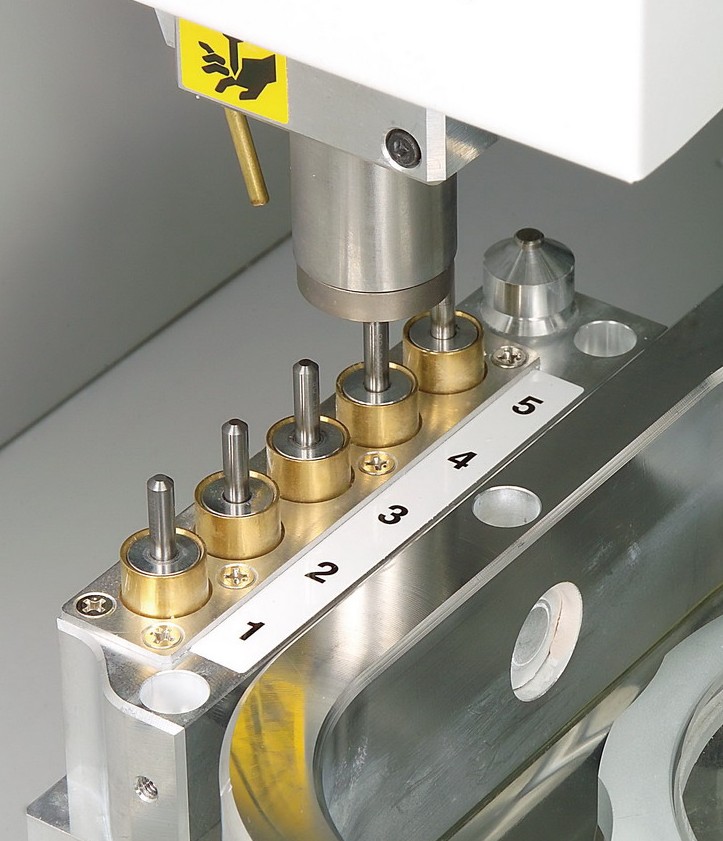
This is tool rack for my machine, last one is tool touch probe. These pockets have inaccurate repeatability length wise.
So cant save tools for entire day jobs. And i want this to be idiot proof so not adding extra codes in part program manually.

Thanks,
Ankit

Please Log in or Create an account to join the conversation.

More
7 years 6 months ago #131775 by andypugh

marq_torque wrote: 1) Can you explain how to activate Pneumatic cylinder using parallel port configuration to declamp tool how to setup output pin delay and all ? I m not able to find any details of output.


Use a G-code digital output
Code:
net tool-clamp motion.digital-out-00 => parport.0.pin-00-out


2) Also in last lines you said that tool table decides tool pocket Location,


I didn't say that. I said that it could.

If you load the selected tool and do a g43 then the parameters #5401 to #5409 will take the values from the tool table.
You aren't using UVW so you could use those tool table entries to hold the pocket locations for each tool and move there with a G53 absolute move.
Code:
G53 G0 X#5407 Y#5408
The following user(s) said Thank You: marq_torque

Please Log in or Create an account to join the conversation.

More
7 years 6 months ago #131777 by marq_torque
Great,

I m trying it just in a while.

Thanks,
Ankit

Please Log in or Create an account to join the conversation.

Time to create page: 0.066 seconds
Powered by Kunena Forum
