
Round Corners
- creisey
-
 Topic Author
- Offline
- New Member
-

Less
More
- Posts: 16
- Thank you received: 1
29 Sep 2020 14:40 #184299
by creisey
Round Corners was created by creisey
Hello together
im facing since lately this issue:
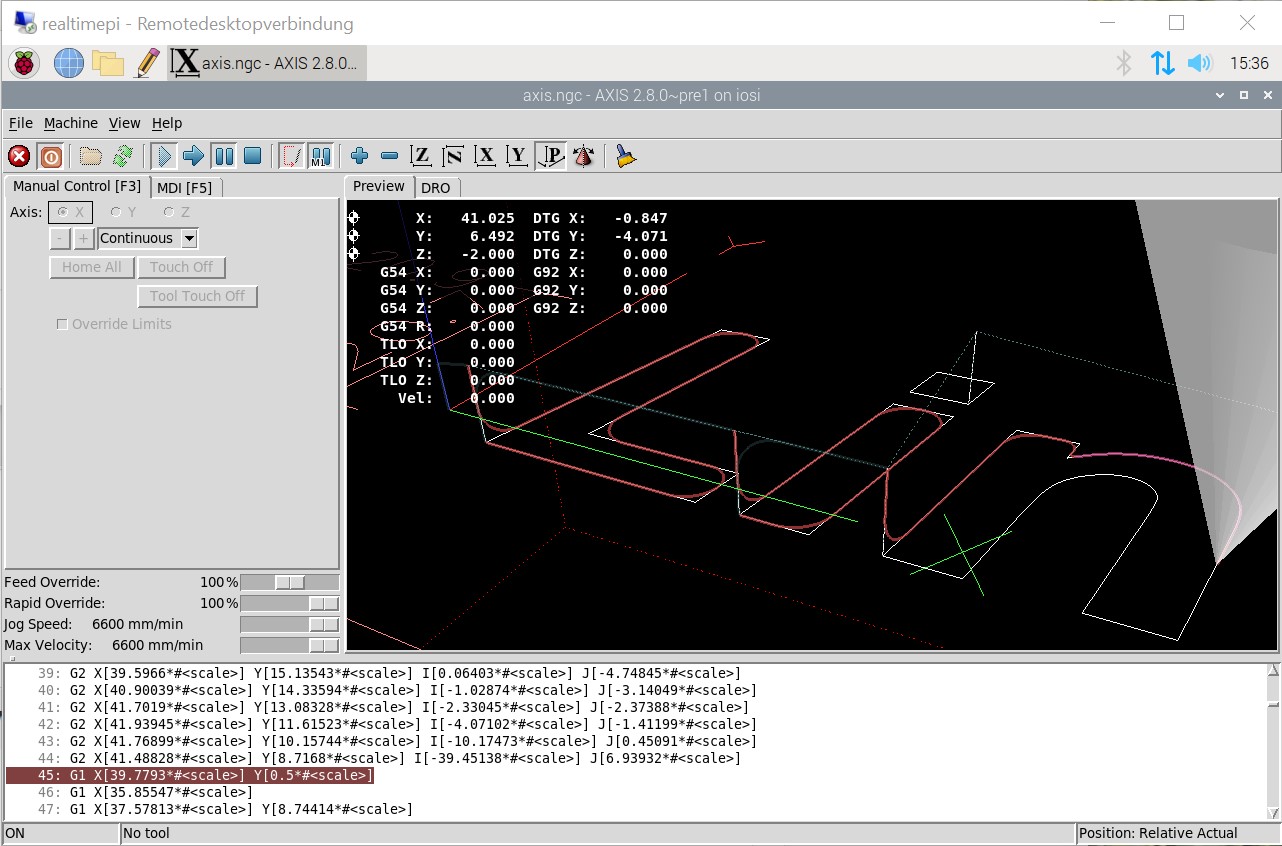
instead of going into the edge, the machine makes a round corner.
i have read about putting G64 PX in the beginning and it works.
BUT! it insanely slows down!
is there another way to get a better result?
thx for your help
im facing since lately this issue:
instead of going into the edge, the machine makes a round corner.
i have read about putting G64 PX in the beginning and it works.
BUT! it insanely slows down!
is there another way to get a better result?
thx for your help
Please Log in or Create an account to join the conversation.
- tommylight
-
- Away
- Moderator
-

Less
More
- Posts: 21922
- Thank you received: 7468
29 Sep 2020 16:20 #184307
by tommylight
Replied by tommylight on topic Round Corners
Raise the acceleration in the ini file.
Please Log in or Create an account to join the conversation.
- Todd Zuercher
-
- Offline
- Platinum Member
-

Less
More
- Posts: 4782
- Thank you received: 1472
29 Sep 2020 19:04 - 29 Sep 2020 19:15 #184321
by Todd Zuercher
Replied by Todd Zuercher on topic Round Corners
The reason the machine is slowing down is because at a corner one axis must decelerate to a stop and the other must accelerate from stopped to the feed rate, but at the point there will be an instant of full stopped.
The G64 Pn setting sets a tolerance to how close the movement must come to the programmed path. G64 with no P tolerance is infinite blending and the corners will be rounded to their maximum for the machines acceleration settings.
It is simple physics and geometry you can't make a square corner without stopping. If you round the corner you can go faster, and the faster you can accelerate the less rounded the corner must be to maintain a certain speed around it.
You have to work out a compromise to determine what G64Pn setting will give you the fastest possible speed, yet still maintain an acceptable tolerance for your work. The larger Pn is the faster and more rounded the machine can go around the corners, if Pn is smaller the rounding will be less, but it will take more time.
G64Pn where n=the minimum resolution of the machine (such as 0.0001inches), might be a good setting for extremely precise work. 50-100 times that is usually a pretty good compromise that usually won't make noticeable deviations on a machine like a wood router.
The G64 Pn setting sets a tolerance to how close the movement must come to the programmed path. G64 with no P tolerance is infinite blending and the corners will be rounded to their maximum for the machines acceleration settings.
It is simple physics and geometry you can't make a square corner without stopping. If you round the corner you can go faster, and the faster you can accelerate the less rounded the corner must be to maintain a certain speed around it.
You have to work out a compromise to determine what G64Pn setting will give you the fastest possible speed, yet still maintain an acceptable tolerance for your work. The larger Pn is the faster and more rounded the machine can go around the corners, if Pn is smaller the rounding will be less, but it will take more time.
G64Pn where n=the minimum resolution of the machine (such as 0.0001inches), might be a good setting for extremely precise work. 50-100 times that is usually a pretty good compromise that usually won't make noticeable deviations on a machine like a wood router.
Last edit: 29 Sep 2020 19:15 by Todd Zuercher.
The following user(s) said Thank You: tommylight, creisey, fernandosf
Please Log in or Create an account to join the conversation.
- fulberfulber77@gmail.com
- Offline
- New Member
-
Less
More
- Posts: 1
- Thank you received: 0
07 Sep 2026 12:41 #349423
by fulberfulber77@gmail.com
Replied by fulberfulber77@gmail.com on topic Round Corners
Em vez de seguir pela borda, a máquina faz uma curva arredondada.
Li sobre usar o comando G64 PX no início e funciona.
MAS! Fica absurdamente lento!
Existe outra maneira de obter um resultado melhor?
Li sobre usar o comando G64 PX no início e funciona.
MAS! Fica absurdamente lento!
Existe outra maneira de obter um resultado melhor?
Please Log in or Create an account to join the conversation.
- Todd Zuercher
-
- Offline
- Platinum Member
-
Less
More
- Posts: 4782
- Thank you received: 1472
08 Sep 2026 11:28 - 08 Sep 2026 11:38 #349456
by Todd Zuercher
Replied by Todd Zuercher on topic Round Corners
Unfortunately no. Linuxcnc must follow the acceleration settings you used in your machine configuration. If your acceleration settings are too slow for your machine you can increase them. But if they are already set as fast as your machine can go, the only other option is to rewrite your g-code to be smoother so the machine does not need to stop and start so much.
Another consideration would be if your G-code has a lot of transitions from short G0 moves short to cutting moves. This can cause serious slowdowns because those transitions are treated as full stop positioning moves with no blending. They are the equivalent of programming in G61 mode instead of G64Pn. (Actually I think all G0 moves are full stop positioning moves.) Sometimes changing all G0 moves to G1 moves can significantly improve runtimes.
Another consideration would be if your G-code has a lot of transitions from short G0 moves short to cutting moves. This can cause serious slowdowns because those transitions are treated as full stop positioning moves with no blending. They are the equivalent of programming in G61 mode instead of G64Pn. (Actually I think all G0 moves are full stop positioning moves.) Sometimes changing all G0 moves to G1 moves can significantly improve runtimes.
Last edit: 08 Sep 2026 11:38 by Todd Zuercher.
Please Log in or Create an account to join the conversation.
Time to create page: 0.109 seconds