Reset machine coordinates on special machine.

More
4 years 3 months ago - 4 years 3 months ago #247694 by BigGray
1)That is what the original controller(dead) did.
The original controller re-homed automatically and reset the machine coords to zero the before cutting then started cutting, because the spool is like a spring if you disable servos it can lose wind itself back a bit. If linuxcnc goes to sleep it auto disables drives.
Btw it also computed the Z and A positions from X&Y.
It re-homed after every time it cut the spool completely.
The original controller just took some nice X Y values without offsets.


2) Avoid writing Gcode like G54 G1 X100 .000 Y100.000 Z45.000 A154366.000
I will have to do this even when using offsets or I would have to call G10 L20 P1 A0 after every line which is kind of crazy as there can be thousands of calls in just one sheet.

Using relative coords is not an option if i cannot do that only for the A axis.


3) I was hoping to avoid dealing with offsets as they make debugging harder.
The g code generator needs to be solid else it will crash the machine.


4)using offsets when loading a new job after the first axis still shows the first job so it goes off-screen which is not handy as a job can be 100000.0000 mm long
The preview is needed to avoid confusion.


I can see how this looks like no issue for someone using a mill.
Maybe this looks trivial but on fast machines that rehoming of X happens several times a minute so it was automated.

Currently I set it up using offsets and large numbers for A in Gcode.
Everything works except it just is not elegant.

If only "encoder.N.reset bit" didn't cause a following error.
Last edit: 4 years 3 months ago by BigGray.

Please Log in or Create an account to join the conversation.

More
4 years 3 months ago #247697 by andypugh

4)using offsets when loading a new job after the first axis still shows the first job so it goes off-screen which is not handy as a job can be 100000.0000 mm long
The preview is needed to avoid confusion.
 
G10 will move the tool point to the origin on the preview. 
The only time that the big numbers would be visible would be if you chose to display absolute machine coordinates rather than relative working coordinates. 

If you use G10 and display working coordinates then I think that the machine will appear much the same as with the old controller. 
 

Please Log in or Create an account to join the conversation.

More
4 years 3 months ago #247708 by BigGray
Can't try it now.

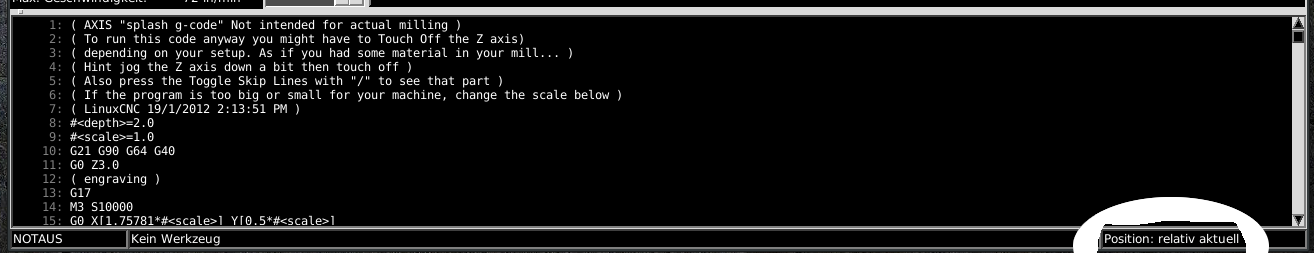
G10 L20 P1 X0 does not set the g54 datum to the origin on the preview.
Or you mean just G10 ?
Please Log in or Create an account to join the conversation.

More
4 years 3 months ago #247709 by tommylight

If linuxcnc goes to sleep it auto disables drives.
LinuxCNC does not go to sleep.
If the PC enters the sleep mode, waking it up will most probably loose control to LinuxCNC.
You can setup LinuxCNC to disable the drives only when E-stop is pressed, the usual way is to disable on any error so machine-is-on or machine-enable are used.
Or you can set it to not disable at all.
If it is a stepper system, leaving it on all the time is OK.

Please Log in or Create an account to join the conversation.

More
4 years 3 months ago - 4 years 3 months ago #247751 by chris@cnc

Can't try it now.

G10 L20 P1 X0 does not set the g54 datum to the origin on the preview.
Or you mean just G10 ?  
 
You can toggle machine coordinate and relative coordinate with the # button  


Idea to the following error... Very rough, but you could try to set the "FERROR" in *.ini file to high number like 9999999. The error control is now off, but i think in your case it's okay. If something wrong we make baguette or calzone instead of pizza. The risk of machine crash is not high. I have no machine to test this at the moment. 
Last edit: 4 years 3 months ago by chris@cnc.

Please Log in or Create an account to join the conversation.

More
4 years 3 months ago #247785 by BigGray
Thanks a lot guys, I knew there would be no easy solution.

@Chris
Lol, well the pizza was just an example, i really do need ferror to be withinn 0.5 mm.
But thinking of it I could maybe temporary set the FERROR High reset the axis and then Set the FERROR again with something like Andy did.


Currently this solution is acceptable.

If/When I have some time I'll have a good look at the code of linuxcnc and perhaps rewrite it to suit my needs, If I get to it I'll update this post.

Please Log in or Create an account to join the conversation.

Time to create page: 0.134 seconds
Powered by Kunena Forum
