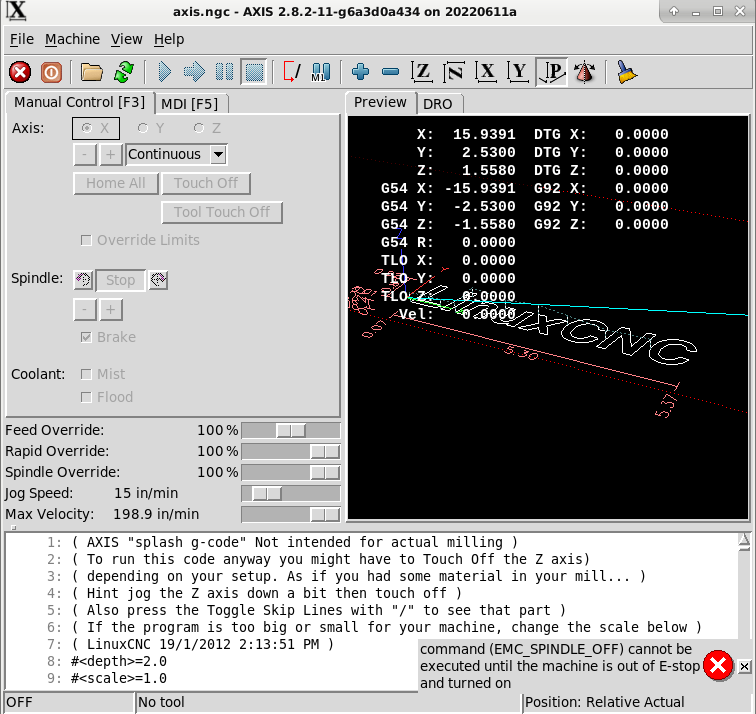
command (EMC_SPINDLE_OFF) cannot be executed until the machine is out of E-Stop

More
4 years 2 months ago #249373 by shanham67
My configuration is the 'unmolested' output of pncconf.  Can anyone point me to the cause of the error message shown in the bottom right of the attachment?  My mill is functional so the error message is just an annoyance. 


thanks

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago - 4 years 2 months ago #249397 by Todd Zuercher
Not sure, need more information.

What do your configuration files look like?

When exactly does the message pop up?

What causes it to pop up is that the input to command the spindle changed state while the machine was in E-stop.
Last edit: 4 years 2 months ago by Todd Zuercher.

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249400 by shanham67
It pops up when Axis is started. I have been ignoring all the while I have been setting up this machine.

Even with the error I am able to start the spindle in both directions and control the speed through the GUI.

BUT...

We just realized that the M3 command doesn't work until we toggle the EStop off and back on then click the RESET button to turn the machine on.

estop-ext is connected to 7i76e input 0 (net estop-ext <= hm2_7i76e.0.7i76.0.0.input-00). .hal file attached.


File Attachment:

File Name: 20220611a_...8-09.hal
File Size:11.39 KB

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249403 by Todd Zuercher
So are you saying that you can turn on your spindle without taking the machine out of e-stop and turning on the machine? Or just that you can start it with the warning message showing? At this point I'm not sure why the message would be popping up at startup. But I am not using 2.8 on any machines either (I havn't updated beyond 2.7 yet.)

My best guess is that it might something to do with your lines relating to:
Code:
net spindle-manual-stop <= hm2_7i76e.0.7i76.0.0.input-07
and
Code:
net spindle-manual-cw halui.spindle.0.forward net spindle-manual-ccw halui.spindle.0.reverse net spindle-manual-stop halui.spindle.0.stop

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249407 by shanham67
Thanks!

I took out the spindle-manual-stop assignment and the warning is gone.

Axis doesn't come up 'in' e-stop (unless a physical e-stop button is pressed). Immediately after starting Axis, I am able to start the spindle by:
1. turning on the machine
2. clicking either the spindle cw or ccw gui buttons.

Can you tell me how to make Axis start with the gui e-stop button pressed?

Please Log in or Create an account to join the conversation.

More
4 years 2 months ago #249411 by Todd Zuercher
The signal out from Linuxcnc's gui estop is this.
"net estop-out <= iocontrol.0.user-enable-out"

You simply need to include it into your external e-stop loop. I usually do this by connecting the above hal signal to an ouput pin. Then using that as the signal source for the e-stop loop run a wire from that output pin to the e-stop switches then back to the input pin connected to "net estop-ext => iocontrol.0.emc-enable-in" and trigger any relays needed for the e-stop.

Please Log in or Create an account to join the conversation.

Time to create page: 0.202 seconds
Powered by Kunena Forum