
- Posts: 170
- Thank you received: 13
Simple G7x Profile editor for Linuxcnc/Axis
- papagno-source
- Offline
- Elite Member
-

Less
More
6 months 1 week ago #345869
by papagno-source
Replied by papagno-source on topic Simple G7x Profile editor for Linuxcnc/Axis
HI good mornig at all.
The GUI, can running on Debian 10 ?
Thanks
The GUI, can running on Debian 10 ?
Thanks
Please Log in or Create an account to join the conversation.
- opw
- Offline
- New Member
-

Less
More
- Posts: 18
- Thank you received: 11
6 months 3 days ago #346010
by opw
Replied by opw on topic Simple G7x Profile editor for Linuxcnc/Axis
It should, just try it, it is a small download and easy to try
Please Log in or Create an account to join the conversation.
- opw
- Offline
- New Member
-
Less
More
- Posts: 18
- Thank you received: 11
4 months 2 weeks ago - 4 months 2 weeks ago #347081
by opw
Replied by opw on topic Simple G7x Profile editor for Linuxcnc/Axis
Sorry it took such a long time. I have updated the code with your suggestions, pushed it to github, but have not gotten around to testing it yet on my own lathe as workshop time is scarce at the moment.
Let me know if you still encounter any issues.
Let me know if you still encounter any issues.
Last edit: 4 months 2 weeks ago by opw.
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- dredivan
- Offline
- New Member
-
Less
More
- Posts: 16
- Thank you received: 3
4 months 2 weeks ago - 4 months 2 weeks ago #347091
by dredivan
Replied by dredivan on topic Simple G7x Profile editor for Linuxcnc/Axis
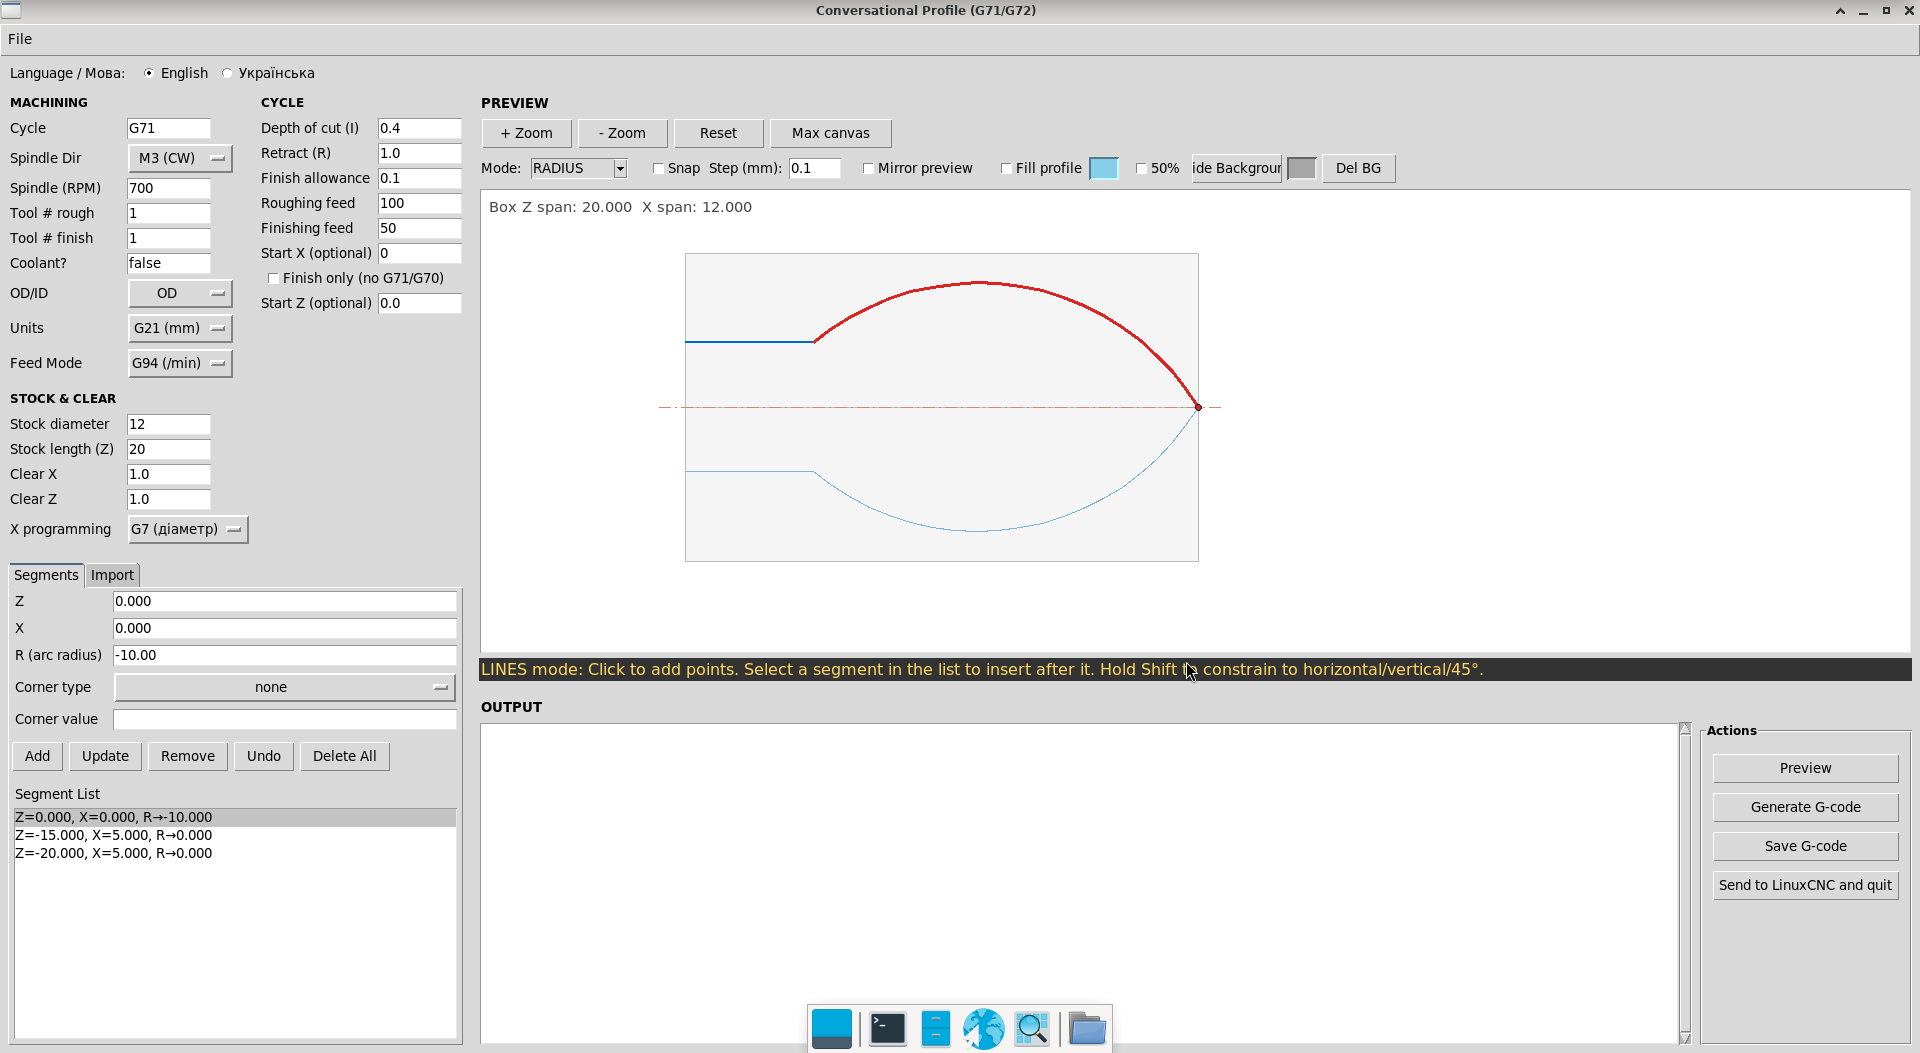
Hi everyone! I'm not a programmer, I have a small lathe (LinuxCNC 2.9.8, Mesa 7I96S), and I'm slowly learning. I found a few real issues in the profiler — some of them can actually cause the tool to crash into the workpiece. All fixes were made together with Claude (AI), and tested on real hardware.What was fixed:
- English/Ukrainian language switcher at the very top of the window (English by default)
- D and I were swapped in G71/G72, plus incorrect scaling for G7 (diameter mode) — the actual depth of cut was twice the value entered
- unsafe G71→G70 transition — for certain Start X values the tool wouldn't retract and crashed into the part
- Start X / retract didn't account for arcs (G2/G3) "bulging" beyond their endpoints
- added a "Finish only" mode — re-run just the last pass without G71/G70
- added a safe approach move at program start, from any starting position
- improved preview (symmetric, centerline at X=0) and DXF import
File and detailed changelog (CHANGES.txt) attached. If it's useful to anyone, feel free to grab it.
Last edit: 4 months 2 weeks ago by dredivan.
The following user(s) said Thank You: tommylight
Please Log in or Create an account to join the conversation.
- dredivan
- Offline
- New Member
-
Less
More
- Posts: 16
- Thank you received: 3
2 months 2 weeks ago #348663
by dredivan
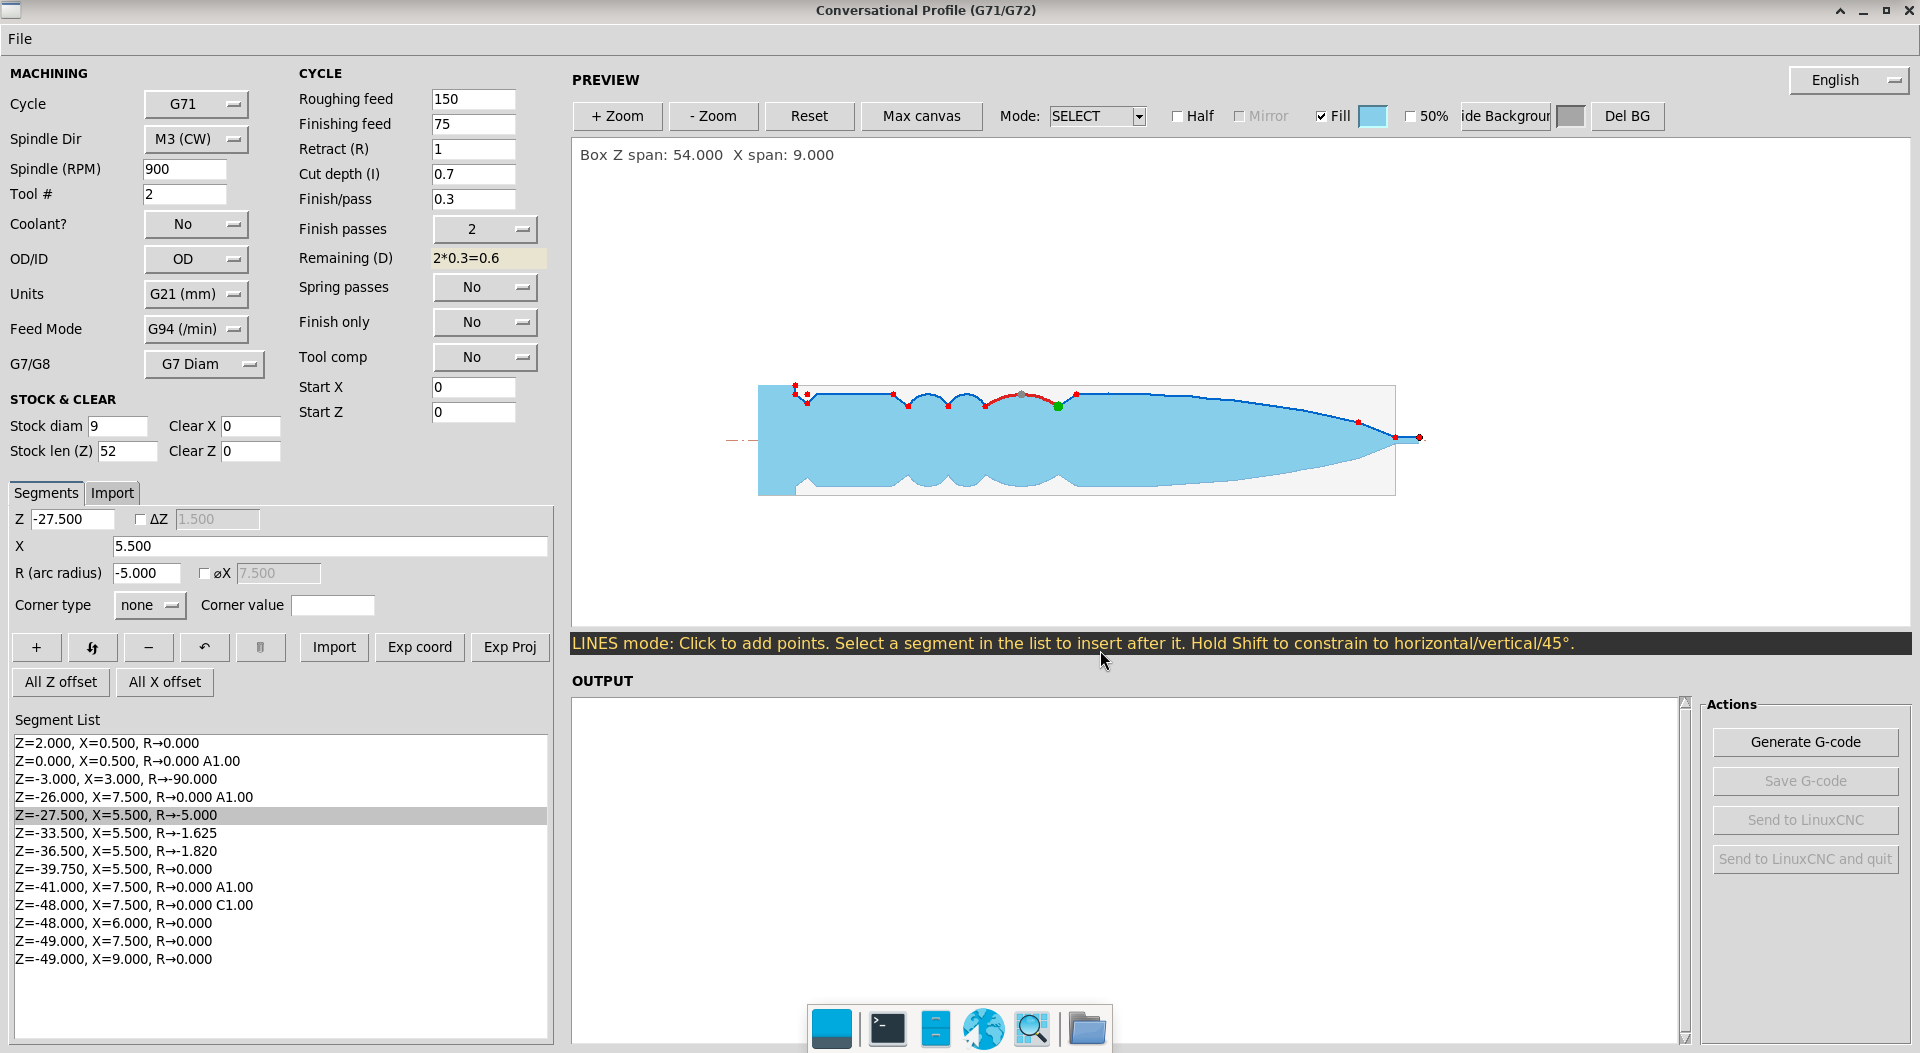 Hi everyone! Follow-up to my earlier post — kept working on the profiler with Claude (AI) and testing on my real lathe (LinuxCNC 2.9.8, Mesa 7I96S). Found more real issues since last time, including a couple more crash risks, plus added several new features.What was fixed:
Replied by dredivan on topic Simple G7x Profile editor for Linuxcnc/Axis
- G72's D/I/R were also wrongly scaled for G7 — same class of bug as the D/I swap from before, but G72 works along Z, where no diameter/radius conversion should apply at all
- Retract (R) in G71 was missing the same G7 scaling fix that D/I already got
- diagonal rapid moves could happen between multiple finishing/spring passes — now explicit, safe L-shaped repositioning between every G70 call
- a profile point sitting exactly on the centerline (X=0) could hang LinuxCNC before any motion even starts — now caught with a clear error instead
- tool nose radius compensation (G41/G42) support, including multiple finishing passes under compensation
- separate "spring passes" (repeat the final cut N times with no material removal) as its own stage
- finish allowance entered per pass (e.g. 0.25mm × 2 passes), with the total shown live
- ΔZ (enter coordinates relative to the previous point) and ⌀X (enter the desired diameter at an arc's peak instead of the radius)
- Half/Mirror preview mode
- full project import/export (.txt with all machine parameters, not just coordinates), with auto-detection on import
- Coolant/Tool comp/Cycle as dropdowns instead of text/checkboxes
- generate-then-save workflow (Save/Send stay disabled until you click Generate)
- better fill rendering in preview (incl. ID bores, and stock length the profile doesn't reach)
The following user(s) said Thank You: tommylight, besriworld
Please Log in or Create an account to join the conversation.
- opw
- Offline
- New Member
-
Less
More
- Posts: 18
- Thank you received: 11
2 months 22 hours ago - 2 months 22 hours ago #349162
by opw
Replied by opw on topic Simple G7x Profile editor for Linuxcnc/Axis
Thanks for the write-up and the machine tests. I am not a G71 expert either, so take this as “what I changed”, not gospel.
I am targeting native LinuxCNC 2.9** only (`G71 Q… D… I… R…`). In those docs, D is remaining distance to the profile (finish stock) and I is the cutting increment** (DOC). PathPilot uses a different letter set, so the two will not match; this tool follows the 2.9 page, not PathPilot.
On G7: I do not think diameter mode should halve D/I/R. In my view DOC is still DOC in G7 or G8 — the rest is just a display issue. Logical in my view is that depth of cut reduces diameter by DOC*2. G71’s increment is radius-based as well. Treating G7 as “divide the cycle words by two” also dragged in a lot of other mistakes (G72, retract, mixed scaling). I am not taking that path unless someone can convince me this is the way to go.
v1.1.0 is out with:
- G71/G72 letters swapped to that 2.9 meaning (UI labels too: DOC is I, stock left is D).
- L-shaped rapids instead of a diagonal `G0 X… Z…`.
- An explicit retract between G71/G72 and G70, so finish should not cut a corner through stock.
- Start/retract X now includes G2/G3 bulge past the endpoints, not just min/max of the points.
- Retract X is separate from a user Start X (so a bore start is not used as the pull-out).
I did not adopt G7 `/2` on D/I/R, cutter comp, or “finish only, skip G71”.
I have not had time to run this on a real machine yet, so treat it as untested on iron. Dry-run / sim first. If someone who lives on native 2.9 `G71 Q` can sanity-check the D/I mapping, that would be very welcome.
Profiler 1.1 is here
Last edit: 2 months 22 hours ago by opw.
The following user(s) said Thank You: besriworld
Please Log in or Create an account to join the conversation.
Time to create page: 0.267 seconds