7i76e SPINDLE OUT voltage is slightly low

More
5 years 10 months ago #193393 by jpvonoy
My CNC router spindle speed is about 3-4% low versus what I am commanding.

I am controlling a 2.2 kW Huanyang VFD and spindle via the 7i76e TB4 Spindle Outputs, 0-10vdc.

I used a laser tachometer to check actual spindle speeds vs commanded speeds and found the actual speeds were low by about 3-4%.

I measured the voltage between TB4 pins 1, 2, and 3. Pin 3 is 10.05 volts, but the "wiper" voltage on pin 2 is slightly low for any given commanded RPM. For example, at the maximum scale of 24000, the voltage is 9.71 vdc, the same percentage error as the RPM.

Any ideas why that voltage would be low? Should the SPINDLE OUT be able to reach a full 10.05 vdc at max scale?

Attaching my ini and hal files since they are commonly requested. You may notice I added a lincurve, which does fix the error across most of the range, but I haven't been able to get it to increase the speed right at 24000. So, rather than patch over the problem I'd like to find the source of the error.

Please Log in or Create an account to join the conversation.
More
5 years 10 months ago #193396 by PCW
You might check that the 10V supply does not droop at full scale

(The 7I76E potentiometer replacement circuit draws higher current
at full scale)

The 7I76E SPIN-OUT pin can never quite reach the SPIN+ voltage
but it normally gets to 50 or so mV of SPIN+ at full scale.

An external 12V supply is one possible fix , as it changing the VFD scaling

Please Log in or Create an account to join the conversation.

More
5 years 10 months ago #193445 by jpvonoy
Thanks PCW. I checked SPIN+ at full scale. It droops to 9.99 vdc from 10.05. This is not enough to account for the error I'm seeing.

The SPIN-OUT at full scale is reading 9.72 vdc, but I noticed that I can hear a drop in spindle RPM as I touch the meter lead to pin 2. It drops by about 200 RPM.

200 RPM corresponds to 0.08 v, so that means I have 9.8 vdc on SPIN-OUT at full scale.

This is an error of 9.99 - 9.8 = 0.19 v, or 1.9%

Accounting for the max SPIN-OUT being 50 mV less than pin 3 (9.99v), I have an error of 9.94 - 9.8 = 0.14 v, or 1.4%.

Does this sound like the best I can expect to get from the 7I76E? Is there a way to adjust this in the firmware?

I'll have to do some experimenting to figure out how I would scale it with the VFD. I don't think I can increase the max frequency above 400Hz. Maybe changing the parameter for RPM at 50 Hz (currently set to 3000)?

Please Log in or Create an account to join the conversation.

More
5 years 10 months ago - 5 years 10 months ago #193446 by PCW
Its probably a combination of the load and possible some HF noise

(the change in motor speed when you touch the meter lead to the output
suggests a noise issue since the meter does not present enough
DC load to change the reading)

By scaling I mean the analog input scaling (some drives for example have both 10 and 5V full scale input selections)

Or like I said, use a external 12V supply
Last edit: 5 years 10 months ago by PCW.
The following user(s) said Thank You: jpvonoy

Please Log in or Create an account to join the conversation.

More
5 years 10 months ago #193459 by chris@cnc
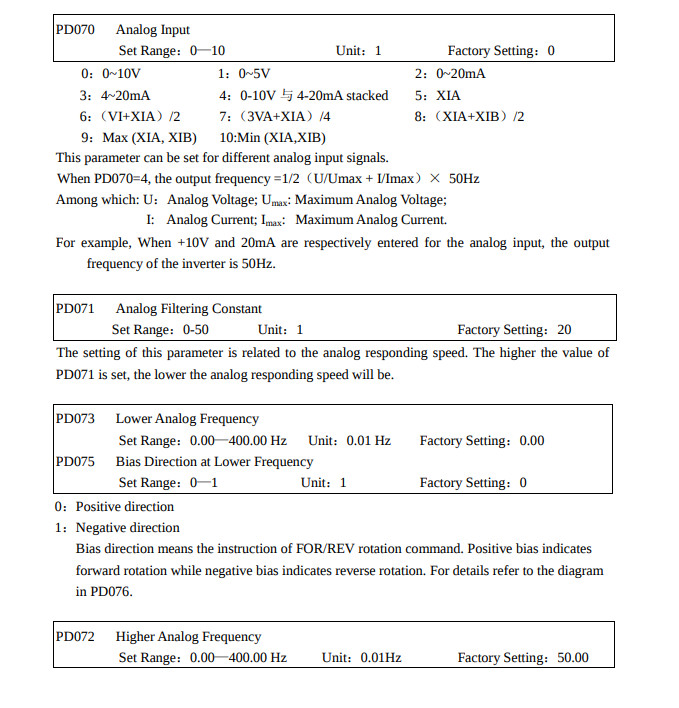
Try Parameter PD71 or PD159 to adjust target speed. Any VDF should compensate this kind of Problem only Parameter are Different. Or increase P of your VFD. Something must be happened.

Please Log in or Create an account to join the conversation.

More
5 years 10 months ago #193505 by Mike_Eitel
What kind of motor do you use?
Are you aware of motor slip.
The frequency of vfd is equal to physical only when it's a synchron motor.
Mike

Please Log in or Create an account to join the conversation.

Moderators: PCW, jmelson
Time to create page: 0.316 seconds
Powered by Kunena Forum
