
- Posts: 77
- Thank you received: 10

Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.

Please Log in or Create an account to join the conversation.
CrashCNC wrote: I'm not having success integrating this code with probe screen as suggested.
I believe the probe screen python code is using linuxcnc call stat.probe_position() to identify where the probe was triggered after each move.
Since the code supplied pulls variables #621-#628 (offsets) through a Gcode subroutine and adjusts the measured probe value within the subroutine into variable 5001 and 5002 probe screen is missing the offset.
Anyone else have this issue? Are variables 5001 and 5002 special? Maybe i'm missing something.
**EDIT - I think i understand . This code is attempting to change the absolute position on the mill before probe screen has a chance to read it. Isn't that dangerous? Would it not throw off the homed location? Probe screen still would never get the result because it is determining the probe trip point from the previous G38.2 calls which do not include the offset table variables.
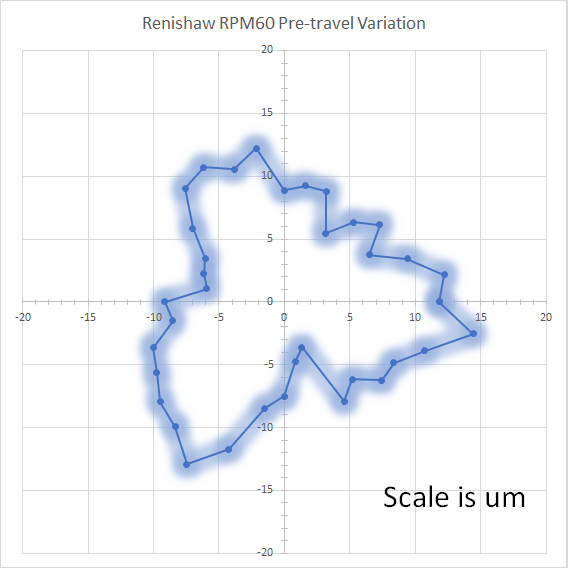
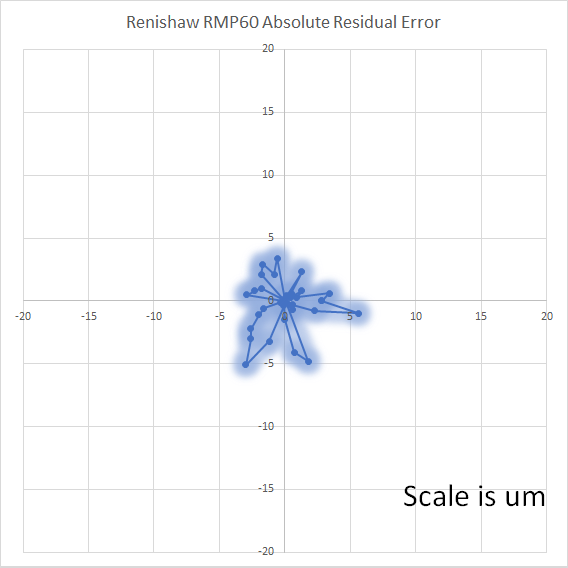
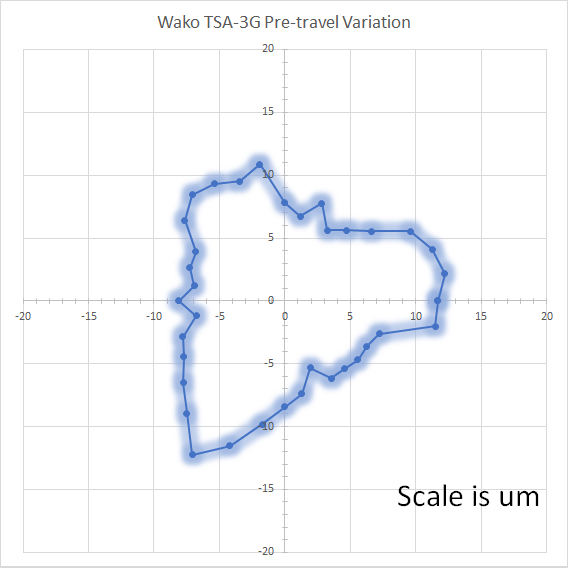
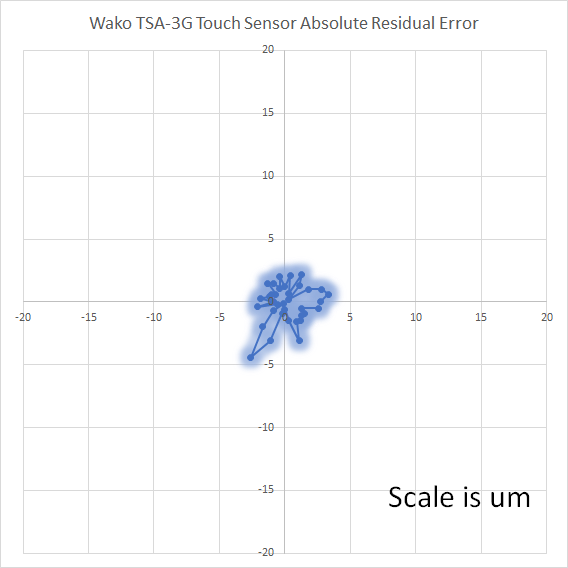
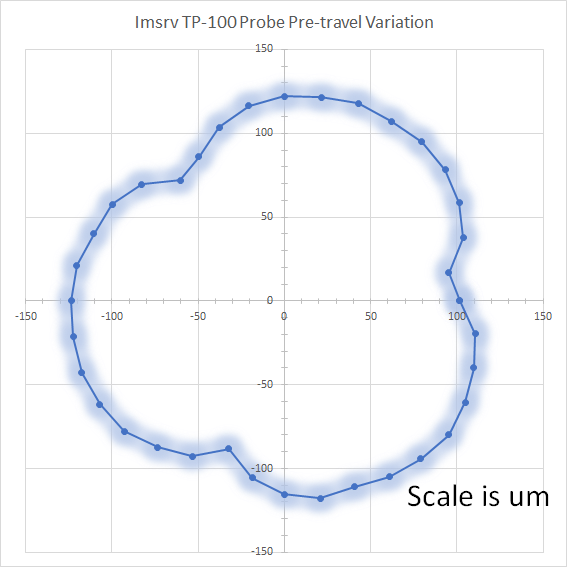
The probing calibration routine worked great. I agree with what was calculated. Thank you plopes9000 for your efforts!
Please Log in or Create an account to join the conversation.


Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
