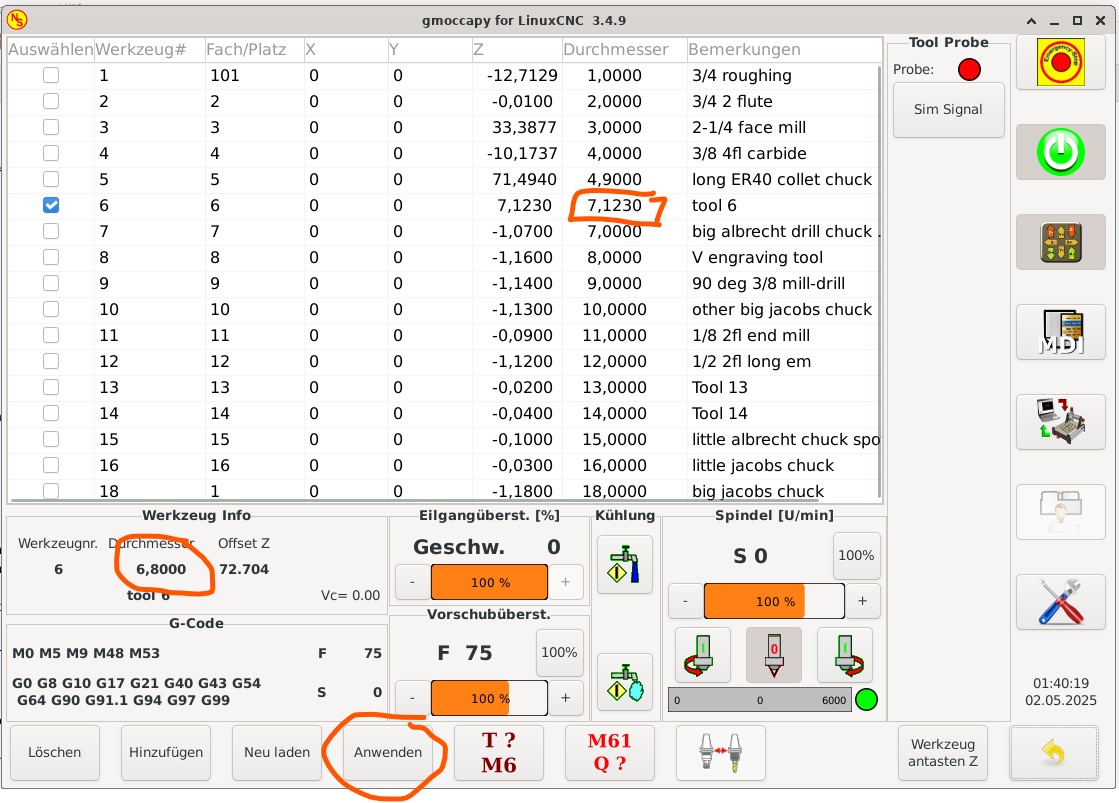
Basically, I agree with you. Specifying some basic settings at the start of the program makes sense and is done that way. However, it's confusing when the machine is always in different states during different phases, such as after the control system starts, during program execution, after a program abort, after a tool change, and so on. For me it's not clear why the tool length should disappear when a program is aborted? I can't see the reason or the rationale for this.
But I have a solution for this.
However, we're getting away from the actual question:
How can I ensure that the radius is updated in the tool info window when applying the tool table after editing? Are incorrect half pins connected here, or where are the functions triggered by the "Apply" button controlled? When milling with radius compensation, the value from the info field is used. G41/42 accesses this value.
When programming, I use radius compensation (finishing, fits, etc.) whenever possible and sensible. This allows for easy adjustment of the dimensions without having to change with the CAD program.