Open Source Controller with internal THC

More
7 years 11 months ago #120237 by cmorley

islander261 wrote: CommandCNC is a Gscreen LinuxCNC application. It is wrapped in a proprietary launcher/configuration program so if you just get the GPL source you will need roll your own .ini and .hal files (not hard following the Gscreen examples). I have hacked it to run on my hardware (7i76e and THCad) with my internal THC.

John


I know it's not what you guys are talking about - but I'm pleased someone found Gscreen was useful and worked out how to make a custom screen. This was exactly what it was for yaay - ok back to your thread.... :)

Chris M
The following user(s) said Thank You: tommylight, Grotius, dvn4life1972

Please Log in or Create an account to join the conversation.

More
7 years 11 months ago #120274 by islander261
I think the biggest problem most DIY machine builders have with THC is that we are trying doing it on wimpy poorly aligned machines and cut thinner material that is subject heat distortion and warpage using cheap imported HF start power supplies and torches. According to one Guru on this subject you need to hold the torch height within +/-.005" of the ideal cut height for best results. This is pretty easy for a stiff high powered industrial CNC machine. Actually many large industrial machines that are used to cut thicker plate don't even use active THC, they just use initial height sensing and the table mapping to adjust during the cut.

Most of the major manufactures actually use an external THC that is tightly coupled to a general purpose CNC controller so both parts know what is happening. I know that Hypertherm has all of their documentation available on their web site if you want to do a little reading.

There is a lot of good information about air plasma THC available. Look on both Plasmaspider.com and cnczone.com for posts by Jim Colt from Hypertherm, he has posted performance requirements several times at least on both sites. Mr. Caudle from CandCNC is also a frequent poster on both sites and works hard to sell his THC equipment.

LinuxCNC allows the creation of custom functions by the user. This feature has been used by many for plasma torch THC. Some have used an external controller, Proma, CandCNC, Neuron and countless Chinese knock offs. Some have used internal LinuxCNC functions as J.T., Rod W., others and I have. My system presently runs pretty well in almost daily use, I can hold +/- .0025" torch height from ideal when doing 18" test cuts on material that does heat warp during the cut. The biggest stumbling block for most DIY builders is getting the electrical engineering correct for measuring a noisy high voltage signal in real time, this actually isn't too hard now with the off the shelf hardware that is available to work with LinuxCNC. I am using a Mesa 7I76e with a THCad board and am very happy with the performance of both.

John

Please Log in or Create an account to join the conversation.

More
7 years 11 months ago #120286 by rodw

islander261 wrote: LinuxCNC allows the creation of custom functions by the user. This feature has been used by many for plasma torch THC.


John touches on the most powerful feature of Linuxcnc. The ability to write your own custom software component and embed it in the system exactly as if it was one of the standard components. Components are the building blocks of LinuxCNC's HAL, the Hardware Abstraction Layer. Components are written in C and compiled and installed by a supplied script using one command from the terminal window.

Whilst it is possible to write one single THC component as PhillC is working on, perhaps a better approach more in keeping with LinuxCNC's design philosophy is to build small discrete components for each individual function. Eg, Velocity anti dive (corner lock), Torch voltage sampling, testing to see if probing is required based on distance from the last pierce, and even triggering air solenoids for downdraft table zoning can all be written in small modules which makes it easy to maintain and debug your system. This feature makes Linuxcnc a good platform for plasma and it is rapidly maturing in this area.

Please Log in or Create an account to join the conversation.

More
7 years 11 months ago - 7 years 11 months ago #120295 by Grotius
Just for info what linux is capable to, thanks to Mr. Chris Morley, for making his user interface python code.
Without his magic, it would be problably not easy to go with linuxcnc on this level.

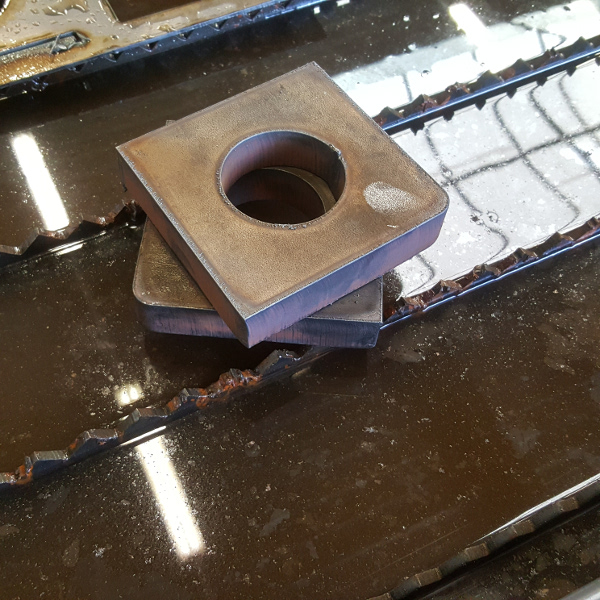
20mm steel test cut during linuxcnc training course today.
Cutted at 105 amp, with powermax 105. First cut without improvement's.


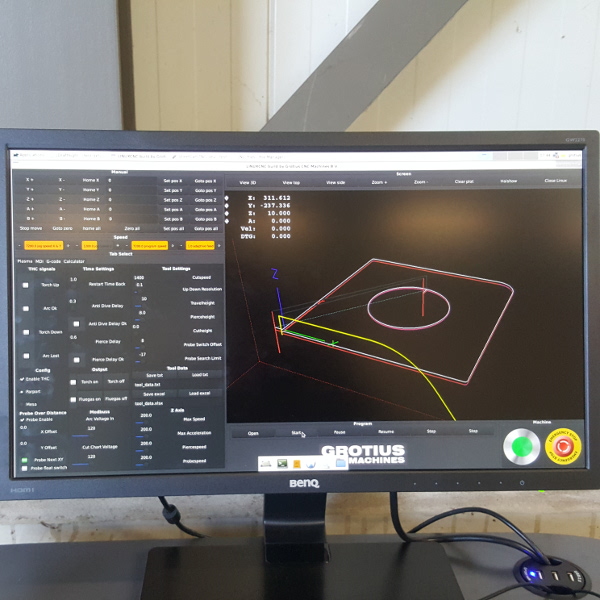
Linuxcnc plasma software application with universal thc component.


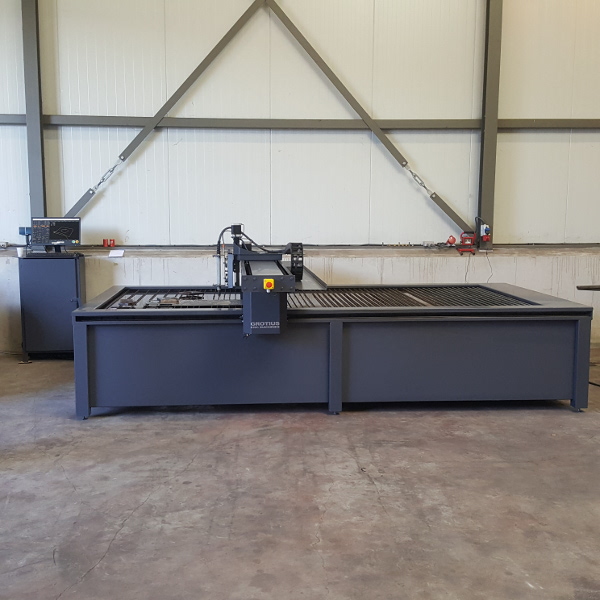
A machine that cut's, my last machine of model 2018, up next is new model 2019.
Last edit: 7 years 11 months ago by Grotius.
The following user(s) said Thank You: rodw, thefabricator03, dvn4life1972

Please Log in or Create an account to join the conversation.

  • thefabricator03
  • Topic Author
  • New Member
  • New Member
More
7 years 11 months ago #120310 by thefabricator03
Replied by thefabricator03 on topic Open Source Controller with internal THC
Your machine looks very well built, Did you build it yourself?

With my machine using a Powermax 125 I have been able to cut 25mm plate with the same quality,

Attachment not found


Attachment not found


What program did you used to generate the G-code? Sheetcam?

Please Log in or Create an account to join the conversation.

More
7 years 11 months ago - 7 years 11 months ago #120361 by Grotius
Hi Stefan,

Thanks. Yes me is the builder.
Nice too see your picture's. Very nice output.
It's generated with sheetcam. I did some test in the past with dxf2gcode to load a dxf straight into linuxcnc without seeing the program dxf2gcode opening actually.

Tonight i did some more test's. I coupled the tool.tbl tool file within the grotius gui python code.
Code:
self.widgets.tooledit1.set_filename("tool.tbl") self.widgets.tooledit1.set_visible("pabcxyzuvwijq", False) #here i say, dont show too much stuff i don't use
So when we are going to use dynamic tool libraries for plasma in the future, the plasma kerf widht (tooldiameter) is actually working nice with (G40/G41/G42) to my surprise. It's has the reloading possibility without restarting Linuxcnc. Just what we need.
In other word's, we can soon do a simple way of cam processing also in linuxcnc for plasma.

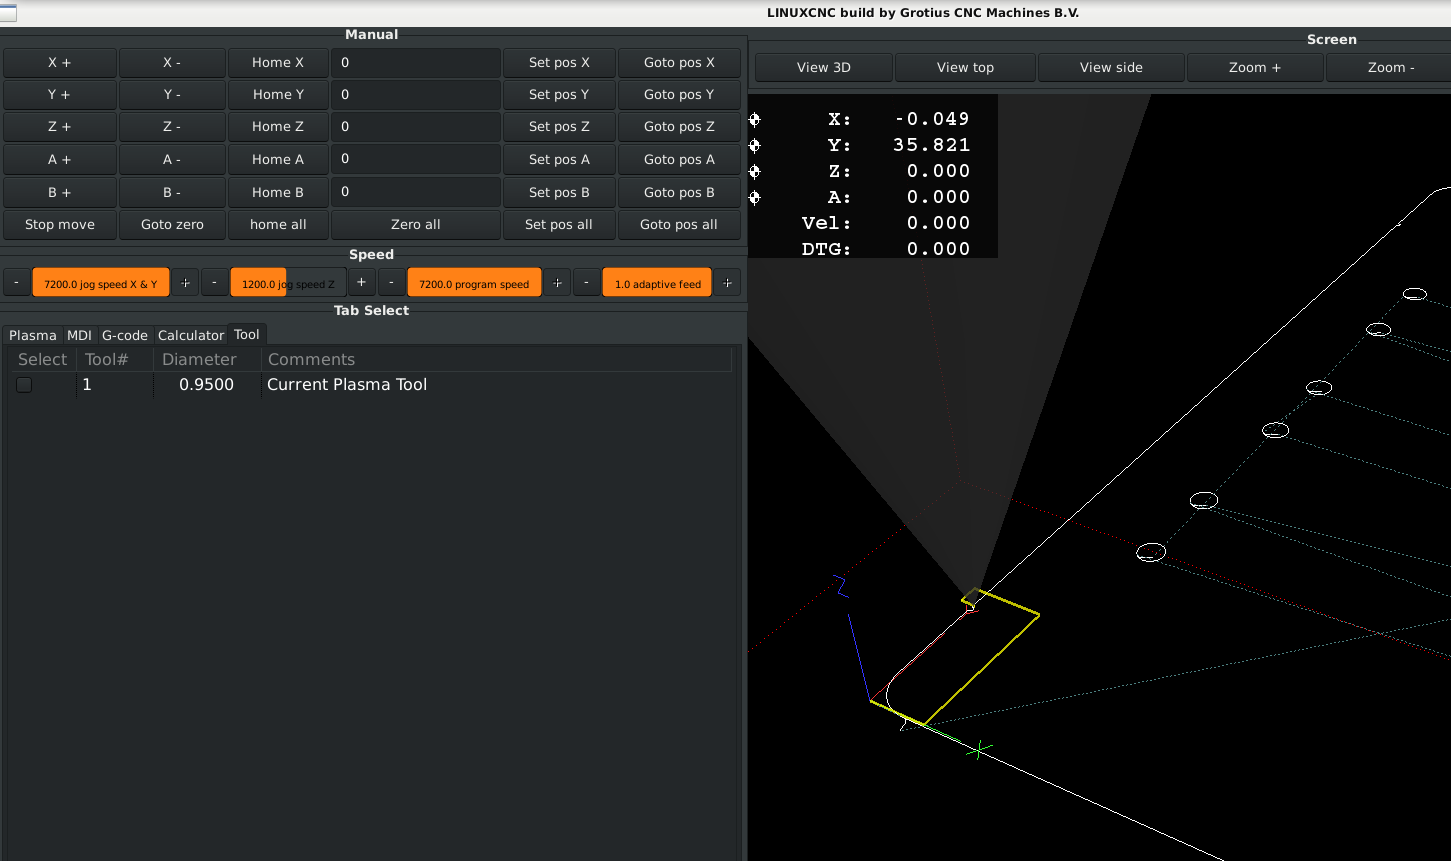
What i noticed about the startpoint is, sheetcam wil allway's start at the cone point on the picture, standard. At that point there is a little press brake mark with radius 2mm. But i don't want to start at that point so i have to modify start point's each time with sheetcam. Okey dxf2gcode is starting at outside contour at a better point, without modifiying start point's. So that is nice.

Generated with dxf2gode :


I think goal of many users is open linuxcnc :

1. click button "tool library" or a button name you want to have on your screen.
2. click your way to the database (.odb file) pop up screen's, select dynamic input fields one by one, everything about the tool is set.
-- cutting chart's in odb format. ( python pluging code for acces databases, full plasma tool databases, also editable off-line )
-- the rs485 (modbus connection) to plasma inverter is set this way. ( also for standard modbus i/o module, standard plasma inverter conversion with modbuss connection. )
-- The kerf width is set this way.
-- The real time plasma THC component is set this way.
-- The G1 speed is set this way. (trick is to use this in the python code for reloading parameters of speed :
self.c.mode(self.cnc.MODE_MANUAL)
self.c.wait_complete()
self.widgets.gremlin.reloadfile(None)
The G0 speed is available in user gui. Master speed is adaptive feed -1 to 1. Feed override is set to max tuning parameters.
3. select dxf file you want to cut. (behind this, the dxf2gcode is autogenerated and loaded into linuxcnc)
4. start your machine.
Last edit: 7 years 11 months ago by Grotius.

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.082 seconds
Powered by Kunena Forum