Is this a bug?
- jazzkramer
- Offline
- Junior Member
-

Less
More
- Posts: 38
- Thank you received: 3
07 Oct 2026 22:53 #350161
by jazzkramer
Is this a bug? was created by jazzkramer
Hi guys,
I'm using QTPlasma 2.9-237.307 Powerd by QtVCP
since a long time, maybe now, it will became a job... (Let's see)
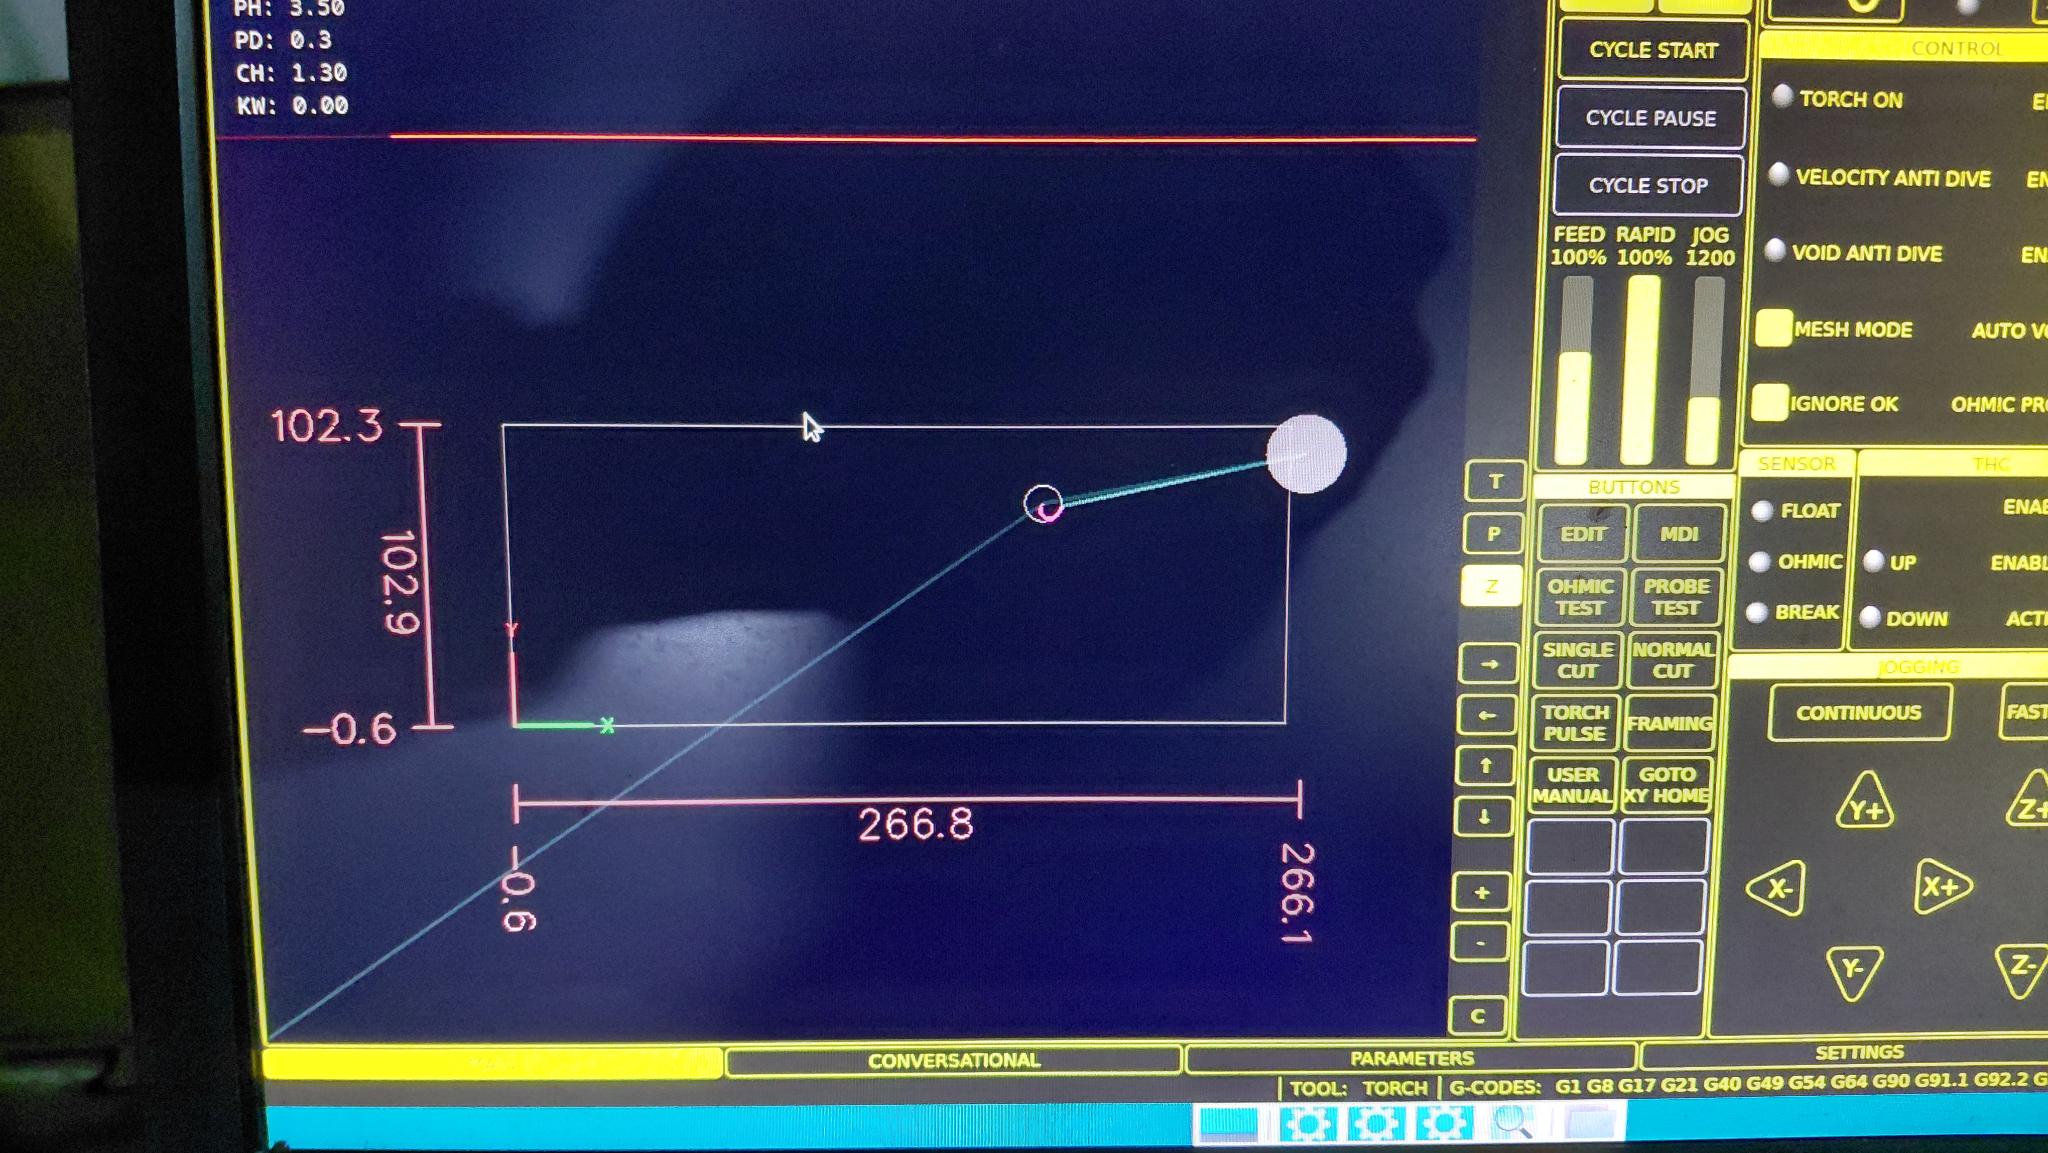
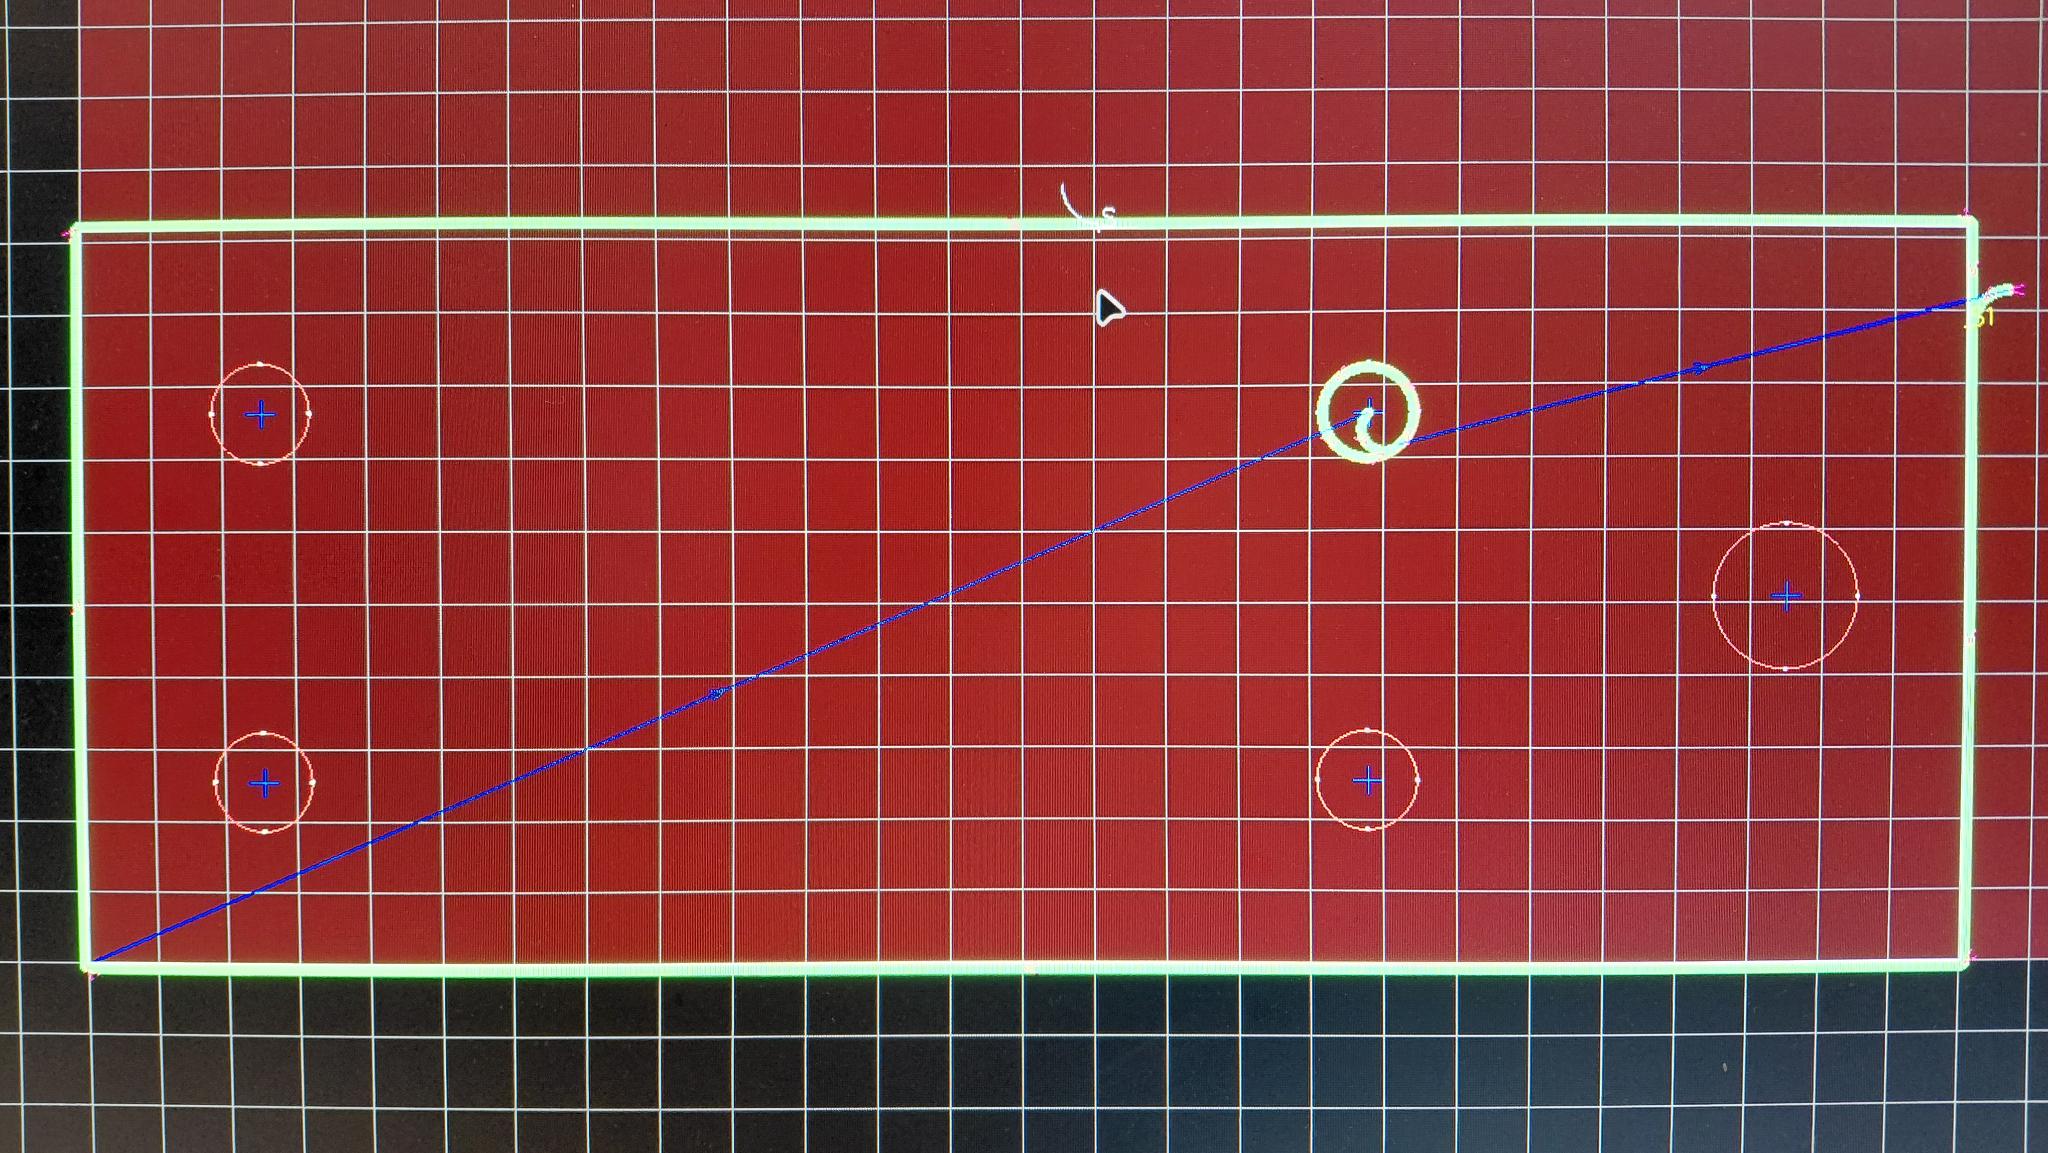
I'm doing some parts to fix the roof of "my shop", a plate with some holes, and PlasmaC does not want to make one hole... It just start the arc inside the hole and when it touch the real circumference it stops and it jumps to the next shape of the plate... others holes are ok.
Is my code good? It was generated by SheetCam-TNG. I tried to recur (ignore arcok.. mesh.. always the same wrong path)
Any ideas? Thanks!
In the photo you see one hole only, just to test I modified the file, but it shows the same mistaken path as the complete code here:
; file name: Piastra piegata per soffitto.ngc
; date and time: Wed Oct 07 2026 11:26:34 AM
; postprocessor: LinuxCNC PlasmaC.scpost rev: 0.5
;
;begin pre-amble
G21 (units: metric)
G40 (cutter compensation: off)
G90 (distance mode: absolute)
M52 P1 (adaptive feed: on)
M65 P2 (enable THC)
M65 P3 (enable torch)
M68 E3 Q0 (velocity 100%)
G64 P0.254 Q0.025 (tracking tolerances: 0.254mm)
#<holes> = 2
#<h_velocity> = 60
#<h_diameter> = 32
#<oclength> = 4
;end pre-amble
;
;begin material setup
T0 M6 (select plasma tool)
G43 H0 (apply tool offsets)
M190 P20 (plasma, mield steel 1/4" material)
M66 P3 L3 Q2 (wait for valid change)
F#<_hal[plasmac.cut-feed-rate]>
;end material setup
G0 X177.8 Y76.2
M3 $0 S1 (plasma start) ****THIS FIRST HOLE IS NOT WORKING
M67 E3 Q100
G3 X182.184 Y71.816 I2.192 J-2.192
G3 X182.184 Y71.816 I-4.384 J4.384
M5 $0 (plasma end)
G0 X177.8 Y25.4
M3 $0 S1 (plasma start)
G3 X182.184 Y21.016 I2.192 J-2.192
G3 X182.184 Y21.016 I-4.384 J4.384
M5 $0 (plasma end)
G0 X234.338 Y44.171
M3 $0 S1 (plasma start)
G3 X241.579 Y44.171 I3.62 J3.62
G3 X241.579 Y44.171 I-6.629 J6.629
M5 $0 (plasma end)
G0 X25.4 Y25.4
M3 $0 S1 (plasma start)
G3 X21.016 Y29.784 I-2.192 J2.192
G3 X21.016 Y29.784 I4.384 J-4.384
M5 $0 (plasma end)
G0 X25.4 Y76.2
M3 $0 S1 (plasma start)
G3 X21.016 Y80.584 I-2.192 J2.192
G3 X21.016 Y80.584 I4.384 J-4.384
M5 $0 (plasma end)
G0 X266.12 Y53.358
M3 $0 S1 (plasma start)
G3 X261 Y48.238 I0 J-5.12
G1 X261 Y0
G2 X260.35 Y-0.65 I-0.65 J0
G1 X0 Y-0.65
G2 X-0.65 Y0 I0 J0.65
G1 X-0.65 Y101.6
G2 X0 Y102.25 I0.65 J0
G1 X260.35 Y102.25
G2 X261 Y101.6 I0 J-0.65
G1 X261 Y48.238
M5 $0 (plasma end)
;
;begin post-amble
G40 (cutter compensation: off)
G90 (distance mode: absolute)
M65 P2 (enable THC)
M65 P3 (enable torch)
M68 E3 Q0 (velocity 100%)
M5 $-1 (backup stop)
;end post-amble
;
;begin statistics
;Pierces = 6
; Cuts = 6, Length = 997.75mm
;end statistics
;
M30 (end program)
Any ideas?
I'm using QTPlasma 2.9-237.307 Powerd by QtVCP
since a long time, maybe now, it will became a job...
(Let's see)I'm doing some parts to fix the roof of "my shop", a plate with some holes, and PlasmaC does not want to make one hole... It just start the arc inside the hole and when it touch the real circumference it stops and it jumps to the next shape of the plate... others holes are ok.
Is my code good? It was generated by SheetCam-TNG. I tried to recur (ignore arcok.. mesh.. always the same wrong path)
Any ideas? Thanks!
In the photo you see one hole only, just to test I modified the file, but it shows the same mistaken path as the complete code here:
; file name: Piastra piegata per soffitto.ngc
; date and time: Wed Oct 07 2026 11:26:34 AM
; postprocessor: LinuxCNC PlasmaC.scpost rev: 0.5
;
;begin pre-amble
G21 (units: metric)
G40 (cutter compensation: off)
G90 (distance mode: absolute)
M52 P1 (adaptive feed: on)
M65 P2 (enable THC)
M65 P3 (enable torch)
M68 E3 Q0 (velocity 100%)
G64 P0.254 Q0.025 (tracking tolerances: 0.254mm)
#<holes> = 2
#<h_velocity> = 60
#<h_diameter> = 32
#<oclength> = 4
;end pre-amble
;
;begin material setup
T0 M6 (select plasma tool)
G43 H0 (apply tool offsets)
M190 P20 (plasma, mield steel 1/4" material)
M66 P3 L3 Q2 (wait for valid change)
F#<_hal[plasmac.cut-feed-rate]>
;end material setup
G0 X177.8 Y76.2
M3 $0 S1 (plasma start) ****THIS FIRST HOLE IS NOT WORKING
M67 E3 Q100
G3 X182.184 Y71.816 I2.192 J-2.192
G3 X182.184 Y71.816 I-4.384 J4.384
M5 $0 (plasma end)
G0 X177.8 Y25.4
M3 $0 S1 (plasma start)
G3 X182.184 Y21.016 I2.192 J-2.192
G3 X182.184 Y21.016 I-4.384 J4.384
M5 $0 (plasma end)
G0 X234.338 Y44.171
M3 $0 S1 (plasma start)
G3 X241.579 Y44.171 I3.62 J3.62
G3 X241.579 Y44.171 I-6.629 J6.629
M5 $0 (plasma end)
G0 X25.4 Y25.4
M3 $0 S1 (plasma start)
G3 X21.016 Y29.784 I-2.192 J2.192
G3 X21.016 Y29.784 I4.384 J-4.384
M5 $0 (plasma end)
G0 X25.4 Y76.2
M3 $0 S1 (plasma start)
G3 X21.016 Y80.584 I-2.192 J2.192
G3 X21.016 Y80.584 I4.384 J-4.384
M5 $0 (plasma end)
G0 X266.12 Y53.358
M3 $0 S1 (plasma start)
G3 X261 Y48.238 I0 J-5.12
G1 X261 Y0
G2 X260.35 Y-0.65 I-0.65 J0
G1 X0 Y-0.65
G2 X-0.65 Y0 I0 J0.65
G1 X-0.65 Y101.6
G2 X0 Y102.25 I0.65 J0
G1 X260.35 Y102.25
G2 X261 Y101.6 I0 J-0.65
G1 X261 Y48.238
M5 $0 (plasma end)
;
;begin post-amble
G40 (cutter compensation: off)
G90 (distance mode: absolute)
M65 P2 (enable THC)
M65 P3 (enable torch)
M68 E3 Q0 (velocity 100%)
M5 $-1 (backup stop)
;end post-amble
;
;begin statistics
;Pierces = 6
; Cuts = 6, Length = 997.75mm
;end statistics
;
M30 (end program)
Any ideas?
Attachments:
Please Log in or Create an account to join the conversation.
- jazzkramer
- Offline
- Junior Member
-
Less
More
- Posts: 38
- Thank you received: 3
07 Oct 2026 23:05 #350162
by jazzkramer
Replied by jazzkramer on topic Is this a bug?
Sorry, I see now there are other posts about this error... I had some lags in the forum and I could not read them... I'm going to read them now.. I apologize for this thread, in case I don't find a solution I will go back here 
Please Log in or Create an account to join the conversation.
- FabLabRacing
- Away
- Junior Member
-
Less
More
- Posts: 20
- Thank you received: 15
10 Oct 2026 20:13 #350190
by FabLabRacing
Replied by FabLabRacing on topic Is this a bug?
I was able to run the GCode above without issue, so I dont think its your GCode
Please Log in or Create an account to join the conversation.
Moderators: snowgoer540
Time to create page: 0.191 seconds