Solidworks CAM CAMWorks Postprocessor

More
3 years 11 months ago #257953 by piflixe
Thanks for the reply. When I have some room for bigger leadin moves it works. But I can't figure out how to get it working in small pockets.

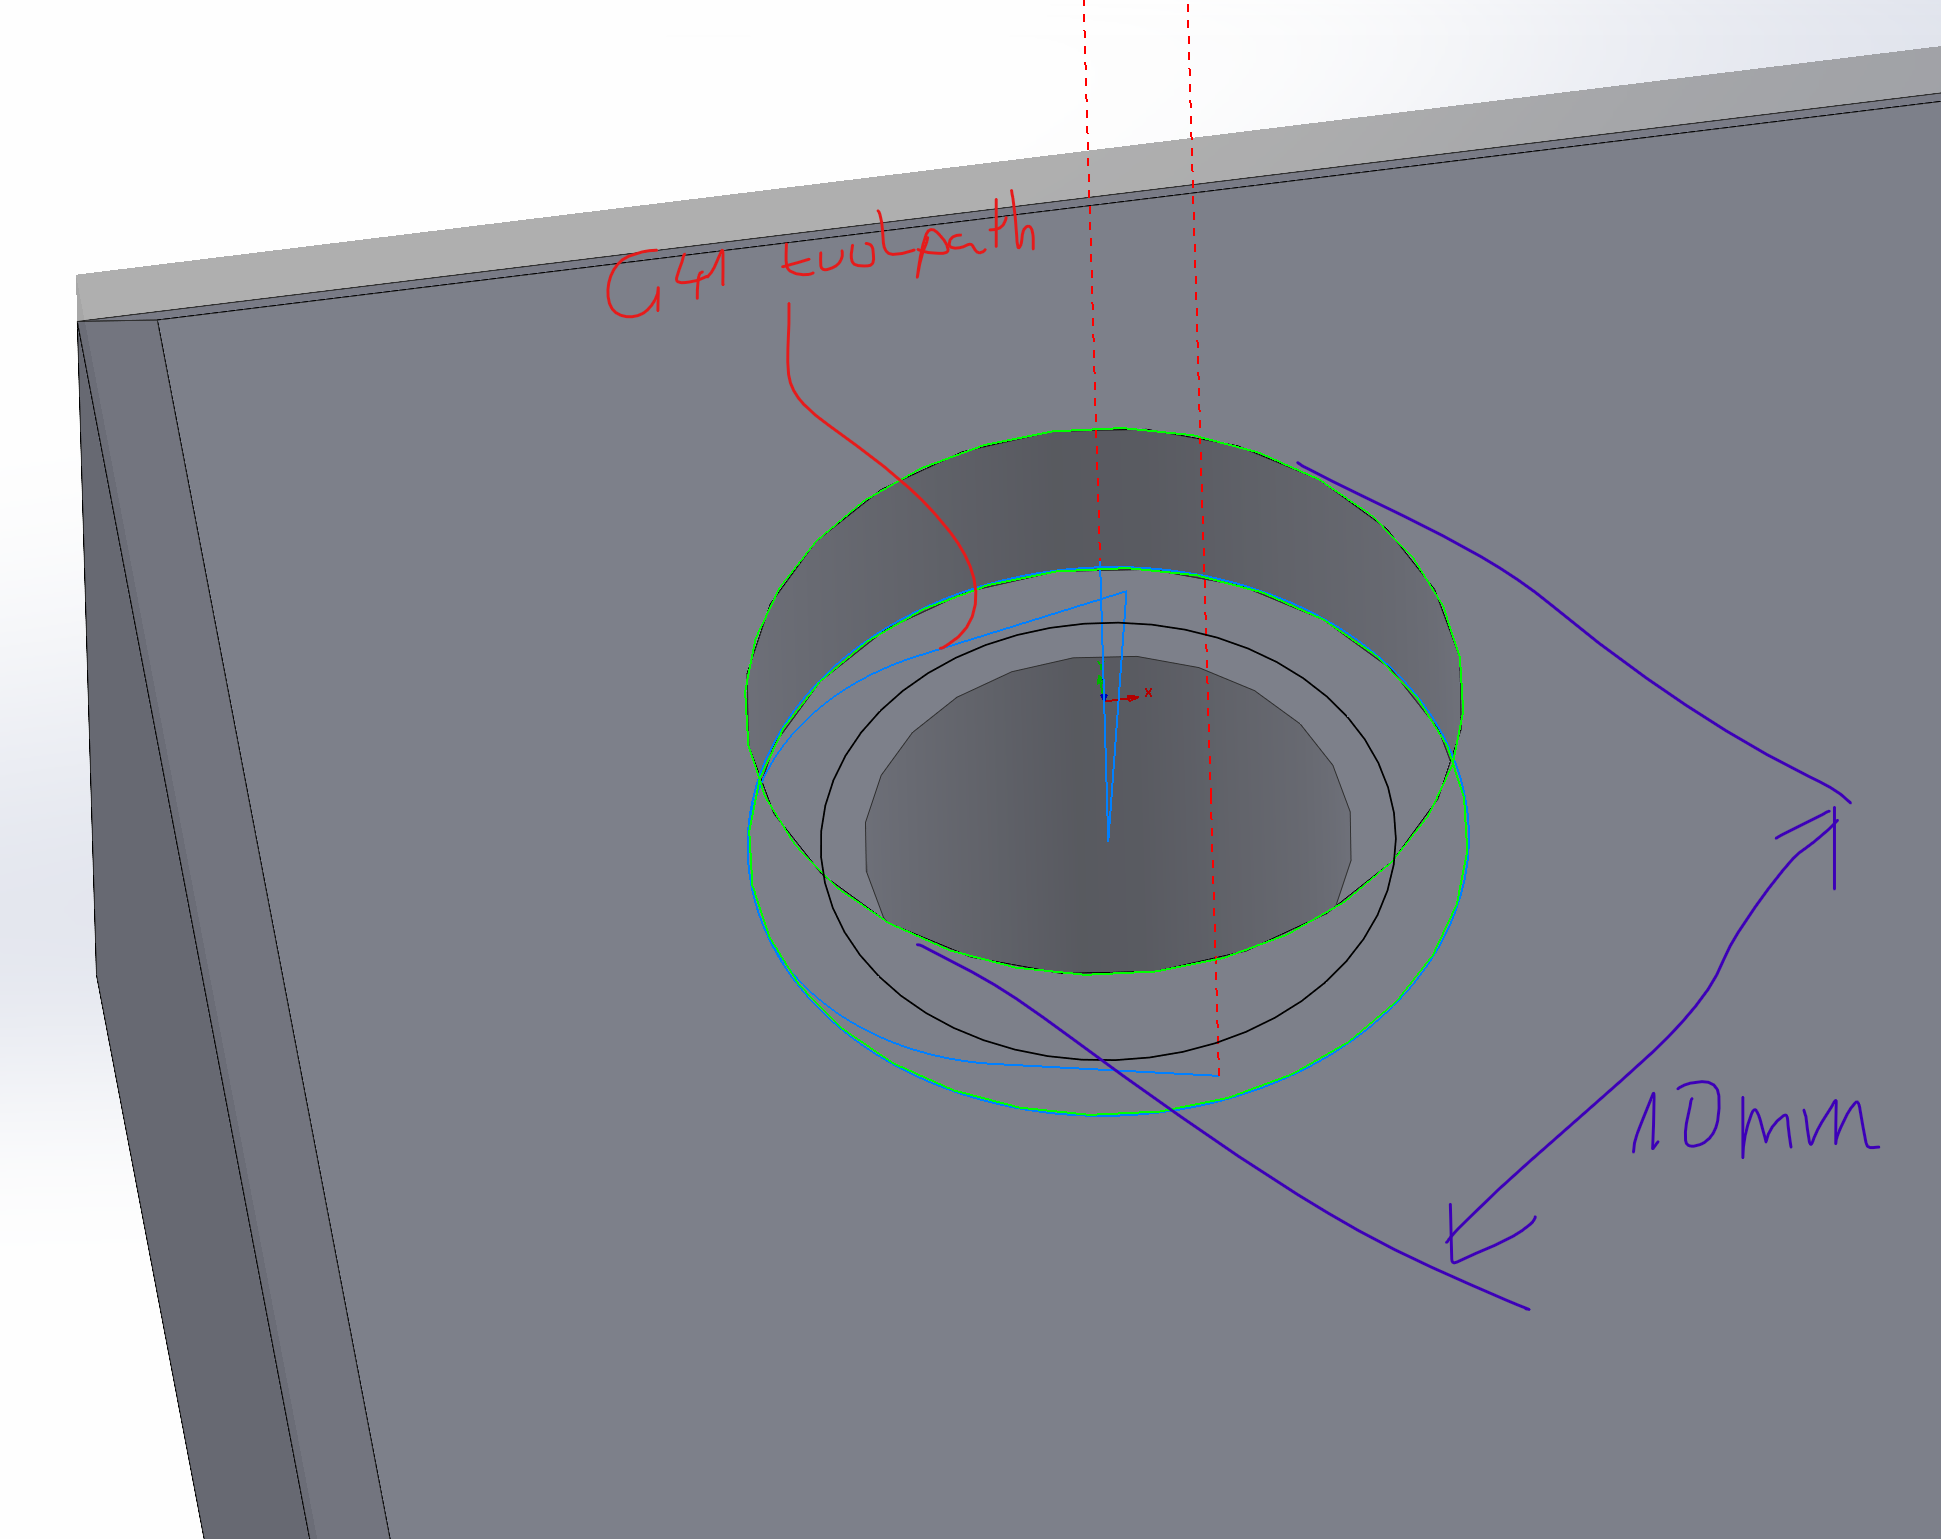
I made some screenshots to better explain the situation:

with all the NC settings set according to Ralfh's post above.

The G-Code looks like this:
Code:
( PART NAME=Grundplatte_FS4MG_Test_G41 ) ( X 346.00 Y 260.00 Z 15.00 ) G21 G17 G40 G49 G54 G80 G90 G64 P0.2 Q0.01 G53 G1 Z165 F1300 M5 T42 M6 (6mm VHM 4S - Enpro EPC449060) S3200 M3 M8 G90 G54 G0 X0 Y0 G1 F1300  Z3. Z-3. F300. G41 D42 X.907 Y4.487 F225. X-2.132 Y3.777 G3 X-4.979 Y.599 I.846 J-3.623 X-5.015 Y0 I4.979 J-.599 F300. I5.015 J0 X-4.979 Y-.599 I5.015 J0 X-2.132 Y-3.777 I3.693 J.444 G40 G1 X.907 Y-4.487 G0 Z3. Z25. M9 G53 G1 Z165 F1300 M5 M30 (0 MIN.  23 SEC. )

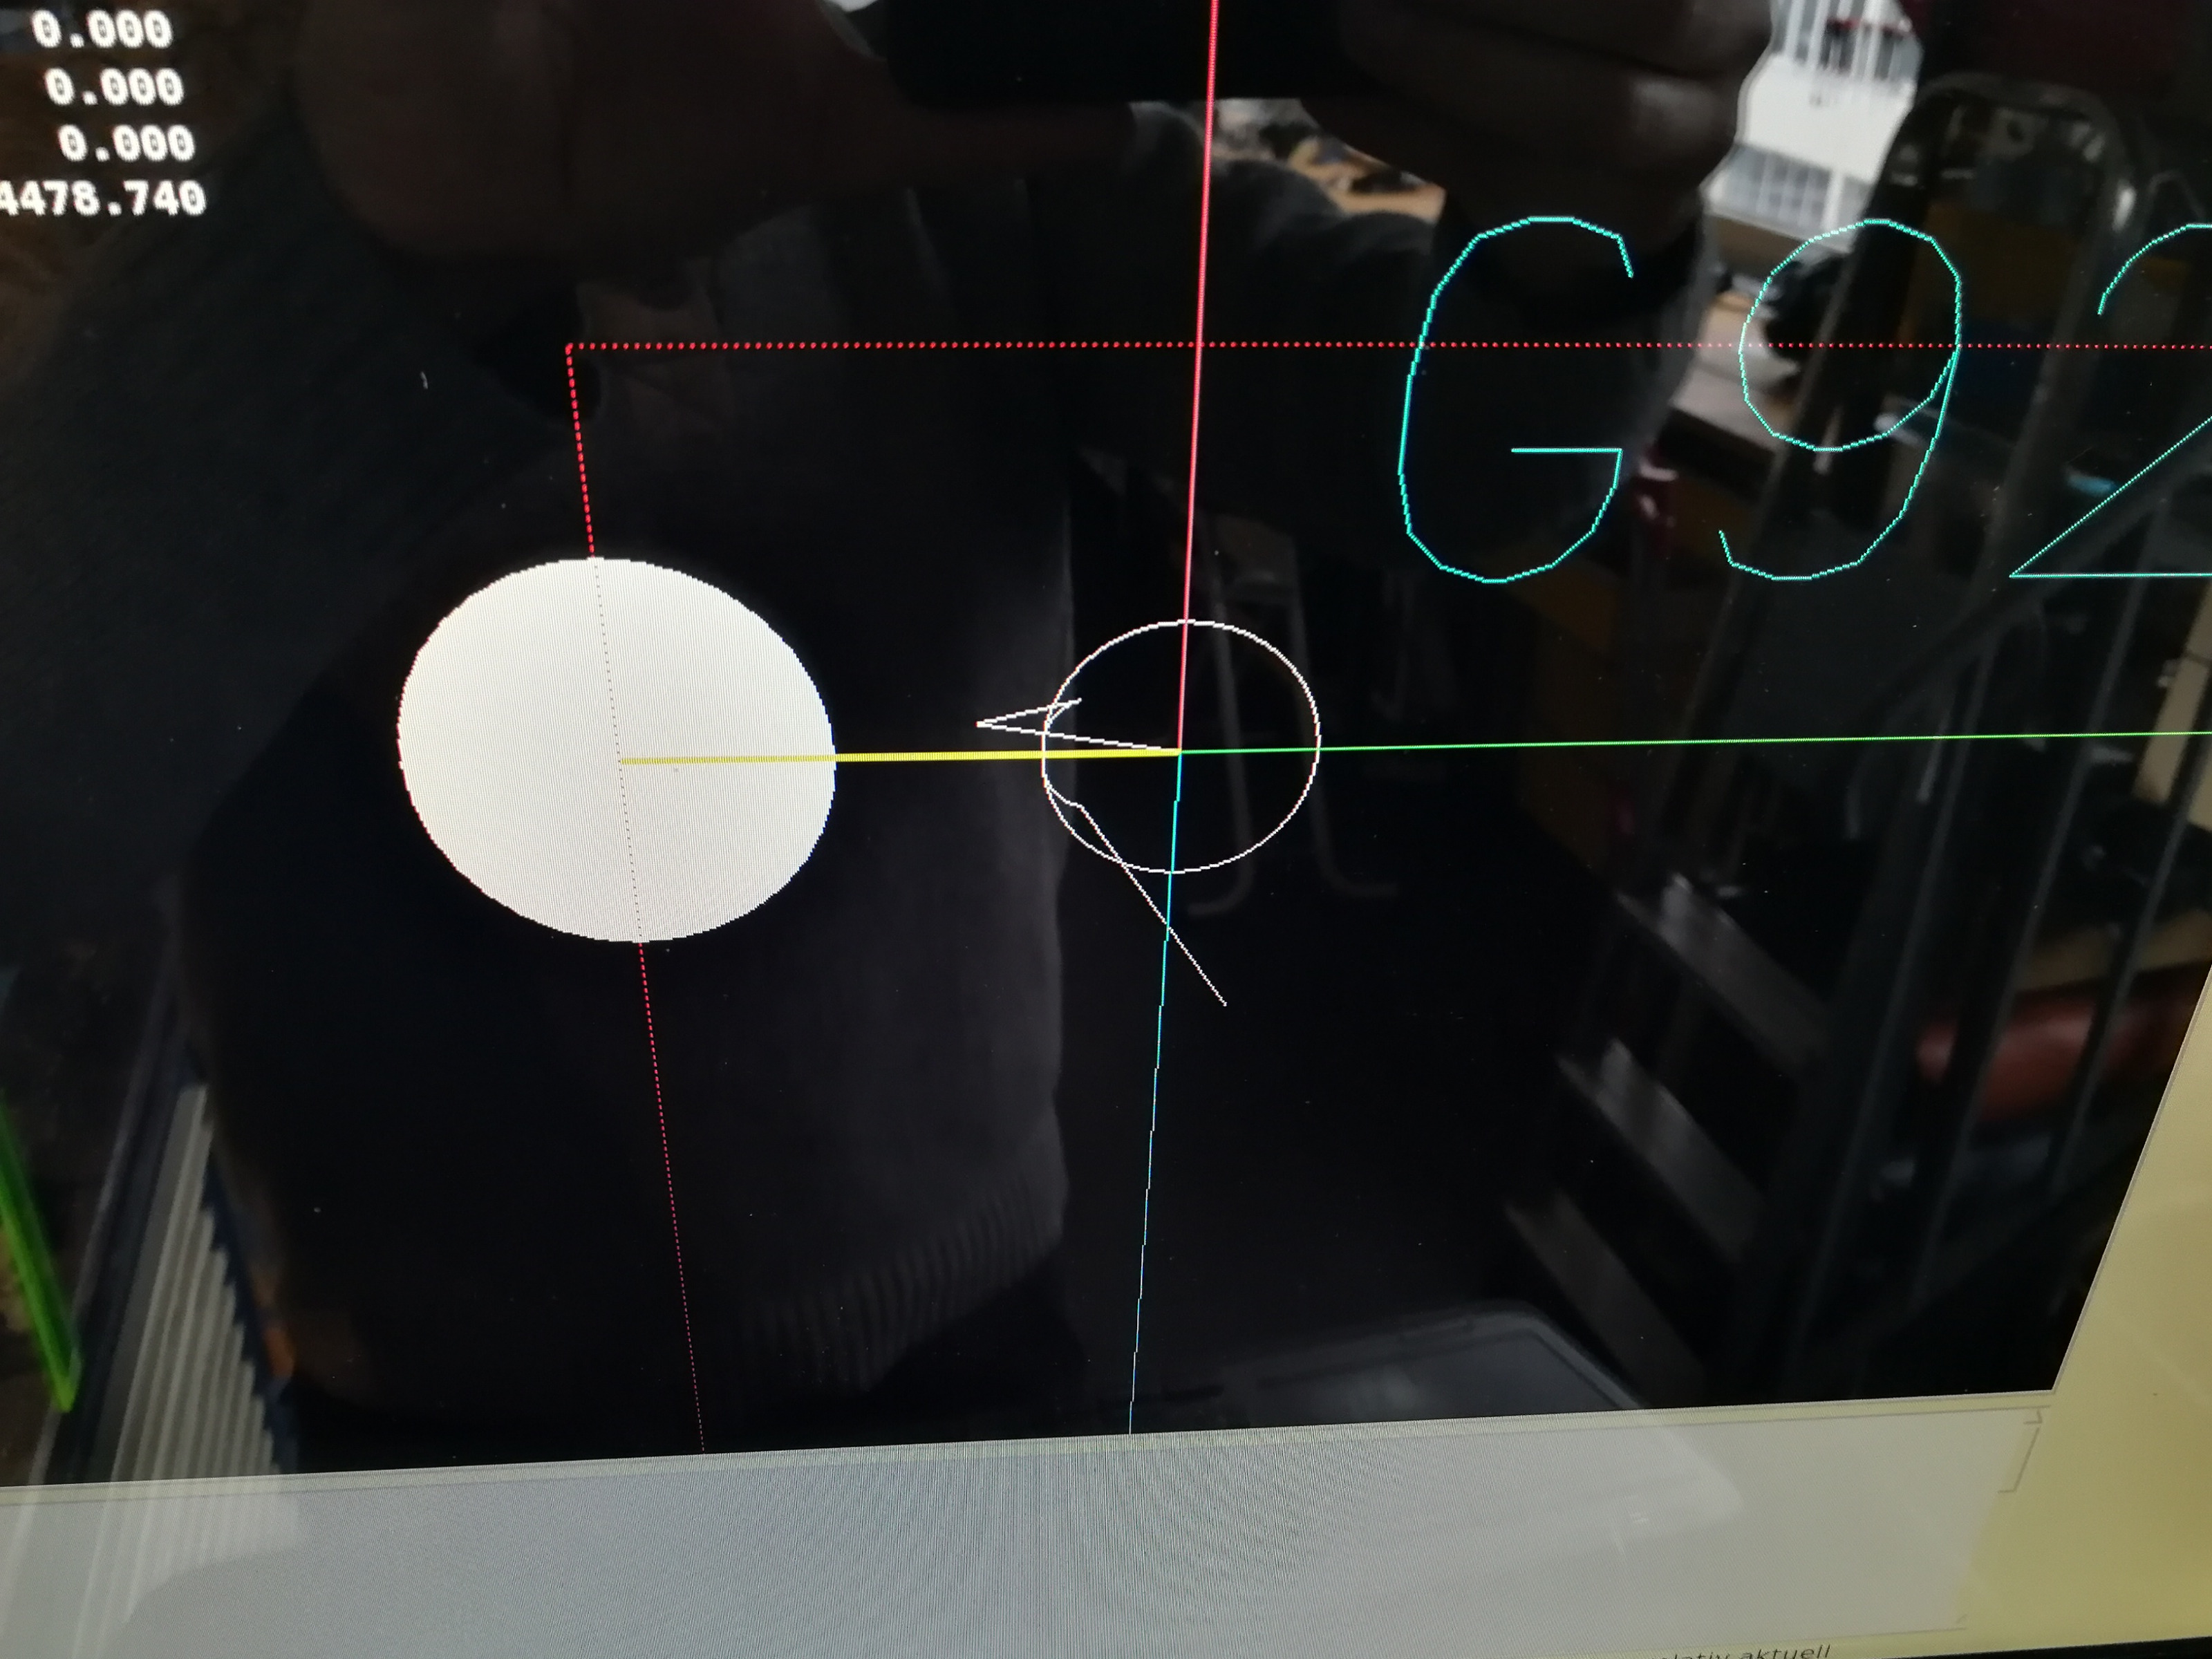
What I get in LinuxCNC looks like this:


By trying to understand the G-Code I thought the G40 command is too early and should be after the last move with a leadout going back to X0Y0.

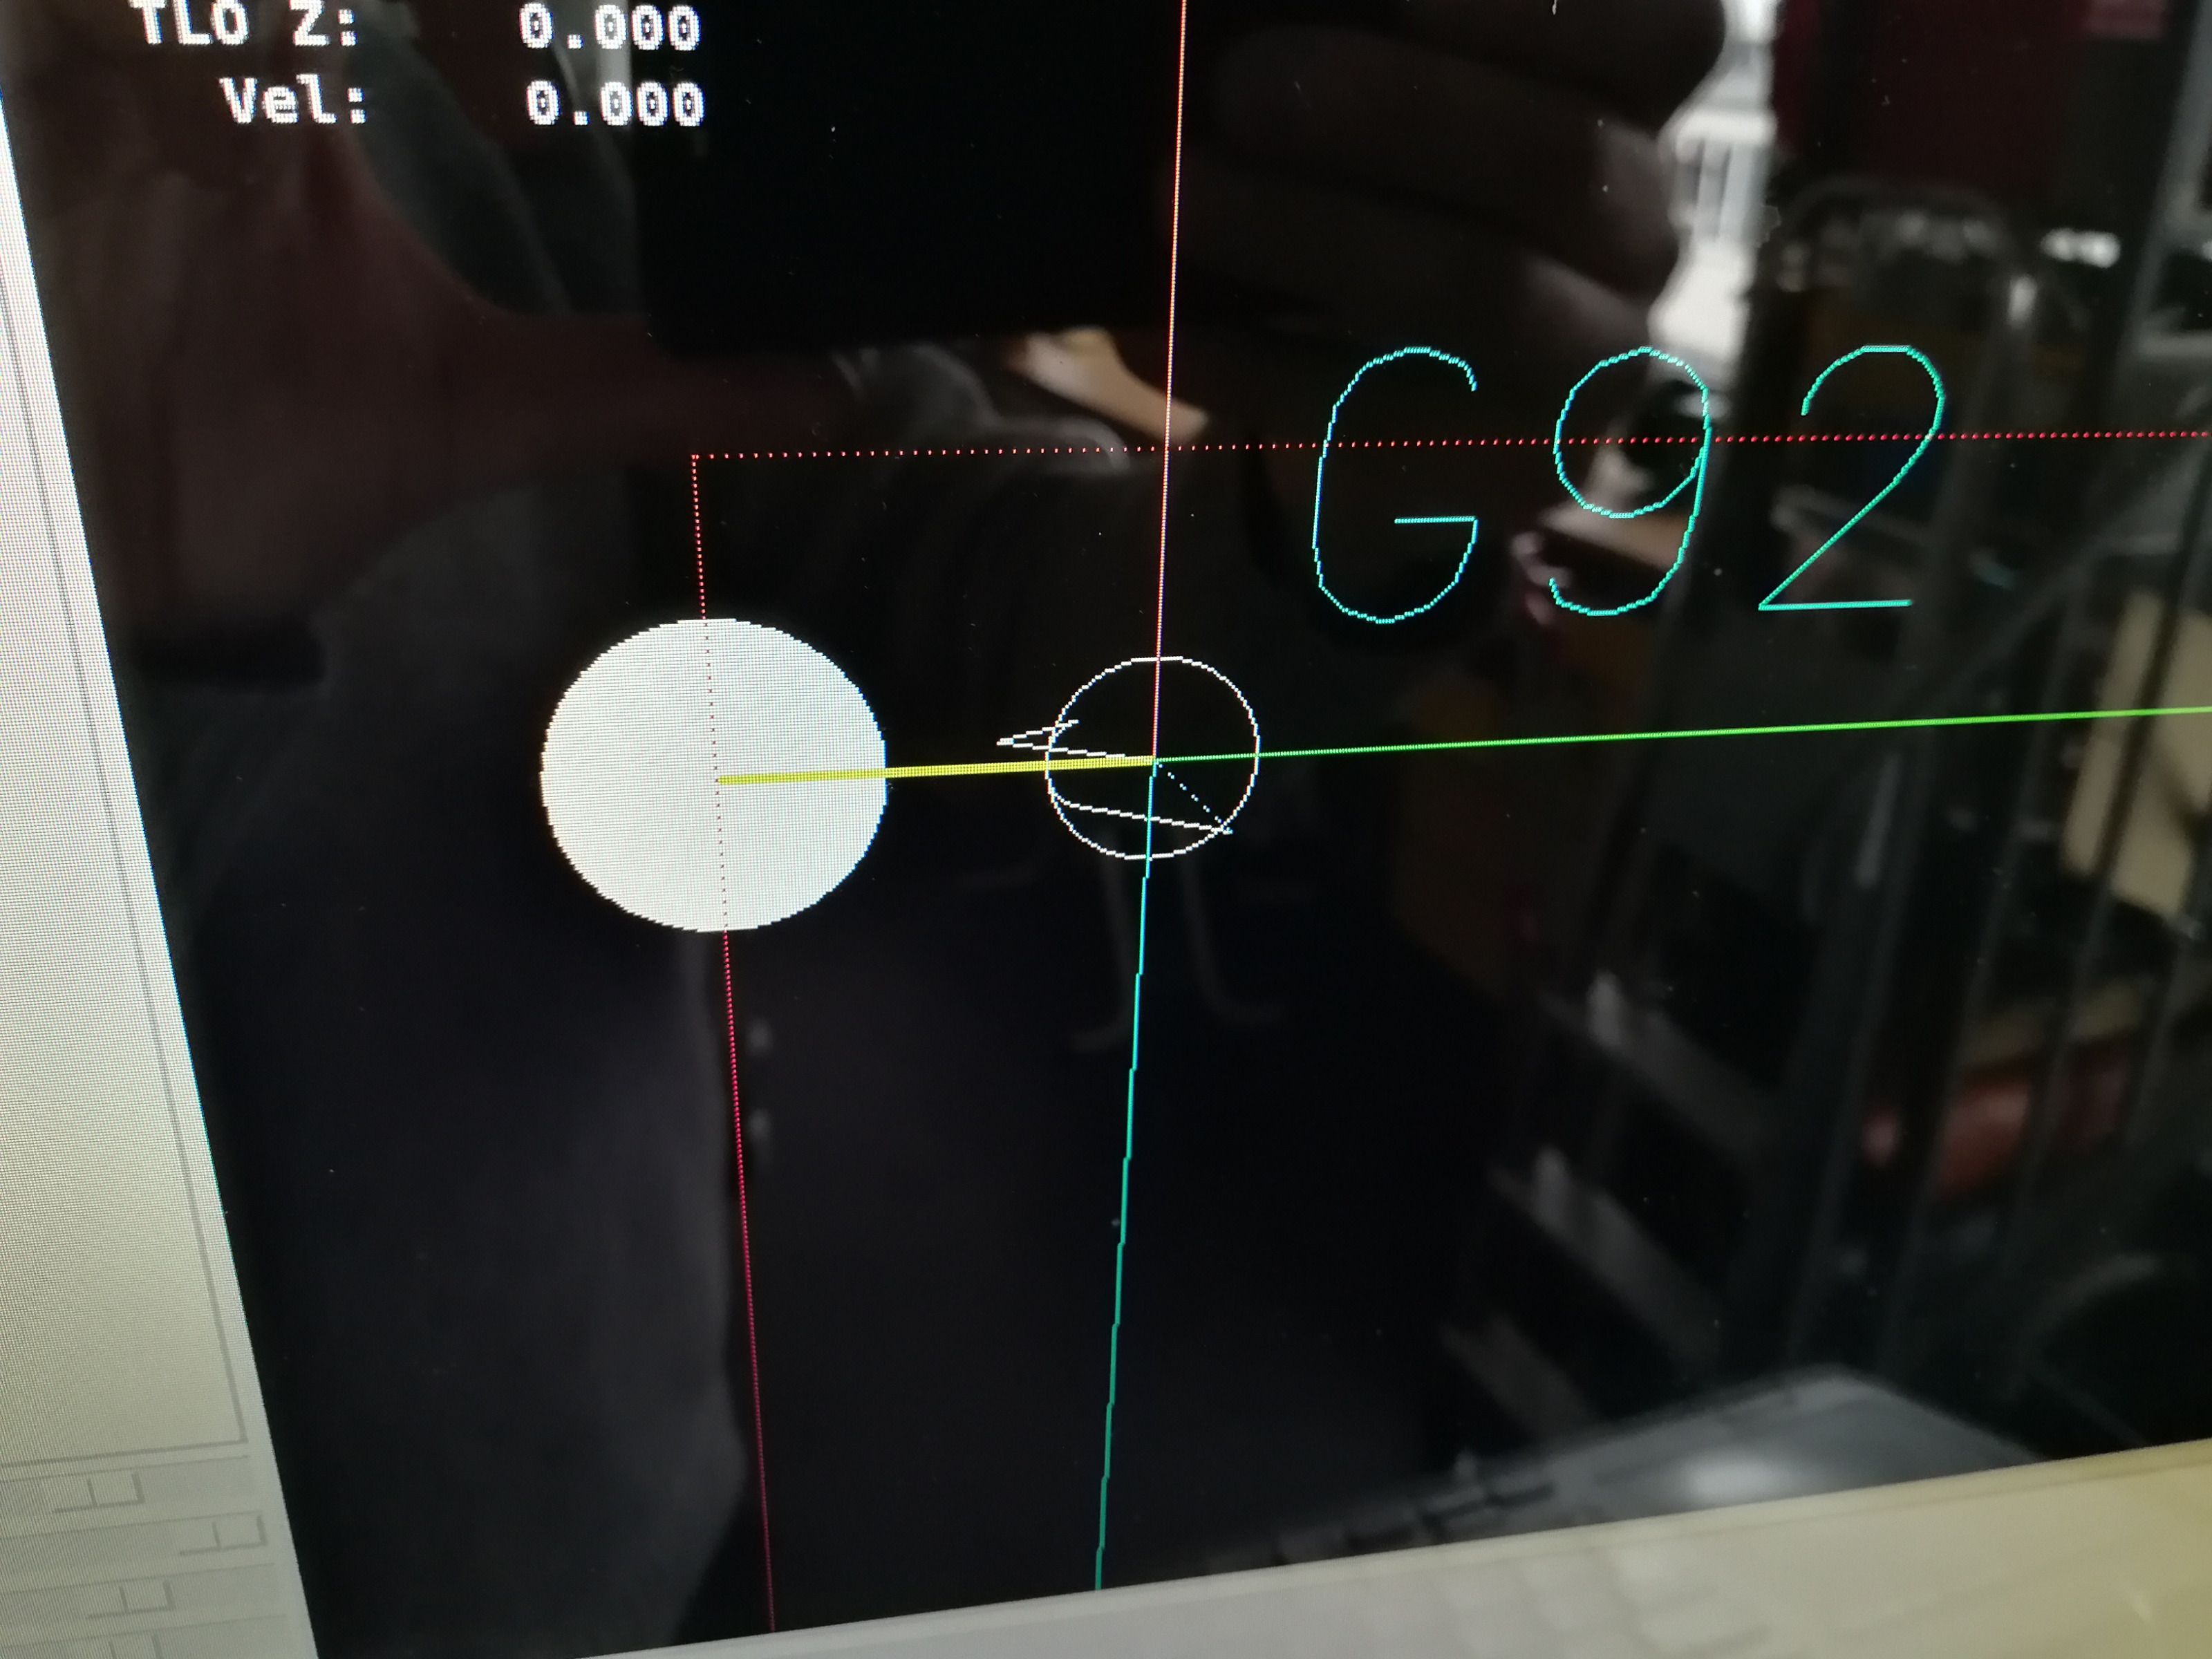
Then I get the following:


I tried moving around the G41 command to get better results but it did not work. When reading the code I can't figure out what is not correct? I am very thankful to any hints and help.

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #257954 by piflixe
By the way Ralfh: We added the G64 command in the START_OF_TAPE section of the PP. The default behaviour of LinuxCNC is to round the corners of Rapid and Cutting moves to achieve the highest possible speed. So this ended up in really large radii which seemed dangerous.

What I would like to get is a different setting for cutting and rapid moves. If possible this could be set globally in LinuxCNC . But from my understanding this is not implemented. So I tried to modify the PP but did not succeed in creating a new modal G64 call with a variable P. P is already taken by other commands and seemed to be defined as an integer.

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago - 3 years 11 months ago #257955 by Ralfh
Ah, i see. Please try to cut the hole with a diameter at least half as big as the diameter of the hole. 

See: linuxcnc.org/docs/2.6/html/gcode/tool_co...:cutter-compensation

Programming Entry Moves -> The minimum length is the cutter radius

When you want to start at X0Y0 and your entry cut is already >3mm and your endmill radius another 3mm you get a hole of at least 12mm? I don't know exactly image missing /media/kunena/emoticons/laughing.png
Last edit: 3 years 11 months ago by Ralfh. Reason: I redid the math

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #257956 by Ralfh
If i remember correctly, you can also program the "P" as text in the postprocessor. Linuxcnc doesn't care, it sees a "P" and is happy.

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #257957 by piflixe
yes we tried using the P as text and that is what we did in the START_OF_TAPE. But then we could not make it modal. So if we want to make it switch between different settings for rapid and cut moves then it would appear in every line. Also tried putting it in the RAPID_DOWN / RAPID_UP moves but did not get a reliable behaviour.

Please Log in or Create an account to join the conversation.

More
3 years 11 months ago #257958 by Ralfh
Ah, i understand. Sadly i can't help in this case...

Please Log in or Create an account to join the conversation.

Time to create page: 0.064 seconds
Powered by Kunena Forum