Probe Basic Not Remembering Current Pocket Number

More
1 year 4 months ago #330366 by djones@burketruck.com
We are just finishing up our linuxcnc retrofit with Probe Basic on our Mazak VTC16B. Everything seems to work just fine, except we are having an issue with the controller not keeping track of the current pocket number (Parameter #3990). The machine has a 24 position index style carousel ATC. It indexes correctly and on the first try after indexing, it will grab or store the appropriate tool in the appropriate pocket using M6 commands. After the first toolchange though, it's almost as if the controller resets itself as starting from Pocket 1. The GUI shows the correct pocket that is supposed to be used. 

For example, if we start with Tool 3 in our spindle, Pocket 3 empty, Tools 2 & 3 in pockets 2&3; just after indexing if we store Tool 3 in carousel, it will rotate to pocket 3 and store the tool. If we then run a M6 T2, instead of rotating -1 pocket to grab T2, it will rotate +1 pocket, as if it were starting back at pocket 1. When doing this, the GUI shows pocket 3 being the active pocket and rotating +1 to pocket 4.

I'm assuming it has something to do with parameter 3990 not being updated or called out properly. We had to make some changes to the default config to make it all work with our machine. I've attached some of the proper config files, would somebody be able to provide any insight on where to start diagnosing this?

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330368 by Lcvette
Have you added the appropriate parameters in the car file for pockets and atc parameter function storing? Have you adjusted the macros for your atc pocket count for the calculations? What version of probe basic are you using?

Do you have a GitHub with your files where I can review them all?

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330372 by djones@burketruck.com
github.com/ddjmechservices/MAZAK-VTC16B.git

We are working off of the Probe-Basic-Staging branch proofing everything out before we merge it with the main branch.

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330377 by Lcvette
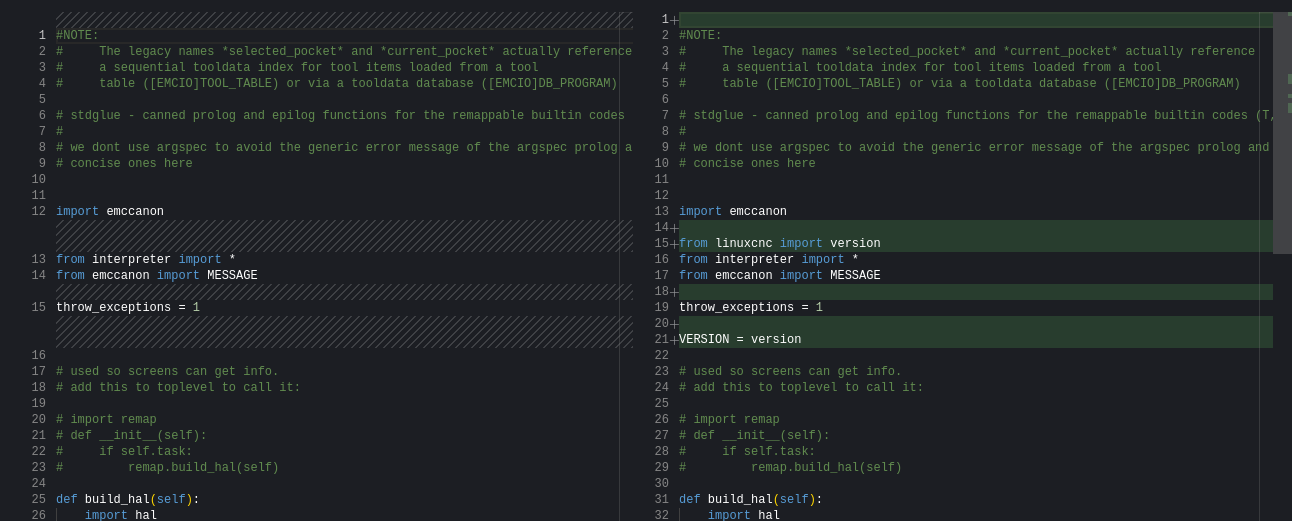
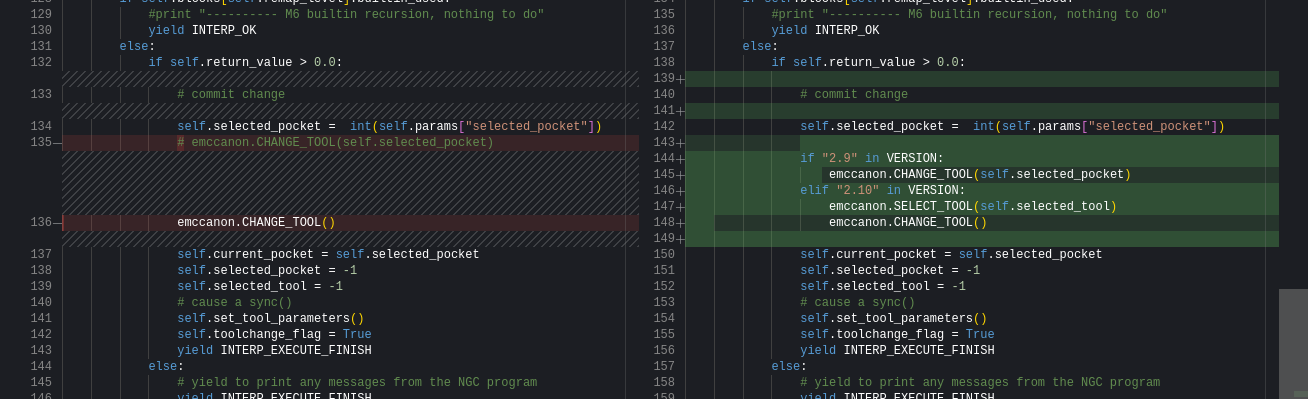
What version of linuxcnc are you running. We noticed the python broke on atc between 2.9.4 and 2.10 master.

If you're running master, check the updated python file from the latest develop version of probe basic. Run a meld file comparison to see if the latest edit is in your current python file.

Beyond that, just come through your subroutines. Check pocket counts to make sure your not dropping an index signal for some reason.

As debug everywhere to see everything is doing what you expect.

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330391 by djones@burketruck.com
I am running the 2.9.4nyx53 which is just linuxcnc 2.9.4 with the Yurtaev Nyx communication module for Mitsubishi Meldas drives. Just to confirm, the python break was on 2.10?

I'll check the subroutines and see if there is anything that drops the index or pulse signal.


Thanks!

Please Log in or Create an account to join the conversation.

More
1 year 4 months ago #330398 by Lcvette
correct, here was the required change, we made a either or fix in the file. but if you are on 2,9,4, unless what ever broke things in 2.10 was also added to your specific branch version of 2.9.4 for what ever reason. either way, i would grab the latest python stdglue file and pop it in your config folder just to be safe.


Please Log in or Create an account to join the conversation.

Moderators: KCJ, Lcvette
Time to create page: 0.353 seconds
Powered by Kunena Forum