Hello All,
New to the forum and first of all would like to thank you for the valuable information you guys post, it has helped so much me moving ahead with my build. id appreciate your help with my issue where it cannot activate the thc even when all the settings (that i know of) have been properly adjusted. first my setup:
-LinuxCNC QTPlasmac table
-Rpi5 with image LinuxCNC 2.9.8 Raspberry Pi 4/5 OS based on Debian Trixie
-Mesa 7176s over ethernet
-THCAD2 + 3M resistor array enclosed near the plasma source, F+/F- routed to mesaboard encoder input A with shielded microphone cable grounded at control side, also used a more simple twisted pair for testing.
-Used Pnconf for setting thcad2 trimming and ratio
Tested for correct voltage measuring for example, hooked a power supply from 39 to 56 volts and Main screen voltage readings coincide very accurately to multimeter reading.
-Flaring 65 plasma source with no cnc interface. (HF piercing) voltage probing connected to torch (-) and clamp (+) leads.
-For testing im using a straight line of 100mm at full speed so thc is not affected by speed reduction (tested from 400 to 1800 mm/min)
-THC is enabled
-Mode 0 is used so arc ok is derived from voltage readings
-setup plasmac.arc_lost_delay =.3 as was having some issues for getting it to start cutting due to initial spike/valley.
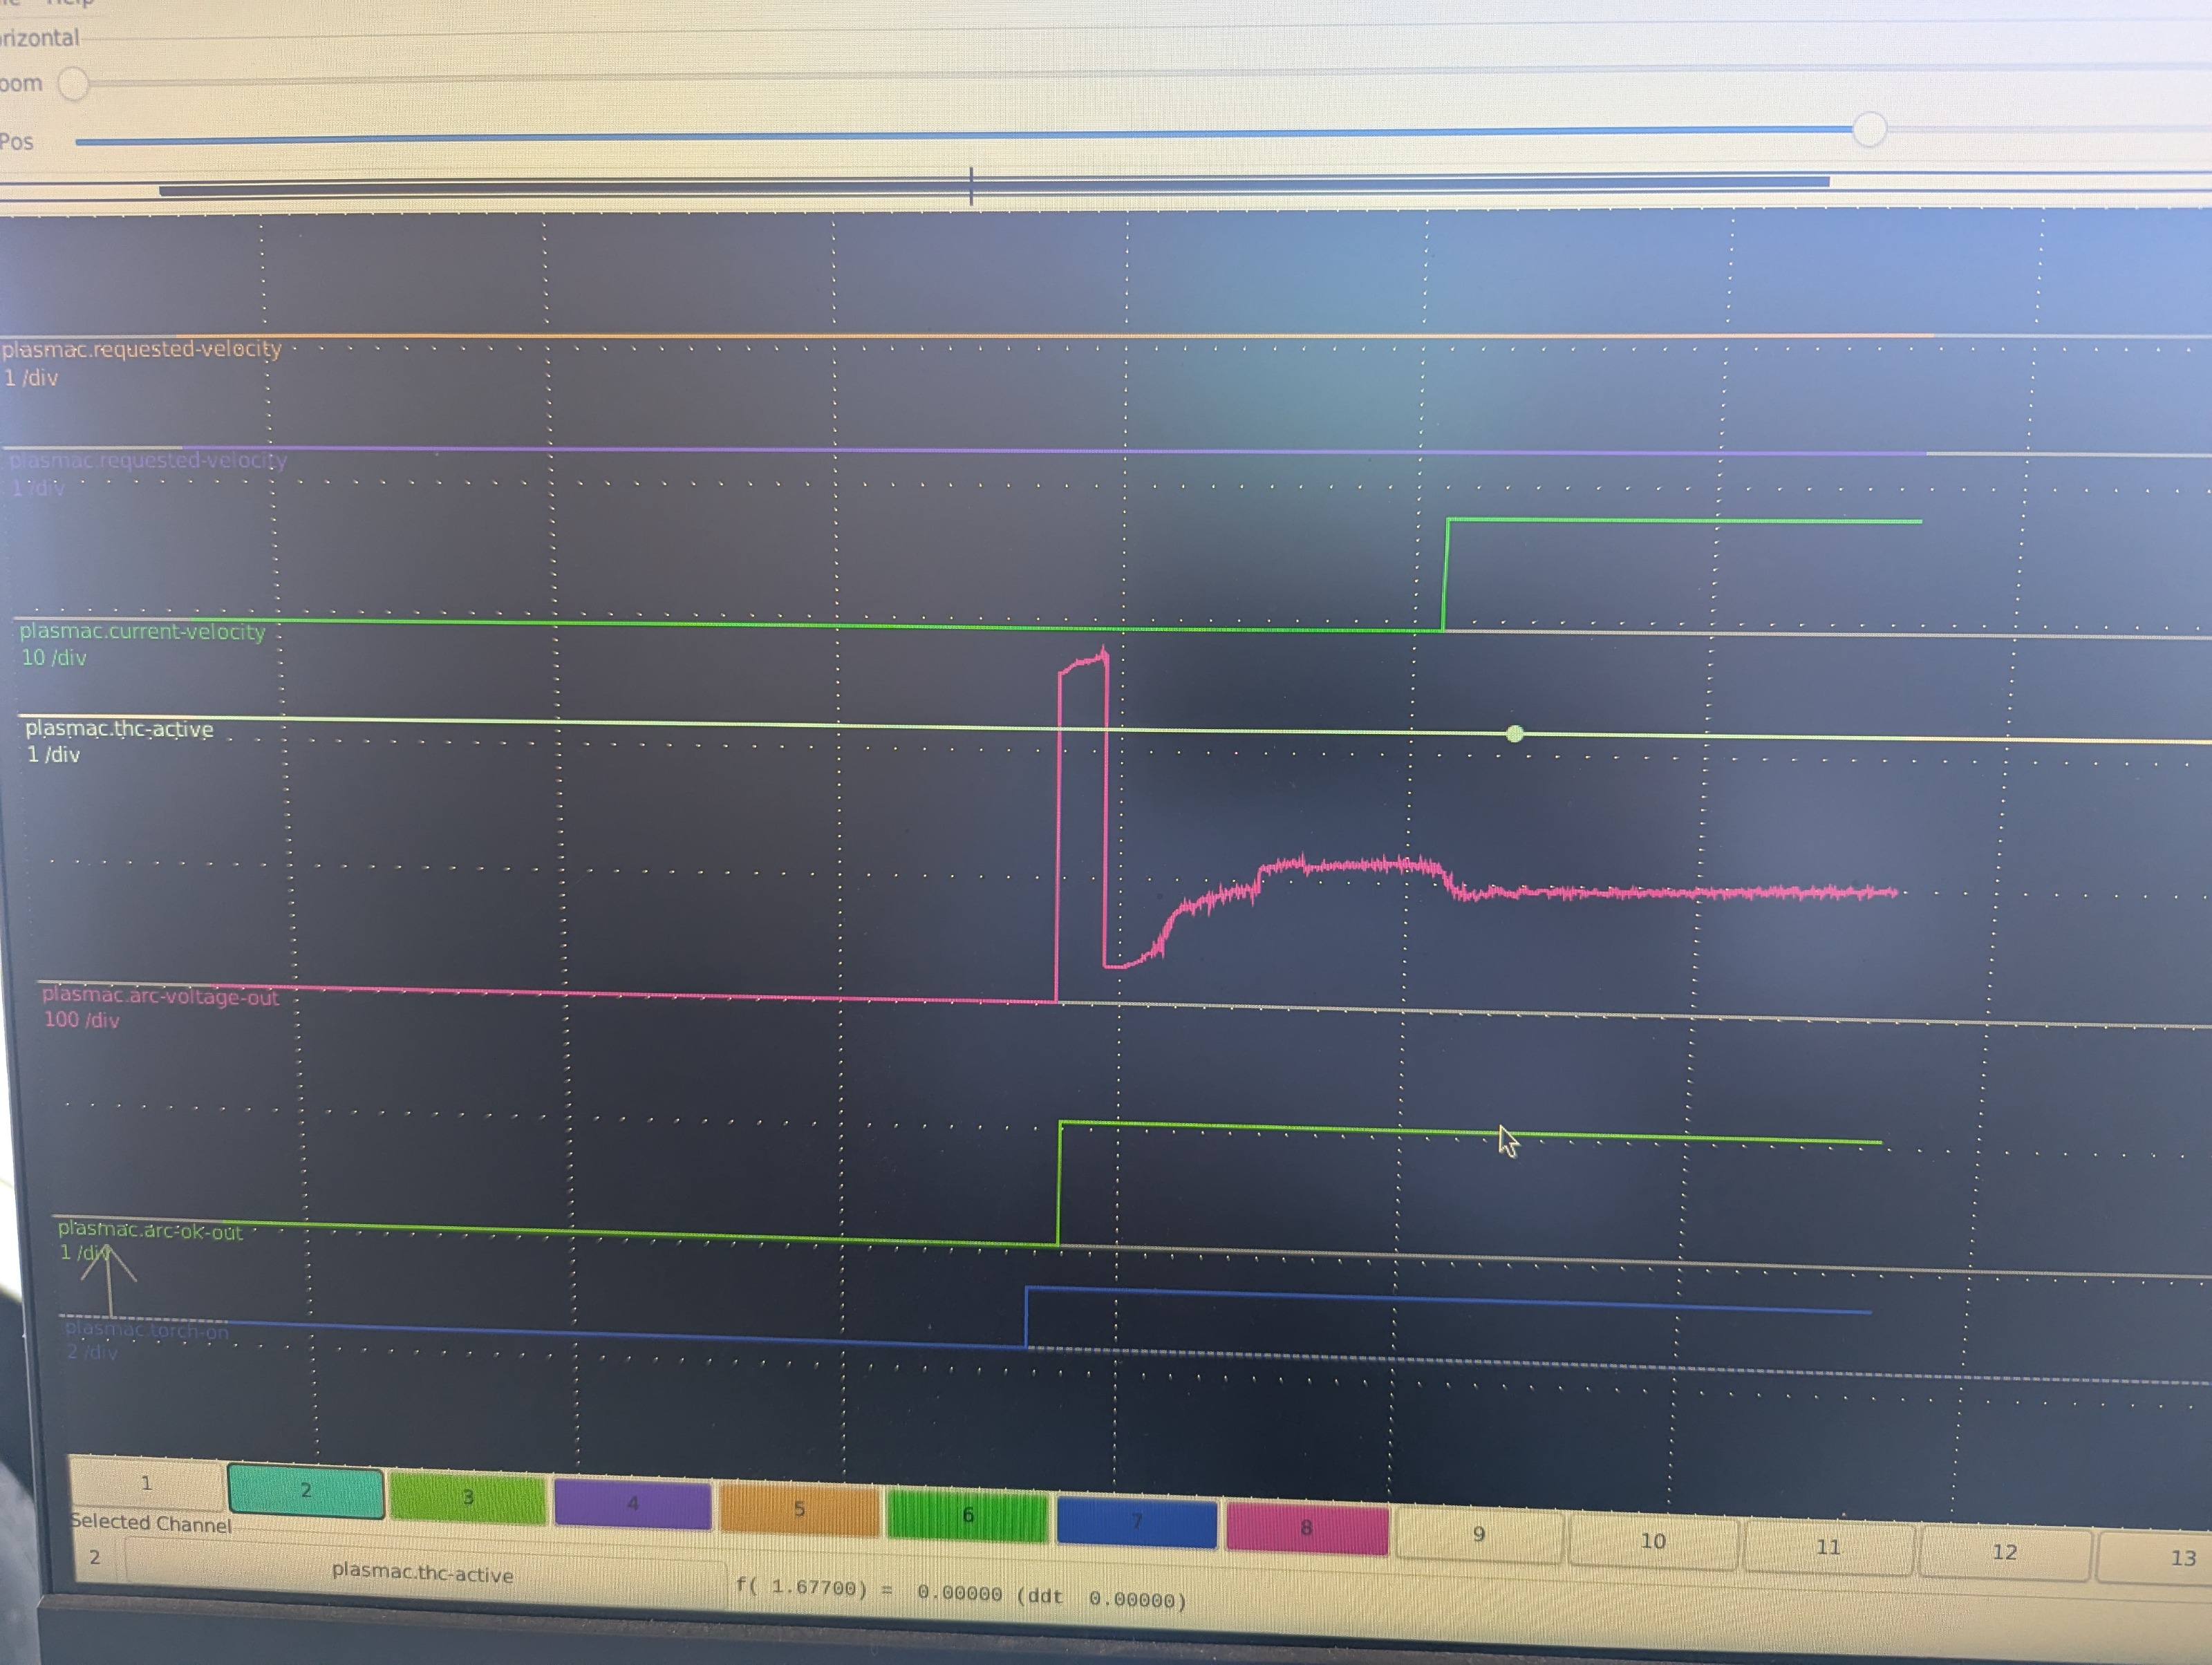
I took the follwing HALSCOPE trace where:
1)torch on triggers,
2)probe voltage goes to 260 for piercing, then falls, then recovers to around 94v
3)Arc OK signal goes to true
4)Pierce delay elapses
5)Movement starts
6)THC active never goes up and of course no correction
as Far as I can see voltage is "stable" once cut starts and there is no variation that could lead to deactivation as the tresholds are LOW=39 HIGH 990 (for testing purposes), samples 10 and threshold voltage 10.
has anyone had this issue or any lead on what to look at?