Search Results (Searched for: )

  • RMJ fabrication
30 May 2026 05:50
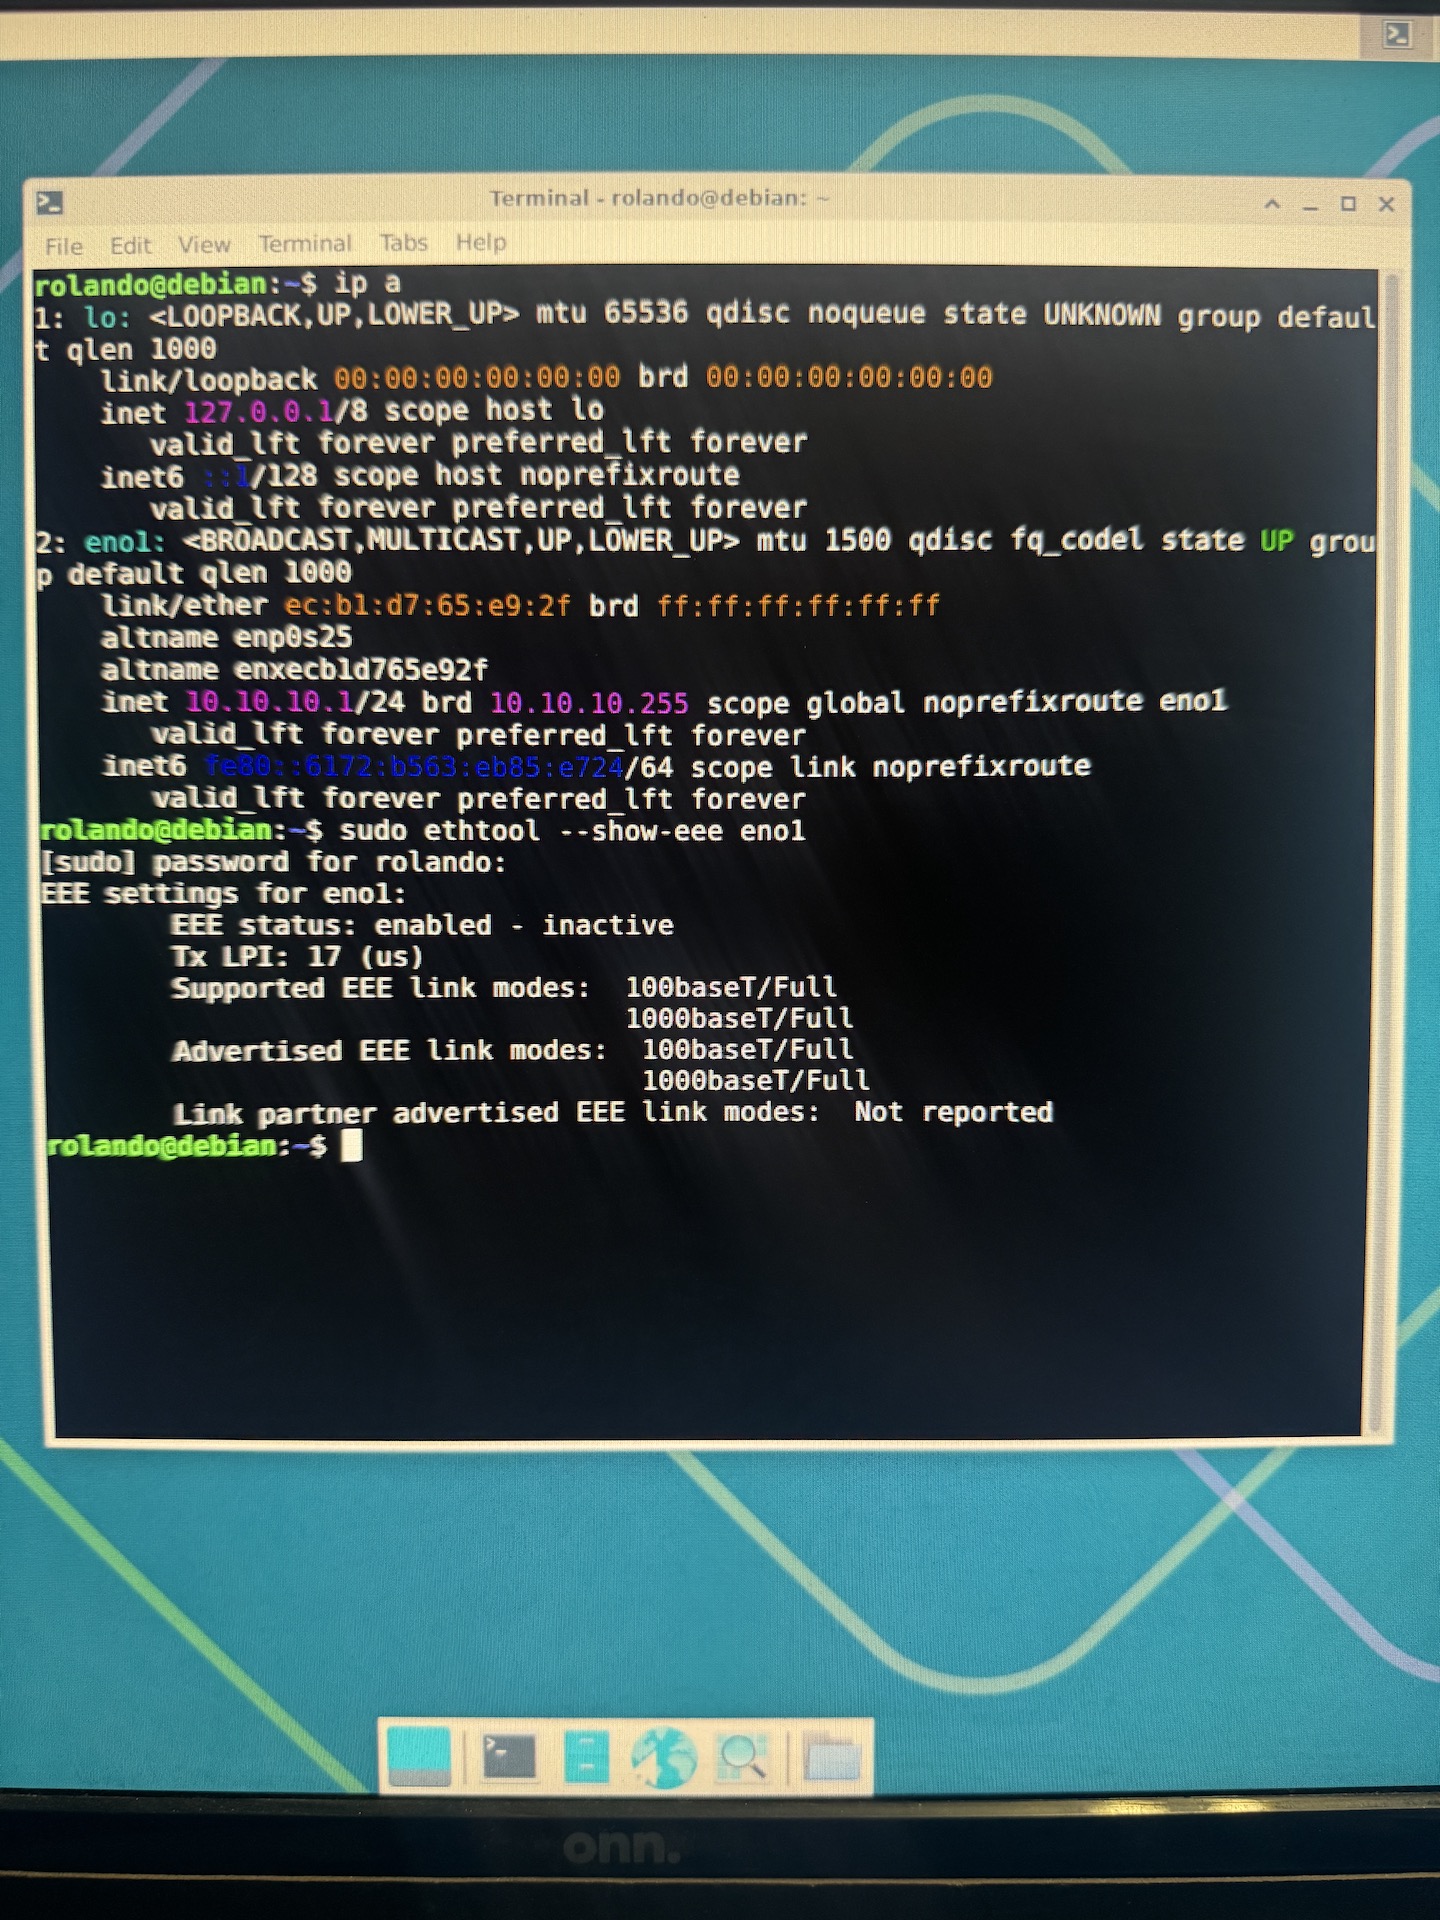
sudo ethtool works 
  • Asymmetrisch
30 May 2026 05:22
Replied by Asymmetrisch on topic TTL to differential converter (STEP / DIR / ENABLE)
I have several motor controllers that are driven by differential signals (CLK, #CLK, DIR, #DIR) – the inputs (5V, Ri = 120 Ohm) are not optically isolated. At first glance, it seems that controlling it with my Mesa 7i76EU works perfectly.

For testing purposes, I'd like to use the parallel port or possibly a RP2040 – in addition, I have a "Benezan Mini Breakout Board" left over from a previous setup that I could use.
It would be great if there were a solution for this.
  • rodw
30 May 2026 05:16
probably needs sudo ethtool
  • RMJ fabrication
30 May 2026 05:08
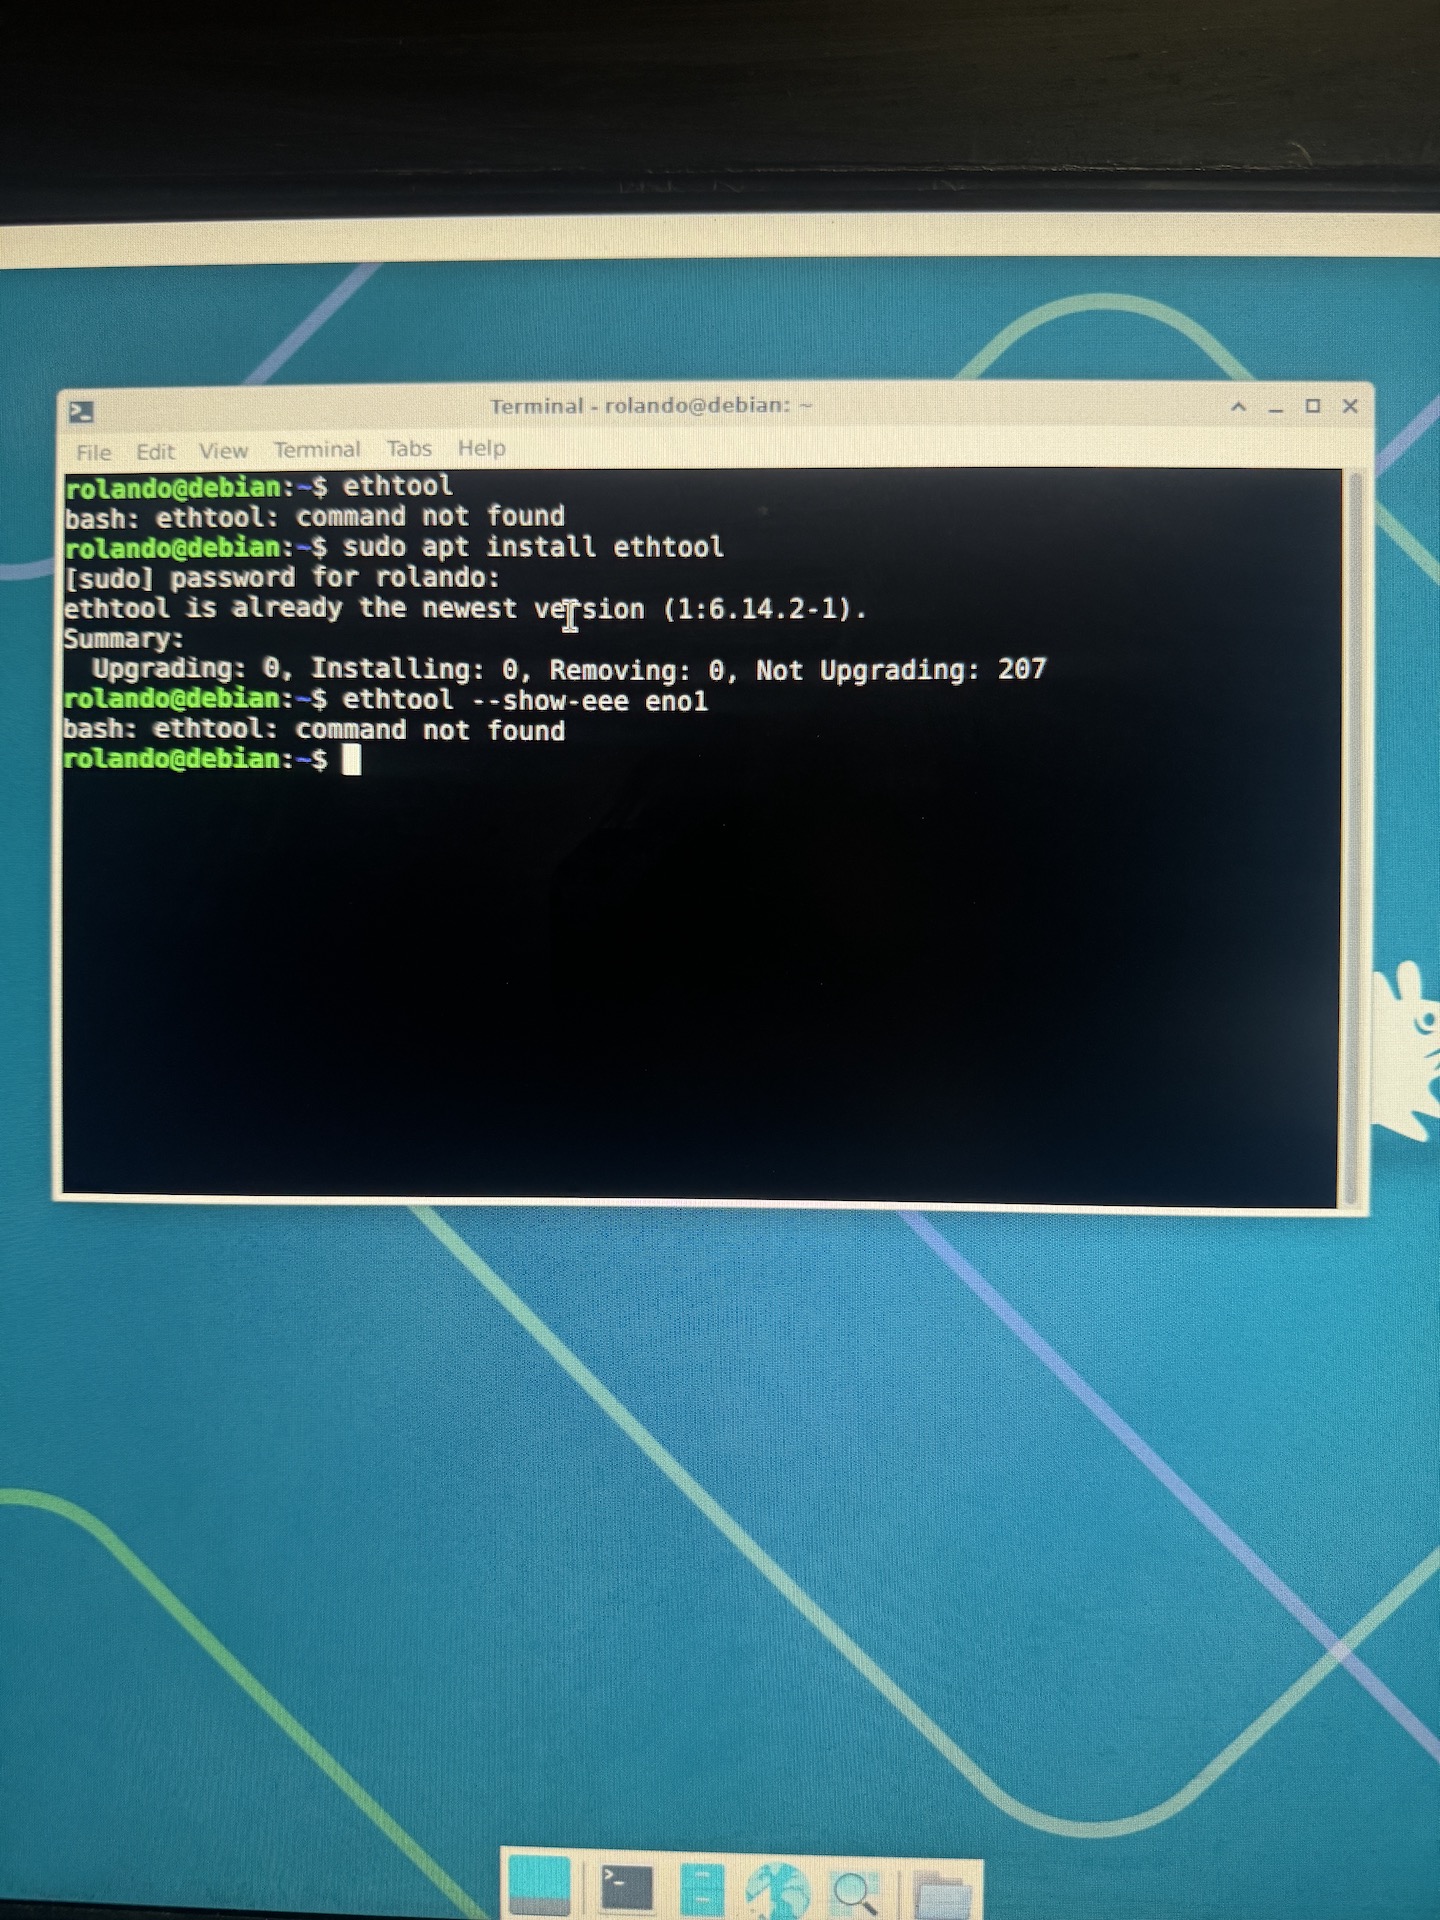
I installed ethtool and I am still getting command not found 
  • rodw
30 May 2026 04:30
I did a video recently about this
  • rodw
30 May 2026 04:07
isolate the last core with isolcpus
Disable coalescing if intel
Use dkms driver if realtek
Set CPU affinity for NIC interrupt to be same as the isolated core
  • PCW
30 May 2026 03:34
Yes, the network is not setup properly (no fixed IP address)
 
  • tommylight
30 May 2026 03:24
sudo apt install ethtool
-
And the network is not set up properly or not connected???
  • RMJ fabrication
30 May 2026 03:19
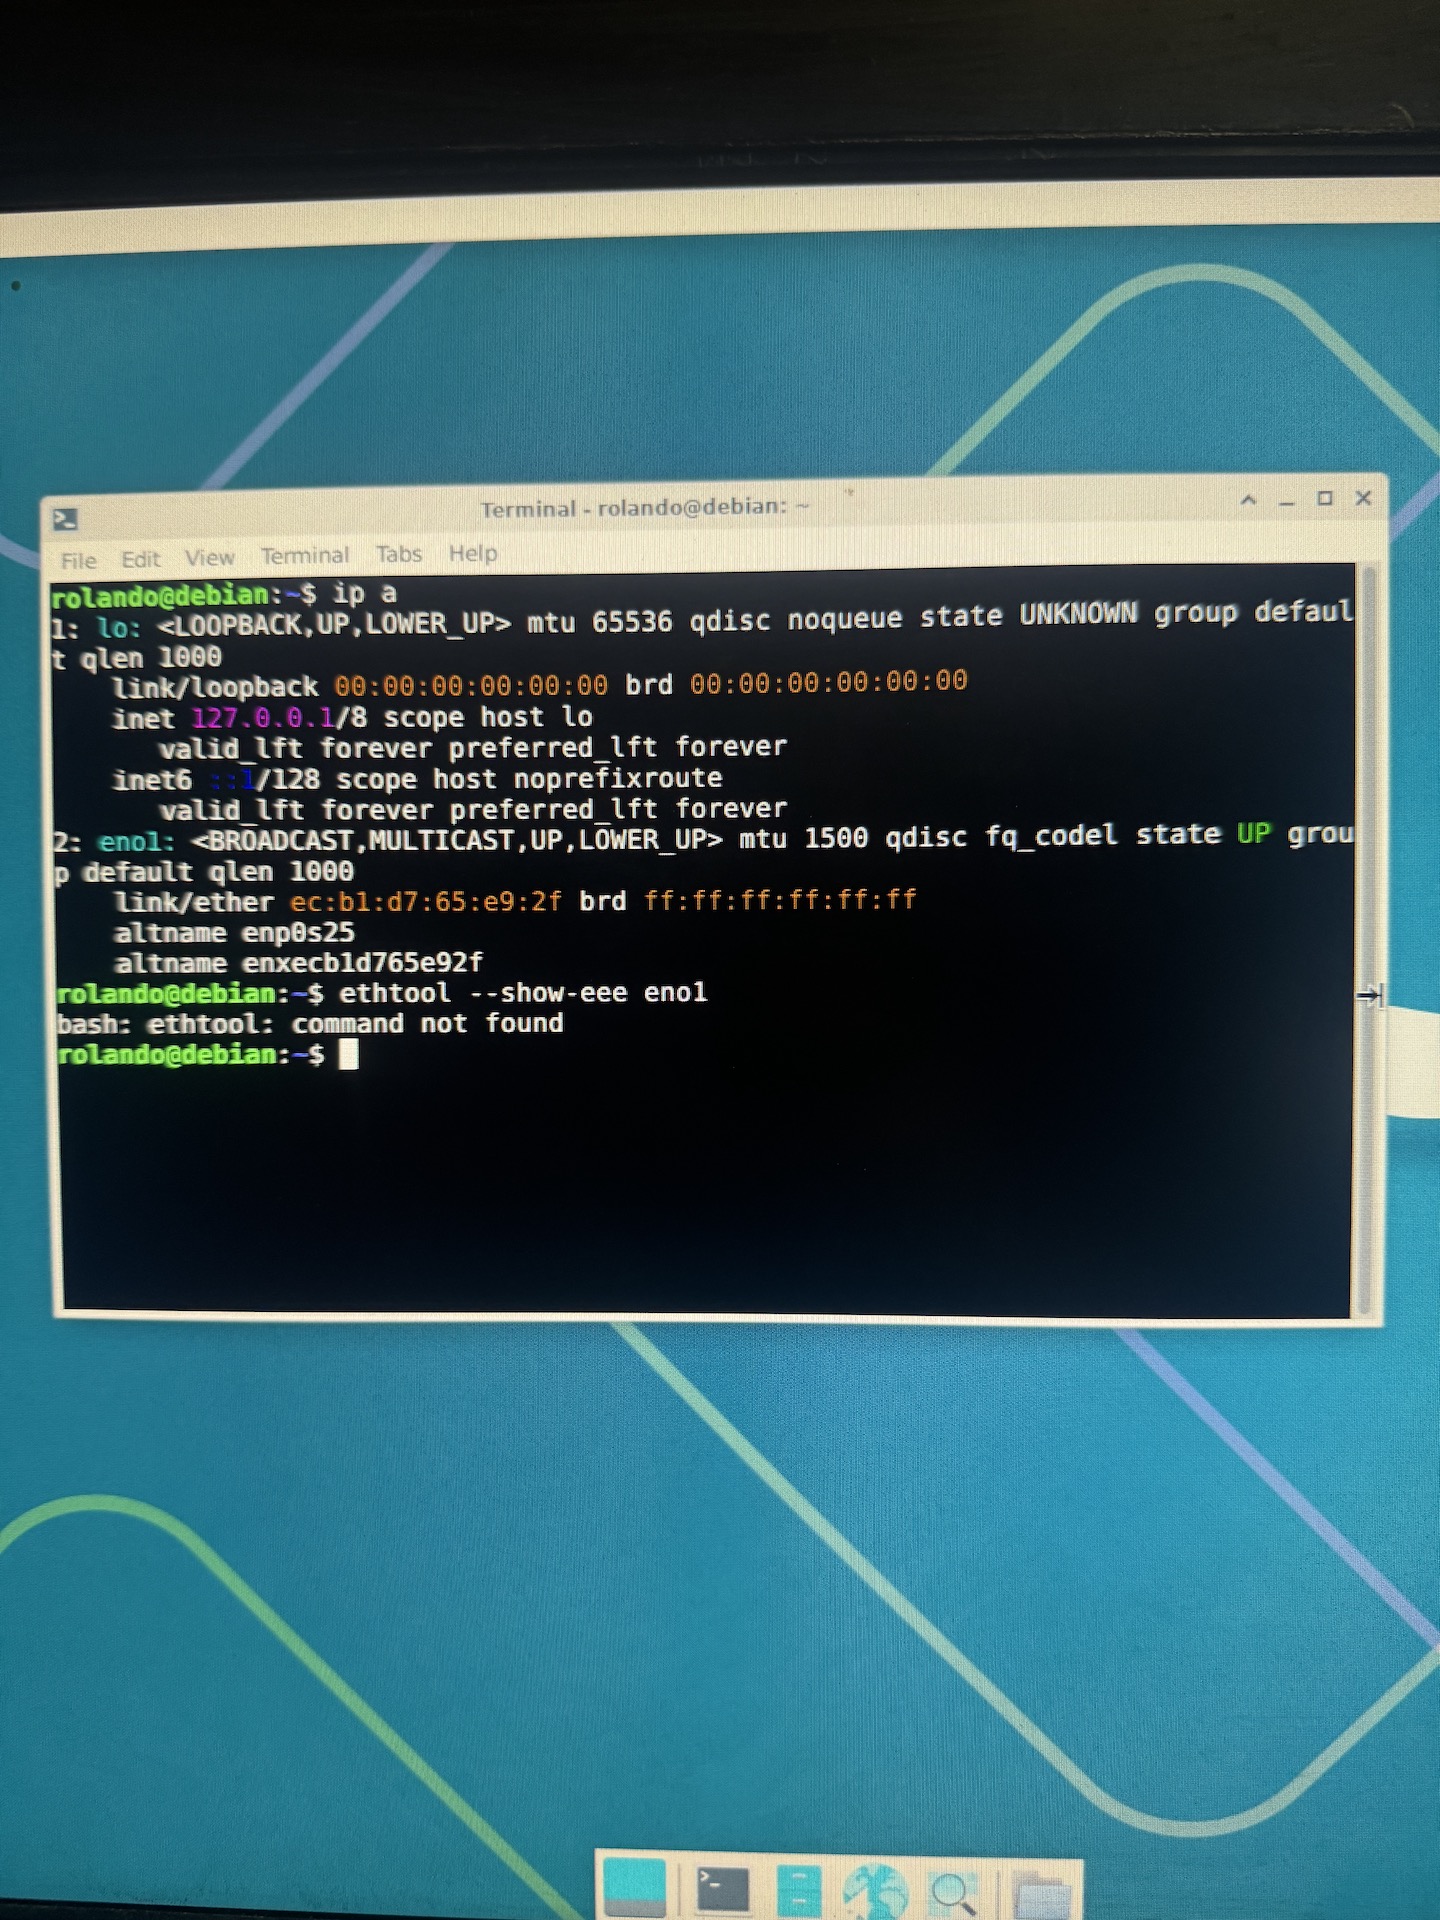
I get command not found for some reason 
  • tommylight
30 May 2026 01:18
Replied by tommylight on topic Hurco BMC 30 AP
We would need more info about what you want to do and what you already did.
  • HansU
29 May 2026 21:15
Replied by HansU on topic HalView
Really nice and very useful debug tool. Thanks for sharing! I think this should be shipped with linuxcnc. What do you think?

Only a little note to the selection behaviour - when I click on several components after each other, and when I hold down on the last one and drag, all the previous clicked components are in the selection and are moved together. I think it would be more intuitive to do that with Ctrl click.
  • HansU
29 May 2026 21:04
The BASE_PERIOD in the sim config is too low for that spindle speed so the sim_encoder component cannot calculate the speed correctly.
Setting a lower BASE_PERIOD in the gmoccapy.ini increases the possible maximum spindle speed ;-)
 
  • Todd Zuercher
29 May 2026 19:40
Replied by Todd Zuercher on topic Reset Custom M-codes on Machine Disable?
Yes with adding the conditional code from the manual seems to be working just the way I want it to.
Here is what I have in the on_abort.ngc file
Code:
o<on_abort> sub o100 if [#1 eq 5]     (machine on) o100 elseif [#1 eq 6]     (machine off)     M123 o100 elseif [#1 eq 7]     (estopped)     M123 o100 elseif [#1 eq 8]     (msg, abort pressed) o100 else     (DEBUG, error parameter is [#1]) o100 endif o<on_abort> endsub %
  • Todd Zuercher
29 May 2026 19:28 - 29 May 2026 19:34
Replied by Todd Zuercher on topic Reset Custom M-codes on Machine Disable?
I started playing with the on_abort.ngc and it might work. I need to play a little more. At this point it does a little more than I want it to. It will trigger it for F2 (what I want), but also triggers it when exiting a running milling file with the escape key (not what I want) and the machine does not enter machine off.

The machine state I'm dealing with is particular about how it is entered and exited. I can't simply turn it on or off without the machine moving, when the M-code is active, it can be turned off without issue when the machine is not enabled (in machine off). So I only want the on_abort sequence to cancel my M-code state when the machine is aborting to machine off. Aborting to a machine on state, such as when aborting a running g-code file, the M-code state needs to be left alone, and the operator will have to clear it themselves (else the machine will shutdown with following error alarms.)

In the remap instructions I read about making some things conditional. I'm going to try to play with that now.
  • Sascha H.
29 May 2026 18:44
Replied by Sascha H. on topic Jumping motion with XHC-WHB04B pendant
You can try this in your hal-file:
Code:
setp axis.x.jog-accel-fraction 0.4 setp axis.y.jog-accel-fraction 0.4 setp axis.z.jog-accel-fraction 0.4

This reduces the acceleration of the axes when moving with the pendant.
Displaying 3571 - 3585 out of 11908 results.
Time to create page: 0.196 seconds
Powered by Kunena Forum