Search Results (Searched for: )

  • rodw
28 Mar 2026 00:18
Replied by rodw on topic Jog troubles
why jog before homing? I always disable it.
  • PCW
27 Mar 2026 23:59
Can you do a

lspci -vv  | grep -A 10 2718 > pci.txt

and post pci,txt here?

 
  • grandixximo
27 Mar 2026 23:15
Replied by grandixximo on topic LinuxCNC S-Curve Accelerations
I tried to follow your instructions, and it works ok for me.
I suspect it maybe something with the custom tool table which is missing from default, could you share that?
  • grandixximo
27 Mar 2026 22:45
Replied by grandixximo on topic Probe Active before non-probe move
Linuxcnc Version?
IMO this is a bug in the source code, i have this error disabled in the codebase I use for work
  • scsmith1451
27 Mar 2026 21:48
Replied by scsmith1451 on topic Configuring and Homing dual Y Axes
I understand your concern now. I only use probing to find my Z height. X/Y is handled by a crosshair laser. Once centered on the starting position of the cut, a button attached to g-code computes the actual position by applying offsets for both X and Y to the current location of the laser. Offsets are stored in my INI file and can be changed if needed without touching the code.
  • andrax
27 Mar 2026 21:20
Replied by andrax on topic Ethercat Setup help needed for beginner
Er, no. It’s not that simple; LinuxCNC isn’t plug-and-play. If you don’t have any prior knowledge, you should put the A6 aside for now and start with simple stepper motors. You’ll first need to learn how the system works and what each component does. With EtherCAT, you’re moving beyond the hobbyist level, and even professionals sometimes find it frustrating.
  • tommylight
27 Mar 2026 20:10
Replied by tommylight on topic Review Request for Arc Volt Sensor Schematic

In what way do you see 2x50k as a better way than 1x100k?

 
Keeps the high power stuff more isolated in case of wire break/short, making it much safer.
I always put those 3 resistors on the plasma source of in a box behind it.
  • grossm5000
27 Mar 2026 20:07
Replied by grossm5000 on topic Differential encoder hard crashes the PC MESA7i77
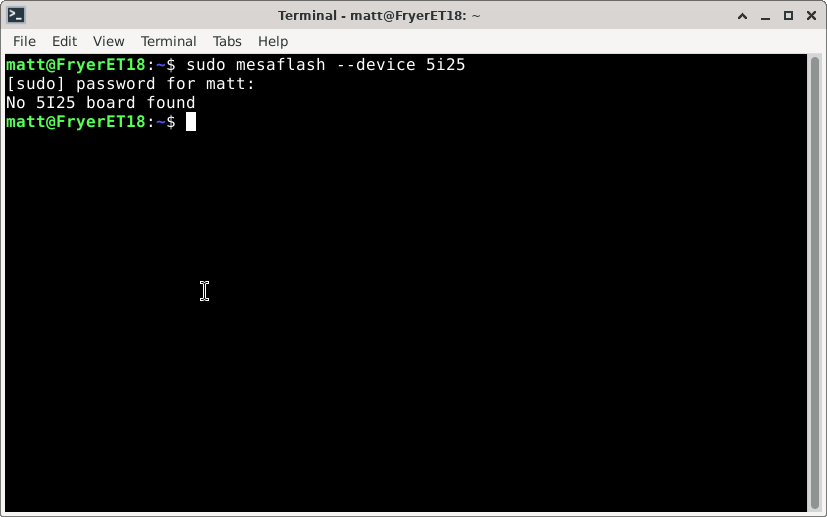
yes, mesaflash still says 5i25 not found

 
  • PCW
27 Mar 2026 19:49
Did you try running mesaflash after running LinuxCNC?
 
  • djdelorie
27 Mar 2026 19:34
Replied by djdelorie on topic Configuring and Homing dual Y Axes
The problem isn't the 50ms, it's that during that time the machine is *moving*. I.e. where you home depends on the bouncing of the sensor, which means it's unpredictable, which means every other position is also unreliable.
If you "hit" on the first contact, instead of waiting for the physics to settle down, you get a more predictable "moment" when the machine is in the known state.
You'd think it wouldn't matter, but I've seen my probe go measurably past the right spot before it "hits", and my probing routines actually probe in both directions (G38.2 then G38.4, and take the average) to try to eliminate this overshoot.
With a "first hit" debouncer, you could set the debounce time to 3 seconds and still get the right value.
  • scsmith1451
27 Mar 2026 19:21
Replied by scsmith1451 on topic Configuring and Homing dual Y Axes
I don't see a problem with de-bouncing a signal when homing since the purpose of homing is to put the machine in a known state and stop before doing anything else. If that takes an extra 50ms to insure the starting position of all axes, it is a non sequitur since the result is the machine is stopped. It might be a minor issues when hitting a limit switch while machining, but I'd rather error on fact rather than bounce.

Just my two cents worth.
  • JT
27 Mar 2026 18:48
Flex GUI has nothing to do with halui.

This is my code for my BP external Estop.
Code:
# E-Stop Chain loadrt estop_latch count=1 addf estop-latch.0 servo-thread # E-Stop Loop net estop-loopin iocontrol.0.user-enable-out => estop-latch.0.ok-in net estop-loopout estop-latch.0.ok-out => iocontrol.0.emc-enable-in # E-Stop Reset net estop-reset iocontrol.0.user-request-enable net estop-reset => estop-latch.0.reset net remote-estop0 estop-latch.0.fault-in <= hm2_5i25.0.7i77.0.0.input-06-not

JT
  • JT
27 Mar 2026 18:43
Replied by JT on topic Flex GUI Keyboard Jogging
And you can now set the jog increments using the keyboard.
gnipsel.com/linuxcnc/flexgui/ini.html#keyboard-shortcuts

JT
  • JT
27 Mar 2026 18:42
Replied by JT on topic Jog troubles
That's a LinuxCNC issue the joints are numbered 0-8 for xyzabcuvw so c is joint 5.

Maybe a jog axis button would work. I'd have to test.

JT
  • rodw
27 Mar 2026 18:39
Replied by rodw on topic Updating Old GladeVCP Files?
This may not help but this 2017 post shows how to update a gmoccappy screen handler from gcode which sounds like your problem 1
forum.linuxcnc.org/plasma-laser/32691-settings-from-g-code-file
Here different values are set using an analog input which is decoded and used to modify screen elements. eg 900 and 999 change screen settings.
Displaying 5401 - 5415 out of 11812 results.
Time to create page: 0.161 seconds
Powered by Kunena Forum