4th Axis Build

More
10 years 2 weeks ago #81634 by Lcvette
Replied by Lcvette on topic 4th Axis Build
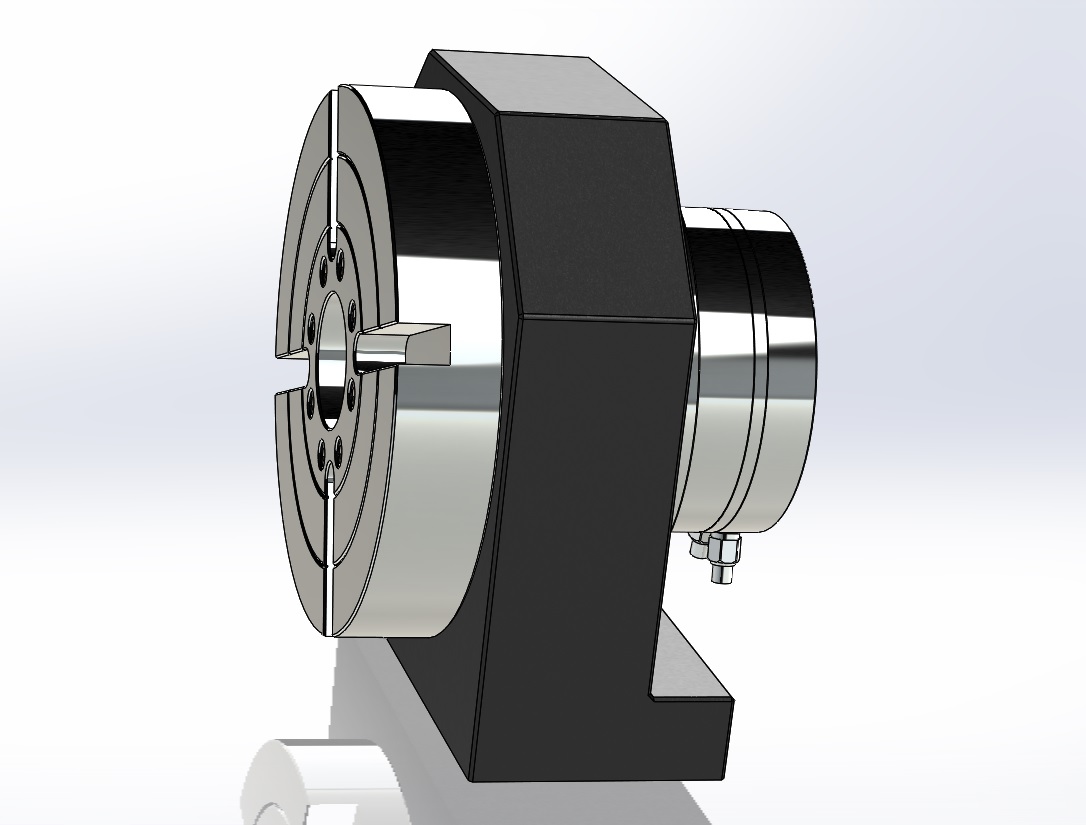
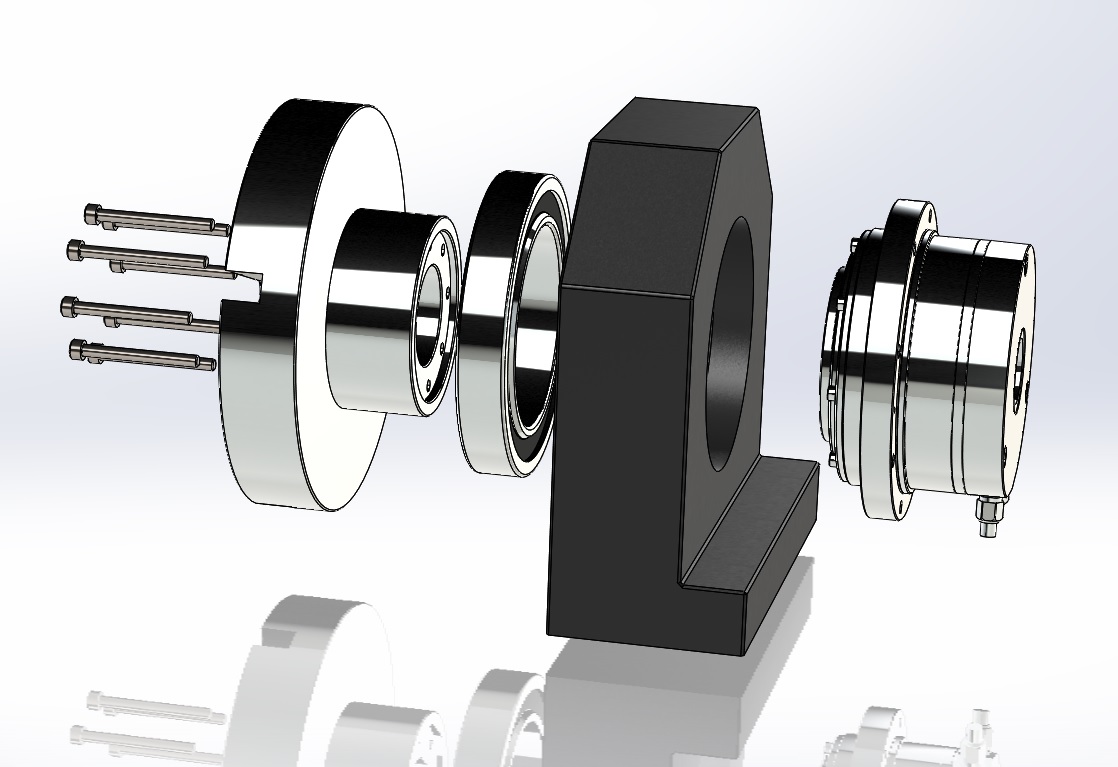
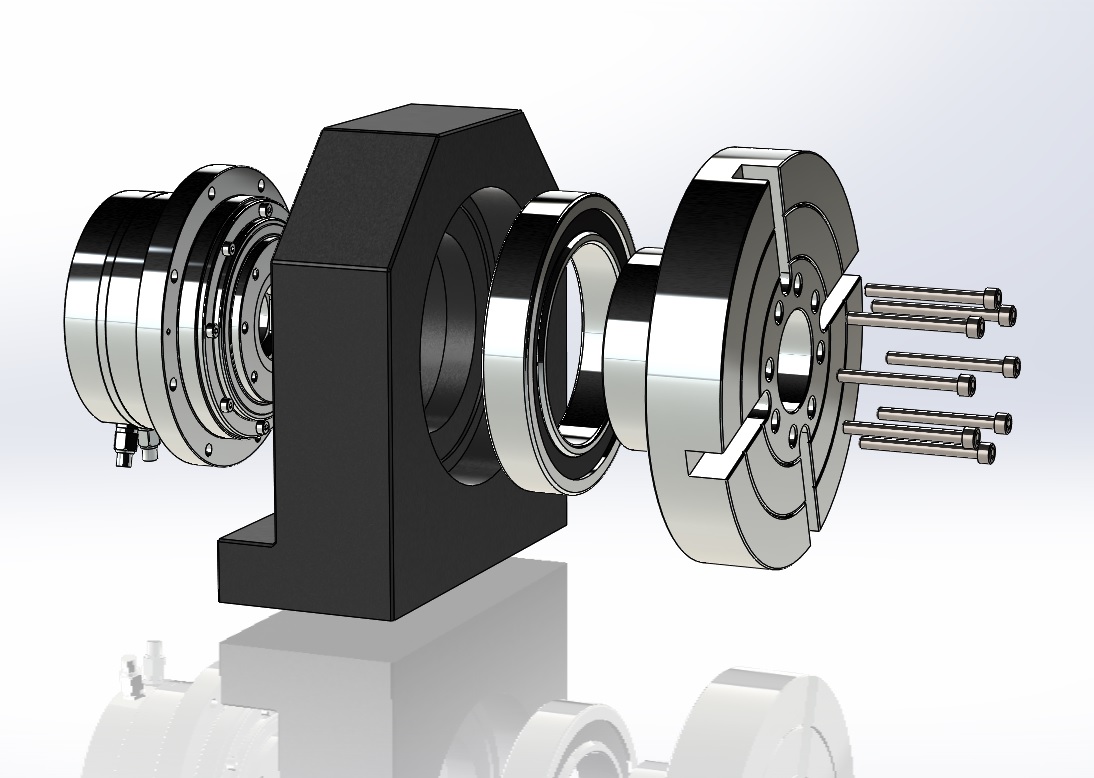
I whipped this up, it is an 8" Rotary Table design, it isn't finished, but it works out to be 4 parts, the harmonic drive, the frame casting, the table and a cylindrical roller bearing for table support right at the frame edge behind the table. the thrust load will be on the cross roller bearing in the harmonic drive to keep things compact. depth from the table face to the back face of the harmonic drive is 6" pretty good. from the table face to the back edge of the frame casting is 5". I think this is about as simple of a design as you could have, the table would be made from a solid casting and machined to finish. it bolts directly to the harmonic drive so no slop can be introduced into the system. the only backlash in the system will be what the harmonic drive has in it which should be very very low. I think this is a winnder! Thoughts?


Please Log in or Create an account to join the conversation.
More
10 years 2 weeks ago #81636 by andypugh
Replied by andypugh on topic 4th Axis Build
What is your lathe spindle nose? (assuming you have a lathe). If it is camlock then you could consider adjusting the T-slot number to fit camlock pins between them. (you could have a loose spigot for centering).

Consider tool access to the work for small diameters too.

You might want to copy your milling machine spindle taper in the centre of the rotary. You can then hold smaller work in collets easily.

This is a real-world 4th-axis job I had to use an overlength piece of stock to get the tool to the work. Often you are likely to end up with a small spigot on the stock held in a collet just to get tool access to the end.

Please Log in or Create an account to join the conversation.
More
10 years 2 weeks ago #81646 by Lcvette
Replied by Lcvette on topic 4th Axis Build
Andy,

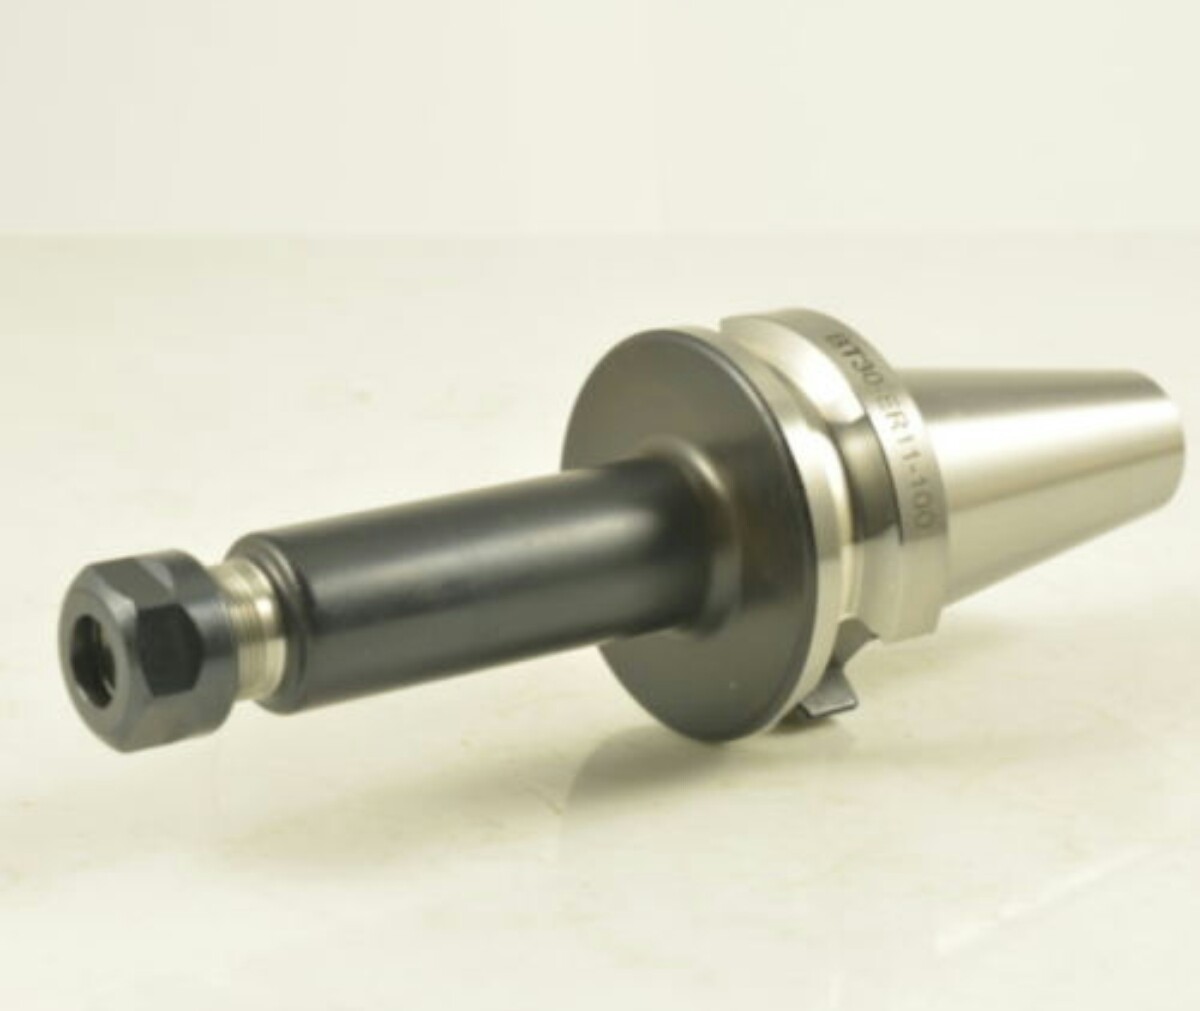
For my application the rotary is going to be used for a 6" X 6" X 24" tombstone for production work. So I won't have to get down toward the center for this setup. But those are excellent points. My mill spindle is a BT30. My lathe is a bolt on stud and nut (benchtop machine). I do like the idea of a camlock setup, just have no experience with them. Will have to take a look at it and do some research. I will also play around with mounting a 5C chuck on the table face send see how the spindle clearance looks, that may give some extension to get a tool down near the center without interference from the spindle nose. Worst case scenario i soul grab some BT30 extended ER11 tool holders for small diameter 4th axis work.

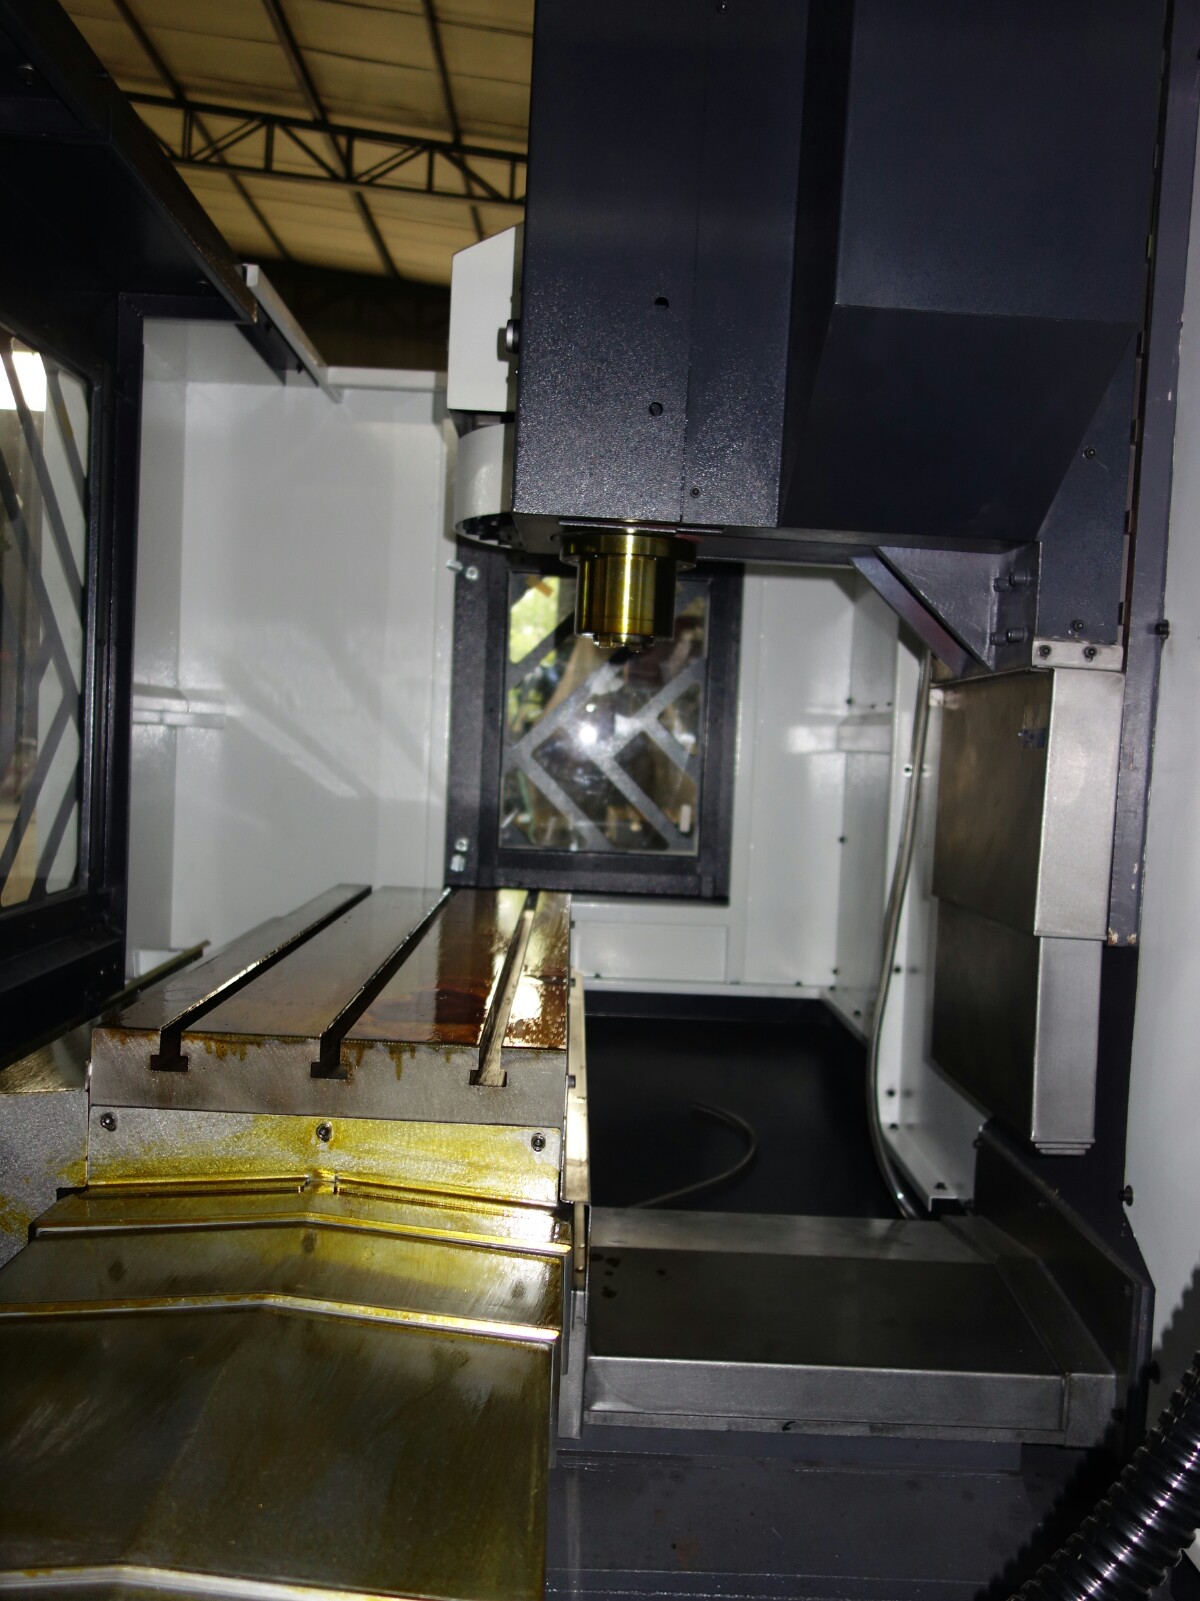
Here are some pictures of the mill spindle and the tool holders I was thinking about to solve being able to f do both fine small work and larger tombstone production work:


Please Log in or Create an account to join the conversation.
More
10 years 1 week ago #82008 by gmouer
Replied by gmouer on topic 4th Axis Build
Dale, I have a couple questions.

Did you check the runout obtained using the tapered bearings? Any chance you have the number of those bearings?

I will be building one nearly identical to what you did. I have the harmonic drive and am gathering the remaining parts.

Thanks,
George

Please Log in or Create an account to join the conversation.
More
10 years 1 week ago - 10 years 1 week ago #82018 by Dale Lusby
Replied by Dale Lusby on topic 4th Axis Build
I used the same bearings out of the front axle of my truck so they would be easy to source and fairly inexpensive (mine are from Autozone). They are Timken brand but I know the duralast ones have the same part number. The bearing is number 387a and the race is 382a. The seal is 415960. These are from my 1986 Ford F-350 4x4 w/6.9 diesel in case you are at a parts house and want them to look it up. The front axle is a Dana 60 and this is the larger inner bearing of the two. It has a 2.25" bore. The two sets set me back about $50.

The runout I don't have the numbers but I know it is quite low. I believe the main reason tapered rollers are not used for spindles is due to the power loss from friction as it is higher than angular contact bearings. I will try to get some numbers and a video of it in use soon.
Last edit: 10 years 1 week ago by Dale Lusby.

Please Log in or Create an account to join the conversation.

More
10 years 1 week ago - 10 years 1 week ago #82021 by gmouer
Replied by gmouer on topic 4th Axis Build
They do use tapered rollers routinely in the import lathes, and they work very well. I looked up specs at timken and it seems their standard grade bearings from zero to 10 inch bore are spec'd at 2 thou max runout. That sounds like a lot to me, thats why I asked. They do have precision grades but of course the price gets prohibitive. Of course, 2 thou runout on a car wheel wouldn't be a problem.

It would be very interesting to see what your runout measures.
Last edit: 10 years 1 week ago by gmouer.

Please Log in or Create an account to join the conversation.

Time to create page: 0.174 seconds
Powered by Kunena Forum