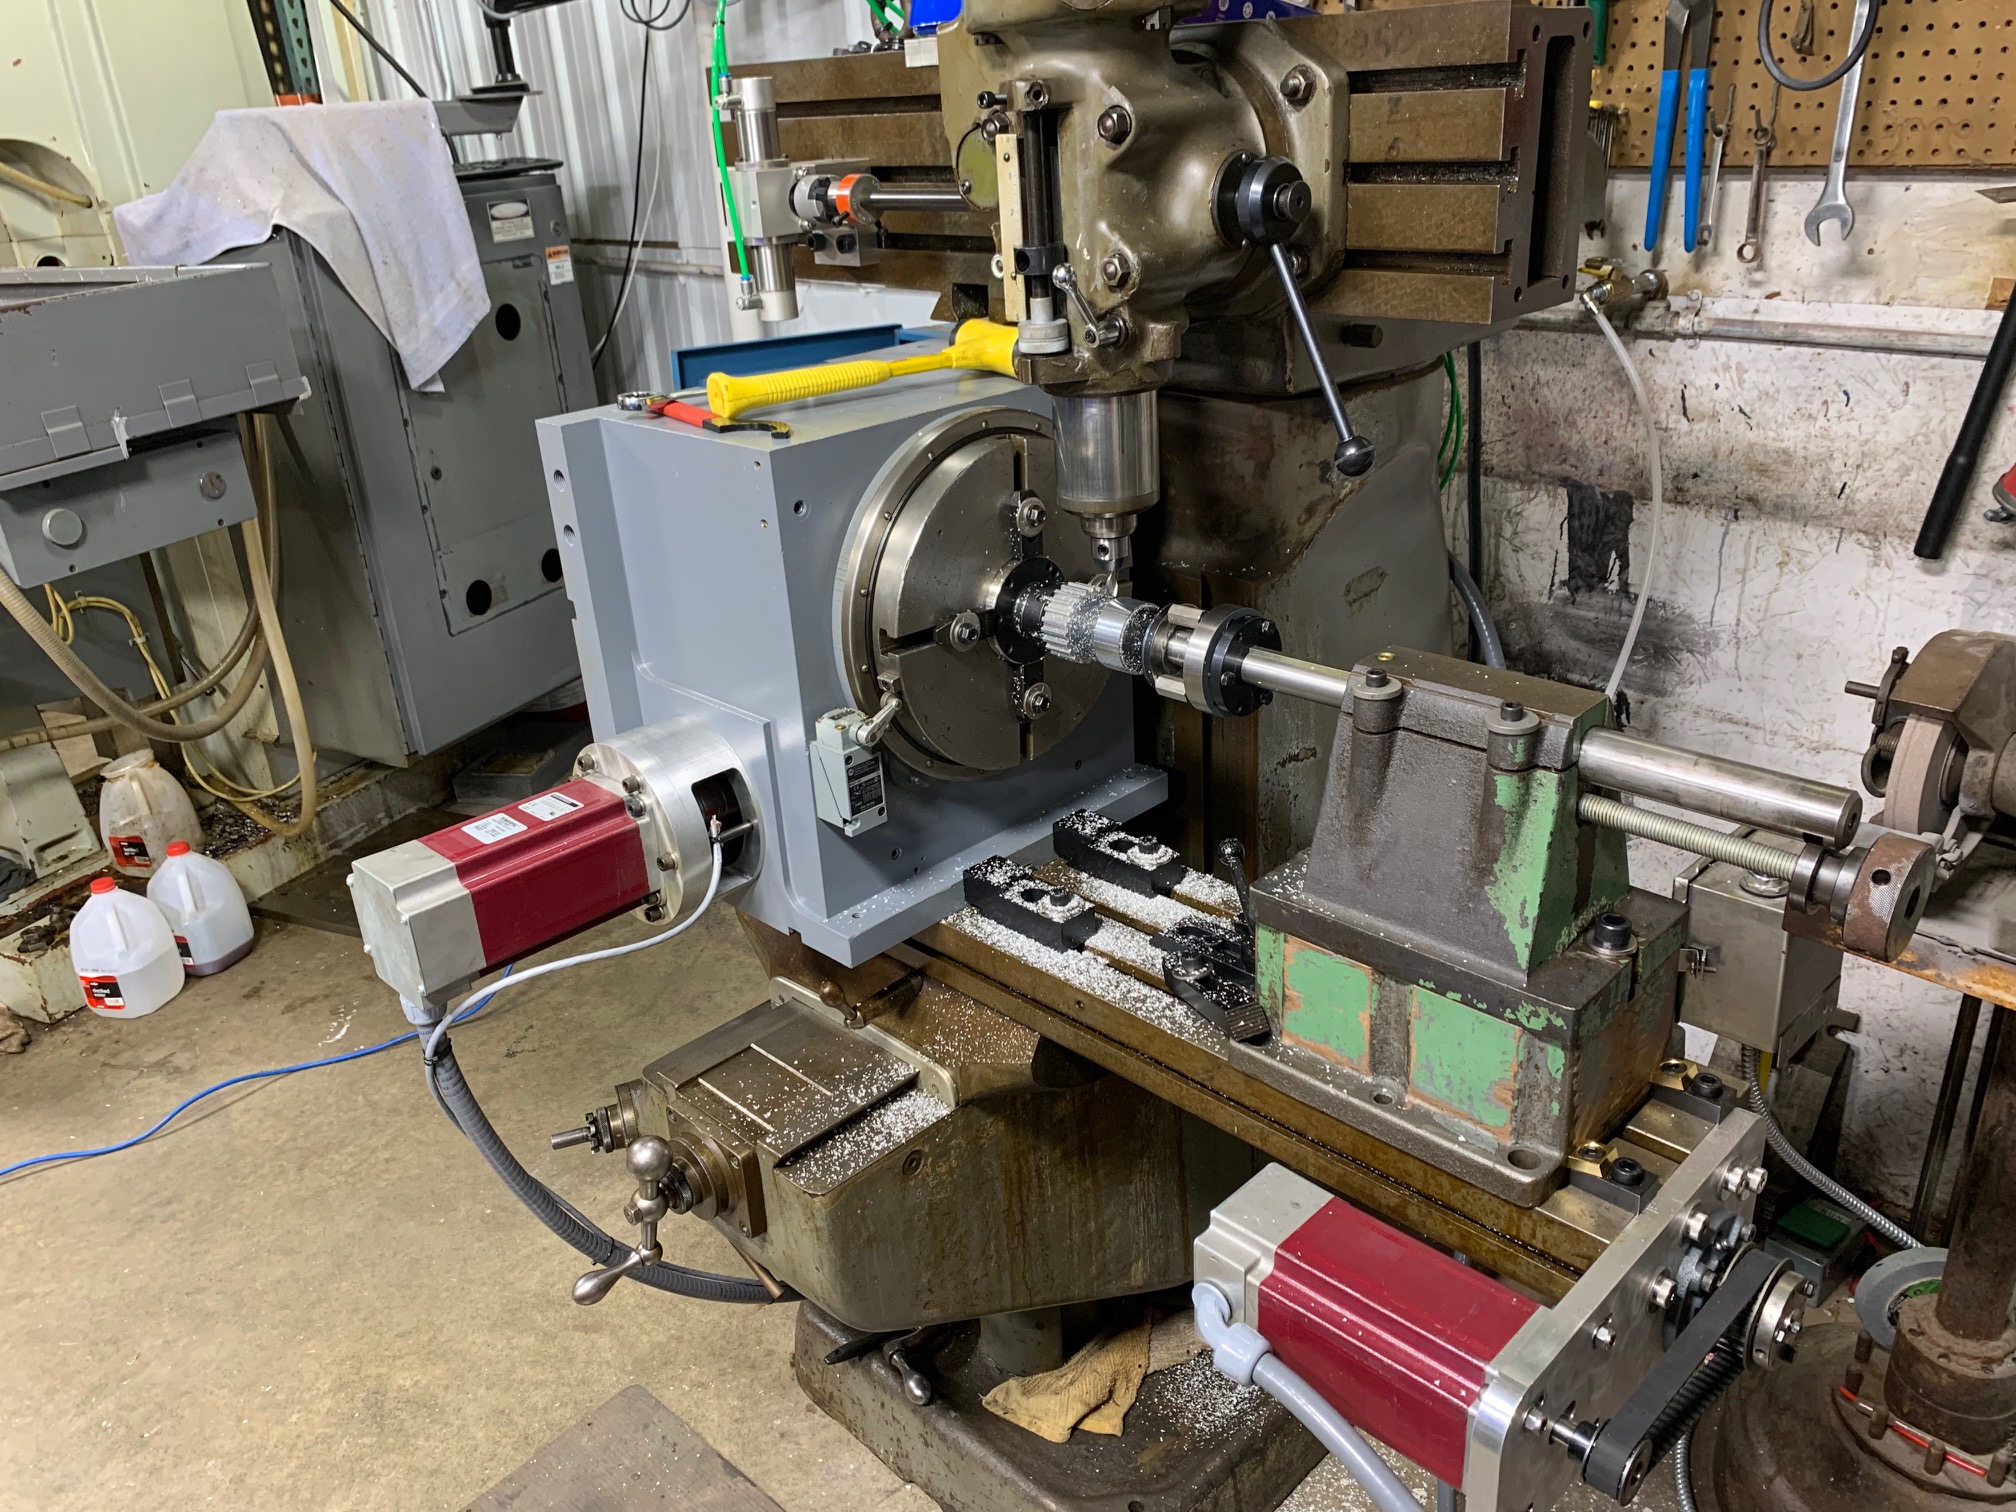
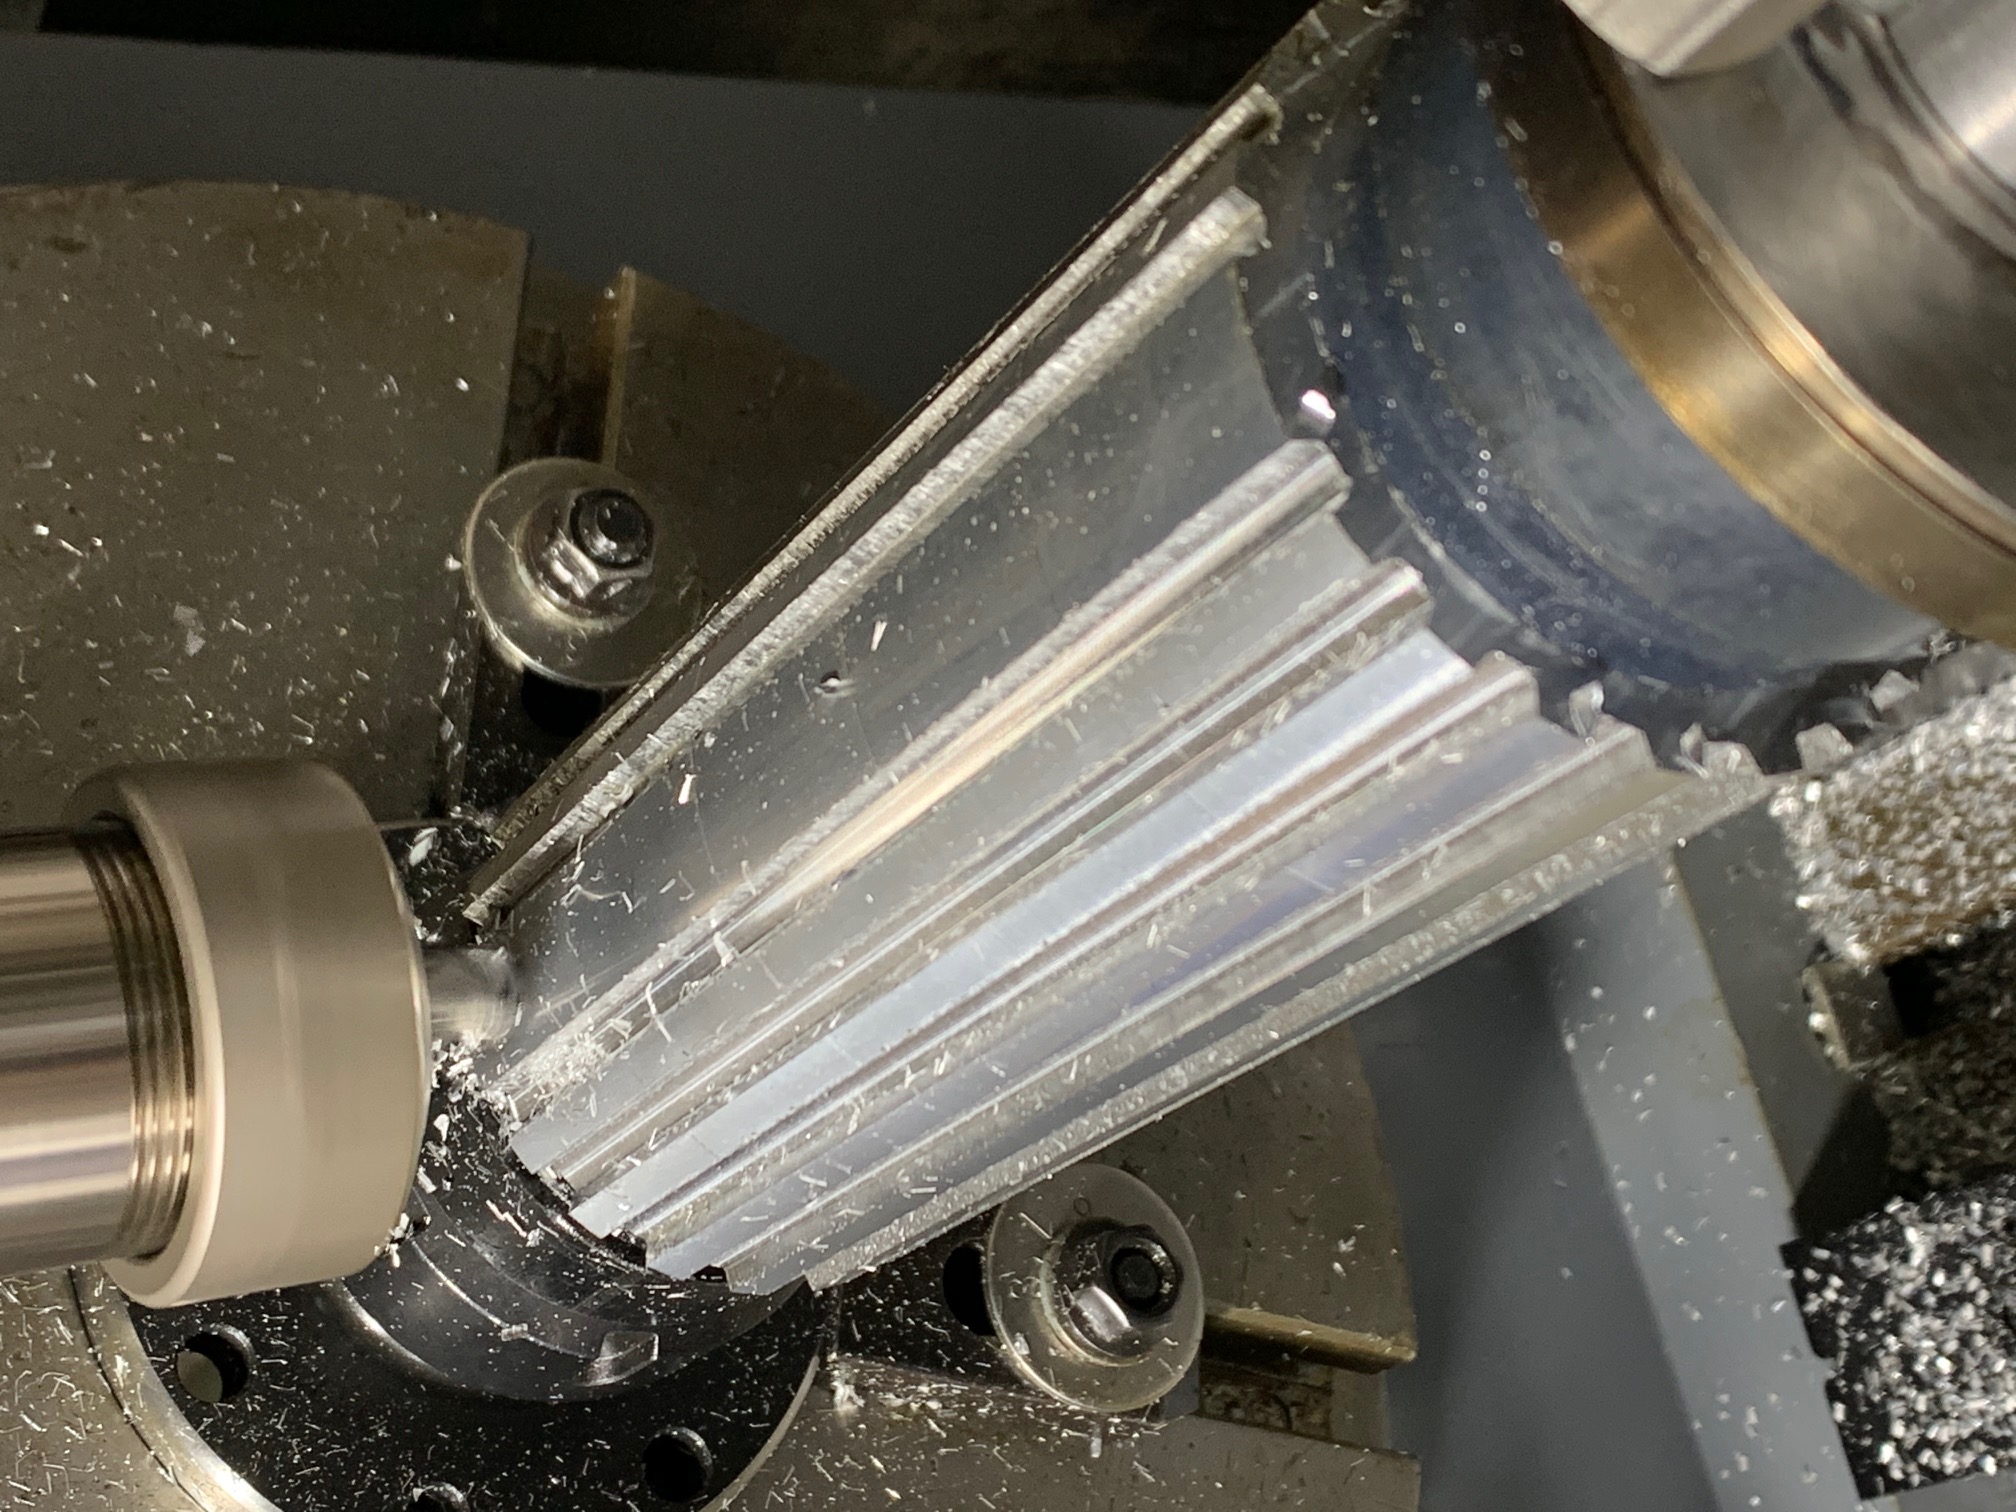
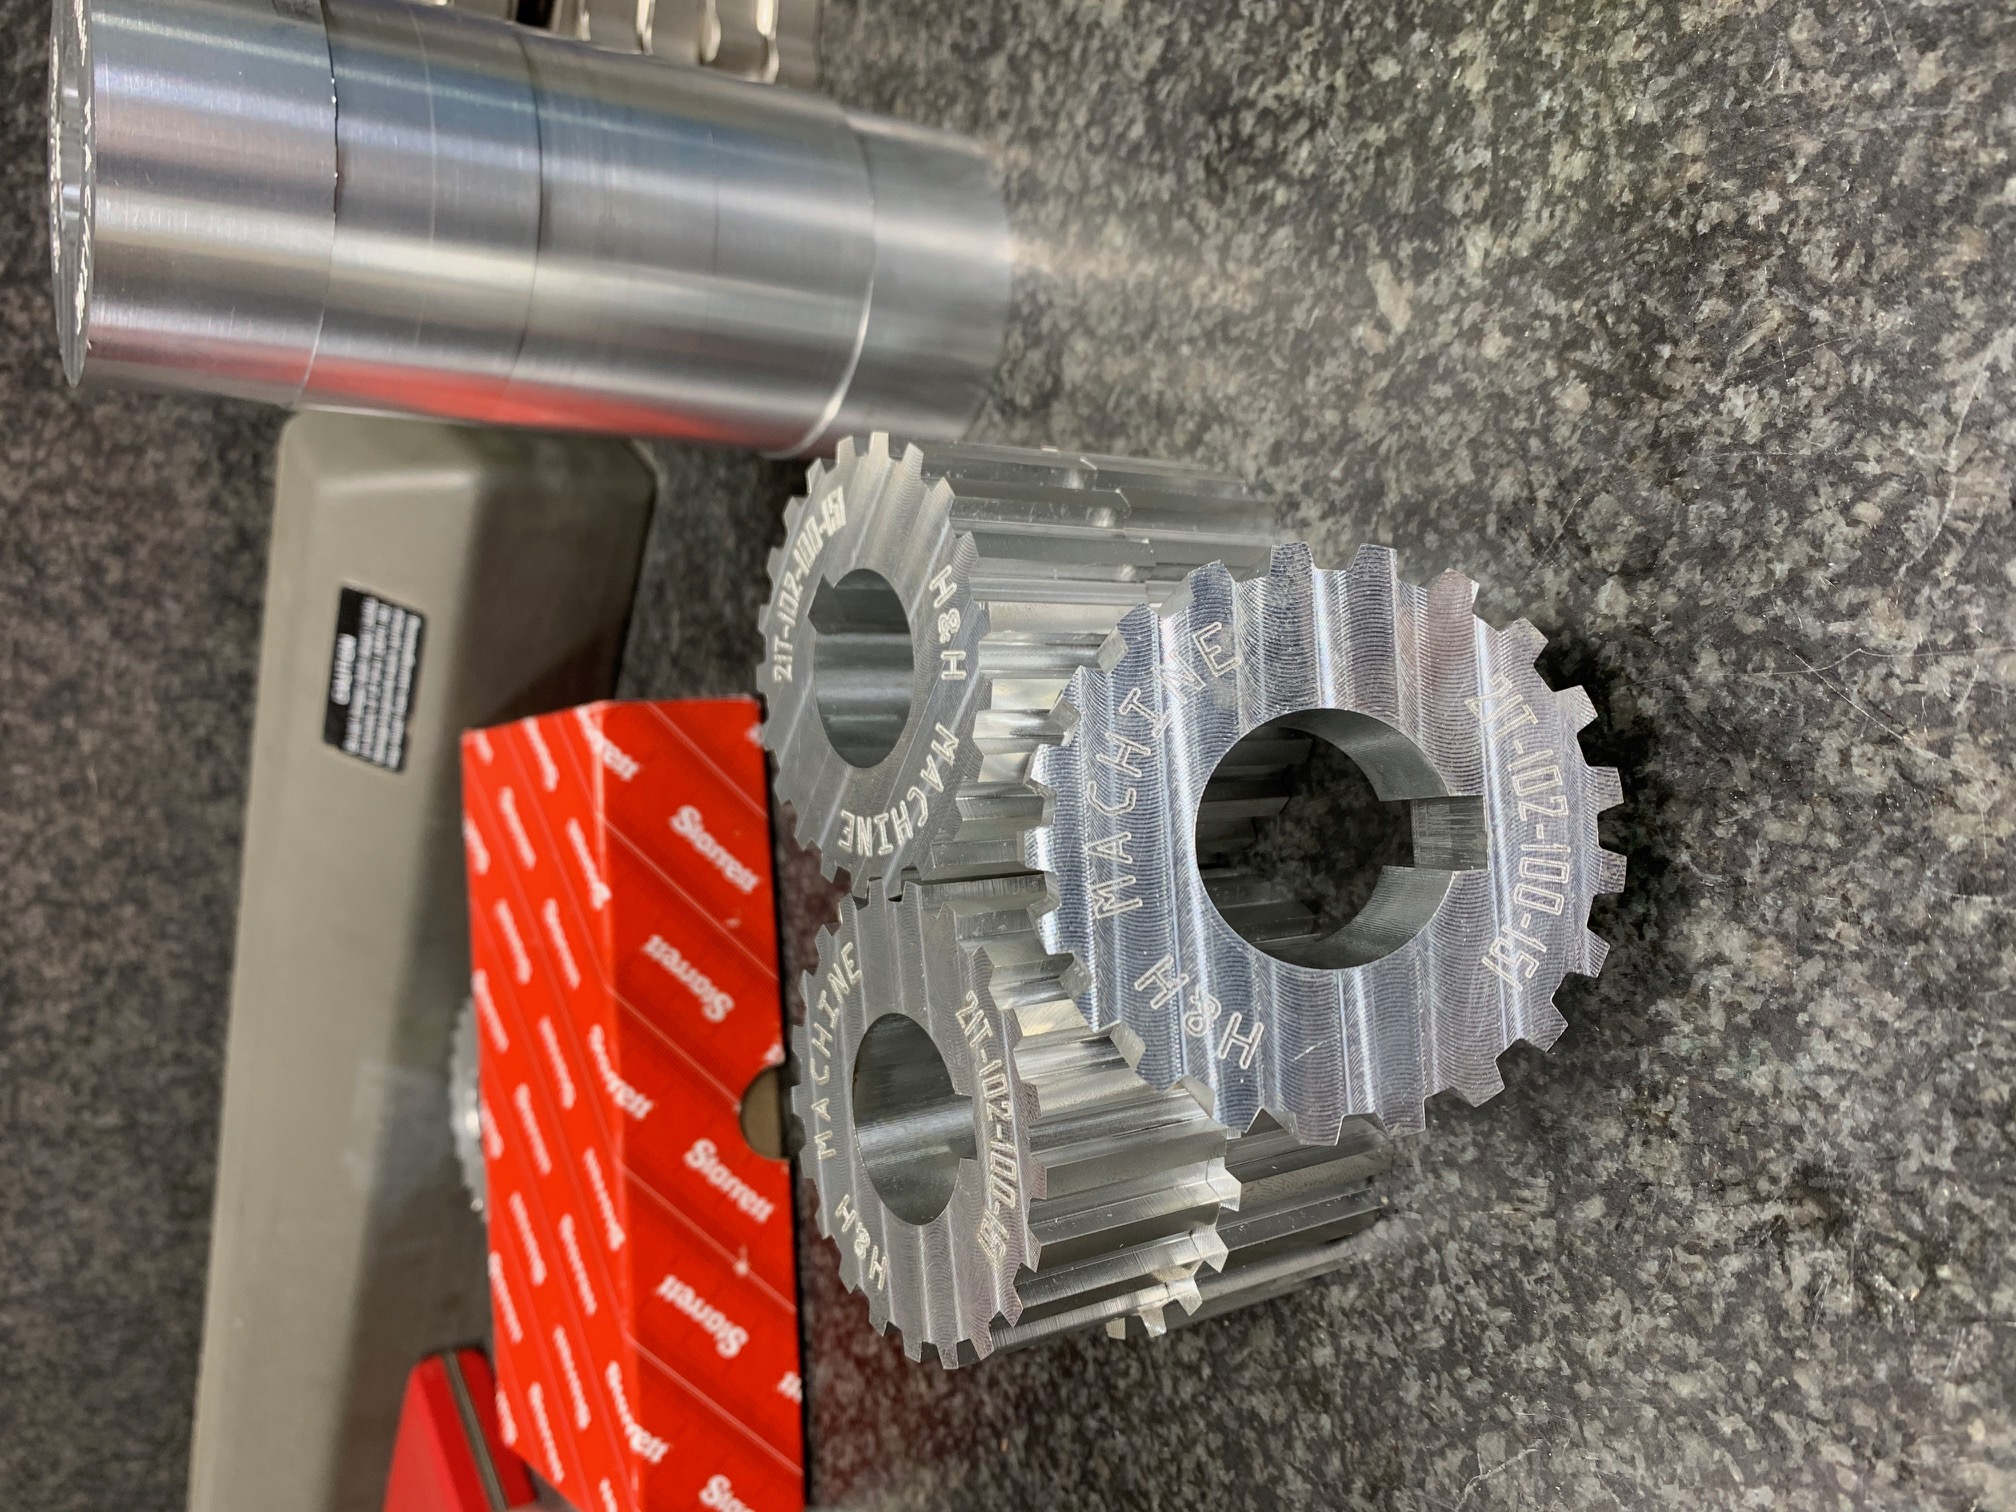
I needed to cut a set of gears for my lathe conversion. While I was sorting out what I had and what I needed to get to make that happen, I came across a job cutting some toothed pulleys. The OEM price left a lot of room for profit so I got this machine done as fast as I could to get the work.
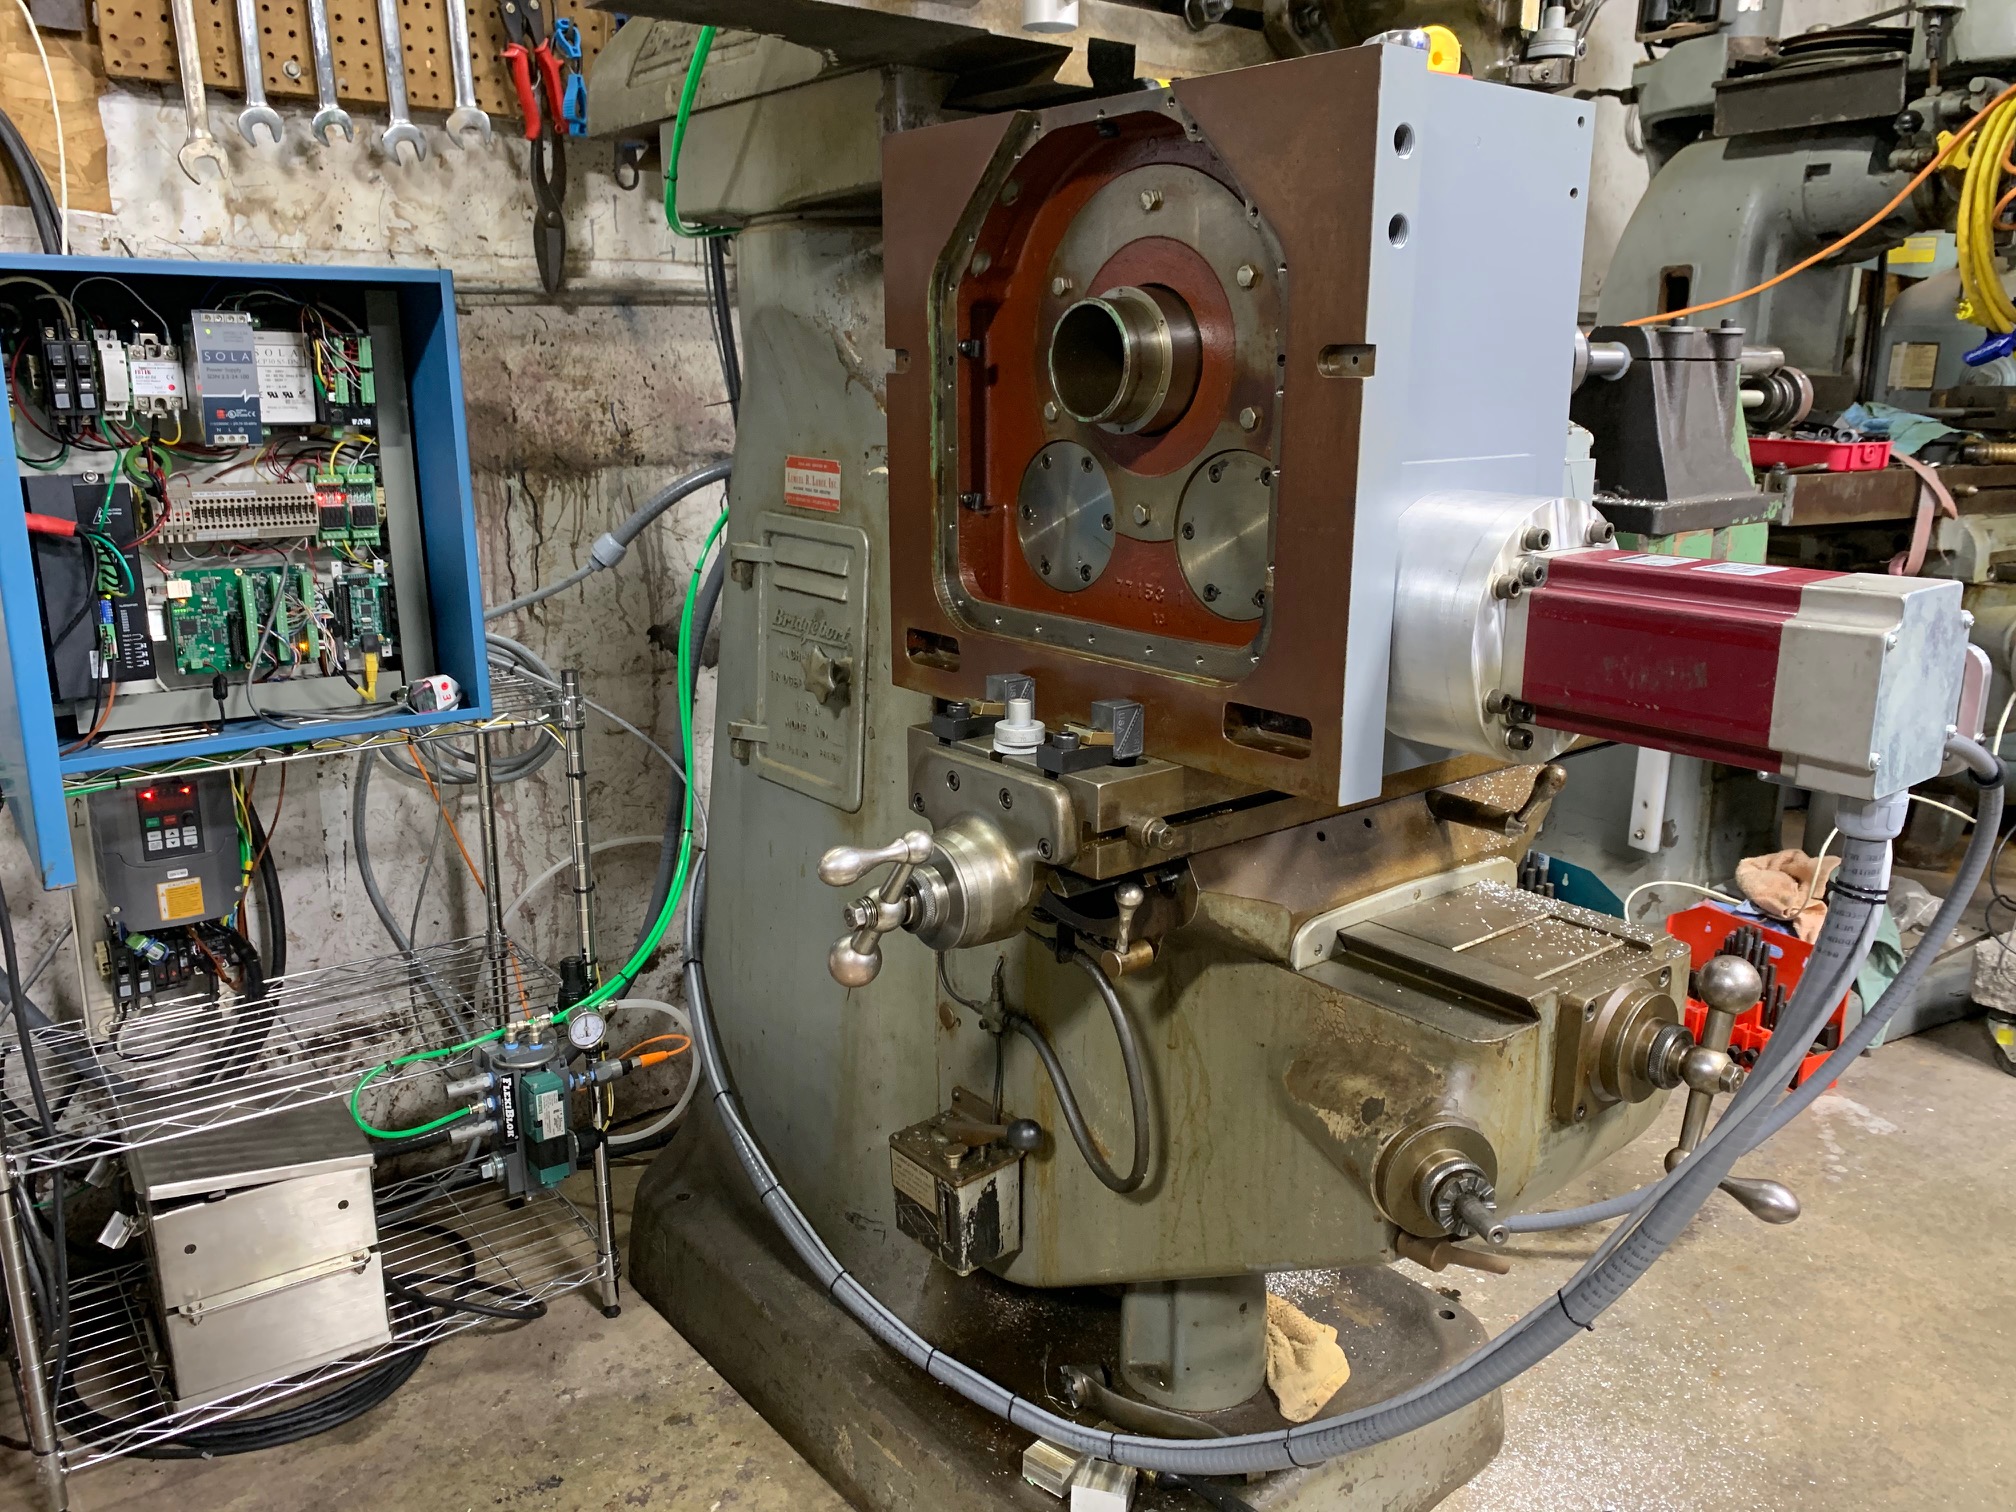
The mill is a Bridgeport "True Trace". It was an eBay find with all the hydraulic drive components missing(along with random things stolen off it over the years). But it was lightly used, the J2 spindle was in good working order and happened to be a good platform for what I wanted to do. The Y axis never looked to have a drive on it and was a blessing to be as is. I added the stepper to the X axis after tying up the missing drive components for the lead screw.
The rotary indexer is another eBay find. It was in fair shape but had been sitting for a couple decades. The drive for it was a massive 156v DC servo and the feedback was an "Inductosyn" similar to a resolver. The circuitry for that fed into a Bendix brand card with no numbers on it. Someone did adjust one of the pots on the board in December of 1983. He left a nice note. Although I haven't given up on the Inductosyn I embedded a rotary encoder inside the stepper mount.
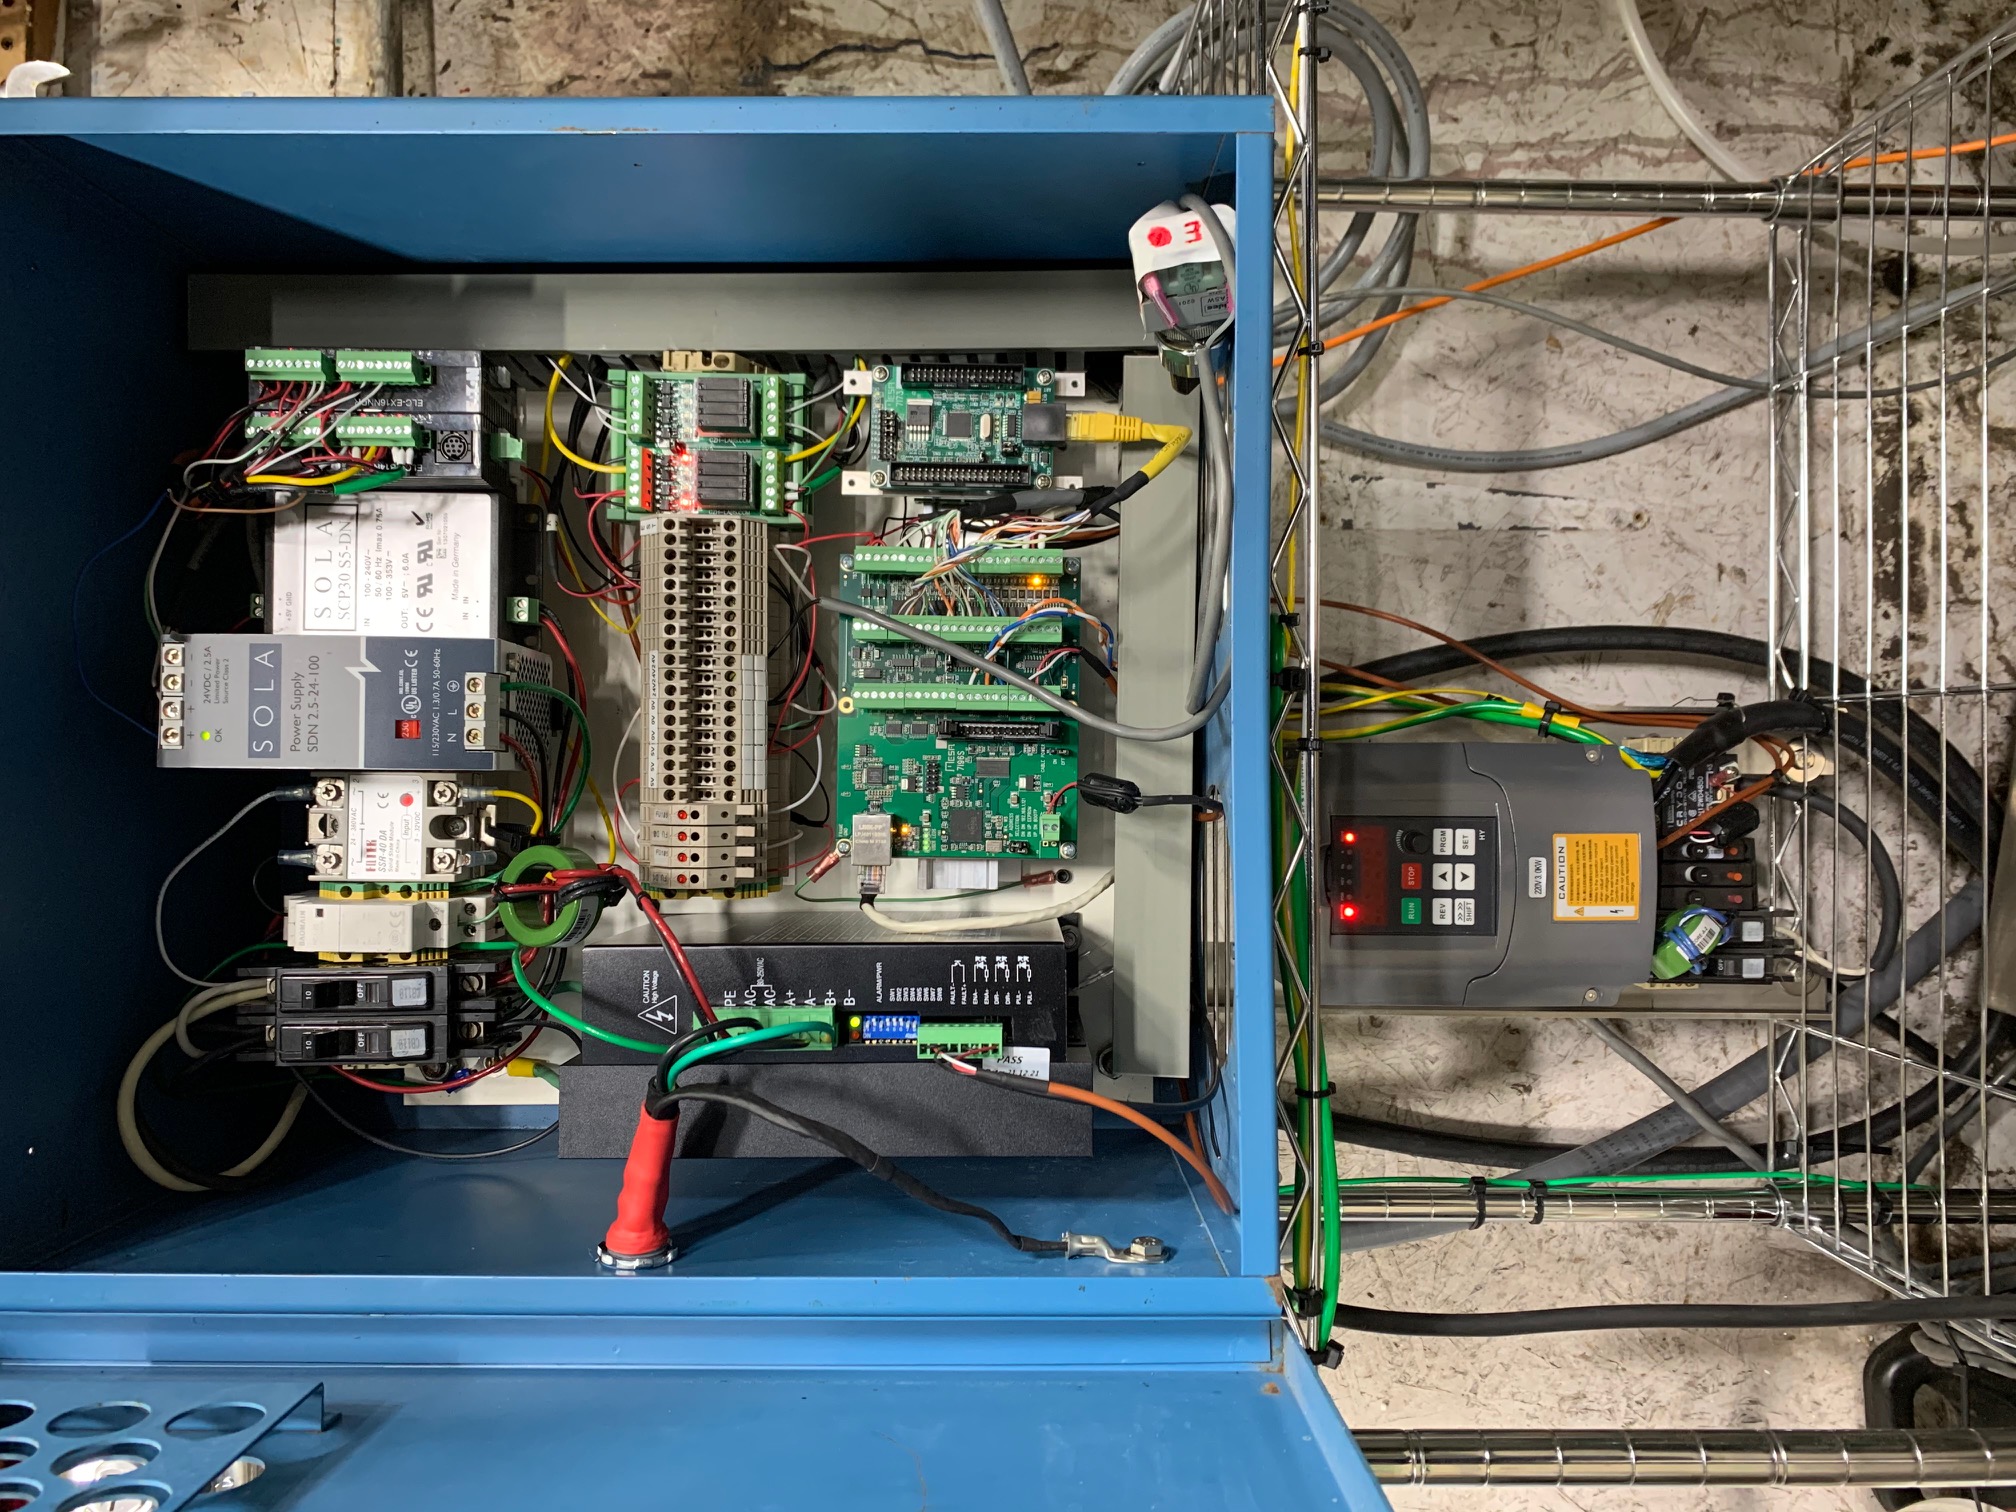
The controls are an Eaton PLC and a Mesa 7i96s. I have a VFD running constant 60hz to the spindle to accommodate my 240v single phase primary. I have a 7i73 I need to build a op panel for but I'm still using the keyboard until I get time for it. Its just riding the rail for now. Besides that and adding some options to the interface I'm about done with this one.
Id like to thank this great community again for being my primary resource for knowledge. This is the 3rd NC machine I have running parts in my shop on LinuxCNC.