Two Axis NC Indexer

More
4 years 2 months ago #249620 by hoffb77
Replied by hoffb77 on topic Two Axis NC Indexer

Do like.

Your tailstock and outboard support is...interesting.  I see a taperlock bushing, and maybe a bearing carrier, but the rest is hard to figure out.


I use a QD bushing with a sheave I turned down for a back stop. I tapped the sheave with 1/2-13 and use those nuts to press and hold the work tight. The tailstock is tapered and seated inside there with a bushing. The dead center shaft is 1-1/2" and my pulley bore is 28mm. So I turned down the end of the work holding shaft and made a bushing to bring it together. I made up two work shafts and have the next set turned to diameter as the Knob Hobber cuts teeth.
The following user(s) said Thank You: spumco

Please Log in or Create an account to join the conversation.
More
4 years 2 months ago #250017 by andypugh
Replied by andypugh on topic Two Axis NC Indexer

When I find an 8" Ill swap it out.. I'm building a machine to cut tapered accelerating pitch feed screws out of cored poly bar stock and I need another rotary A axis to do that. I'm on the hunt for an 8" if you see a deal.

Maybe keep an eye out on eBay for an FHA-25B harmonic drive.
bodgesoc.blogspot.com/2017/05/harmonic.html

FYI....... the OEM price on those pulleys is $400+ US.


What is that tooth profile? It looks unusual.

I picked up a proper hob for T5 pulleys some time ago:


The following user(s) said Thank You: tommylight, hoffb77

Please Log in or Create an account to join the conversation.
More
4 years 2 months ago #250071 by hoffb77
Replied by hoffb77 on topic Two Axis NC Indexer
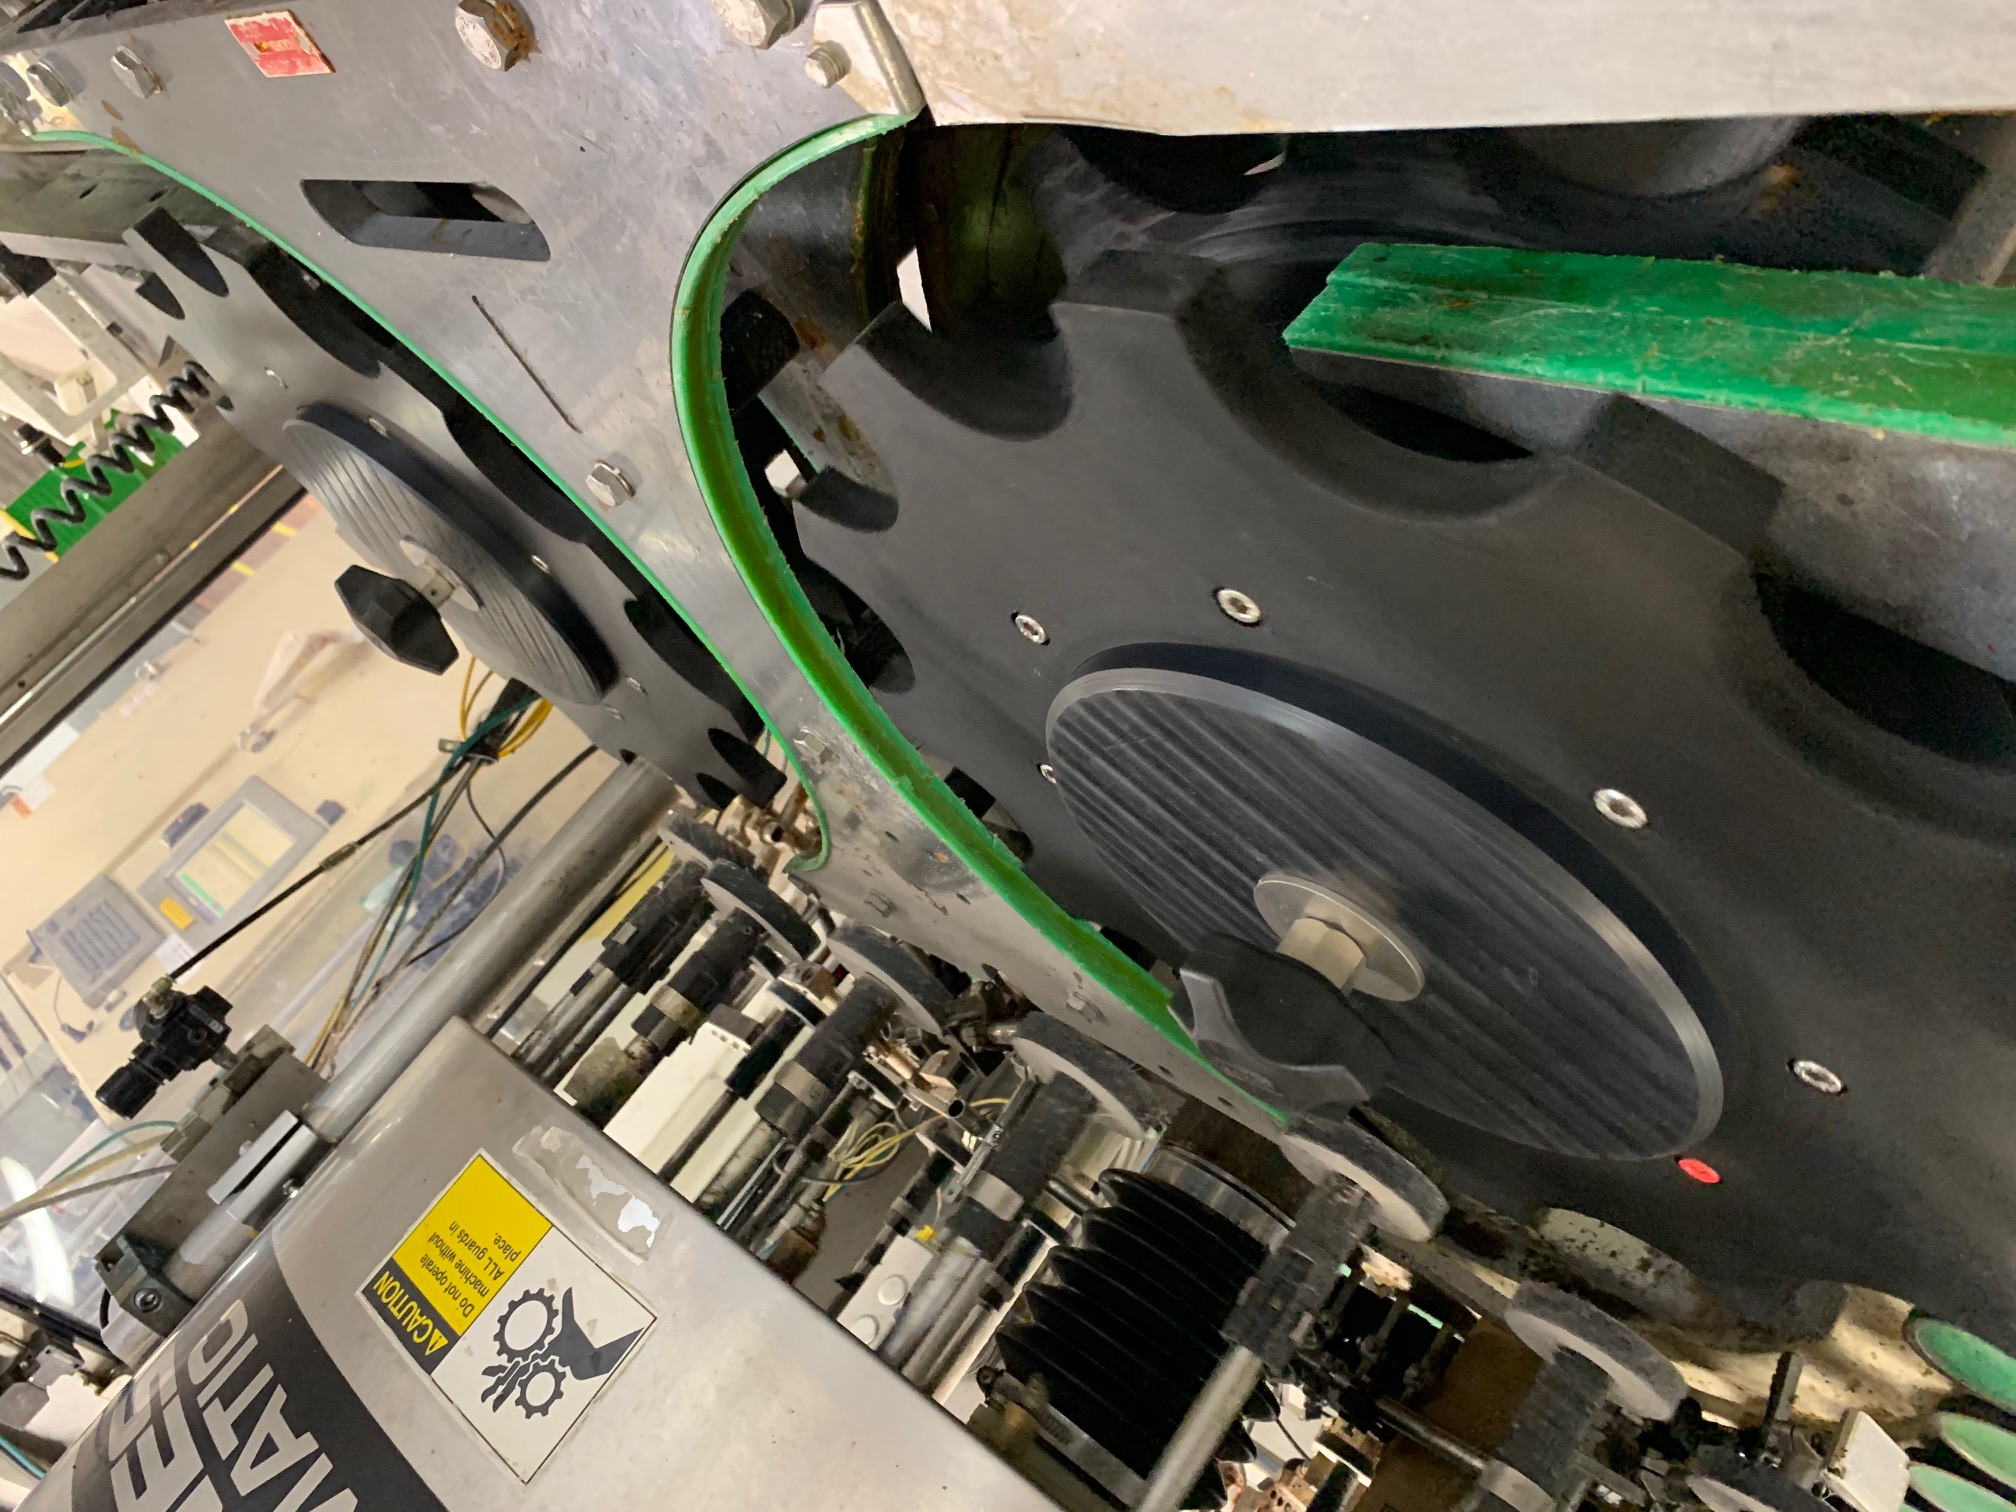
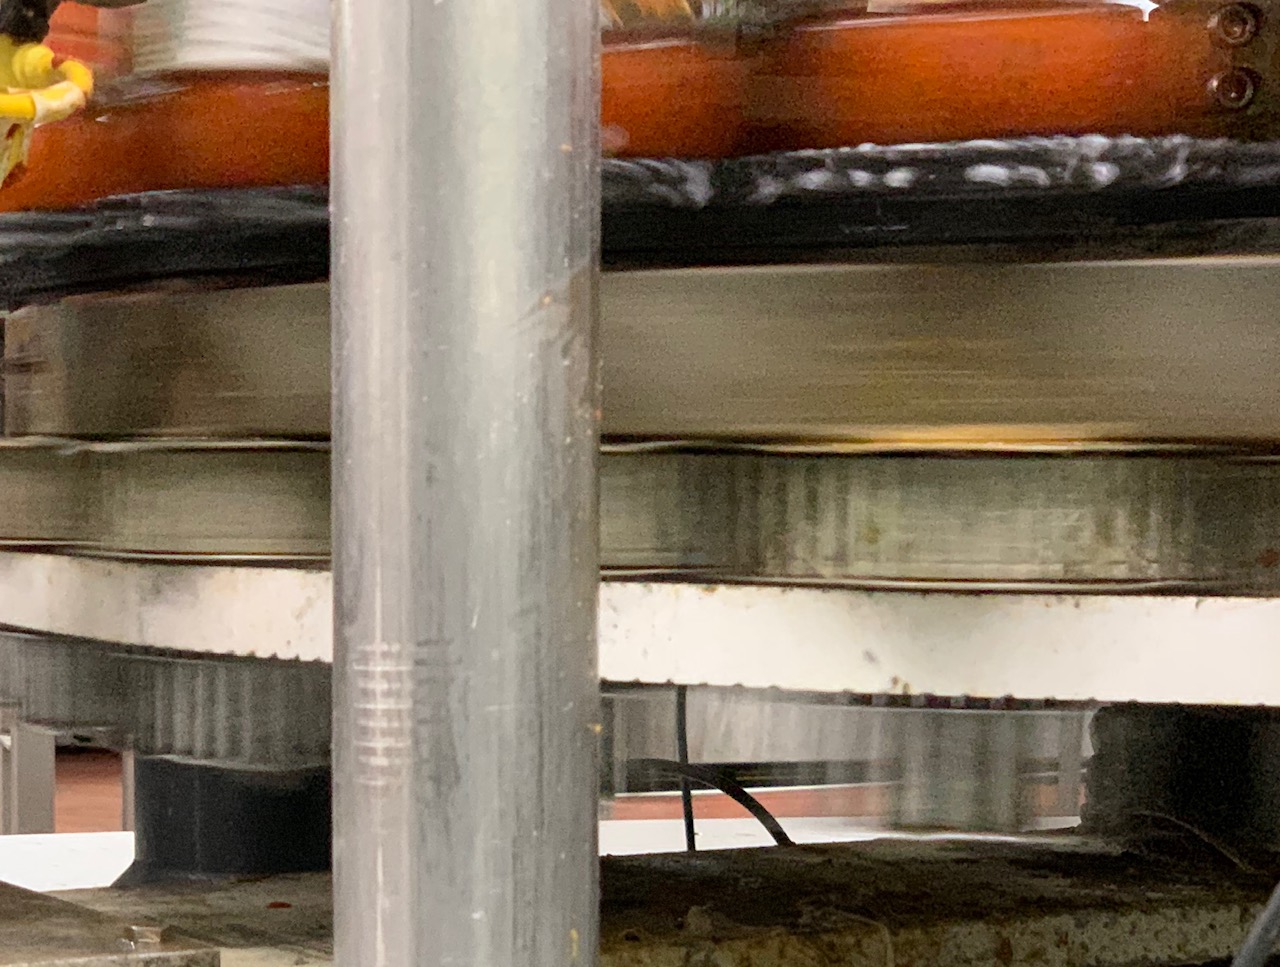
The belt we use is T-10 but the teeth are cut deeper. I would imagine the OEM did this to make room for debris, especially glue. They are for a german labeler. The 21T pulley is for a small condensed can of soup. A 26T is used on a 24oz jar of sauce. The bigger diameter bottles, jars and cans use a taller pulley. It times the jar to the machine during the application cycle. It passes the sensor as the pulley engages the belt. It does one rev and the can gets hit with glue dots/swirls. The next rev rolls those dots into the label magazine. It does another rev to guide the label on and then the label code is read by a cognex scanner and its picture is taken. After all that it comes off the belt and discharges the machine.

The closest I have seen to one of these is some idler pulleys. Im thinking if run the taller pulleys I will need to program the dimensional changes or get another tool shaped. Luckily I have plenty of different sizes of these OEM to make sure my geometry is right.

I will look at a harmonic drive and the proper equipment for the long term. Id like to get a hold of all the part work locally for these machines. Its tough to get parts quickly out of Germany and its only becoming worse. All of these parts were run on LinuxCNC driven machines......

 
There are three pulleys stacked there. 22T 26T 33T. The belt get moved to match the production run. for 14oz 24oz 48oz.

 
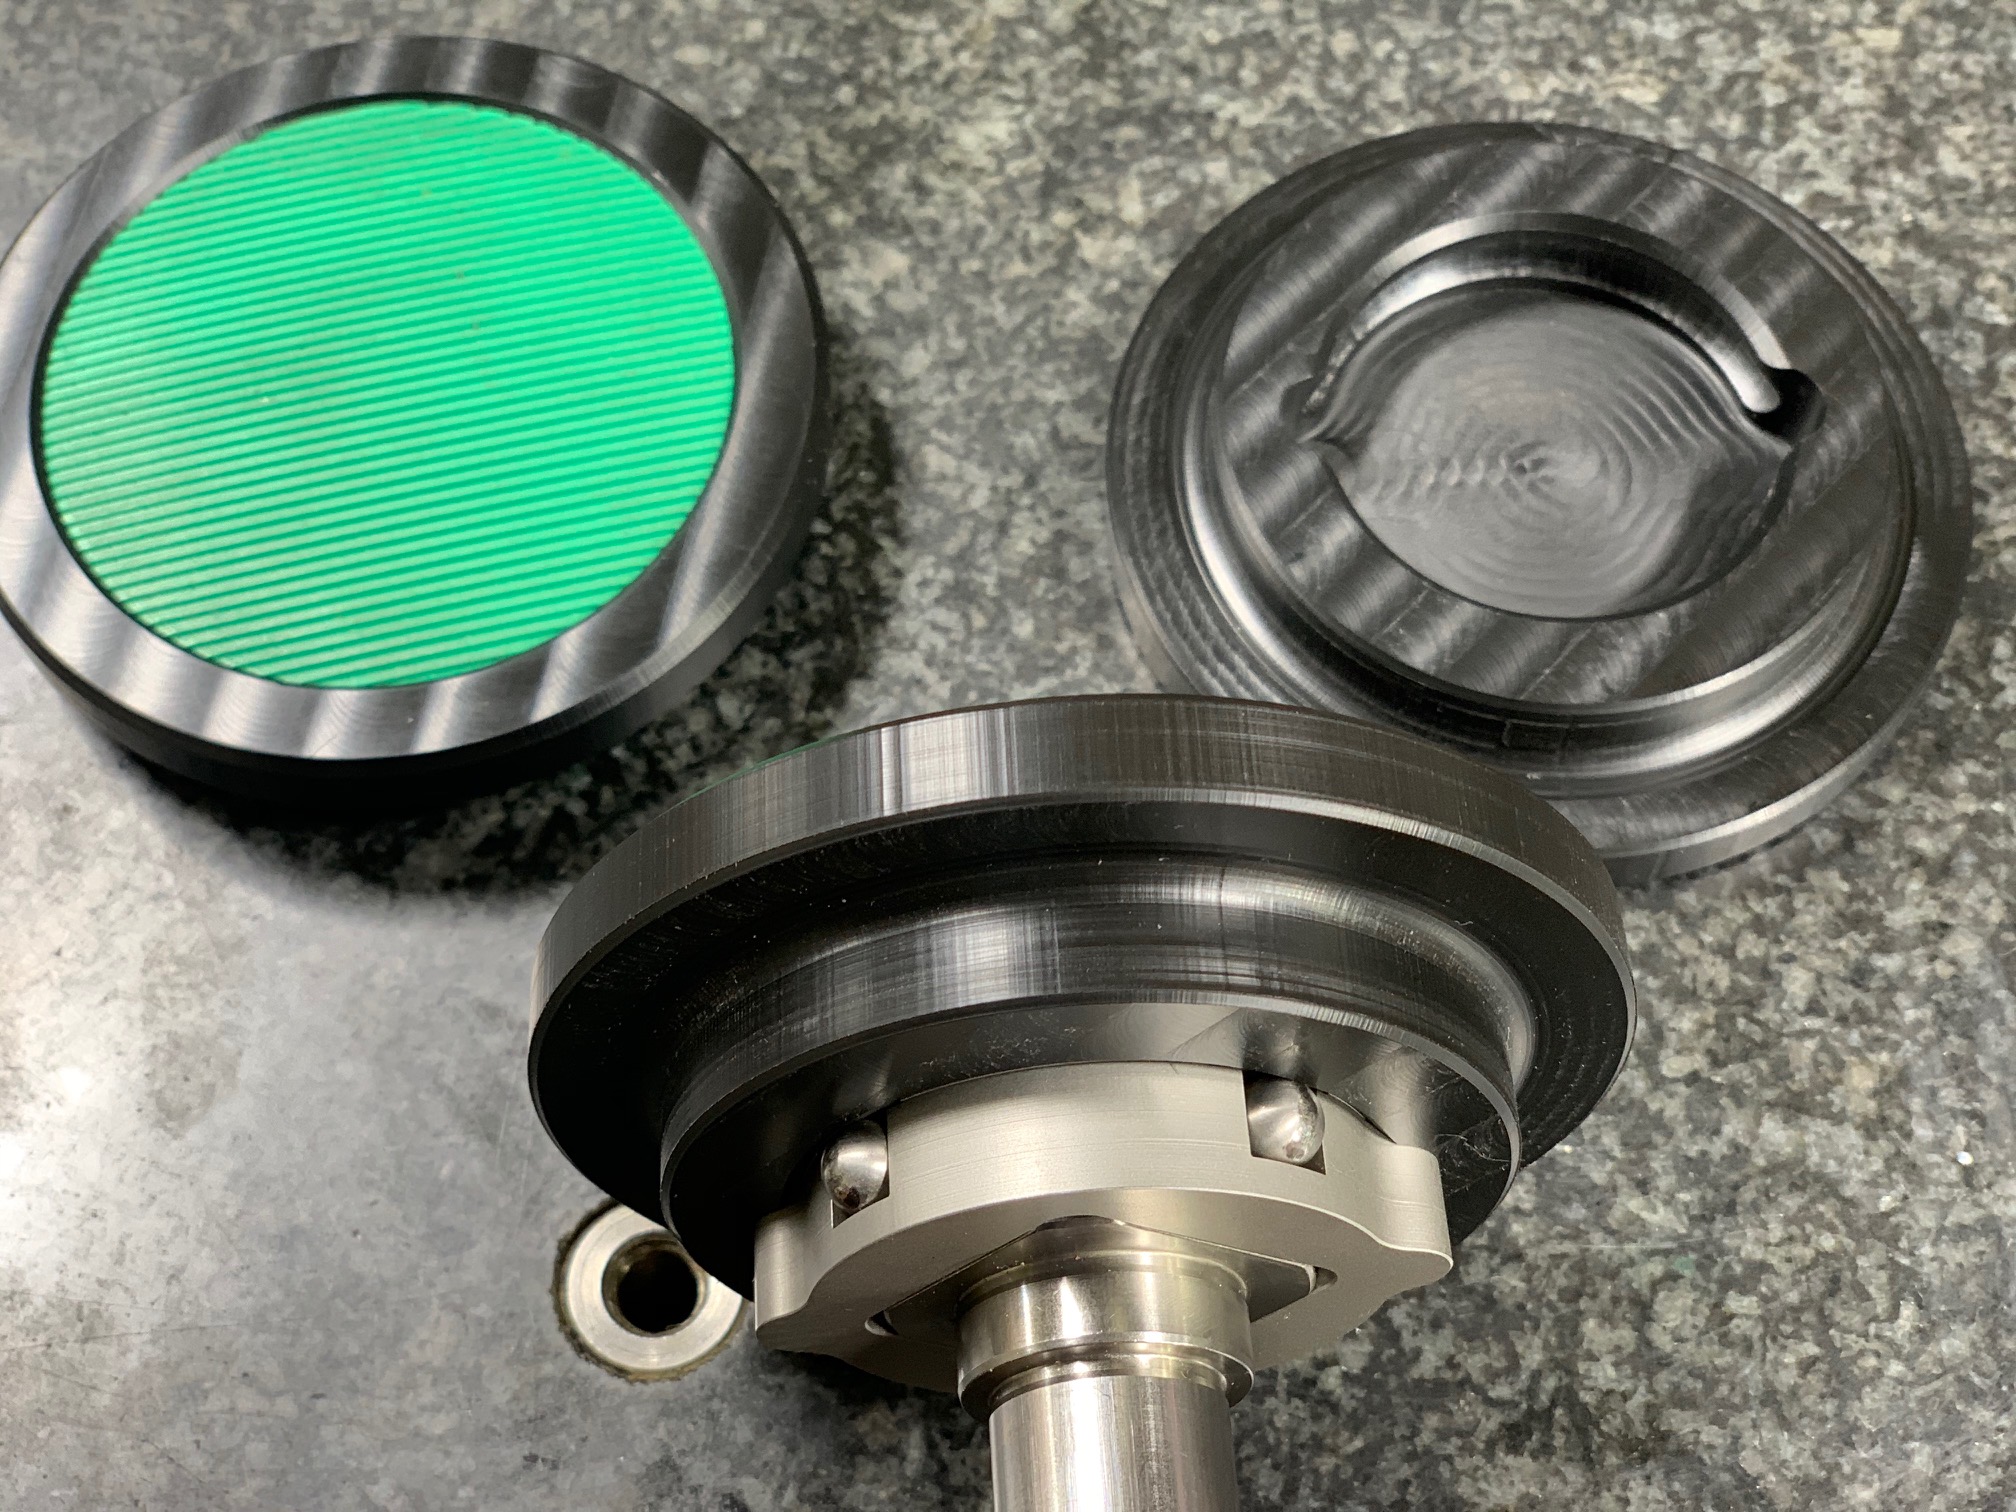
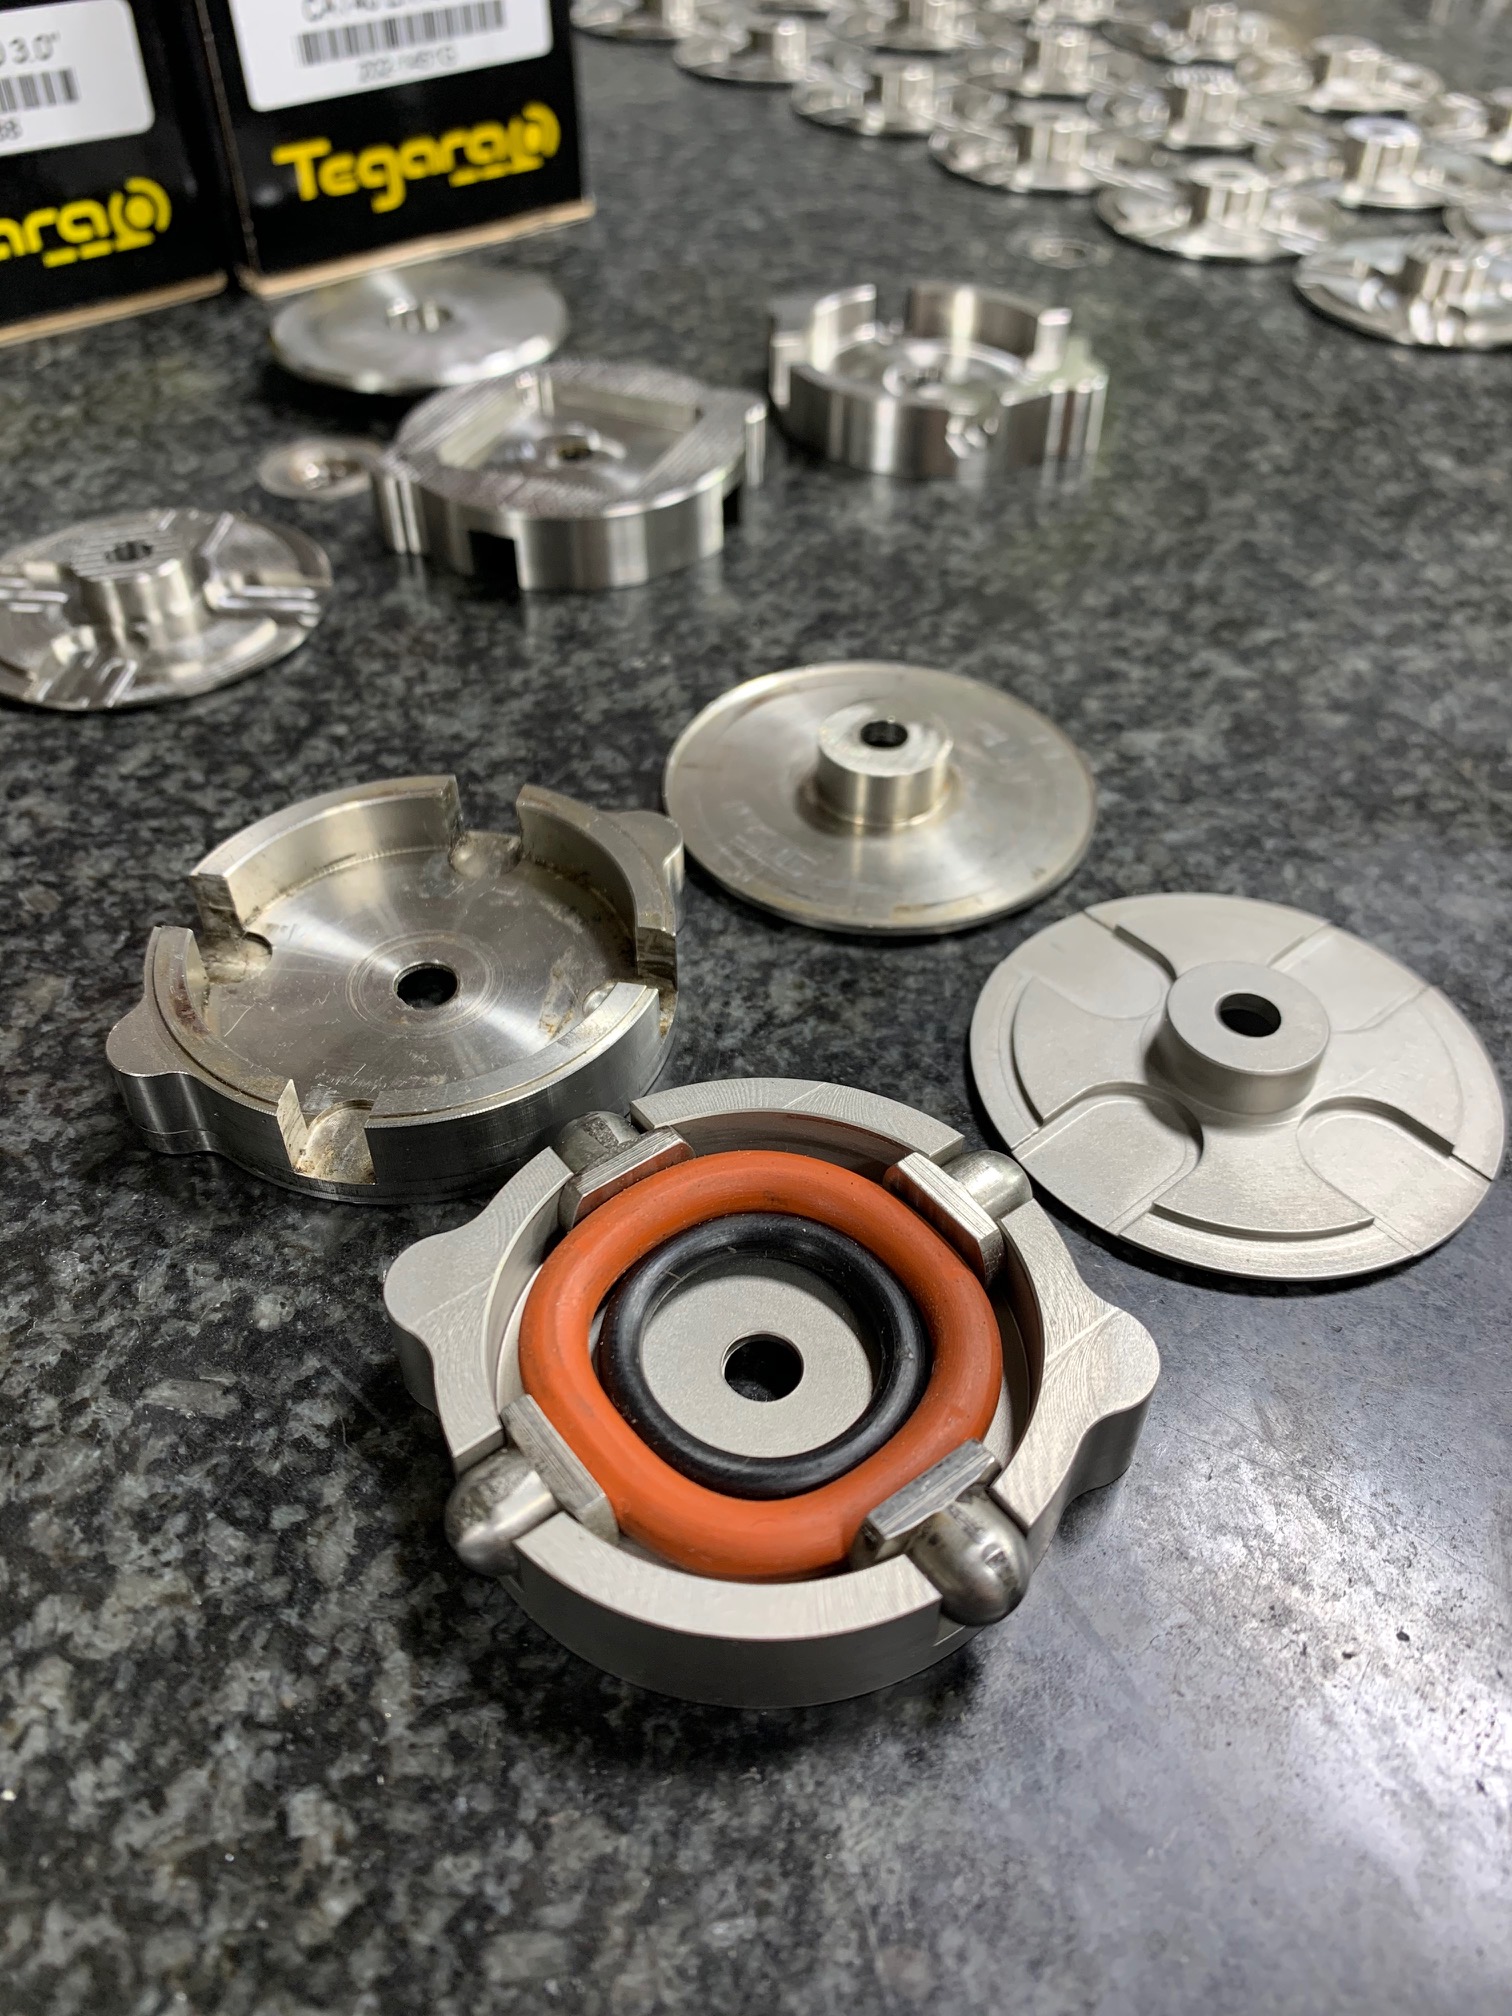
These bottle plates are what the product sits on in the machine and the shaft is where the pulleys mount underneath the turret.

 
These are third party chucks the plates snap onto. I made some changes to them.

 
These are the wheels that put product on the machine and than back on the conveyer.


The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.
Time to create page: 0.318 seconds
Powered by Kunena Forum