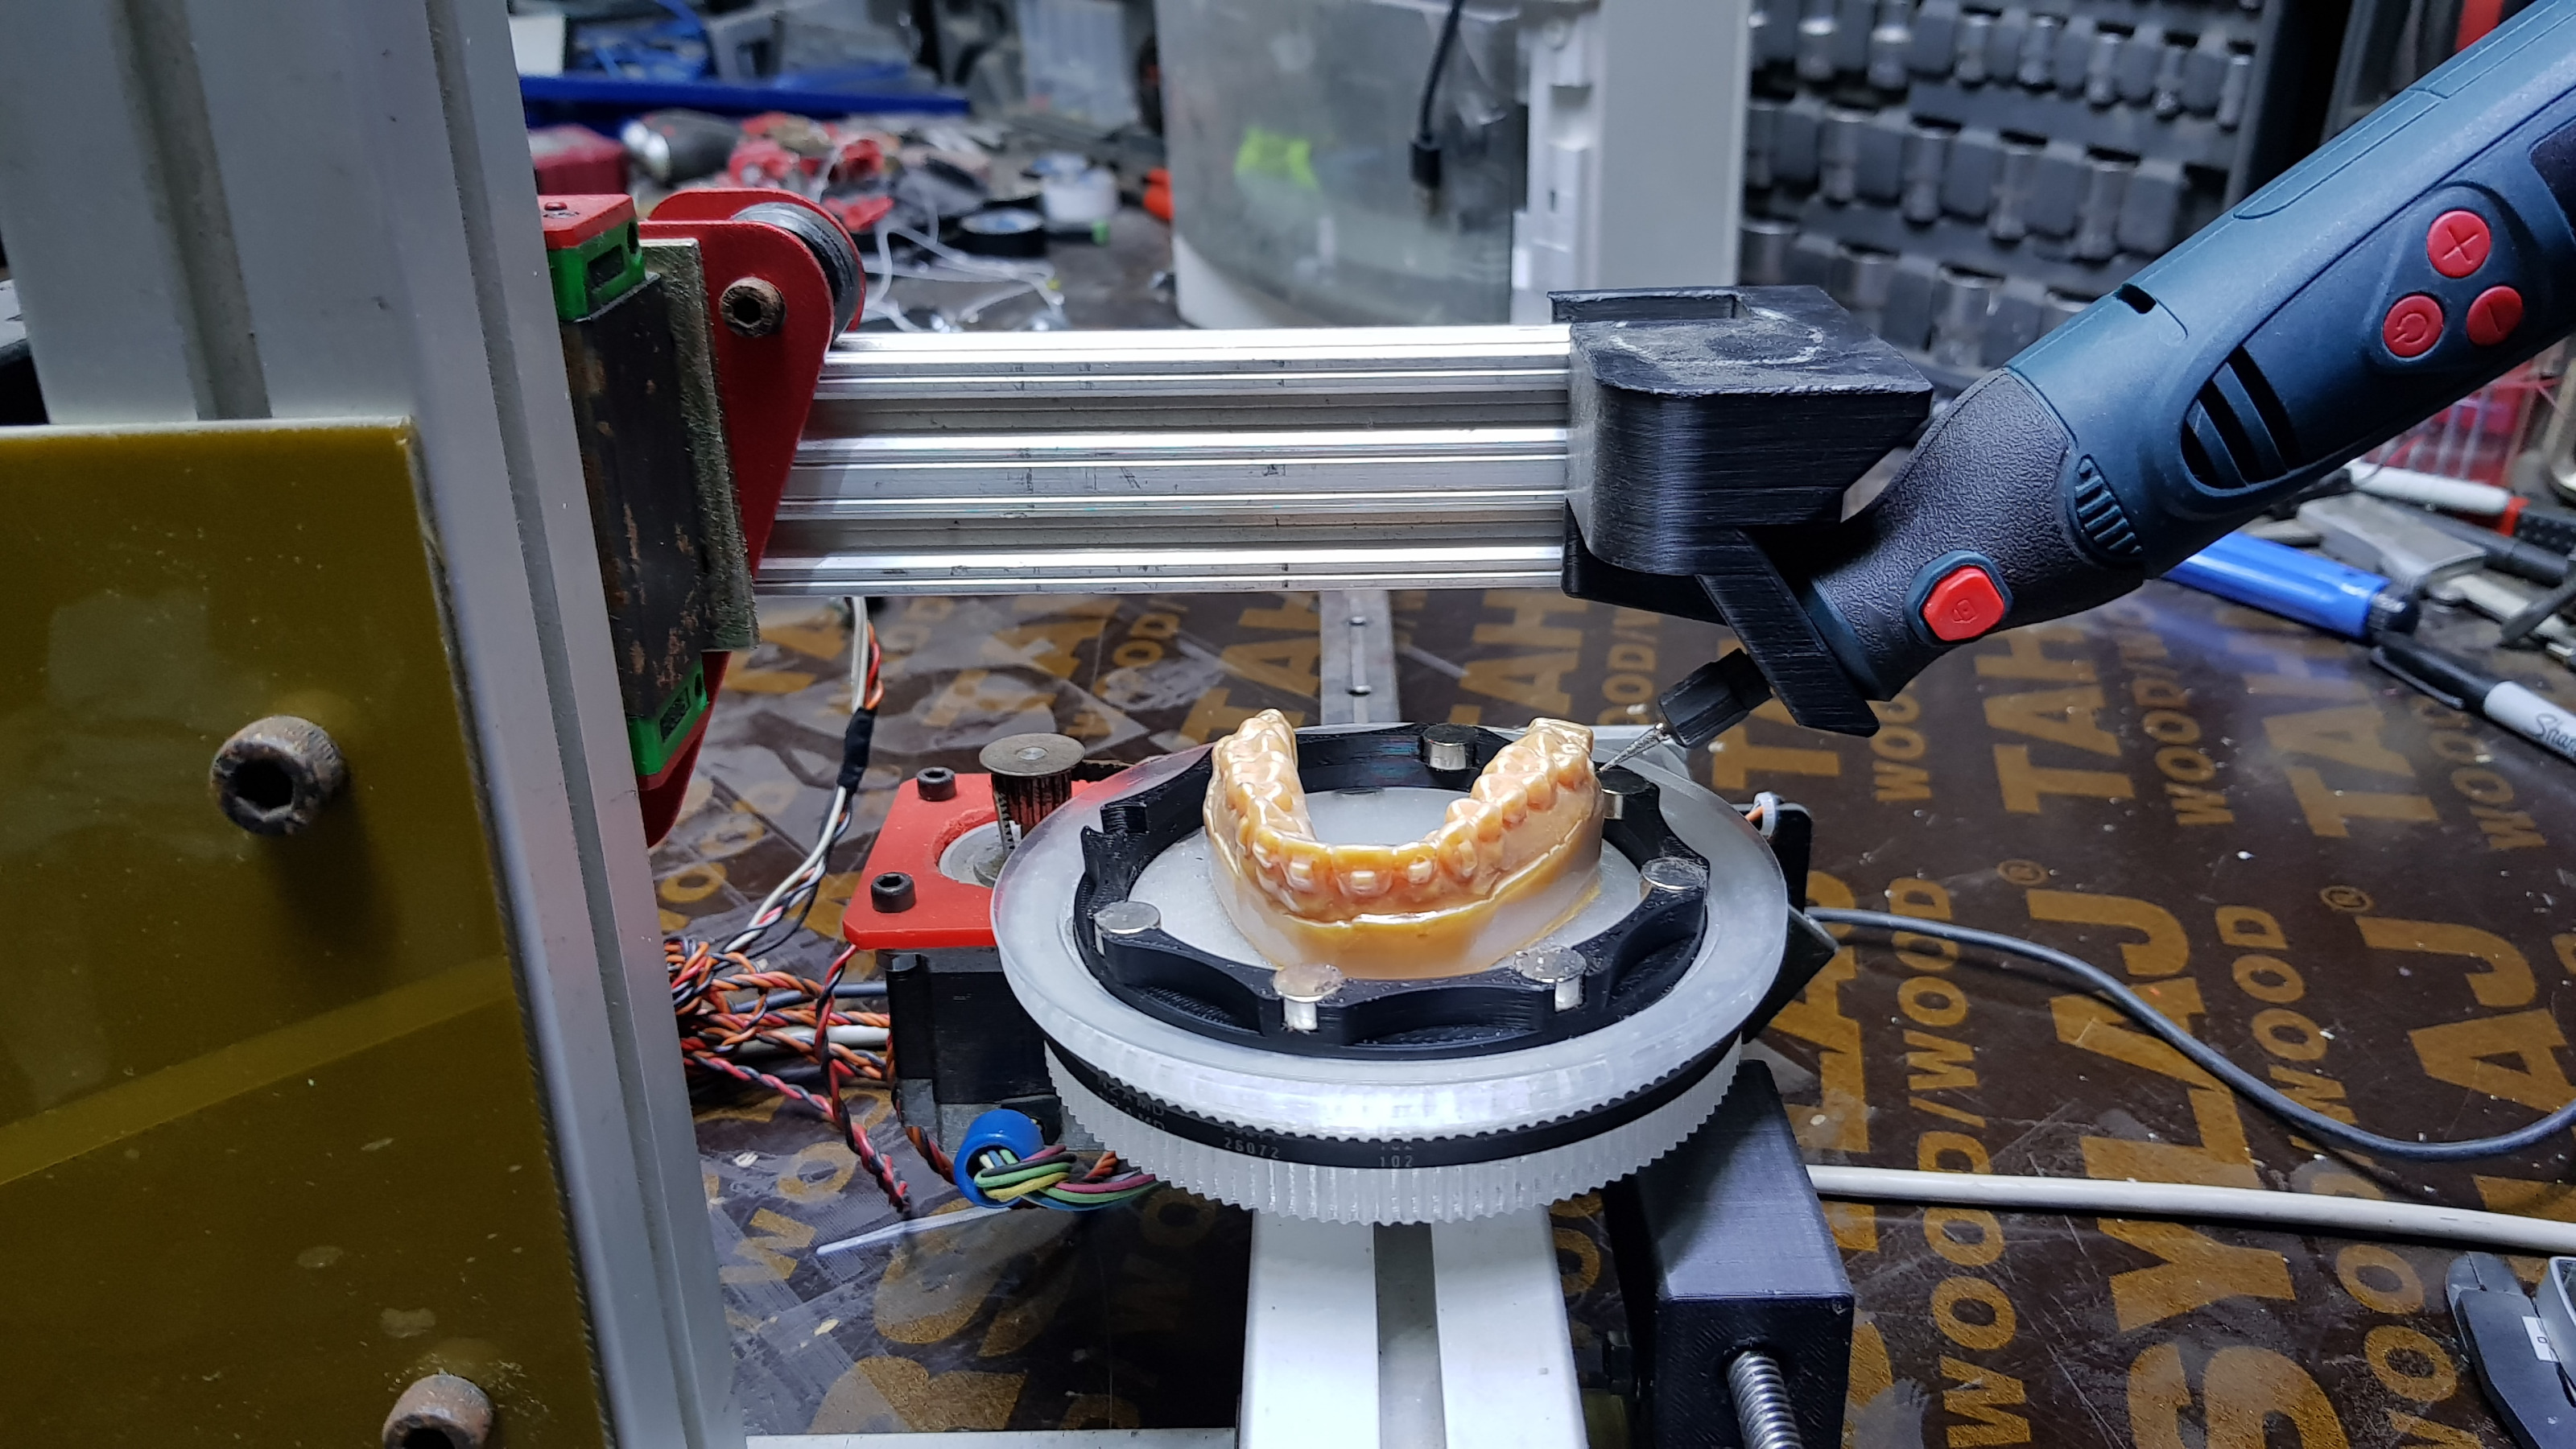
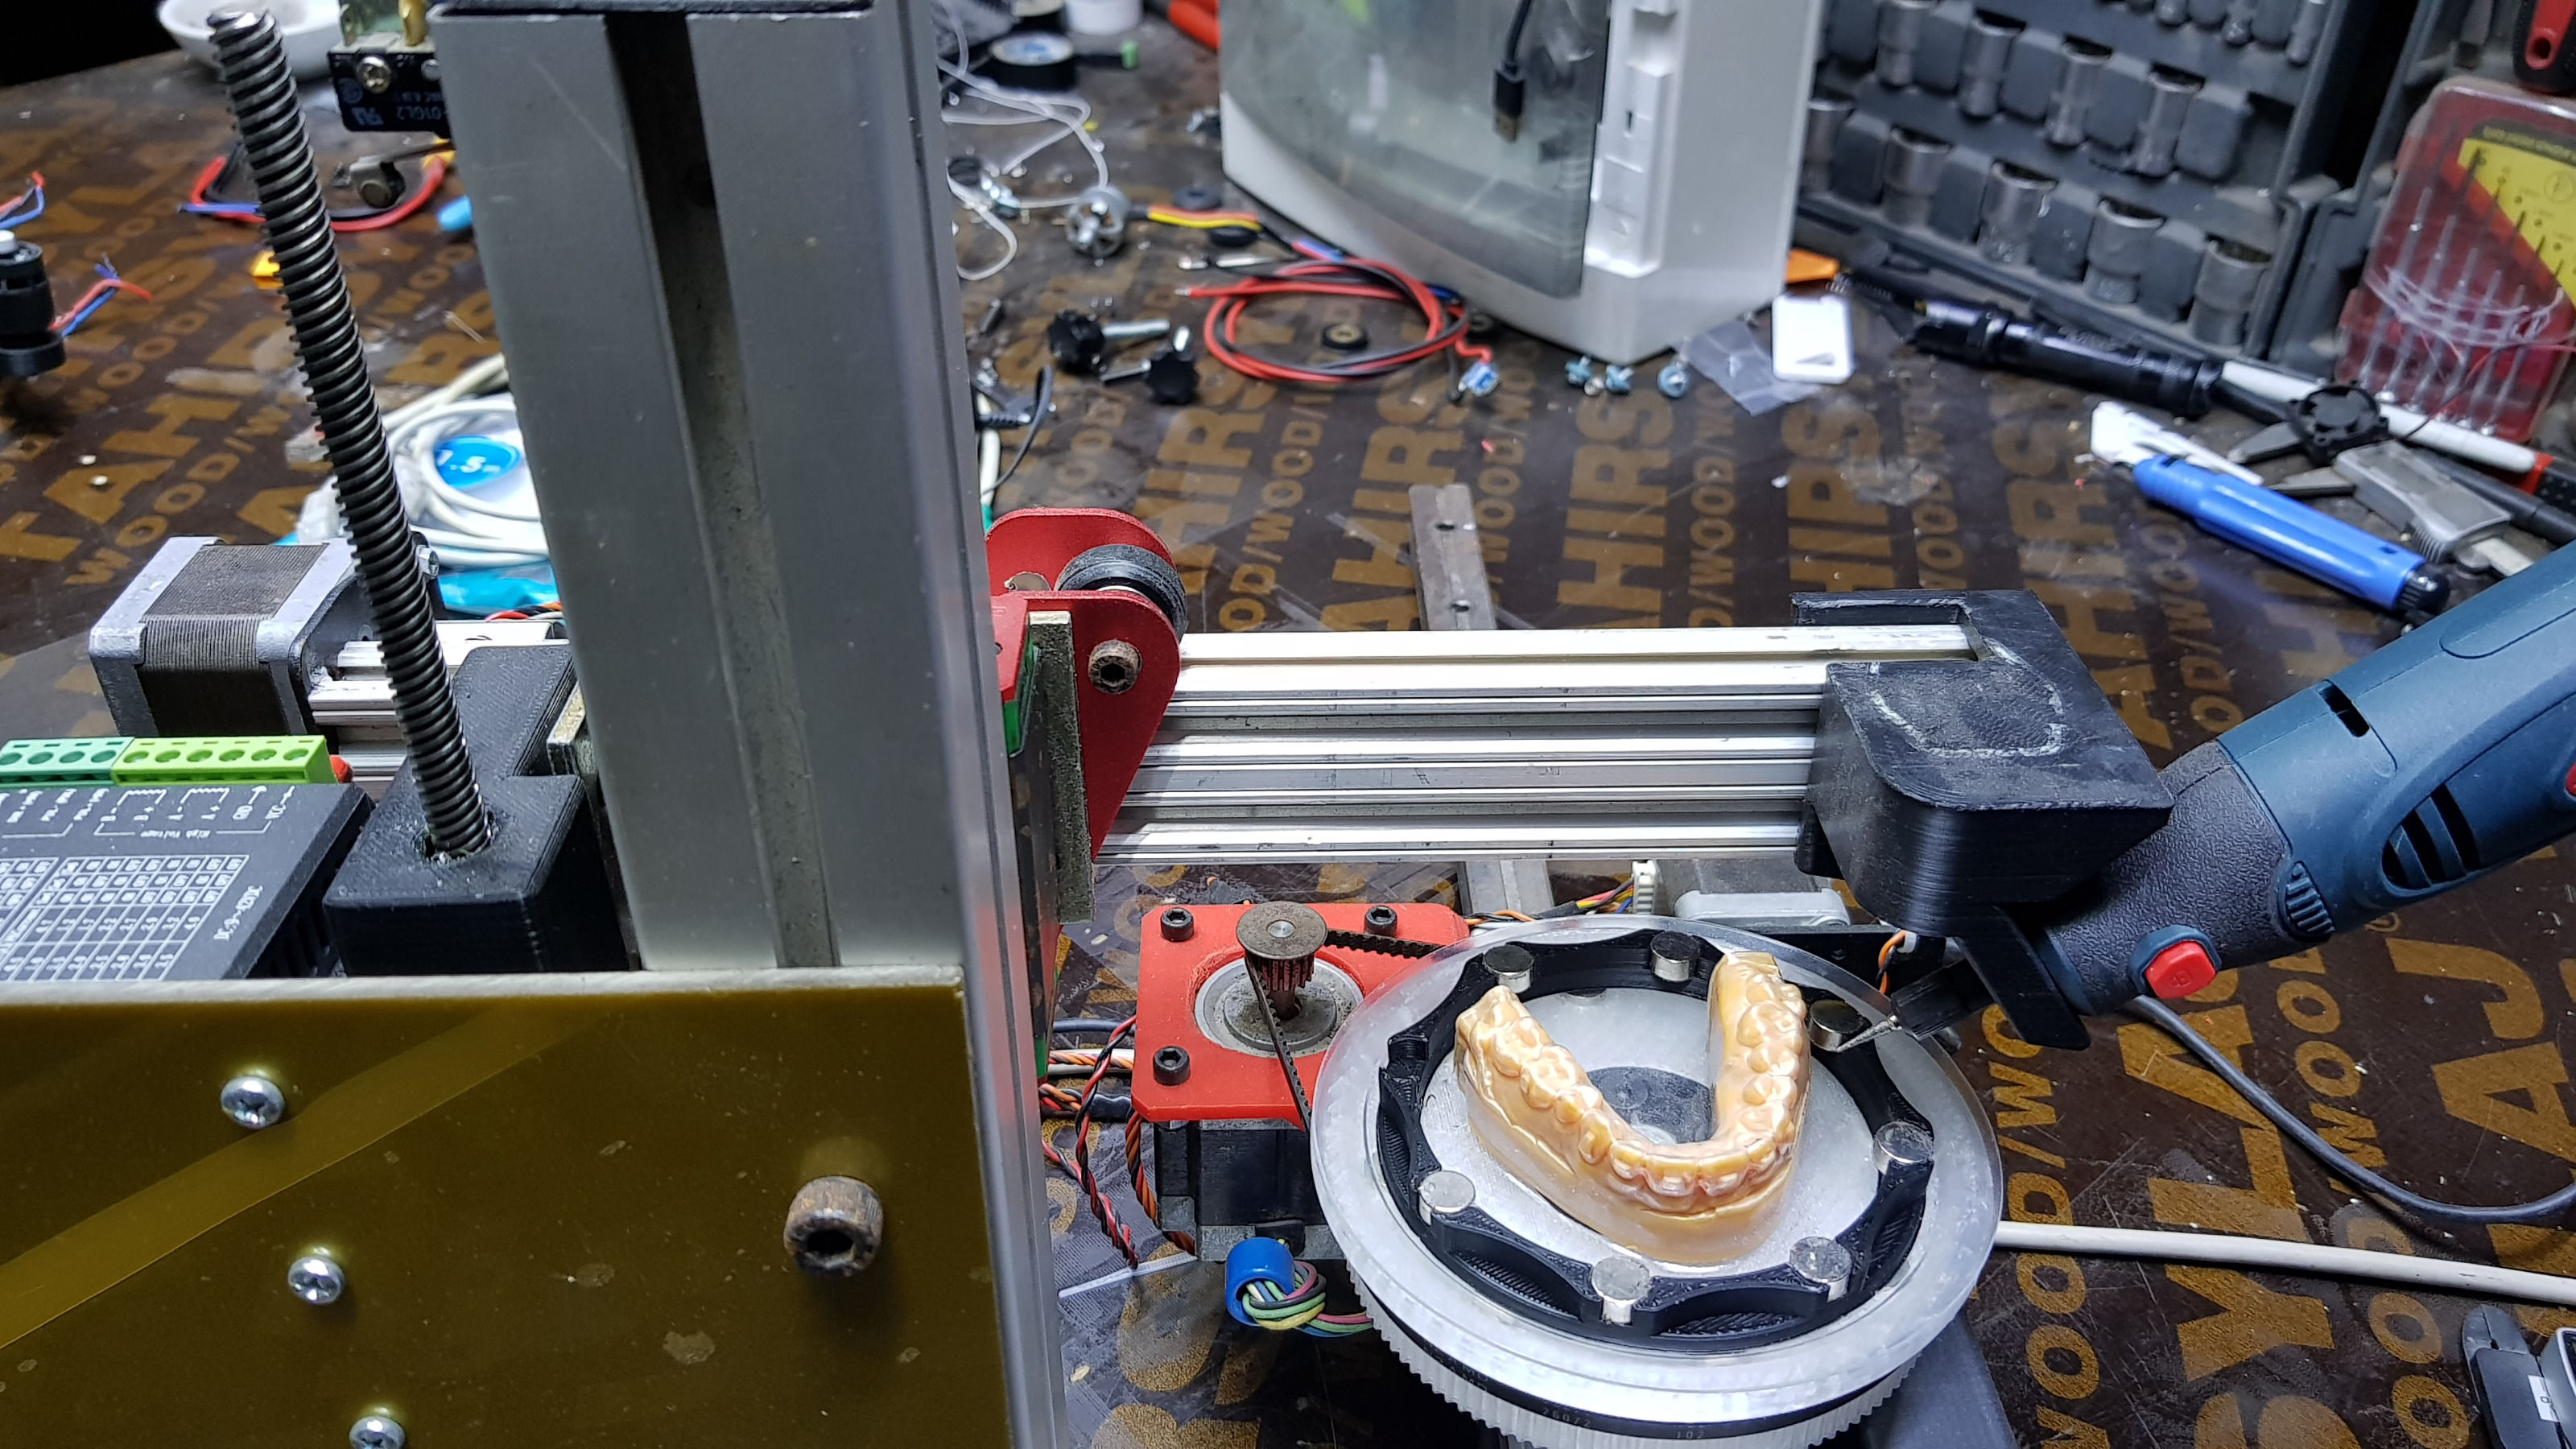
Spindle mounted at the right side of the X axis, and all that mounted to the Z axis (see HiWin HGH25 left)
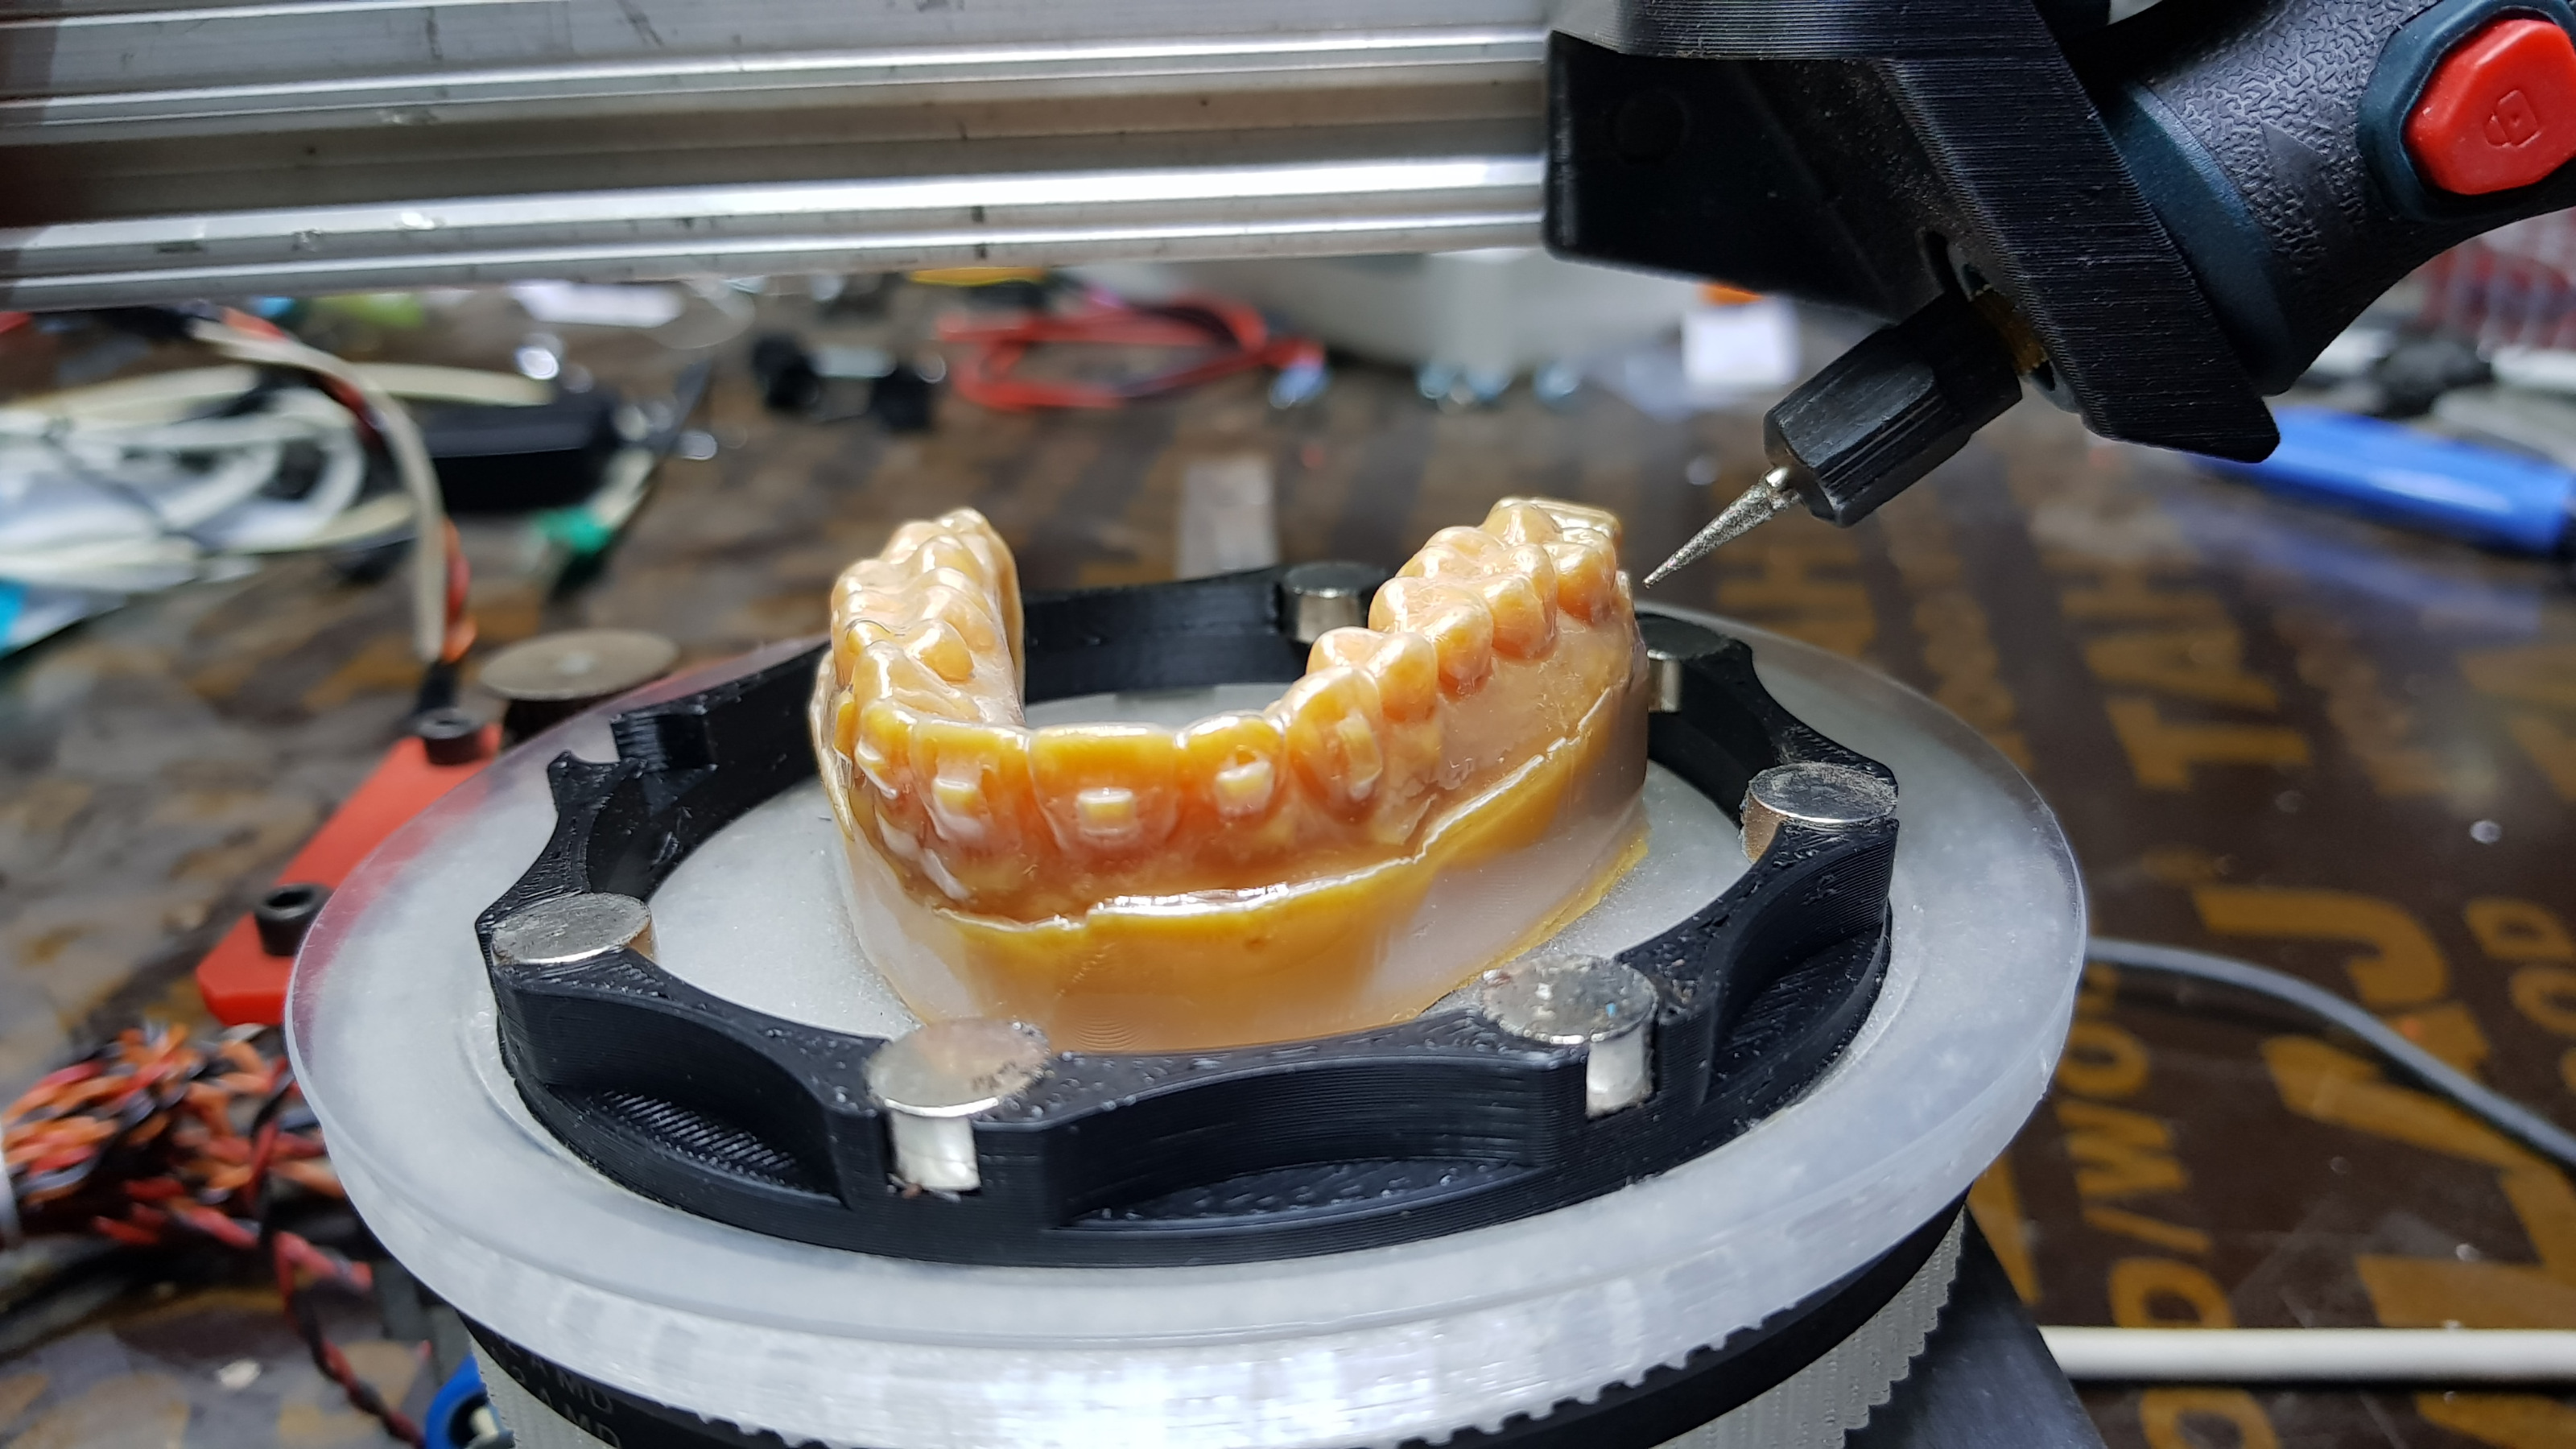
How the tool should be positioned during cutting, only the see-thru thin sheet over the brown (orange?) part must be cut, so about 0.5-1mm deep
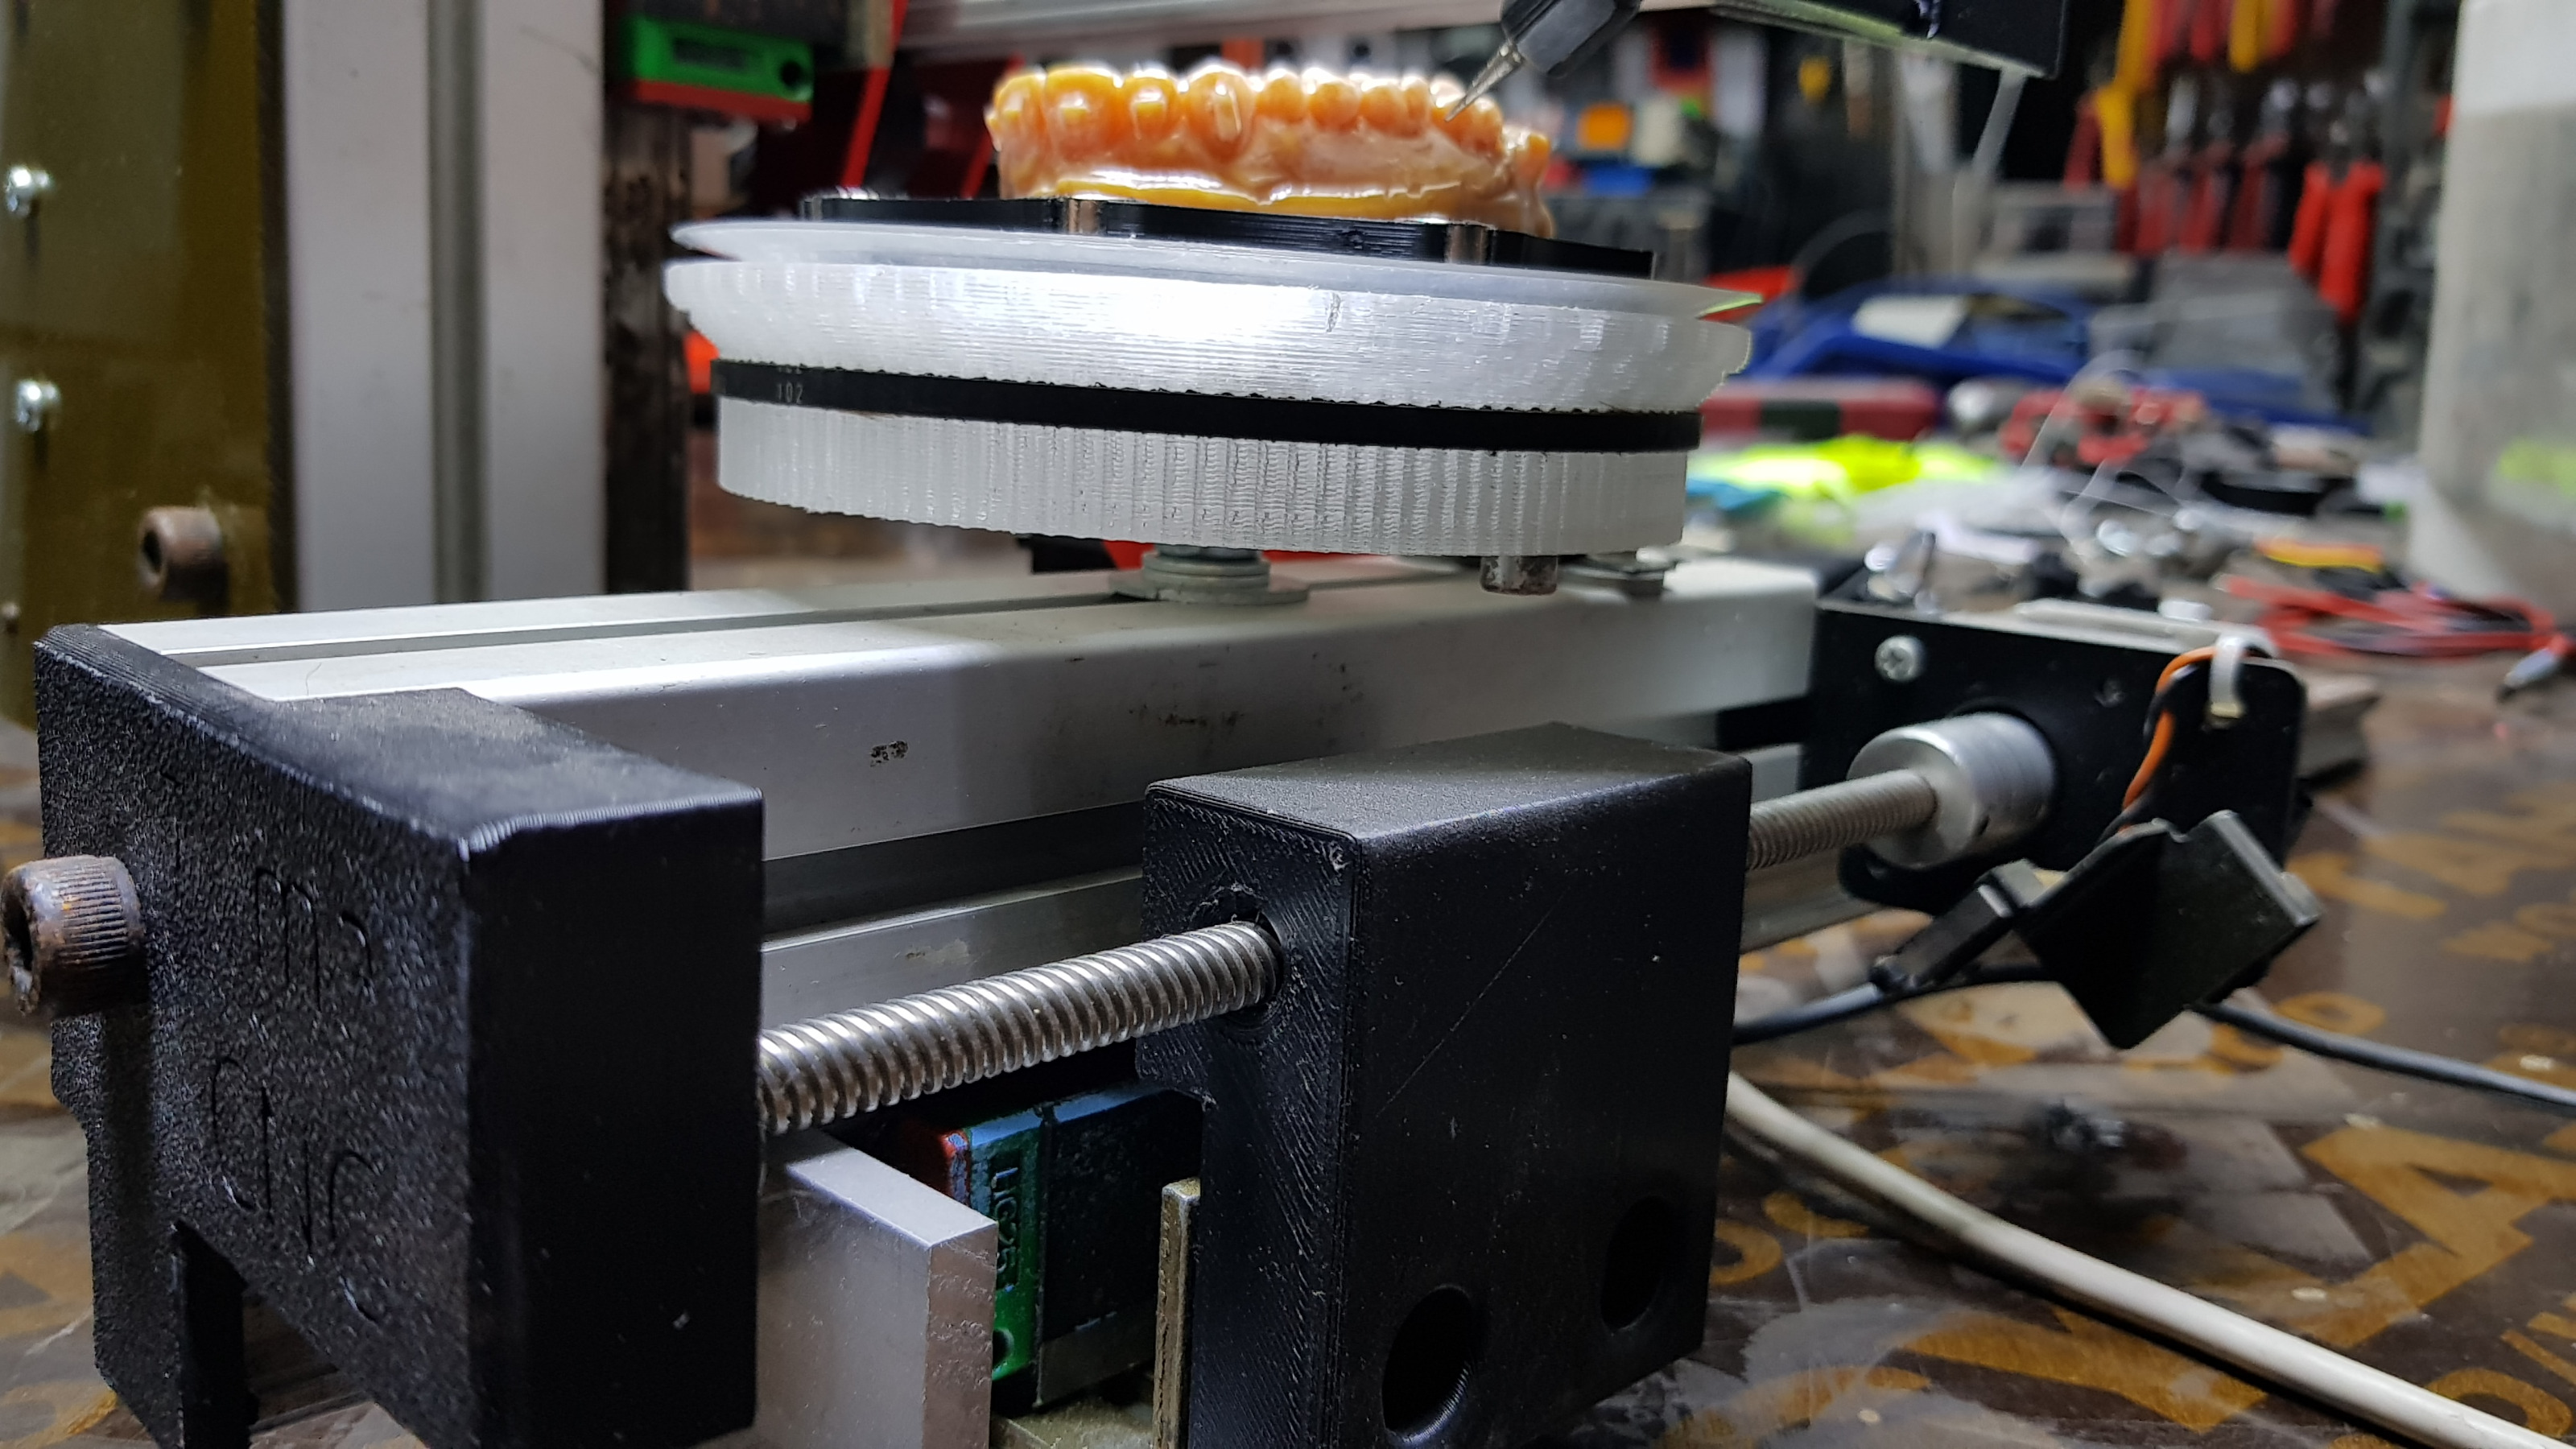
C axis (3D printed round part with teeth for belt) is mounted above the Y axis and moves with it.
Full view of the important parts:
So far i have tried and tested over 10 configs, and over 40 scripts generated by Gemini, so this has become a late evening sport and an exercise in futility, although there were some moments when it seemed it is working, just to fail miserably.
None of those had TCP, just variations of axis/joints and different planes of works space.
Last two configs have TCP, and the subsequent failure to obey the joint/axis velocities and accelerations, the parallel port one a lot, the Mesa one less often so at least i can test a bit with TCP on and feed/speed lowered beyond useful.
And that brings us to:
Aciera, thank you for helping with this, i did not reply last night as i did not have much time to test, so gave it another go tonight (well yesterday, i see now it is 2:04AM here), so here are some of the results, probably in a non-coherent manner:
-in sim, it starts sine but after a short while it rolls/winds the C axis a lot as can be seen on the preview by the tool making a full rotation around the cut line, but in the same spot on the cut line, then continues nicely for most of the cut.
-on a machine, after fixing the limits and G53 0, it does the same thing, but here LinuxCNC errors out and stops the machine, even at very, very low feed rate and low max velocity, usually C axis at the beginning and Y axis a bit later. I am sure i read somewhere here about TCP causing this but could not find it, so i will try again today/tomorrow.
-the thing with C axis going from approx. 110 to -280 in about 10 lines of gcode does not seem OK, and i could not find what is causing that, it happens on several converted/filtered files, not just one, always after several lines of OK code.
-
Again, thank you, will report back whenever i can.

 Topic Author