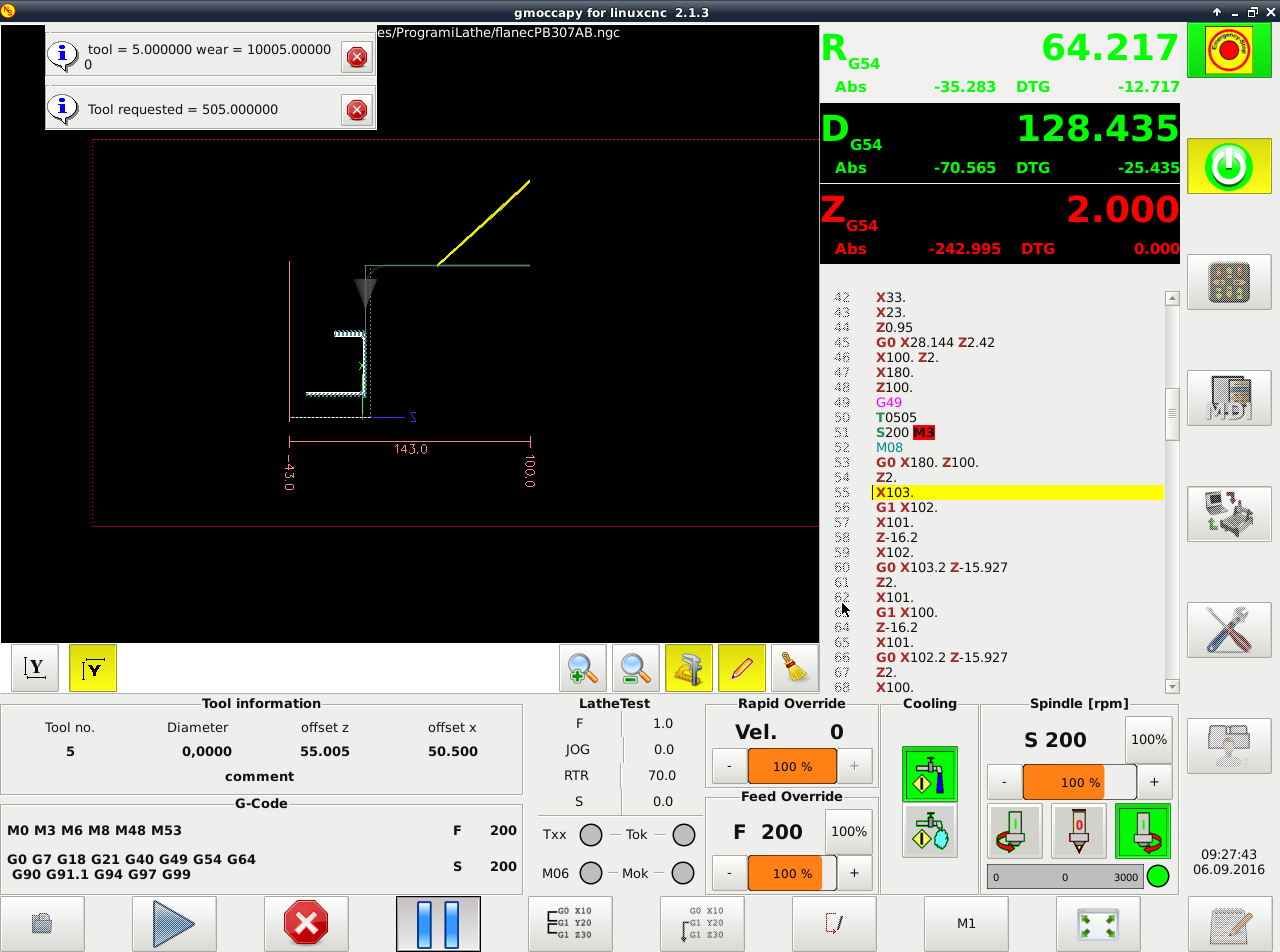
Tool wear in tool table ?

More
10 years 1 month ago #80065 by dinkata
Replied by dinkata on topic Tool wear in tool table ?

could you post your program?

Of course :
Code:
% G18 G21 G7 G40 G49 T0101 S150 M3 M08 G0 X180. Z100. Z5. X0. G1 Z-43. F200.0 G0 Z5. X180. Z100. G49 T0202 S200 M3 M08 G0 X180. Z100. Z2.35 X100. G1 Z2. F200.0 Z1.65 X23. Z2. G0 X24.47 Z2.42 X100. Z1.65 G1 Z1.3 X23. Z1.65 G0 X24.47 Z2.07 X100. Z1.3 G1 Z0.95 X23. Z1.3 G0 X24.47 Z1.72 X100. Z0.95 G1 Z0.8 X92. X33. X23. Z0.95 G0 X28.144 Z2.42 X100. Z2. X180. Z100. G49 T0505 S200 M3 M08 G0 X180. Z100. Z2. X103. G1 X102. X101. Z-16.2 X10². G0 X103.2 Z-15.927 Z2. X101. G1 X100. Z-16.2 X101. G0 X102.2 Z-15.927 Z2. X100. G1 X99. Z-16.2 X100. G0 X101.2 Z-15.927 Z2. X99. G1 X98. Z-16.2 X99. G0 X100.2 Z-15.927 Z2. X98. G1 X97. Z-16.2 X98. G0 X99.2 Z-15.927 Z2. X97. G1 X96. Z-16.2 X97. G0 X98.2 Z-15.927 Z2. X96. G1 X95. Z-0.369 X95.131 Z-0.434 G03 X95.6 Z-1. K-0.566 I-0.566 G1 Z-16.2 X96. G0 X97.2 Z-15.927 Z2. X95. G1 X94. Z0.131 X95. Z-0.369 G0 X96.2 Z-0.095 Z2. X94. G1 X93.6 Z0.331 X94. Z0.131 G0 X102.201 Z2. X103.2 X102. X180. Z100. G49 T0606 S200 M3 M08 G0 X180. Z100. Z2. X26.7 G1 X26. F250.0 X26.7 Z-32.996 X26. G0 X25.16 Z-32.075 Z2. X26.7 G1 X27.4 Z-32.996 X26.7 G0 X25.86 Z-32.075 Z2. X27.4 G1 X28.1 Z-32.996 X27.4 G0 X26.56 Z-32.075 Z2. X28.1 G1 X28.8 Z-32.996 X28.1 G0 X27.26 Z-32.075 Z2. X28.8 G1 X29.5 Z-1.184 X29.434 Z-1.217 G02 X29.2 Z-1.5 K-0.283 I0.283 G1 Z-32.996 X28.8 G0 X27.96 Z-32.075 Z2. X29.5 G1 X30.2 Z-0.834 X29.5 Z-1.184 G0 X28.66 Z-0.263 Z2. X30.2 G1 X30.9 Z-0.484 X30.2 Z-0.834 G0 X29.36 Z0.087 Z2. X30.9 G1 X31.6 Z-0.134 X30.9 Z-0.484 G0 X30.06 Z0.437 Z2. X31.6 G1 X32.2 Z0.166 X31.6 Z-0.134 G0 X29.655 Z2. X25.16 X26. X180. Z100. M5 M9 M2 %

Please Log in or Create an account to join the conversation.

More
10 years 1 month ago - 10 years 1 month ago #80066 by dinkata
Replied by dinkata on topic Tool wear in tool table ?
1.If we start from the beginning - no problem
2.Very useful tool wear in tooltable !
3.But we need when setting program use " run-at-line "
..If we start from line
.....G49
T0505 ..


remap wants to put previous tools

4.If I hide previous tools
.........
( T0101 )
.........
( T0202 )...
.......
and start from line
.....G49
T0505 ..
Then remap work properly


Is it possible to avoid hiding previous instruments?
Last edit: 10 years 1 month ago by dinkata.

Please Log in or Create an account to join the conversation.

More
10 years 1 month ago #80067 by cmorley
Replied by cmorley on topic Tool wear in tool table ?
I confirm the problem.
I'll try to look into it tomorrow
Chris M
The following user(s) said Thank You: dinkata

Please Log in or Create an account to join the conversation.

More
10 years 1 month ago - 10 years 1 month ago #80112 by nkp
Replied by nkp on topic Tool wear in tool table ?
I think that "the bug" in remap.
The following code works fine:
Code:
% G18 G21 G7 G40 ;------------------------tool 1, wear 1 G49 T1 M6 G43 G43.2 H10001 ;------------------------ S150 M3 M08 G0 X180. Z100. Z5. X0. G1 Z-43. F200.0 G0 Z5. X180. Z100. ;------------------------tool 2, wear 2 G49 T2 M6 G43 G43.2 H10002 ;------------------------ S200 M3 M08 G0 X180. Z100. Z2.35 X100. G1 Z2. F200.0 Z1.65 X23. Z2. G0 X24.47 Z2.42 X100. Z1.65 G1 Z1.3 X23. Z1.65 G0 X24.47 Z2.07 X100. Z1.3 G1 Z0.95 X23. Z1.3 G0 X24.47 Z1.72 X100. Z0.95 G1 Z0.8 X92. X33. X23. Z0.95 G0 X28.144 Z2.42 X100. Z2. X180. Z100. ;------------------------tool 5, wear 5 G49 T5 M6 G43 G43.2 H10005 ;------------------------ S200 M3 M08 G0 X180. Z100. Z2. X103. G1 X102. X101. Z-16.2 X10². G0 X103.2 Z-15.927 Z2. X101. G1 X100. Z-16.2 X101. G0 X102.2 Z-15.927 Z2. X100. G1 X99. Z-16.2 X100. G0 X101.2 Z-15.927 Z2. X99. G1 X98. Z-16.2 X99. G0 X100.2 Z-15.927 Z2. X98. G1 X97. Z-16.2 X98. G0 X99.2 Z-15.927 Z2. X97. G1 X96. Z-16.2 X97. G0 X98.2 Z-15.927 Z2. X96. G1 X95. Z-0.369 X95.131 Z-0.434 G03 X95.6 Z-1. K-0.566 I-0.566 G1 Z-16.2 X96. G0 X97.2 Z-15.927 Z2. X95. G1 X94. Z0.131 X95. Z-0.369 G0 X96.2 Z-0.095 Z2. X94. G1 X93.6 Z0.331 X94. Z0.131 G0 X102.201 Z2. X103.2 X102. X180. Z100. ;------------------------tool 6, wear 6 G49 T6 M6 G43 G43.2 H10006 ;------------------------ S200 M3 M08 G0 X180. Z100. Z2. X26.7 G1 X26. F250.0 X26.7 Z-32.996 X26. G0 X25.16 Z-32.075 Z2. X26.7 G1 X27.4 Z-32.996 X26.7 G0 X25.86 Z-32.075 Z2. X27.4 G1 X28.1 Z-32.996 X27.4 G0 X26.56 Z-32.075 Z2. X28.1 G1 X28.8 Z-32.996 X28.1 G0 X27.26 Z-32.075 Z2. X28.8 G1 X29.5 Z-1.184 X29.434 Z-1.217 G02 X29.2 Z-1.5 K-0.283 I0.283 G1 Z-32.996 X28.8 G0 X27.96 Z-32.075 Z2. X29.5 G1 X30.2 Z-0.834 X29.5 Z-1.184 G0 X28.66 Z-0.263 Z2. X30.2 G1 X30.9 Z-0.484 X30.2 Z-0.834 G0 X29.36 Z0.087 Z2. X30.9 G1 X31.6 Z-0.134 X30.9 Z-0.484 G0 X30.06 Z0.437 Z2. X31.6 G1 X32.2 Z0.166 X31.6 Z-0.134 G0 X29.655 Z2. X25.16 X26. X180. Z100. M5 M9 M2 %
ini:
#REMAP = T prolog=get_T_number ngc=toolchange
Last edit: 10 years 1 month ago by nkp.
The following user(s) said Thank You: jo_key, dinkata

Please Log in or Create an account to join the conversation.

More
5 years 11 months ago #189112 by jlviloria
Replied by jlviloria on topic Tool wear in tool table ?
Hi,
You managed to fix this problem. It happens to me exactly the same. when I try to run Run-at-line, having fanucy remap. executes wrong tool change.

Jorge Viloria.

Please Log in or Create an account to join the conversation.

Time to create page: 0.084 seconds
Powered by Kunena Forum