
- Posts: 39
- Thank you received: 3

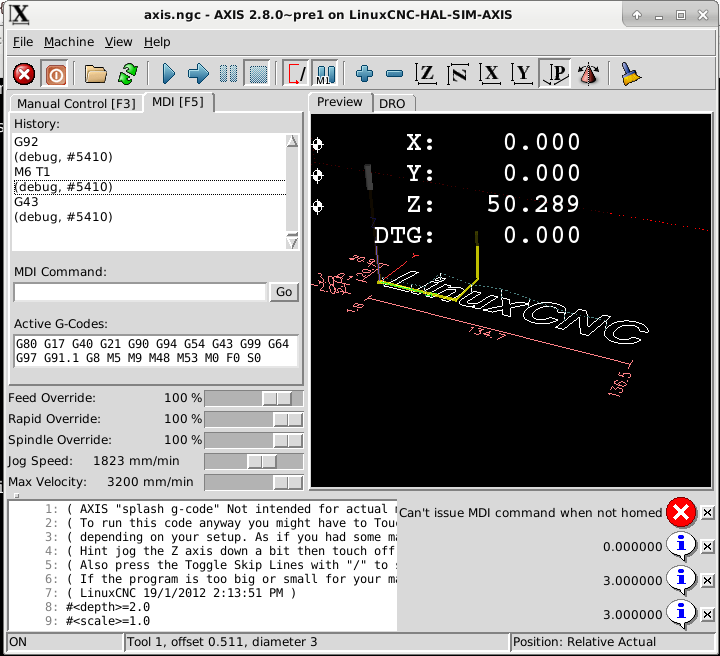
It turns out that #5410 is always zero for me. I have added a non-zero diameter in the tool table for a specific tool, reload the tool table and change to that tool. Still zero.andypugh wrote: G53 G0 X[100 - #5410] Y100
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
cahlfors wrote: Had some more time to tinker with this. It turns out that #5410 et al contain information about the *current* tool, not the one we are changing *to* and so cannot be used in the remap code.
Please Log in or Create an account to join the conversation.
andypugh wrote: G43 takes an optional H parameter, so you can issue a G43 to load the offsets for the next tool and read out the diameter from #5410 without physically changing tool.
You probably then want to zero-out the offsets (G49) before probing and finally load the new offsets at the same time as issuing the M6.
Please Log in or Create an account to join the conversation.
cahlfors wrote:
andypugh wrote: but #<_selected_tool> still refers to the old tool.
Which prolog are you using? The one I just looked at uses #<selected_tool> without the _
You need to do the M6 in your remap at some point anyway, why not do it early in the routine so the numeric parameters are accurate?
Please Log in or Create an account to join the conversation.
