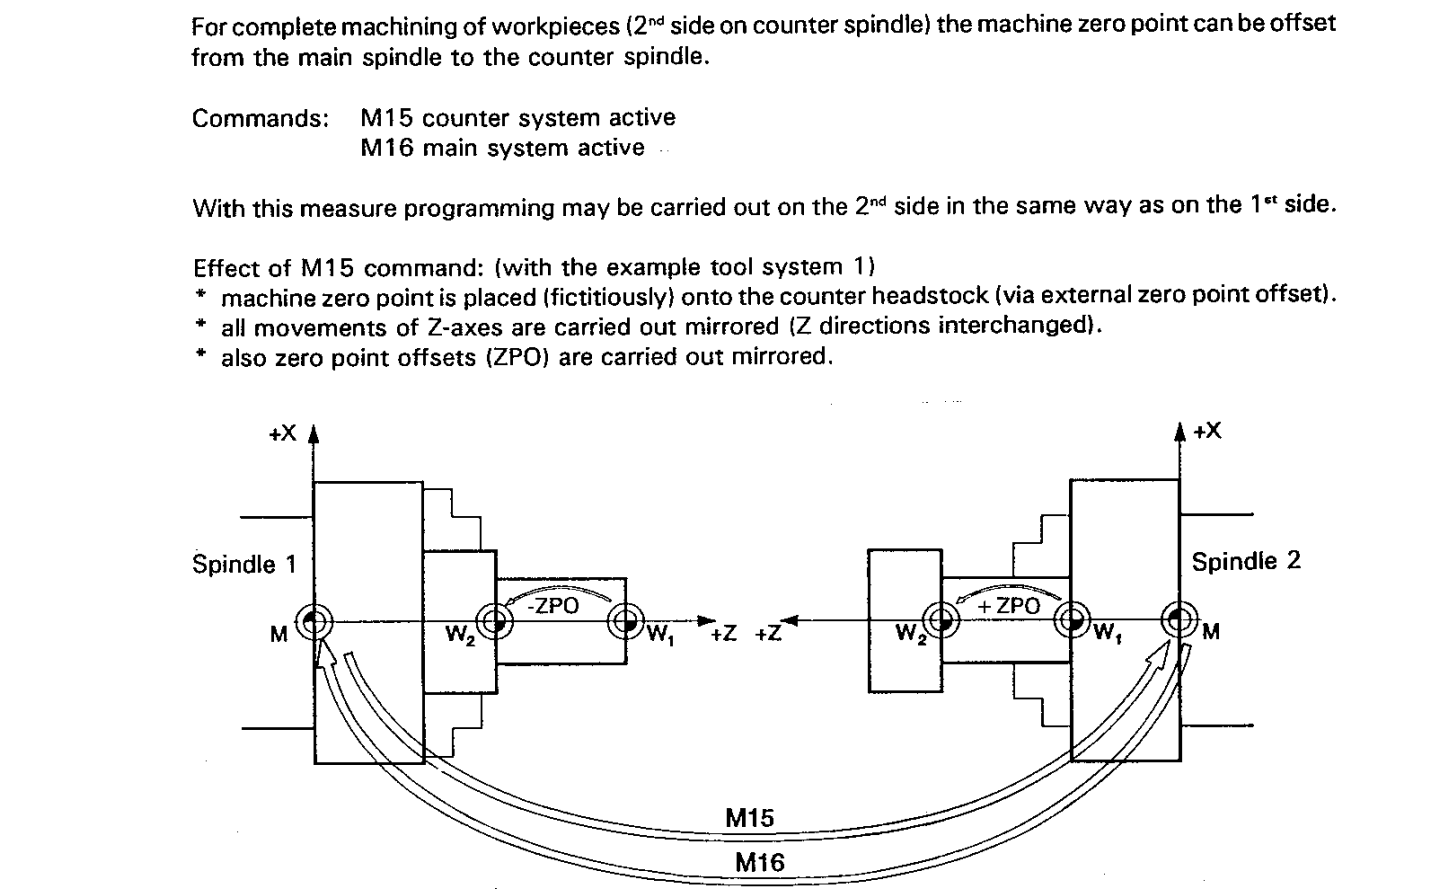
I think that axis mirroring with cutter comp would be difficult (by which I mean that it won't work within the current LinuxCNC architecture)
The XZUW positions are determined by the G-code, then the offsets are applied, and then it goes to the kinematics module.
So whilst there are many ways to combine joints inside the kinematics (as is done for gantries) there isn't a way to have the axis offsets apply (also as these are _axis_ offsets not joint offsets)
There is also no way to program an XY arc and a UW arc to occur simultaneously. (This is a G-code limitation)
So, it is easy to make the UW axes move in a exact mirror of the XZ axes (whether by using HAL wiring or the kinematics modules.) But it isn't easy to apply offsets.
However, if you are willing to consider _only_ having length compensation for UW (not diameter) then it might be possible to link
halui
.tool-length.u/w in to a modified kinematics module to achieve approximately the required effect. A custom kinematics would also allow you to move the origin from one spindle to the other.
The problem with switching kinematics on the fly like this is that it tends to cause an immediate following-error. This needs to be handled, and there is some work ongoing in this direction with Switchkins.
If the counter-spindle moves in Z, does the coorodinate system move with it?