
- Posts: 19899
- Thank you received: 4655
Retrofitting a 1986 Maho MH400E
- andypugh
- Offline
- Moderator
-

Less
More
7 years 10 months ago #122692
by andypugh
It would do London to Edinburgh and back in the same day, so at least 1 million linear feet.
That's a _lot_ of G-code path.
Replied by andypugh on topic Retrofitting a 1986 Maho MH400E
RotarySMP wrote: Wonder what the MTBR was

It would do London to Edinburgh and back in the same day, so at least 1 million linear feet.
That's a _lot_ of G-code path.
The following user(s) said Thank You: RotarySMP
- RotarySMP
- Offline
- Platinum Member
-

Less
More
- Posts: 1635
- Thank you received: 595
7 years 10 months ago #122693
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Pretty amazing when you considered the state of the art of oil technology and metallugy back then.
Is the tendancy to galling in machine slides acentuated by the extemely short moves used in HSM, not allowing the hydrostatic bearing to build? Or are we just seeing the machines which ran without way oil, and worn out wipers for years?
Mark
Is the tendancy to galling in machine slides acentuated by the extemely short moves used in HSM, not allowing the hydrostatic bearing to build? Or are we just seeing the machines which ran without way oil, and worn out wipers for years?
Mark
- Todd Zuercher
- Offline
- Platinum Member
-
Less
More
- Posts: 4793
- Thank you received: 1480
7 years 10 months ago #122696
by Todd Zuercher
Replied by Todd Zuercher on topic Retrofitting a 1986 Maho MH400E
Without knowing how well the machines were maintained and used, I'd be inclined to say the latter.
- Glemigobles
- Offline
- Elite Member
-

Less
More
- Posts: 201
- Thank you received: 18
7 years 10 months ago #122702
by Glemigobles
Replied by Glemigobles on topic Retrofitting a 1986 Maho MH400E
Mark, I would tend to agree with Todd, in that I think you're being very conservative in terms of these machines' capabilities when they're properly tended to. You mentioned linear ways for HSM toolpaths, but DMG linear way machines reach 100 m/min in rapids:
en.dmgmori.com/products/machines/milling...near/dmc-80-h-linear
5-10 m/min is definitely not beyond the realm of slide ways, it's just that there's a lot of things to consider and a hobby modder can make a whole bunch of wrong choices that result in damages. Also, the machines are so old you never know how they were treated before.
Btw, I think Stig is fine with his Maho, though using a toolroom machine as a basis for a mill intended to cut aluminum seems sort of bizzare to me. My friend uses a 750 W 24000 rpm spindle on a 5000€ Chinese gantry-type machine (that's including transportation costs and taxes) with Mach3 to cut aluminum and he turns a tidy profit doing so. He bought a cast-iron machine and simply had the ways ground on a surface grinder to get the geometry right. Seems like far less work for a similar result (unless he's working on some large castings and needs the long Z travel).
All things considered, I think your retrofit is a much better idea. You can drill and tap in steel without worry and it's really easy to attach a fast spindle in the place of the vertical head to make short work of aluminum and plastics. To be honest, if you're cutting metals, the feeds are never all that high, especially with small endmills. Fast rapids, on the other hand, are always useful.
The following user(s) said Thank You: RotarySMP
- Bernd
- Offline
- New Member
-

Less
More
- Posts: 11
- Thank you received: 2
7 years 10 months ago #122802
by Bernd
Hi Mark, sorry for my late answer, yes it is possible to do this without a program running.
You can use the Gmoccapy button "change to selected tool" (don't know the right name, it is a button under the tool list menu), or use the MDI and write a Tn M6.
As soon as the window appears with the request to "please change to Tool Nr.n and click OK" the button on the controlpanel goe`s hot.
during this request message the spindle can not turn, and you are safe for tool-change.
Replied by Bernd on topic Retrofitting a 1986 Maho MH400E
RotarySMP wrote: Thanks Bernd, how do change a tool if there is no program running, does the Gmoccapy tool change button activate this pin? For example if you are just setting up and want to mount a touch probe?
Mark
Hi Mark, sorry for my late answer, yes it is possible to do this without a program running.
You can use the Gmoccapy button "change to selected tool" (don't know the right name, it is a button under the tool list menu), or use the MDI and write a Tn M6.
As soon as the window appears with the request to "please change to Tool Nr.n and click OK" the button on the controlpanel goe`s hot.
during this request message the spindle can not turn, and you are safe for tool-change.
The following user(s) said Thank You: RotarySMP
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
7 years 10 months ago #122866
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
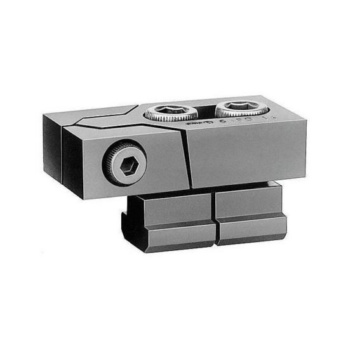
Merry Christmas to all. Hope you all had a nice family time yesterday or today, depending on tradition. I received a pair of AMF "Bulle" toes clamps, which are going to come in handy, along with a couple if other bits and pieces for the mill.
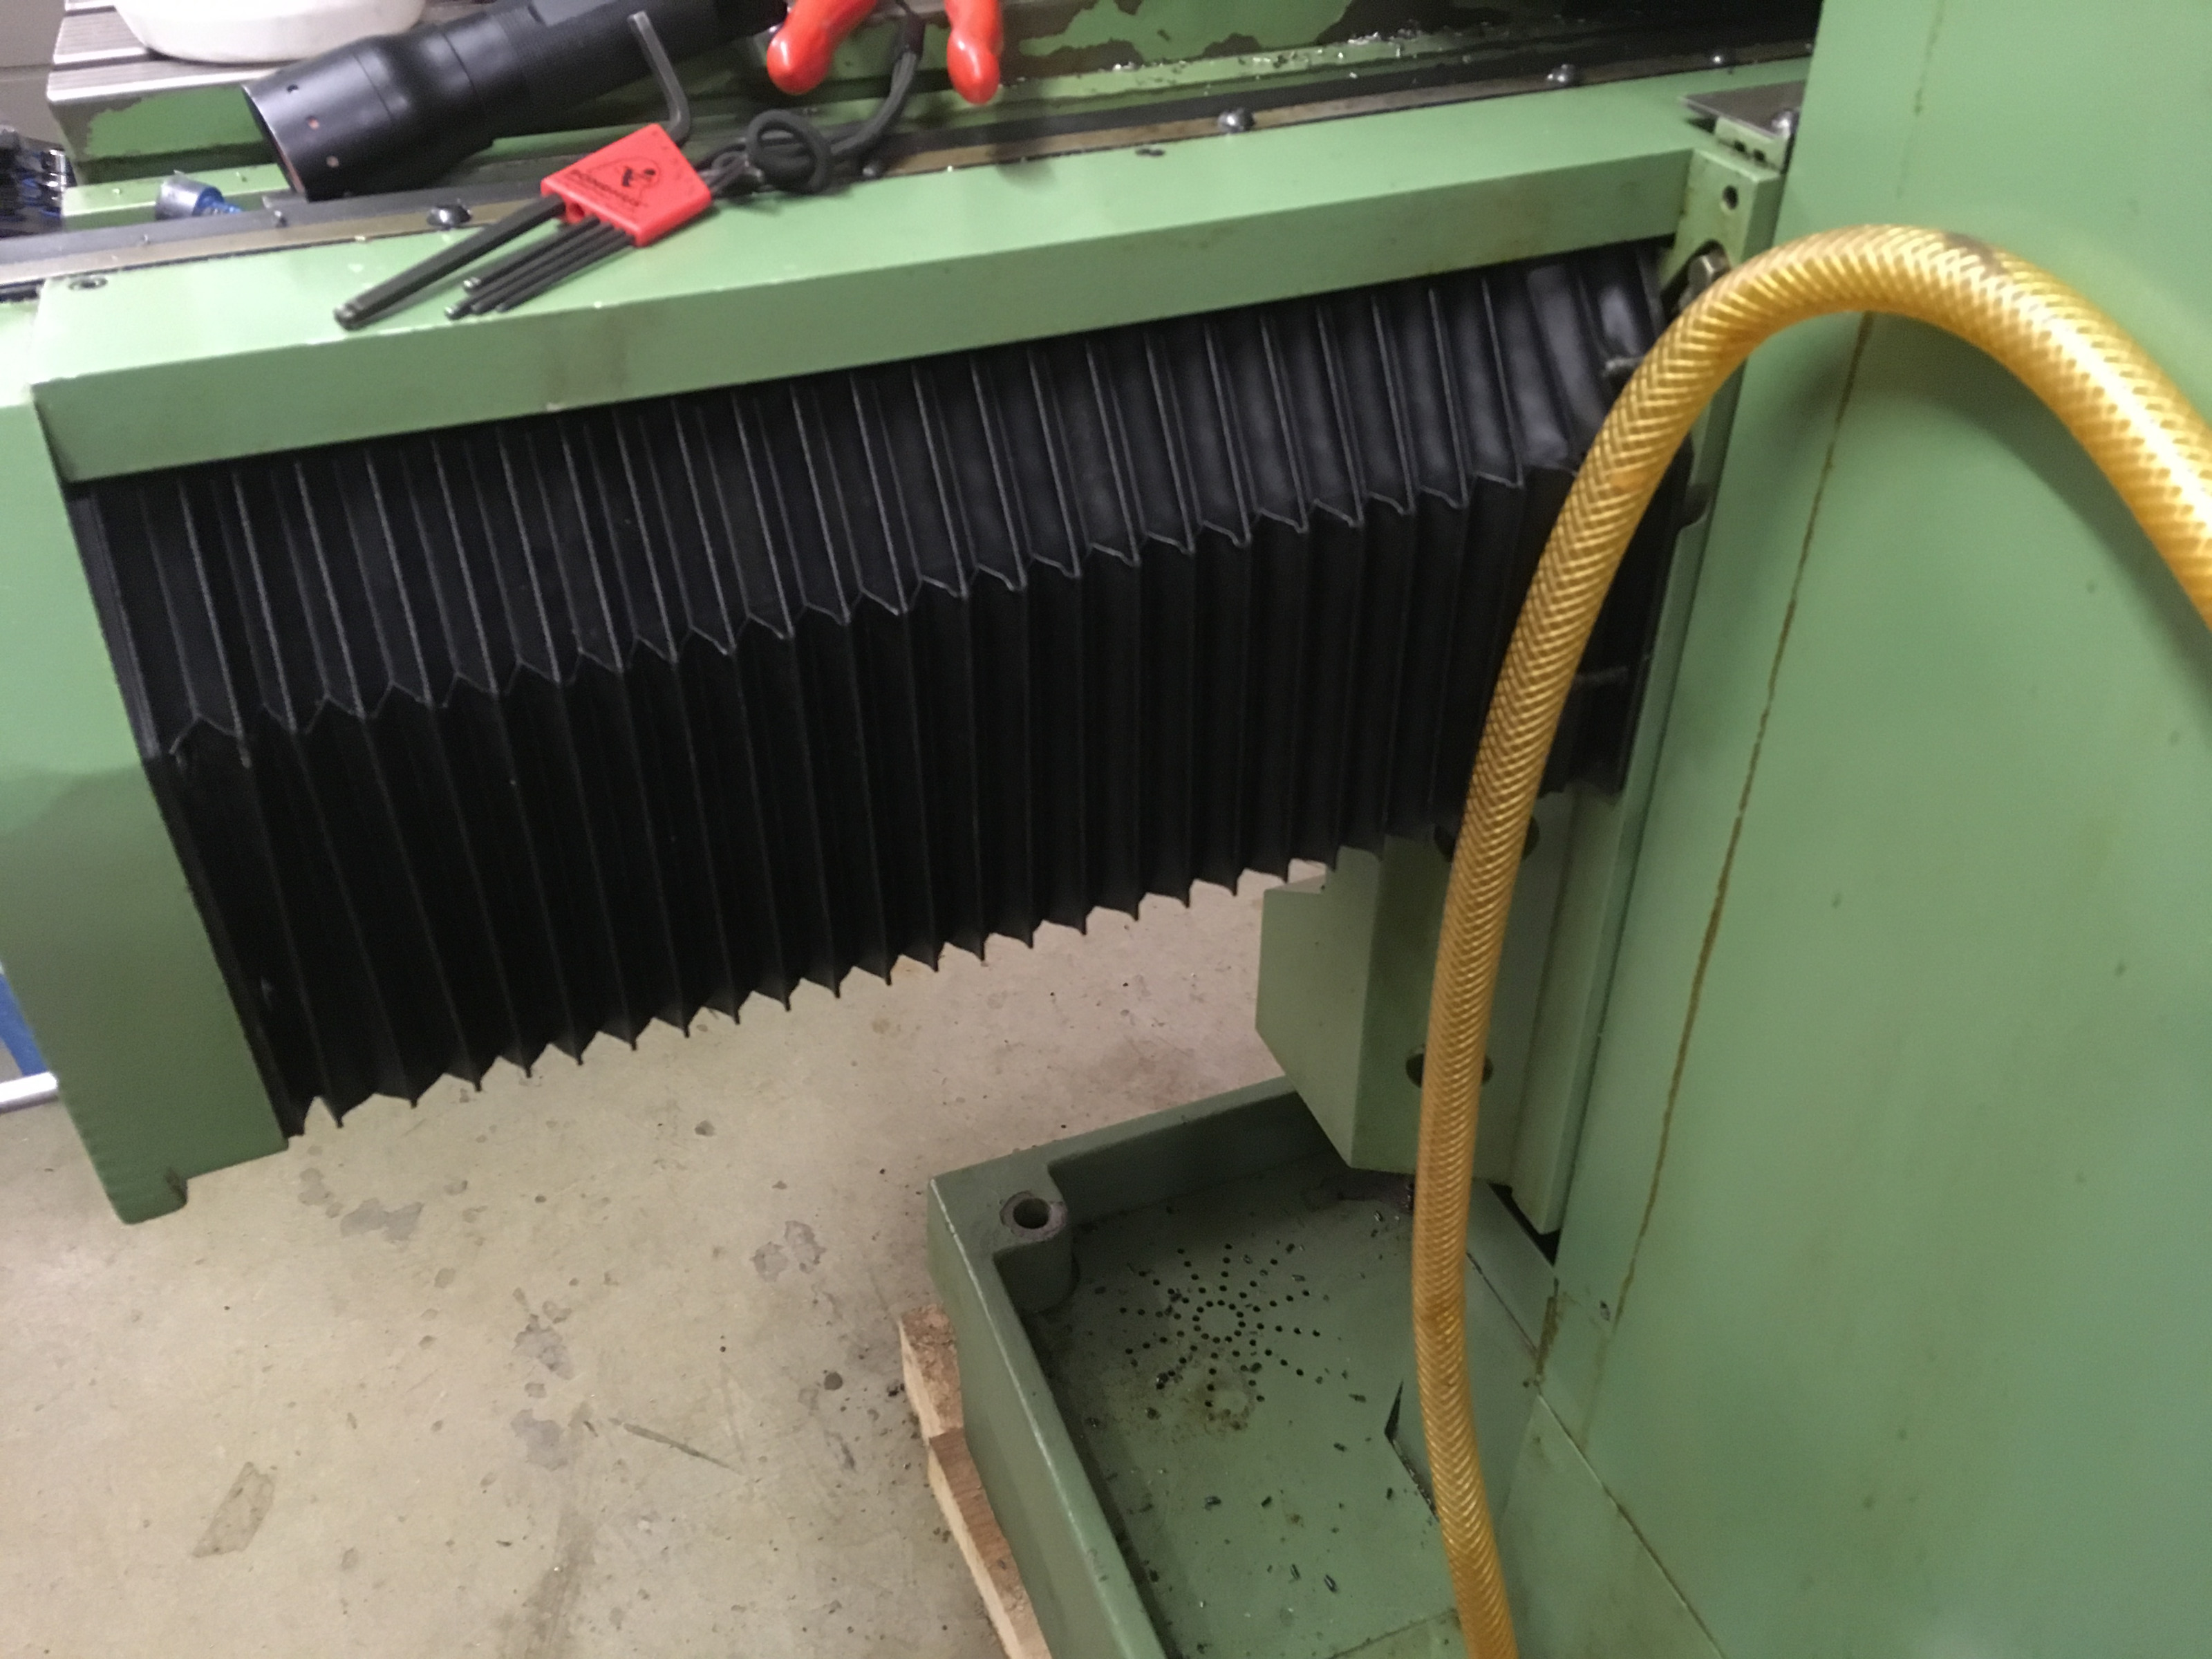
Thanks Bernd. I wanted to edit that into my HAL, but my chinese bellows arrived. I installed them (which is a real PITA) on the LH side, as the rear guard has to be installed at the same time, so you are working down in the gap between the transformers, and the guarding. This photo is from the RH side, and I had to take this back off a couple of times till I worked out the order of assembly of all the guards - the rear wall also gets sandwiched by the bellows mounts screws here.
But now all the guards are back on. Swarf tray and doors installed. The coolant which is in the machine is probably 20 years old and pretty gross, but I is working. I'll have to drain it and clean out the sludge and get some fresh coolant.
The replacement LH door which I bought from Ebay turned out to have the latch fittings 25mm away from mine (did MAHO ever make 2x the same thing?). Easy job to drill new holes for the lathe blocks and install them.
Thanks Bernd. I wanted to edit that into my HAL, but my chinese bellows arrived. I installed them (which is a real PITA) on the LH side, as the rear guard has to be installed at the same time, so you are working down in the gap between the transformers, and the guarding. This photo is from the RH side, and I had to take this back off a couple of times till I worked out the order of assembly of all the guards - the rear wall also gets sandwiched by the bellows mounts screws here.
But now all the guards are back on. Swarf tray and doors installed. The coolant which is in the machine is probably 20 years old and pretty gross, but I is working. I'll have to drain it and clean out the sludge and get some fresh coolant.
The replacement LH door which I bought from Ebay turned out to have the latch fittings 25mm away from mine (did MAHO ever make 2x the same thing?). Easy job to drill new holes for the lathe blocks and install them.
Moderators: piasdom
Time to create page: 0.727 seconds