
- Posts: 19899
- Thank you received: 4655
Hesitation between two consecutive G33 codes
- andypugh
- Offline
- Moderator
-

Less
More
9 years 4 months ago #94169
by andypugh
Replied by andypugh on topic Hesitation between two consecutive G33 codes
I wonder if you can use G76 with a combination of infeed and outfeed tapers?
I suspect not.
There is this:
www.wallacecompany.com/tmp/G76/
G76 with a taper option.
Looking at the standards the "vanish threads" are due to the die taper, and have a different (and variable) profile, so can't be single-point cut anyway.
I suspect not.
There is this:
www.wallacecompany.com/tmp/G76/
G76 with a taper option.
Looking at the standards the "vanish threads" are due to the die taper, and have a different (and variable) profile, so can't be single-point cut anyway.
Please Log in or Create an account to join the conversation.
- PCW
- Offline
- Moderator
-
Less
More
- Posts: 18115
- Thank you received: 5334
9 years 4 months ago #94172
by PCW
Replied by PCW on topic Hesitation between two consecutive G33 codes
But since G33 waits for index (at least that's what the docs say) , it will always pause at the beginning
so It may not be possible to use it the way you are trying to use it
(merging 2 G33s instead of a separate pass), that is because of the wait for index sync
you cannot be cutting at the beginning of G33
so It may not be possible to use it the way you are trying to use it
(merging 2 G33s instead of a separate pass), that is because of the wait for index sync
you cannot be cutting at the beginning of G33
Please Log in or Create an account to join the conversation.
- 10K
- Offline
- Premium Member
-

Less
More
- Posts: 142
- Thank you received: 33
9 years 4 months ago #94175
by 10K
Replied by 10K on topic Hesitation between two consecutive G33 codes
Here's a picture of the threaded pipe:
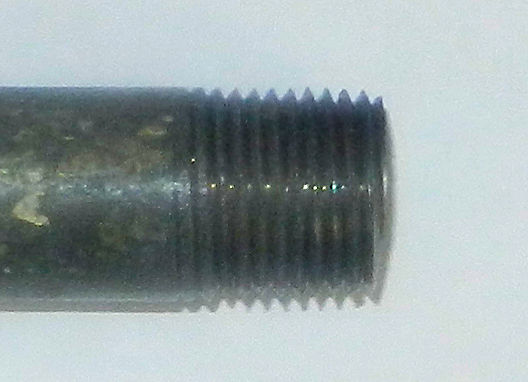
There's a somewhat puny thread about three threads from the left end. That's the transition between G33 commands. It's not too bad on this sample, since I ran at about 100 RPM. If I run the lathe faster, it's much more pronounced.
I agree that the vanish taper is an artifact of the pipe die, and that this cut is an approximation. However, some transition is needed, or the thread would have to be cut too long. A steeper taper can help make up the pipe joint if the tolerance between the pipe and fitting is a little off.
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
9 years 4 months ago #94179
by andypugh
Replied by andypugh on topic Hesitation between two consecutive G33 codes
Is there a problem with just retracting the tool?
Certainly with G76 this works fine and leaves no groove. The thread just ends.
Certainly with G76 this works fine and leaves no groove. The thread just ends.
Please Log in or Create an account to join the conversation.
- 10K
- Offline
- Premium Member
-
Less
More
- Posts: 142
- Thank you received: 33
9 years 4 months ago #94182
by 10K
Replied by 10K on topic Hesitation between two consecutive G33 codes
The main part of the thread must have a taper of 3/4" per foot. I think that G76 will only taper at the end of a straight cut. I could be mistaken. When I first started looking at writing code to thread pipe, I wanted to use G76, since I already had written code to do threading. I read posts here and other places that said G76 could not be used.
Please Log in or Create an account to join the conversation.
- cmorley
- Offline
- Moderator
-
Less
More
- Posts: 7368
- Thank you received: 2181
9 years 4 months ago #94266
by cmorley
Replied by cmorley on topic Hesitation between two consecutive G33 codes
You used to be able to create a continuous , variable pitch , variable diameter thread:
wiki.linuxcnc.org/cgi-bin/wiki.pl?JMKsFusee
Seems a setting is wrong or a possible bug (which would be easy to not exercise).
What version of linuxcnc are you using?
Chris M
wiki.linuxcnc.org/cgi-bin/wiki.pl?JMKsFusee
Seems a setting is wrong or a possible bug (which would be easy to not exercise).
What version of linuxcnc are you using?
Chris M
Please Log in or Create an account to join the conversation.
Time to create page: 4.262 seconds