I want to mill steel with this machine.

More
6 years 4 months ago #170035 by Marcodi
Hey all,

I am looking for some advice before breaking things.

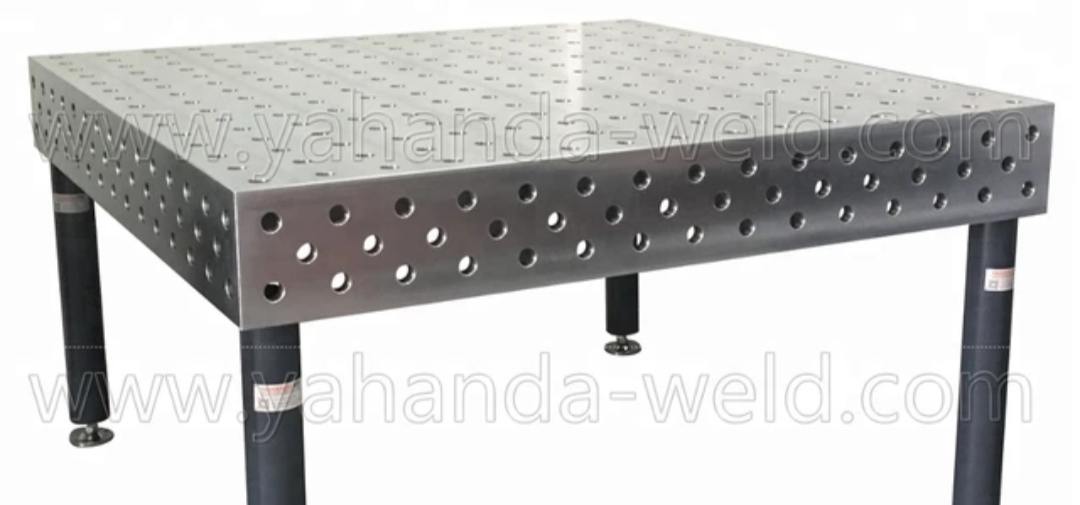
I want to make a 3d welding table like this:


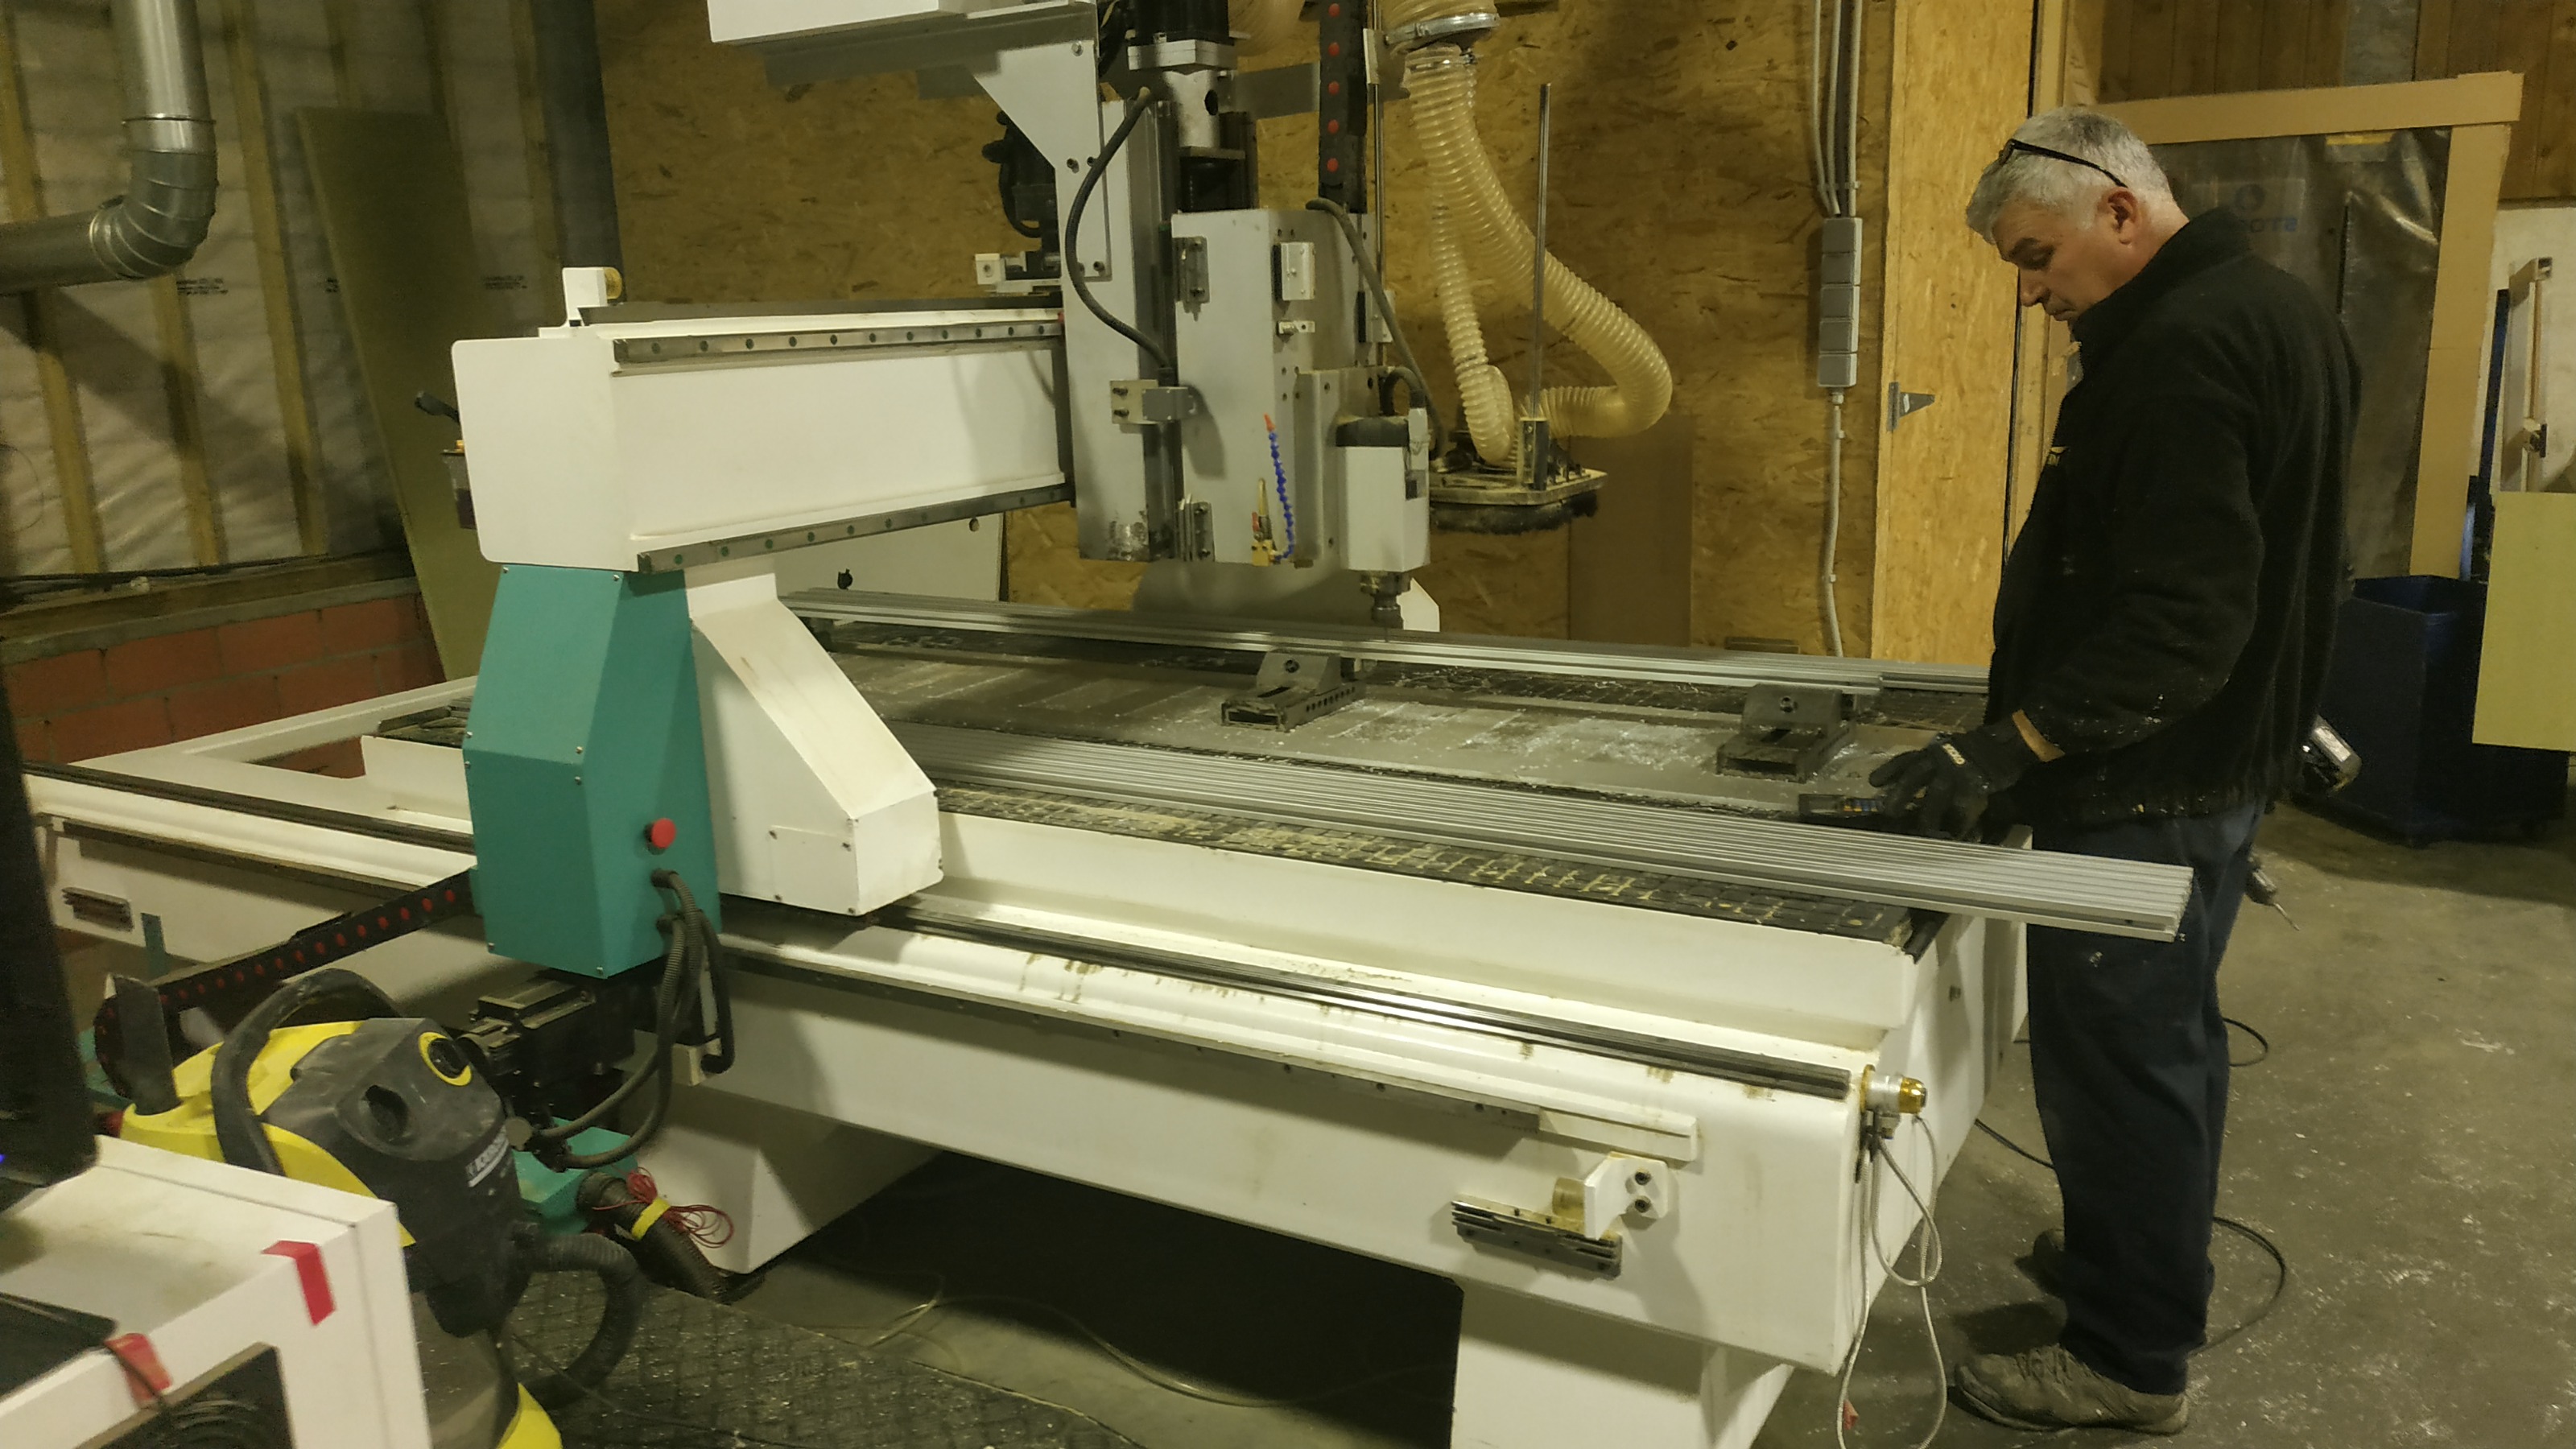
The idea is I cut out the rough form with my plasma machine. Thickness is 10mm steel or 20mm steel . So far I am good but than to get the precision I need I want to put it on my router which looks like this:


Machine weight 3500kg bridge weight 1000 kg. The z axis is made out of cast aluminium. Motors on all axis are 1000w servos. My spindle that I would use is a 4.5kw spindle. I could also do this with a 9kw ATC that I am buying, but don't want to hurt that one.

I would position this plasma burnt metal plate with all holes already plasma burned on the router and than precision cut all the holes.

I would like to know if it would be at all possible to do this. I have a full waterbed with 2 sprinkles on the machine so cooling is not an issue. It can take as long as needed to make it, I just don't want to break any of the motors or guide rails or something like that.also I don't care for tool life.

Could someone recommend me if it can be done and if so how deep and how much I can chip of with this kind of machine. I will use gwizard than for the correct spindle speeds and so on.

Thanks.

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago #170040 by tommylight
Not really, not without the end result costing way more that a new table.
Issues:
The machine on the picture (router) is made for wood and wood only. It will do aluminium with some feed tweaking and light passes, easily. It can also do metal with some fancy nice milling cutters and adjusted feeds, but it will suffer a lot, everything will suffer in it, even the rails and carriages.
The metal cut with a plasma machine will be hardened at every cut face, the parts you will try to mill, and very, very fast find out that HSS end mills will just melt making a mess, carbide ones require higher cutting forces that that machine can not provide, so will end up melted again.
After all this, please do give it a try with some lighter material and different end mills, it will be very hard to find a balanced feed and speed combo that will work, but it should be possible.
Personally i would not try it at all, i would point my efforts towards finding some cut speeds for the plasma machine that will produce acceptable holes.
The following user(s) said Thank You: RacingMat

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago #170044 by Marcodi
I know the machine is not build for it indeed.

I was having in mind to go with 0.5mm down and take 0.1mm from the side with a 6mm carbide mill 4flanges at a slow feed rate.

That was my idea to not hurt the machine. But as I have no experience in steel aside milling the top of my clamps which went surprisingly well , drilling holes in steel and cutting through the occasional mispositioned screw, my knowledge of steel milling is 0.

Secondary option is to make the whole table out of aluminium. The machine doesn't give a flinch when taking 3mm stepover 15mm deep with a 10mm endmill.

I doubt that I can cut with the plasma that accurately on 0.1 through 10mm steel. Plasma is 160A Chinese.

Please Log in or Create an account to join the conversation.
More
6 years 4 months ago - 6 years 4 months ago #170074 by rodw
As Tommy said, the plasma cut material will be so hard you won't mill it easily if at all.

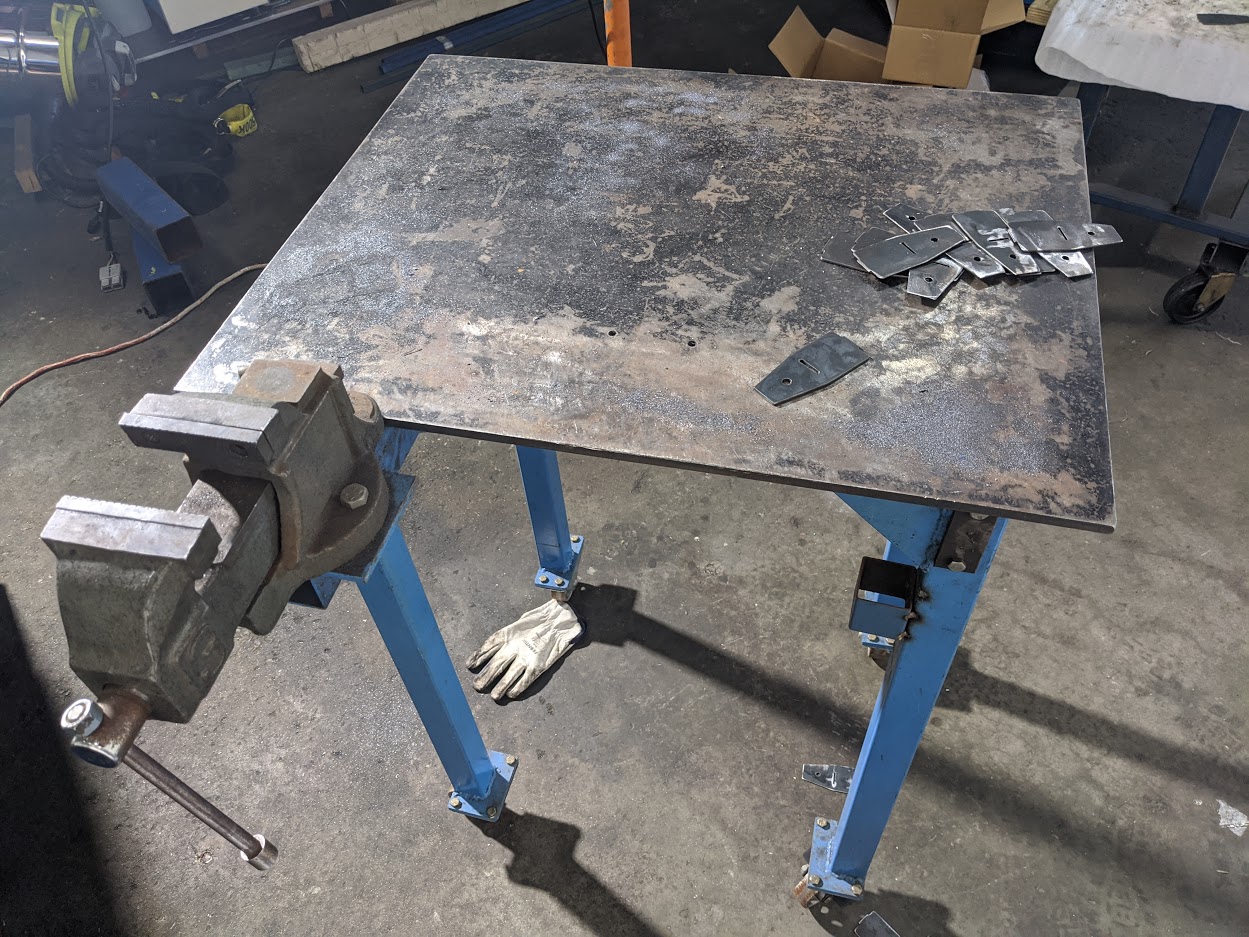
I really don't get the attraction of those tables, just use a flat plate and when its required, drill and tap a hole in it where you need to hold something down, leave a 50mm overhang of the top to allow for clamps and include a receiver to accept a 50mm square section that has a vice attached so you can slide it in and take it away as required.

Seeing I have been using it today


I got my laser cutter to cut out the top, gussets and caster mounting plates. Top is 10mm and it would be nicer if it was thicker but then I would never had been able to lift it.

I made this a while ago and don't use it a lot so I've only ever had to drill 2 holes so far :)
Last edit: 6 years 4 months ago by rodw.

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago - 6 years 4 months ago #170076 by machinedude
i think the biggest problem with VFD spindles is they are all high speed spindles. the tool paths for aluminum are light and fast cuts for high speed machining applications. why because aluminum is the only type of metal you can get away with running at a high speed with and high feed rates. when you get into steel it requires much lower speeds even when using carbide and the feed rates are a lot slower as well. like everyone else has said the plasma process will case harden every cut made and that is tough to get under before the material is somewhat normal again.

one thing about the moving gantry machines is they are not meant to rough or hog any kind of metal period but with some fancy tool paths you can get away with not destroying the machine because you can limit the load on the tool to fit the rigidity of the machine. you just have to be mindful of tool loads. but like i said before you have to have the right speeds and feeds to even get into trying steel and enough torque at those speeds to get anywhere. HSM advisor will give you a good layout of the load created with your cuts and materials your working with to test out so you can predict what will happen before it even hit the machine.

not sure how much abuse a phenolic table can stand there so that's something to think about as well.
Last edit: 6 years 4 months ago by machinedude. Reason: more information

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago #170081 by bbsr_5a
if you use HSC bits and a HELIX toolpath this mashine can do the job easy
if the mashine has the precition you need it will do it

make a SUB that takes the xy of the drill
and does a incremental G2/G3 Zfor helix P for full turns down <0,5mm
www.linuxcnc.org/docs/html/gcode/g-code.html#gcode:g2-g3

its as easy as that

Please Log in or Create an account to join the conversation.

Time to create page: 0.220 seconds
Powered by Kunena Forum