
- Posts: 34
- Thank you received: 18
Injection molding
- Ritterchen
- Offline
- Junior Member
-

Less
More
11 months 1 week ago #338864
by Ritterchen
Replied by Ritterchen on topic Injection molding
Yes sure, here is the code attached. Most of it runs on the timers (Block-no) and Sensors.
The temperature is not implemented in this version jet.
Mainly to control the piston (plunger) and the closing mechanics.
Here are the electronics to get an idea. Yes its messy/ unnecessary complex.
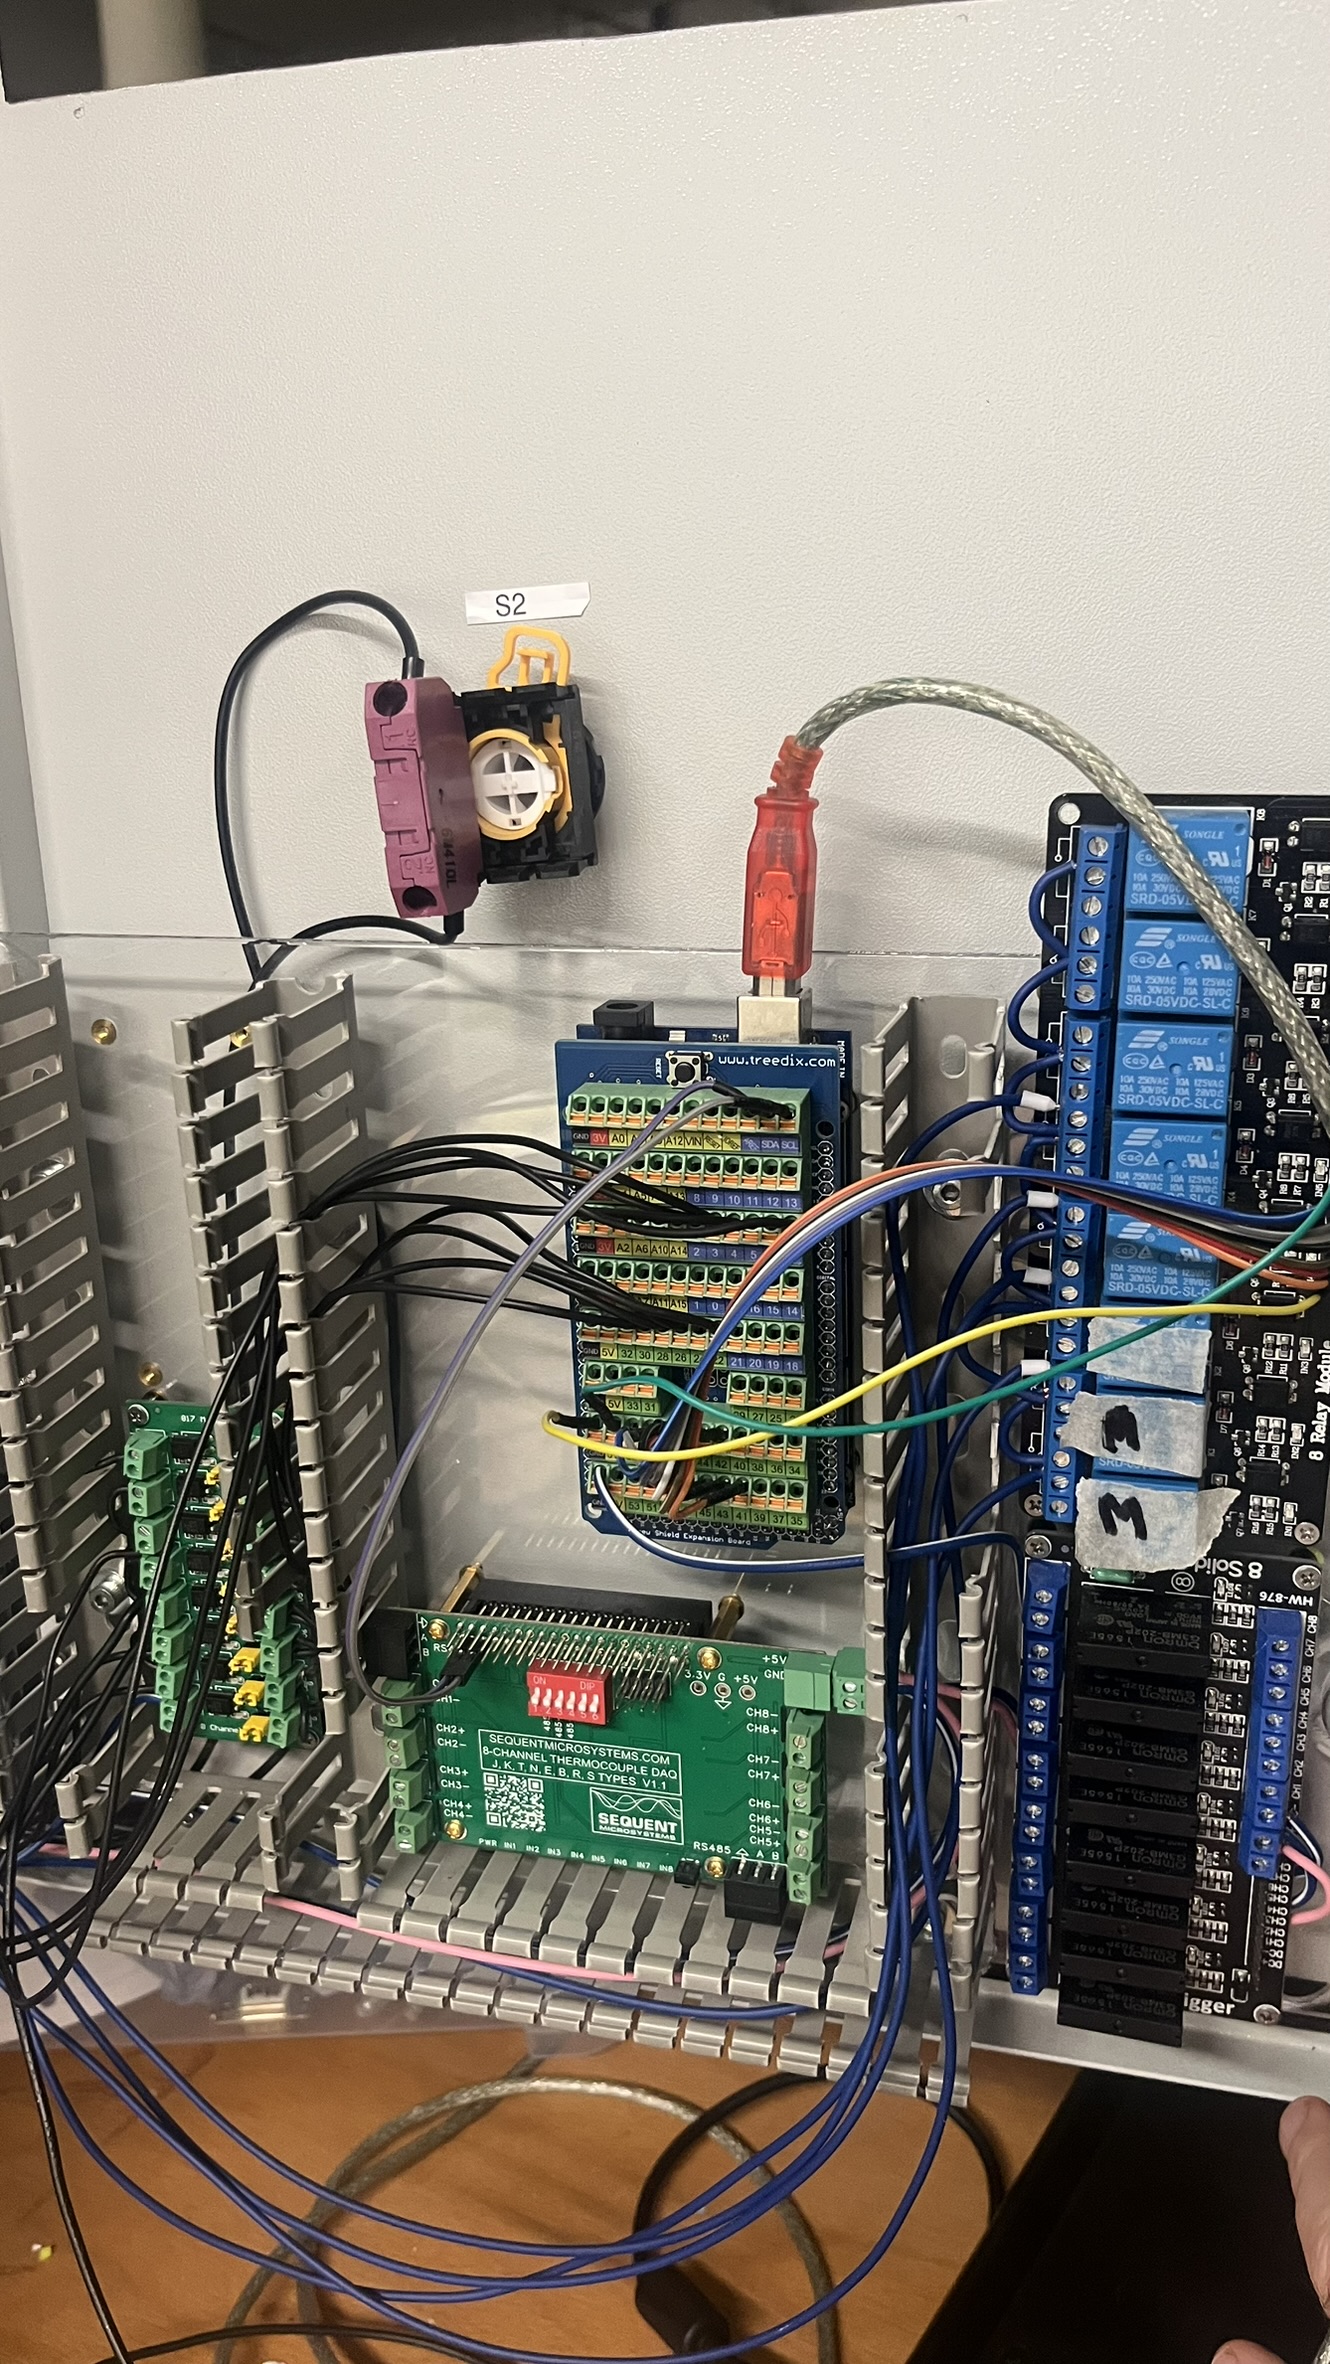
The temperature is not implemented in this version jet.
Mainly to control the piston (plunger) and the closing mechanics.
Here are the electronics to get an idea. Yes its messy/ unnecessary complex.
The following user(s) said Thank You: vre
Please Log in or Create an account to join the conversation.
- vre
- Offline
- Platinum Member
-

Less
More
- Posts: 612
- Thank you received: 17
11 months 1 week ago - 11 months 1 week ago #339085
by vre
Replied by vre on topic Injection molding
I think i will use something like you but with better mcu like esp32-s3 or an sbc like rpi5(only for the better user interface)
Last edit: 11 months 1 week ago by vre.
Please Log in or Create an account to join the conversation.
- Haras_abdrt
- Offline
- New Member
-

Less
More
- Posts: 1
- Thank you received: 0
2 months 3 weeks ago #348487
by Haras_abdrt
Replied by Haras_abdrt on topic Injection molding
Hello, good afternoon. I came across your post and wanted to ask you for some advice because I’m dealing with a very similar situation.
At the company I work for, we have an old Arburg 220-75.250 injection molding machine from the late 1980s. The floppy disk drive is no longer working, and I have been asked to find a way to get the machine back into operation.
I’ve been researching the machine, its control system and possible solutions, and from what I’ve seen so far, I’m starting to think that instead of trying to repair the original control, the better option might be to replace the control system and modernize the machine, potentially using something like LinuxCNC or another modern industrial control platform.
However, I have quite a few questions about how to approach a project like this.
First of all, how would you approach the retrofit from a technical point of view? What information would you consider essential to identify before starting?
I’m particularly unsure about the electrical side. How do you determine what the existing connections and signals are supposed to do? Is there normally an electrical schematic or I/O documentation that can be used to map the original controller’s inputs and outputs? If the original documentation is missing, how would you go about identifying and tracing the signals?
Could the existing sensors and switches on the machine be reused with a modern controller, or would they normally need to be replaced? For example, can the original position sensors, pressure sensors, limit switches, temperature sensors, etc. be connected directly to a modern I/O system, or does it depend on their signal type and voltage?
I’m also wondering about the hydraulic system. Would the original hydraulic valves and proportional valves normally be controllable by a modern system, or would these components also have to be replaced? How would you determine what type of signals the original valves require?
The same question applies to the injection and screw-position control. How would you interface a modern controller with the existing servo motors, drives, encoders or position feedback systems, if the machine has them?
Another important point is safety. How would you normally integrate the existing safety circuits, emergency stops, door switches, safety relays, etc. into a modern control system? Would you keep the original safety architecture wherever possible, or would you recommend replacing the safety system as part of the retrofit?
I’d also like to understand how you determine the required I/O. Is there a standard procedure for creating an I/O list for an old injection molding machine before designing the new control system?
Finally, if you have done a similar retrofit, I’d really appreciate any advice about the practical side of the project: what components you would keep, what you would replace, what information you would try to obtain from Arburg, and what mistakes or problems you would specifically look out for before starting.
If you don’t mind, I’d also be very interested in seeing any wiring diagrams, I/O lists, documentation, examples or photos from a similar retrofit that you could share.
Thanks a lot for your time. Any advice would be greatly appreciated.
Please Log in or Create an account to join the conversation.
- robh
- Offline
- Premium Member
-

Less
More
- Posts: 111
- Thank you received: 24
2 months 3 days ago #349090
by robh
Replied by robh on topic Injection molding
this topic is grate so watching this closly to see how you solve this
i also have a nigribosi machine around 1998 eara , before they went full PLC type etc currently the conotrol keeps needing TLC on its many PCB boards due to age and drift , always down to the way it monitors position and control of its rams
in this machine there are a number of proportional valves , i looked at other controls out there but they are mostly aimed at VFD driven pumps and not many proportional valve outputs
mine has two proportional on the pump block
one for Flow and one for pressure , these work together during differant operations during the cycles to keep energy use down etc
also when the machine is first turned on, they use the platen valve block and pump in full flow to heat up the oil faster so no preheaters are needing only the pump is used.
valve on the screw carriage to control distance and speeds seems to be a standard vale and they must use the pump to control the speed in pump flow. and they seem to do this for afew other things, where only 1 thing works at one time,
one on the molding machine platen is proportional doing distance and speeds for the multi point open and shut speeds and distance for open and close strokes, this would be due to the fact you can do ejection while platten is still opening by seting the 1st ejectoin distance start
also one on the ejection plate to set the distance and speed for ejecting the part from the mold must be a proportional as works during the high flow high presure on the plattern if enabled to eject during open stroke.
looking at it, the same seems to be on the screw for the screw speed control, not sure how they are controlling the back pressure on the screw and screw injection profile settings.
i had through about using linuxcnc also as alot can be done in hal easy, not that much to address in a molding machine, more how you control its cycle in its little fucntion blocks as such.
mine has a safty relay for the estop buttons , not sure what else they routed through it
for safty guards, they seem to read these in on the control, the ones on the guard door and must work in the corrrect sequence when opening or closing the door or it does alarm out with guard out of sequence, i assume as on this machine you can move the safty switch and open the door extra day light which is good for loading in bigger tools over head
the control also has options for things like core pullers normaly 3/4 can be used
also air ejection is on this machine
also ability to read thermo couples from a mold tool
also the control also controls the hydrulic tank temp but turning on and off a valve that pushes the oil through the heat exchanger for cooling from the cooling water coming into the machine.
as already pointed out, alot of the machine works on timers and waits for one section to finish before it starts the next, is alot the user can input and change during the machine working cycles. also a good handfull in the machine setup pages that are fixed like time out for screw back and screw injection etc, along with max presure for platten open and close
they seem to be Bosh or Atos alot for the valves i find in nigri bosi
lube cycle tends to be done on the number of completed ejection cycles
i do have some wiring diagrams and hydrulic i can share if it would help in understanding , can also share some control screen shots for reff
Please Log in or Create an account to join the conversation.
- robh
- Offline
- Premium Member
-
Less
More
- Posts: 111
- Thank you received: 24
2 months 3 days ago #349091
by robh
Replied by robh on topic Injection molding
oh and on mine it has linear resistive measuring devices to track potion and they use this to control the proportional valve also.
Please Log in or Create an account to join the conversation.
Time to create page: 0.173 seconds