Rounding the corners off

More
9 years 1 month ago #98950 by new2linux
Replied by new2linux on topic Rounding the corners off
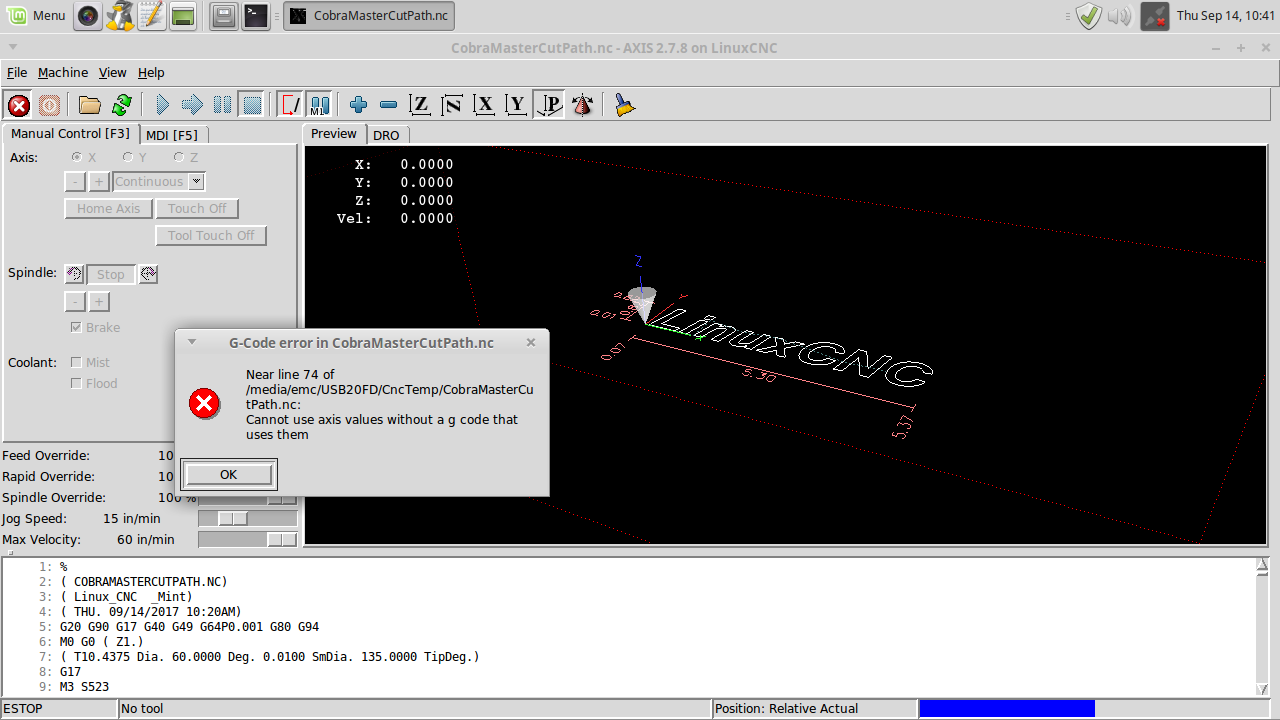
I have edited the post (the G64P0.001 is saved along with G20 G17 G90 G40 G49 G80 G94) with some success, linuxcnc will get hung up (see screen shot, & ref gcode in attachments)
I just am not shore what I am looking for, with a error like that. naturally the machine will not move, so an't tell if the G64 is working. When I edited the post, I did not use find and replace this time. The 1st time used find and replaced and there was some g code copied more than one time. Any advise is welcomed. I trust the "max_acceleration=10.0, " is in the ok range.

many thanks!

Please Log in or Create an account to join the conversation.

More
9 years 1 month ago - 9 years 1 month ago #98955 by Todd Zuercher
That alarm is because on the 73rd line of the file you have:
Code:
X2.2879 Y-.4525
With no motion command (G0,G1,G2...)
G0,G1,G2... are all modal commands so they don't have to be put on every line, but the G80 command cancels them, so a new one must be commanded before a new axis command is given.

So to fix your problem either add a G0 after every G80 or remove the unnecessary G80s.

The preamble codes are only really needed at the very start of the file, so inserting them all at every tool change is a little excessive. I also usually put a motion command on every line that makes a movement rather than trying to rely on their modal state.
Last edit: 9 years 1 month ago by Todd Zuercher.
The following user(s) said Thank You: new2linux

Please Log in or Create an account to join the conversation.

More
9 years 1 month ago #98956 by new2linux
Replied by new2linux on topic Rounding the corners off
Many, many thanks Todd, I only edited the post, the rest of the code was generated from within the software. From reading your comment, it would appear that the G80 needs to go. My hope is that the post will automate this part. I will study the file more.

many thanks!

Please Log in or Create an account to join the conversation.

More
9 years 1 month ago #98960 by new2linux
Replied by new2linux on topic Rounding the corners off
Bobcad, called and suggested the following post:

File Attachment:

File Name: Linux_CNC_...CPst.txt
File Size:25.35 KB


I am in need of 2nd opinion, the help has been good from bobcad with the exception of the post processor, the 1st part cut had this same issue 3 to 5 weeks ago, I am wondering if my post processor person is in over there head. I have been transparent with my info about G64P0.001, it appears in the post. I will try a pic again of the cut. 1.38 mb pic would not load. Will try fresh post to see if pic will work.

many thanks!!

Please Log in or Create an account to join the conversation.

More
9 years 1 month ago - 9 years 1 month ago #98963 by new2linux
Replied by new2linux on topic Rounding the corners off
Just going to try the pic by its self. the left shows the rounding, the rt side shows sharp corners, left is the gcode "start from here in the code" all ready existing geometry, full part of code. the rt is started with the same file edited all geometry that was not of the part in question. Will try pic again later, 1.38 mb. will try to compress or zip.

Edit: The zip file worked. The top left is the same geometry and tool path as rt side, left lower is roughing pass for larger tool. This pic is of an "E" & a "T" (they lay down at an angle a bit), I know the right is cut the best but is rotated 90*, the radis is at the bottom edges of the "e" and the very end of the "t". Hope this is easier to follow.

many thanks!!

2nd Edit: If it would help, I would run thru the gcode to it comes to the exact radius in question(post the info on that line, by following linux cutter path) if that would help isolate the issue?
Last edit: 9 years 1 month ago by new2linux. Reason: add zip file, a question

Please Log in or Create an account to join the conversation.

More
9 years 1 month ago - 9 years 1 month ago #99003 by new2linux
Replied by new2linux on topic Rounding the corners off
These are some screenshots of the area of the code in question, just left these for bobcad people. I know the feed rate was varied, (I just ran the "override to 0, so it would stop") so is not exactly the same.

many thank!

Edit: Many thanks, I went back to bobcad and have a post that works!! I very thankful to the forum, Todd Zuercher and andypugh for there accurate timely information. I am not shore at what feed rate (currently tried 10"/min) will be to fast to suit.

Many thanks!!
Last edit: 9 years 1 month ago by new2linux. Reason: update

Please Log in or Create an account to join the conversation.

Time to create page: 0.426 seconds
Powered by Kunena Forum