Strange behaviour after program stop button pressed in axis

More
6 years 5 months ago #168979 by cadcam
Yeah I get that. I wouldn't mind doing some more testing on this... but don't have time, so I will just remember to pause and e-stop next time.

I find it hard to believe tool change and G43 is causing this issue.

I've never seen it before on 2.7, but then I moved to 2.8 for G84 as soon as it was available... so that must be years ago now.

I know this is open source, use at you own risk.. blah blah, but this sort of bug isn't acceptable in a machine shop.. Lets hop it gets resolved sooner than later.

Please Log in or Create an account to join the conversation.

More
6 years 5 months ago #169010 by RichJordan
Linuxcnc has enabled me to do so much. It is a pretty fabulous open source project. And apart from this bug it has not failed to impress me.

But motion after the stop button was pressed felt like treachery!

I can't be sure that the issue was with my remapping of M6 but like i say stop button works perfectly when I don't call M6 and the associated remapping for a touch probe after tool change that ships with linuxcnc. I have another machine which I haven't remapped tool change and stop button behaves properly there.

Please Log in or Create an account to join the conversation.

More
6 years 4 months ago #170337 by tommylight
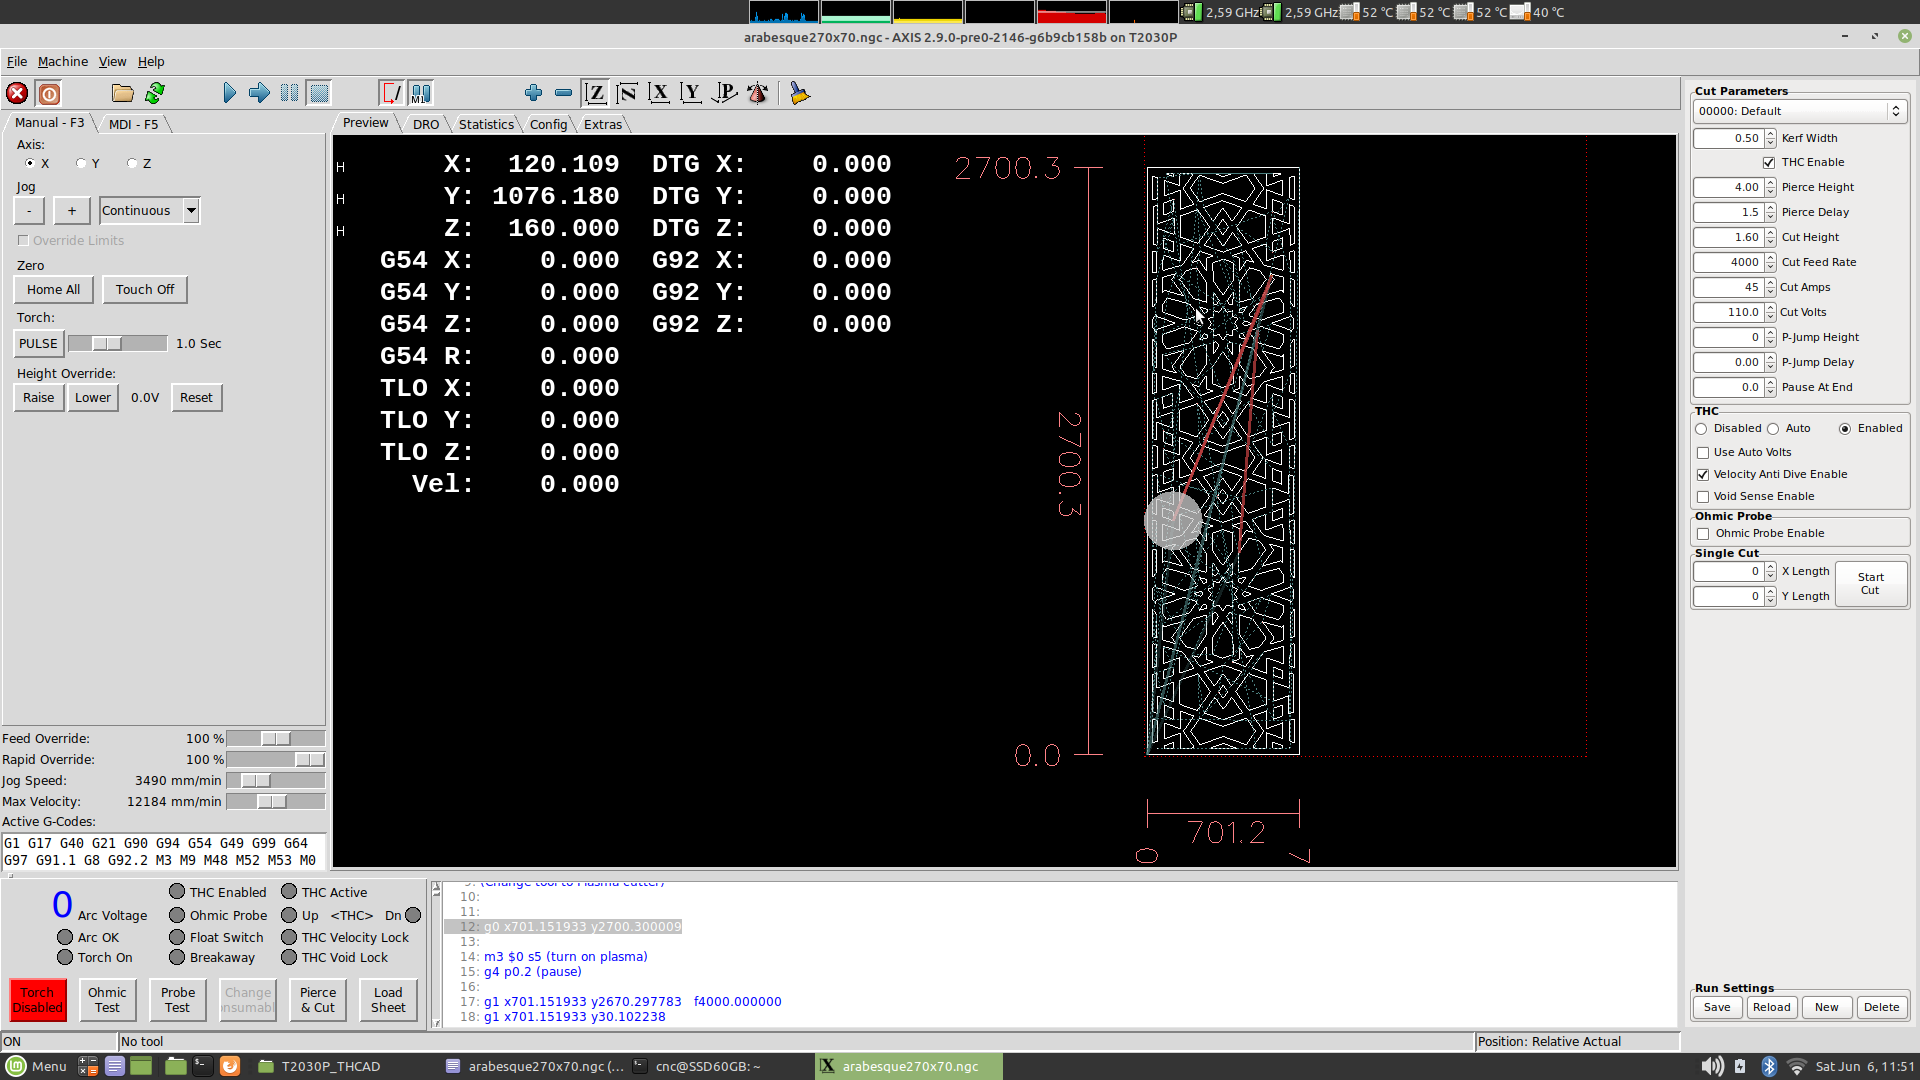
Noticed the same issue on 2.9 build 2133 and 2146, using 3 different configs on the same machine, the PlasmaC, toma_thc, and a plain standard config.
The issue:
-start LinuxCNC, home the machine, load gcode file, press start,
-while in rapid, press stop or ESC
--what should happen is the machine should stop,
--what happens is the machine will start moving back, both X and Y axis, to some random point that is not random as it can always be found in the gcode, but that point will change, already had two positions that the machine goes to with the same config and same gcode file.
In the attached screenshot, there are two dark red/brown lines, the upper part of those lines is where the stop was pressed, while the bottom of those lines is where the machine actually stopped. Same config, same gcode, just reloaded the gcode, homed the machine and run. Both of those end positions can be found in gcode.

The same procedure using Gmoccapy with the same gcode and plain config is not present, so this affects only axis GUI so far.

Please Log in or Create an account to join the conversation.

More
More
6 years 4 months ago #170387 by PCW
github.com/LinuxCNC/linuxcnc/issues/865

RMU has a fix that seems to work but may have undesired side effects
If you are building from source you might try adding emCTaskPlanReset()

int was_open = taskplanopen;
emcTaskPlanClose();
++ emcTaskPlanReset();

at about line 261 in src/emc/task/emctask.cc
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.
More
6 years 4 months ago - 6 years 4 months ago #170390 by tommylight
Thank you, PCW,
I am aware of that as i did read everything here, but the explanation on the original post was lacking, so i did some test today and it is repeatable and the return point is always somewhere in the gcode. The original poster named it as a dangerous issue, and rightfully so.
I use this for plasma cutters, so it has no real side effects as at rapid the torch is always up.
Last edit: 6 years 4 months ago by tommylight. Reason: More info

Please Log in or Create an account to join the conversation.

Time to create page: 0.216 seconds
Powered by Kunena Forum
