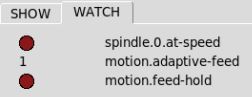
Hi everyone
Sometimes the machine stalls when probing the tool length. Usually at the start of a program which is good so I can just rerun everything and it will be fine. But I kinda wanna know why this happens so I can trust the machine again
This is what I do:
Use MDI (or ngc program) to issue an "T1 M6" command
This calls the tool length measuring macro "messen.ngc"
File Attachment:
File Name:
messen.ngc
File Size:1.52 KB
I added some debug lines to see where exactly the program stalls.
1, 2, 3 -> stall
So the machine is stuck @ line 34 "G1 Z2.5 F500 (frei fahren)"
What is confusing me is when I check the machine status
It tells me the command is: "G38.2 Z-10 F25 (messen fein)"
But the debug message "4" never shows which is before that command.
Also the status shows "current_line 34" which would be a different command (the one above).
Could it be that the probe is jumpy and that is cancelling line 34?
Is there a way can see if it stalled because of a bouncy probe?
(I'm using debouncing in hal already with a value of 3)