
- Posts: 8
- Thank you received: 0
LinuxCNC python
- kwanlokto
- Offline
- New Member
-

Less
More
11 months 1 week ago #338912
by kwanlokto
LinuxCNC python was created by kwanlokto
I am looking to leverage
linuxcnc.org/docs/html/config/python-interface.html
to build an API which will be able to perform basic machine functions like homing the axis, measuring tool length and running gcode. Out of curiousity do you guys know of any github repos or any open source projects I can reference to start this project?
- cmorley
- Offline
- Moderator
-

Less
More
- Posts: 7368
- Thank you received: 2181
11 months 1 week ago #338913
by cmorley
Replied by cmorley on topic LinuxCNC python
Do you mean like this ?
linuxcnc.org/docs/devel/html/gui/qtvcp-l...ml#_code_action_code
or something like this?
linuxcnc.org/docs/devel/html/man/man1/axis-remote.1.html
linuxcnc.org/docs/devel/html/gui/qtvcp-l...ml#_code_action_code
or something like this?
linuxcnc.org/docs/devel/html/man/man1/axis-remote.1.html
- JT
- Online
- Administrator
-

Less
More
- Posts: 1107
- Thank you received: 598
- Donb9261
- Offline
- Elite Member
-

Less
More
- Posts: 169
- Thank you received: 103
7 months 15 hours ago #345017
by Donb9261
Replied by Donb9261 on topic LinuxCNC python
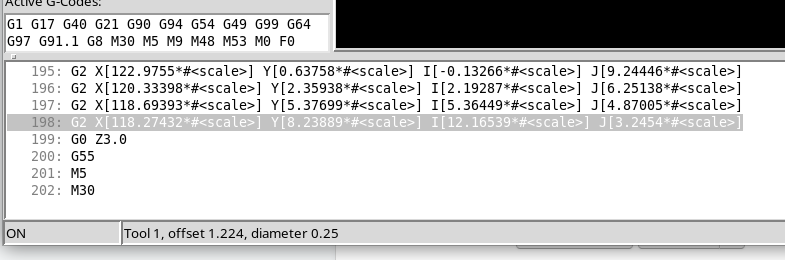
Consider the following gcode lines:
197: G2 X[118.69393*#<scale>] Y[5.37699*#<scale>] I[5.36449*#<scale>] J[4.87005*#<scale>]
198: G2 X[118.27432*#<scale>] Y[8.23889*#<scale>] I[12.16539*#<scale>] J[3.2454*#<scale>]
199: G0 Z3.0
200: G55
201: M5
202: M30
LCNC reads/runs all the way down and stops at G0 Z3.0. And the program never resets. I stat.red_line, stat.motion_line, current_line, and see that motion_line is actually the line it is stuck on. In this case, it would be line 199. After 202: there is an EOF carraige return. I tried this using Axis, and all the others. I get the same result these do.
M30 should read and rewind to first line in the program which is RS-274 GCODE. But, no matter what I try, nope.
Any ideas?
Thanks,
Don
- Donb9261
- Offline
- Elite Member
-
Less
More
- Posts: 169
- Thank you received: 103
7 months 15 hours ago - 7 months 14 hours ago #345018
by Donb9261
Replied by Donb9261 on topic LinuxCNC python
Last edit: 7 months 14 hours ago by Donb9261.
- tommylight
- Offline
- Moderator
-
Less
More
- Posts: 22011
- Thank you received: 7491
6 months 4 weeks ago #345080
by tommylight
Replied by tommylight on topic LinuxCNC python
@Don,
Do those replies belong on this topic, or am i missing something?
Do those replies belong on this topic, or am i missing something?
Time to create page: 0.256 seconds