How to set current machine position manually?

More
9 months 2 weeks ago #341394 by WobblyZ
Hello, I have a machine with handwheels that can be moved with the power off. For reasons that I won't get into, I want to be able to set everything up manually, move the tool to the part origin and then directly tell linux CNC that my tool is at X0 Y0 Z0.25" from home and then touch off the part.

I don't see a shortcut in AXIS to do this? Is there g code that I can put in the MDI to tell it where the current machine position is?

Thanks.

Please Log in or Create an account to join the conversation.

More
9 months 2 weeks ago #341398 by rodw
Axis has a touch off features for each axis. Its not really any different to a manual mill when you set up your DR0. Use a edgefinder to locate X0 and  then touch off with an offset of 0.5 x radius. eg for a 6 mm dia edge finder, touch off at x -3 and repeat for Y axis y -3 (for top left hand corner)
then roll a drill or milling cutter (say 10mm dia) under the tool until you feel you have light drag. Then touch off Z +10
There are cheap Chinese edge finders but the Starrett is a class on its own by comparison

www.amazon.com/Edge-Finder-Single-End-0-...ps%2C474&sr=8-3&th=1

Please Log in or Create an account to join the conversation.

More
9 months 2 weeks ago #341402 by WobblyZ
From what I can see, touch off sets the part origin relative to the current position, but linuxCNC doesn't know what the real current position is because I moved it with the handwheels and not the jog function. So when I touch off, it thinks I'm still at home position and sets the part origin relative to home which causes the tool paths to be outside the machine limits.

Is there no way to set the current position relative to home directly? I can't use the jog function because my computer is too slow and the machine keeps moving long after I've let go of the mouse.

Please Log in or Create an account to join the conversation.

More
9 months 2 weeks ago #341403 by rodw
if you expect a CNC machine to be able to be moved without using the CNC control to move it you are outside the normal paradigm.
You could try immediate homing without limit switches but I think that may restrict you motion to just one quadrant.
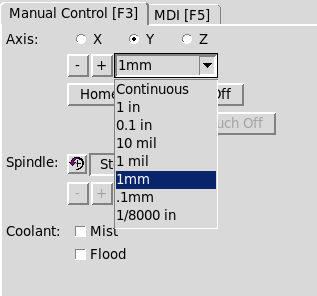
Try changing the jog scale when jogging in the gui.
There is something to be said for a good pendant

Please Log in or Create an account to join the conversation.

More
9 months 2 weeks ago - 9 months 2 weeks ago #341410 by NWE
Not sure if I caught on, am I correct:
1. You're jogging the machine by turning handwheels attached to each axis while the motors are powered off,
2. You want the resulting position to be your starting point.

Which GUI are you using? I experimented in Axis, I can do touch-off and enter a value instead of 0 to tell it where it is starting. You will need to know how far from home you jogged it, and enter that value in touch off for each axis.
EDIT:
Sorry, I was wrong. That will not work. Entering an offset moves the part away from the tool. I think my brain needs sleep soon.

Lacking any other options to reliably jog it, you might use MDI commands to send it to the touchoff point. If it is in incremental mode 'jogging' might be less complicated compared to absolute mode depending how quick you are with math.

Surely switching the jog increments from 'continous' to a specific value would suffice, and be easier than MDI commands. It should then only move the specified distance each time you press a key, if it continues anyway, I would suspect a problem with the keyboard auto-repeat on your system.
Last edit: 9 months 2 weeks ago by NWE.

Please Log in or Create an account to join the conversation.

Time to create page: 0.244 seconds
Powered by Kunena Forum