Lathe spindle index only?

More
1 year 7 months ago #323367 by 109jb
Replied by 109jb on topic Lathe spindle index only?
jtrantow - Good to hear from someone with the same hardware to convert. I think what I will try first is a slotted disk with as many slots as I can reasonably fit on it with one deeper slot and 2 optical slot detectors. It may wind up less slots than you have and since I would only have one detector reading them, I will have less counts per rev but will see how it goes. I like the idea of the slot detectors because they don't have any moving mechanical parts like a rotary encoder. It should also be less involved to implement than a rotary with the sprockets, belts, brackets etc. Maybe I'll wind up with a rotary but I'm going to give this a try.

Thanks Again.

Please Log in or Create an account to join the conversation.
More
1 year 7 months ago #323369 by 109jb
Replied by 109jb on topic Lathe spindle index only?
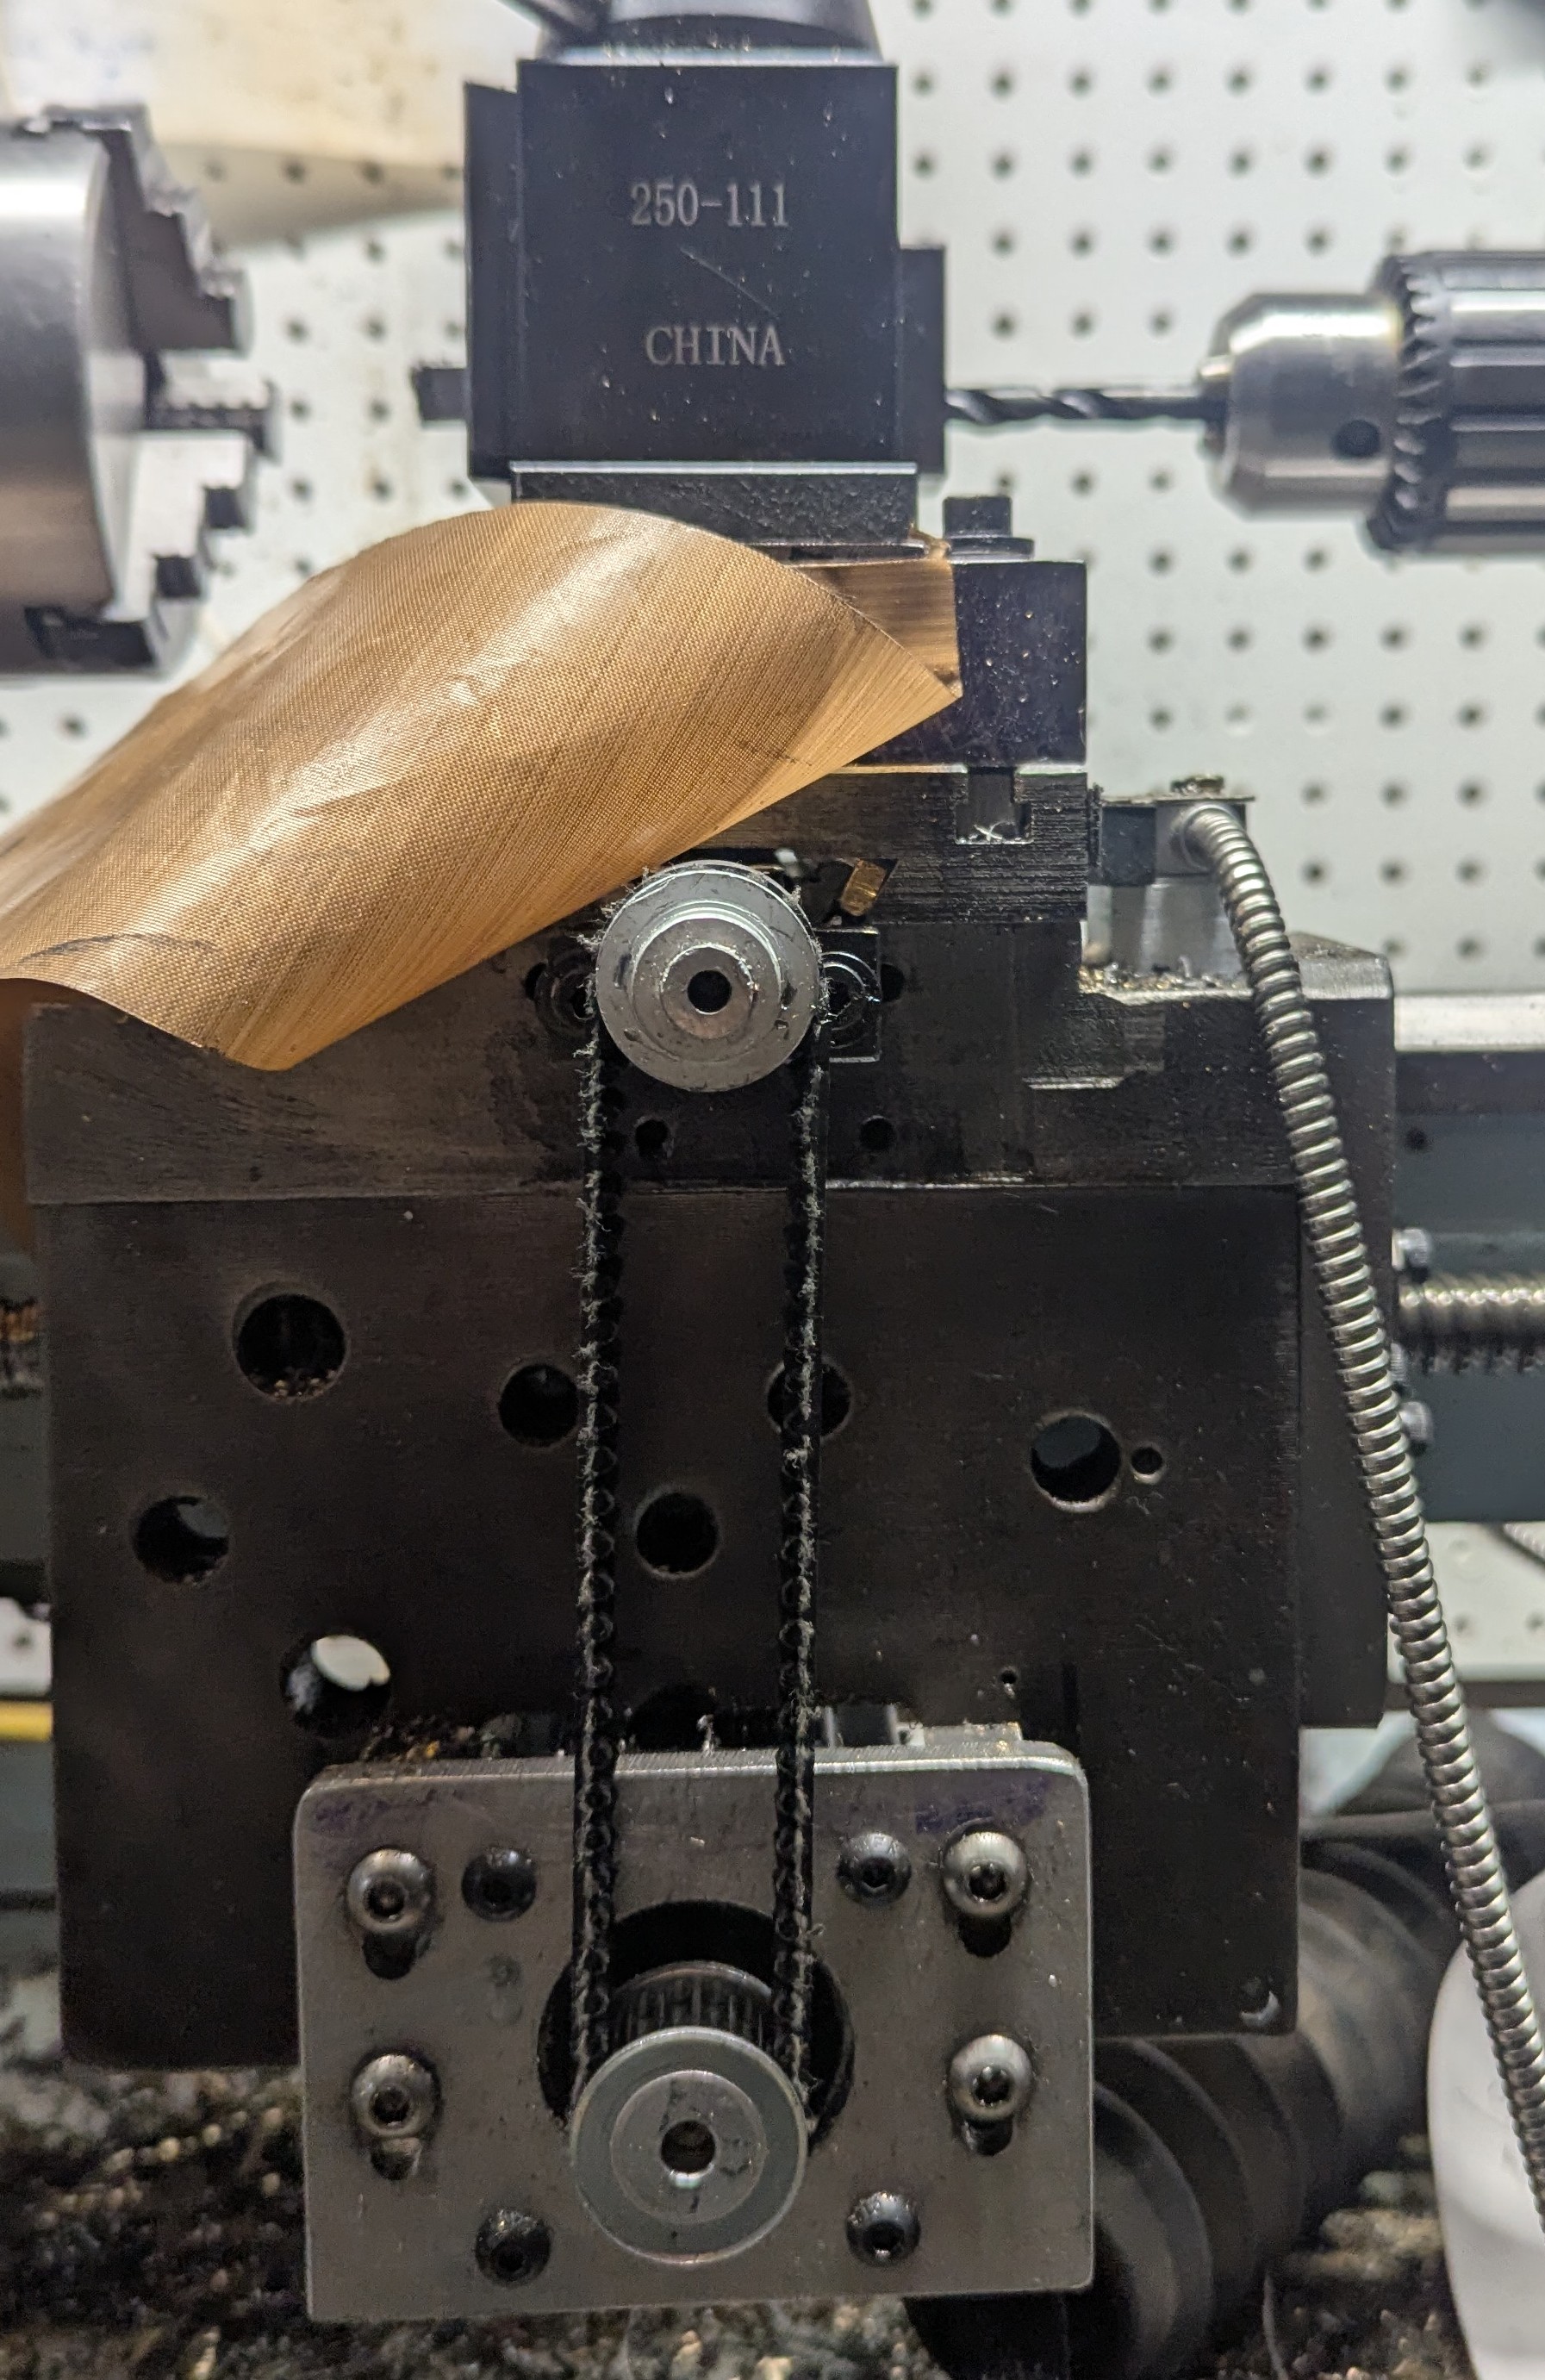
Oh. Forgot to mention. I got a 12mm ballscrew for the cross slide. Hoping it is small enough to make it work.

Please Log in or Create an account to join the conversation.
More
1 year 7 months ago #323426 by jtrantow
Replied by jtrantow on topic Lathe spindle index only?
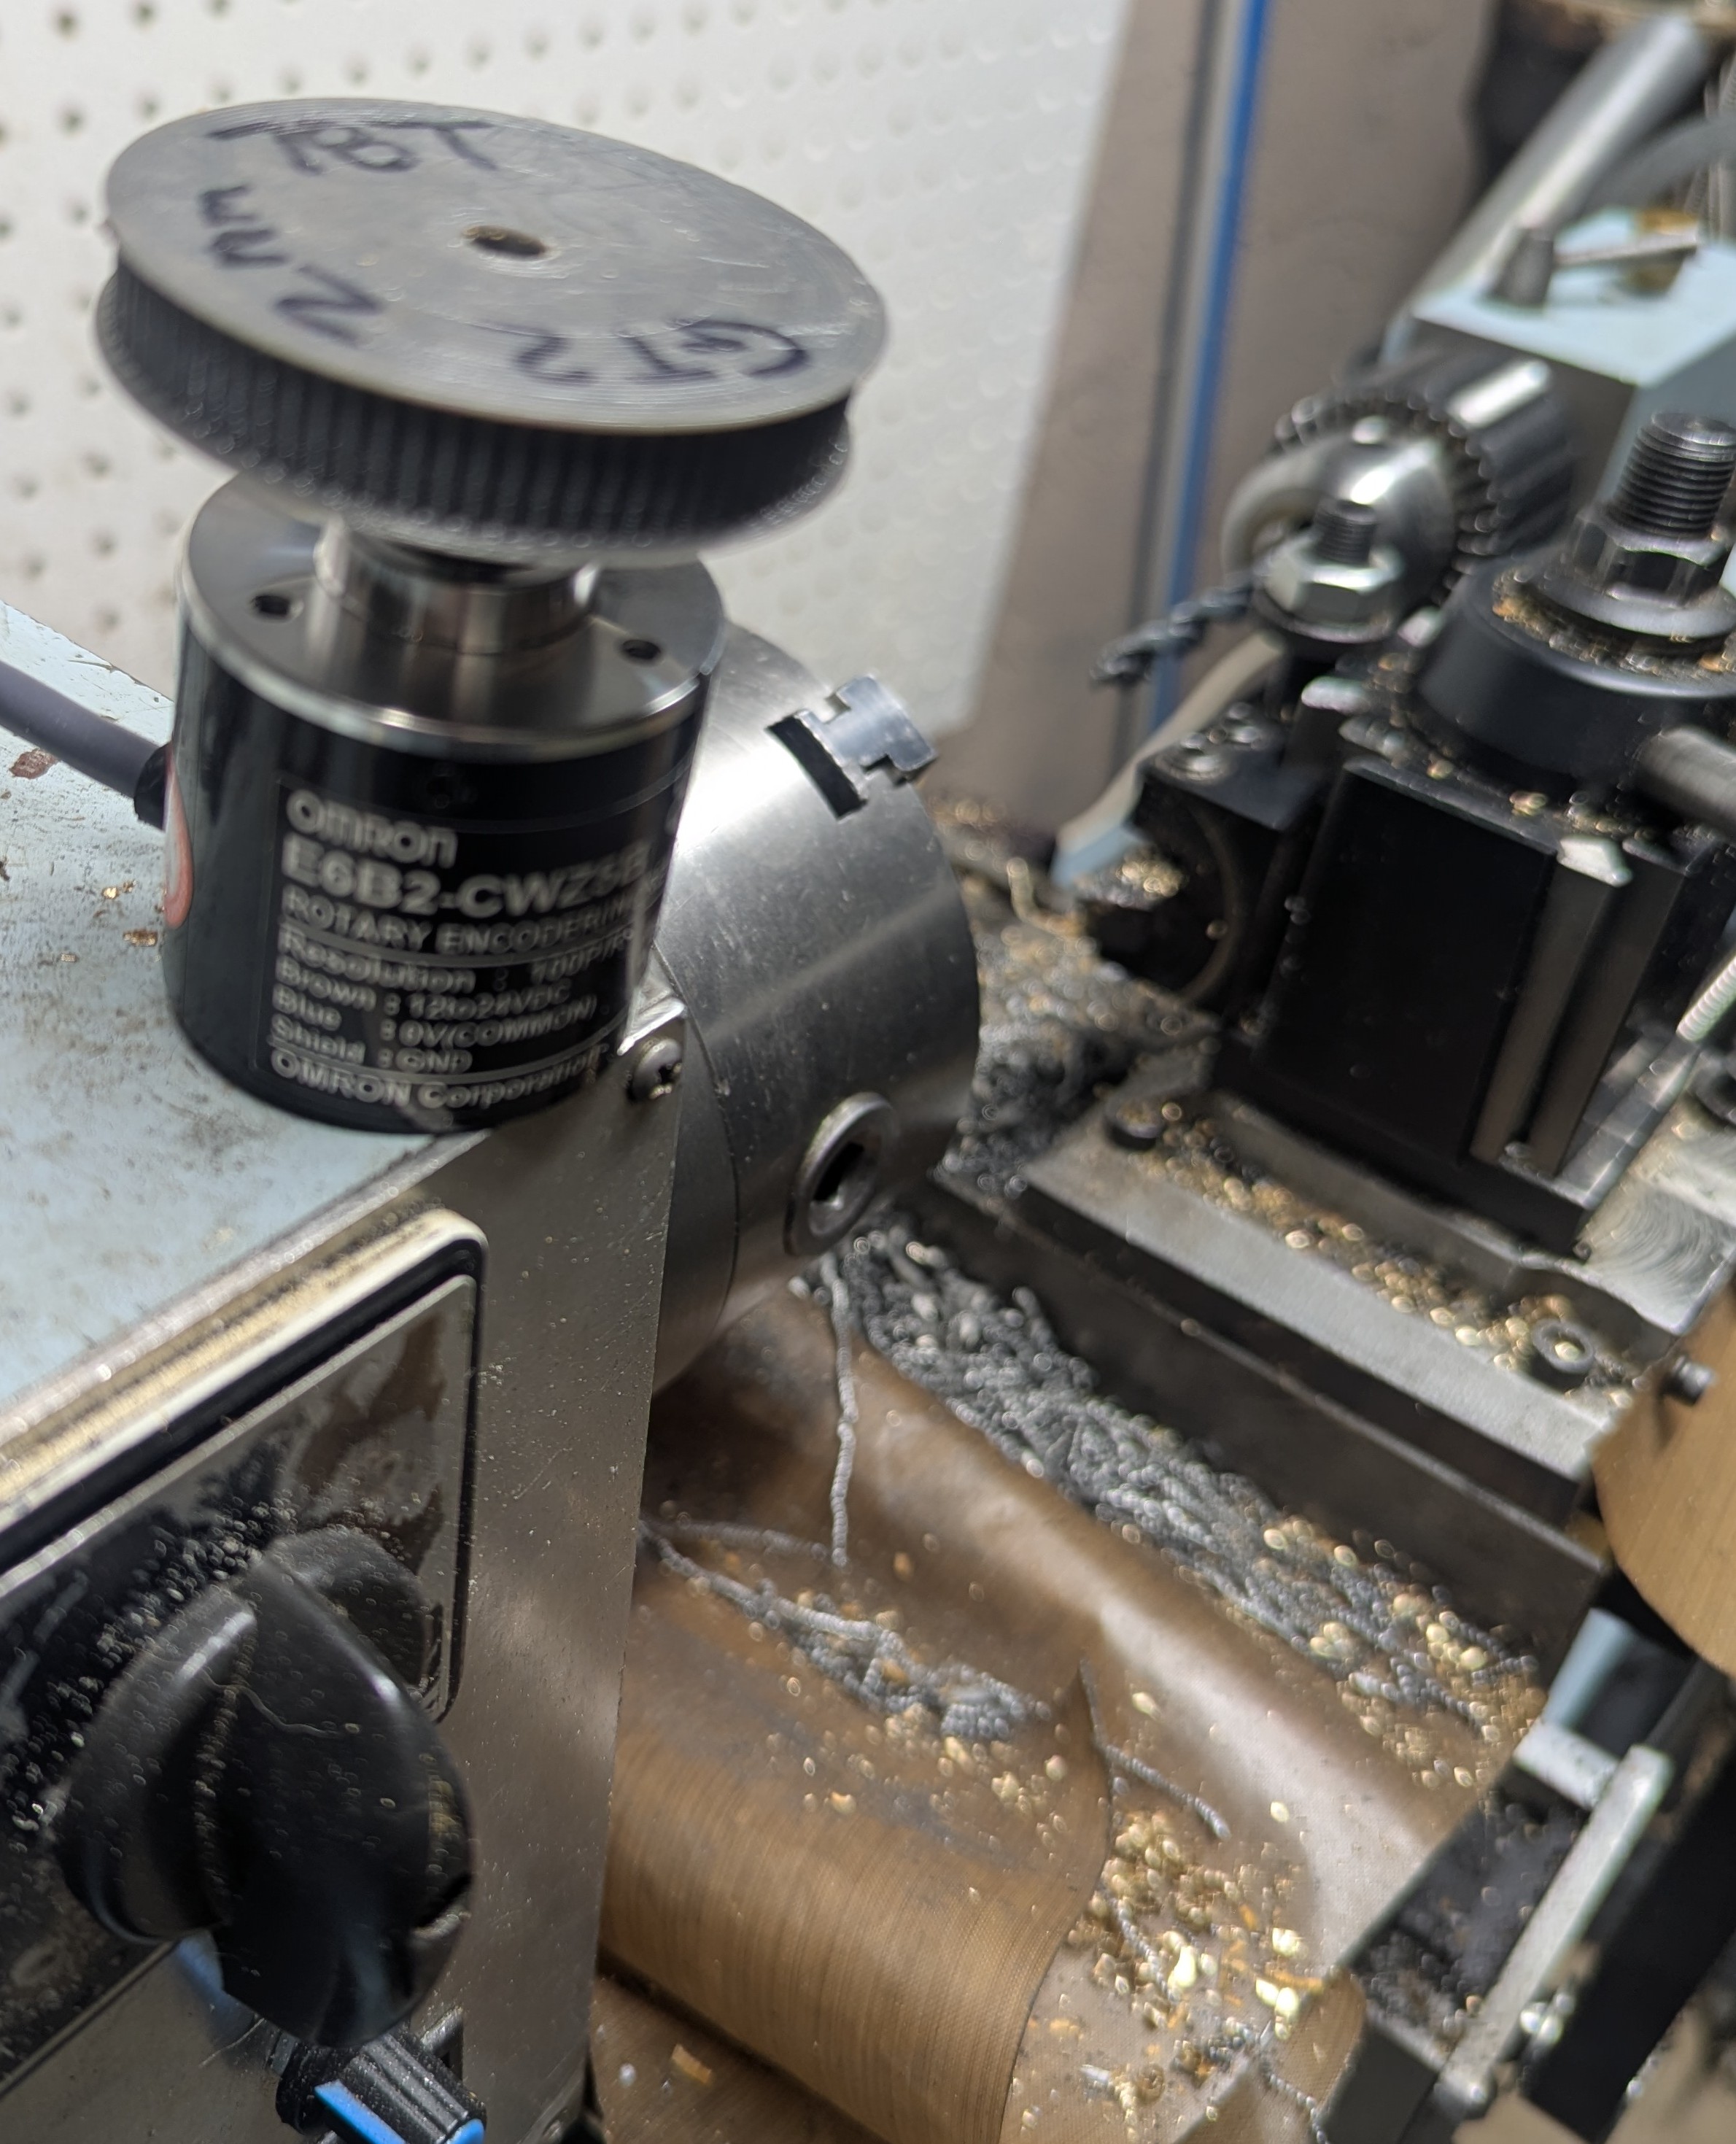
You can get a quadrature signal using the same slots and offsetting another detector approx 1/2 the spacing. It can be a little finicky to adjust but gives you 4x resolution and lets you track direction too. ( Important if you want to use spindle like a dividing head)

I added another detector to pick up index, missing tooth should be fine.

I expect the omron install will be a lot easier. I could probably just wrap a belt around the spindle shaft. The omron encoder spins with imperceptible drag to the spindle just about any belt or string is enough to spin it. I also have an omron encoder that I can position on my mill drawbar for rigid tapping. Janky but functional. It worked with a rubber band while I waited for a gt2 belt. After the mill install I ordered another for lathe but haven't gotten around to installing it.

Please Log in or Create an account to join the conversation.
More
1 year 7 months ago - 1 year 7 months ago #323431 by jtrantow
Replied by jtrantow on topic Lathe spindle index only?
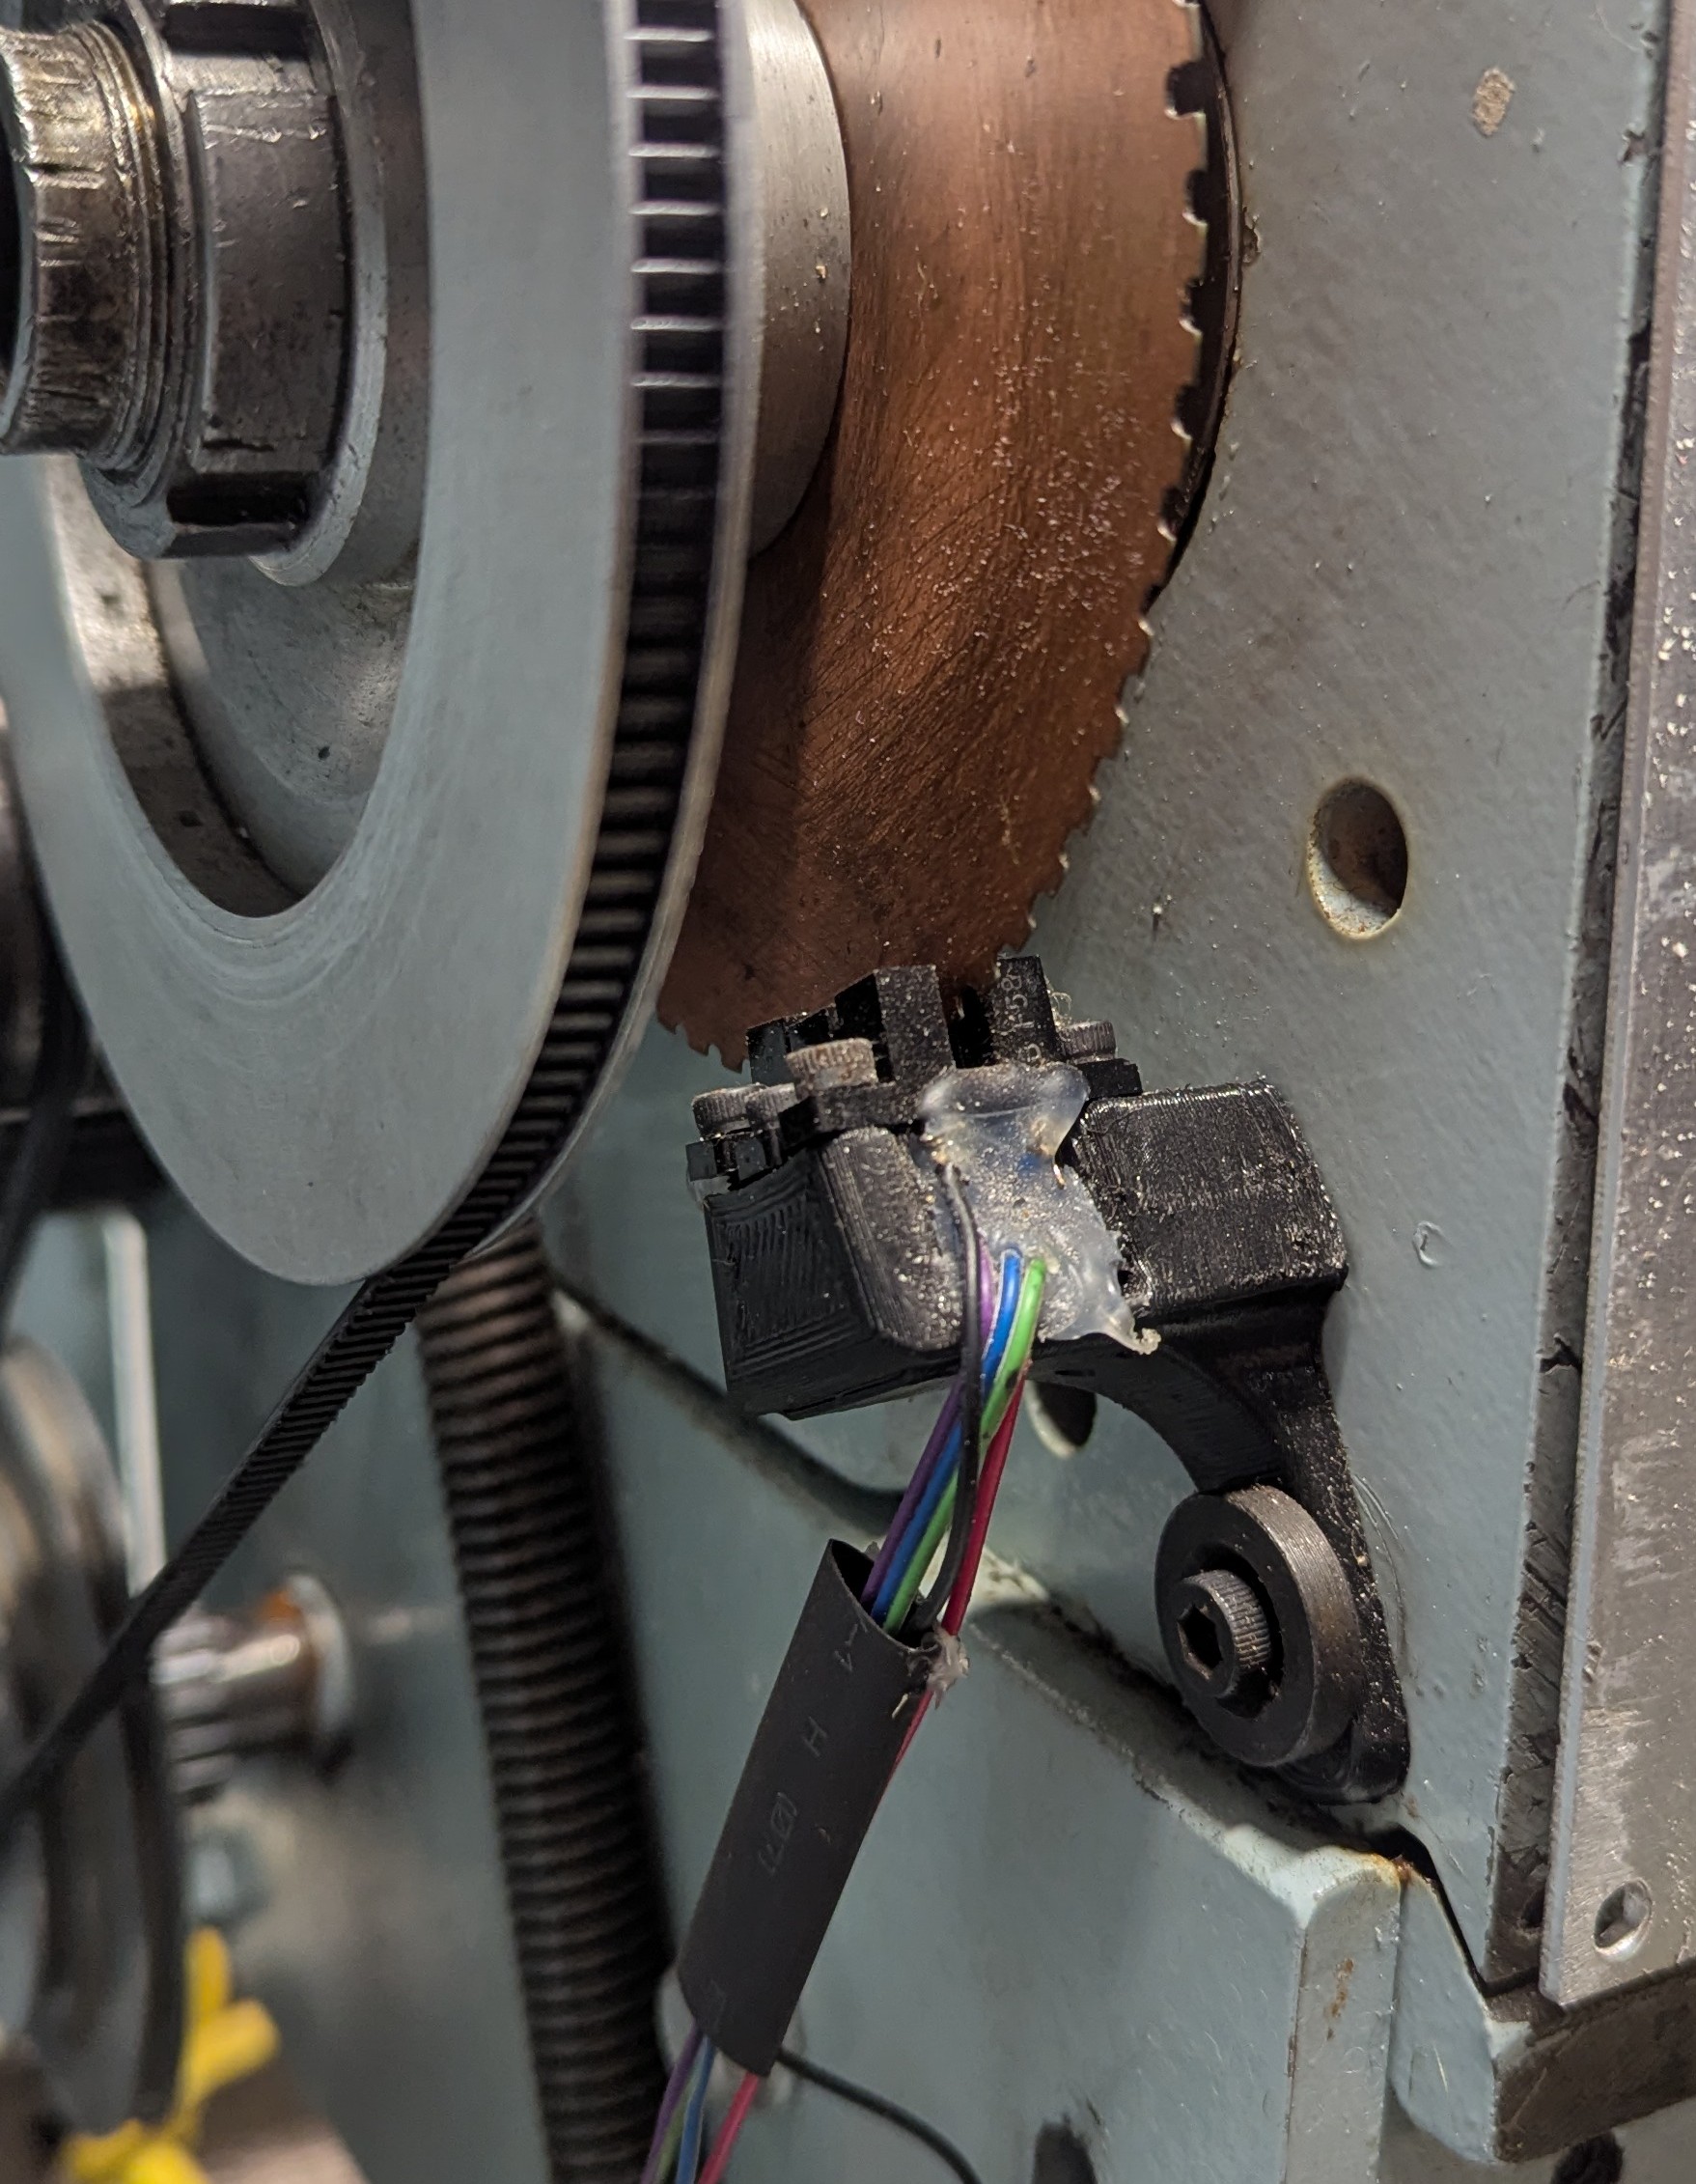
Photo of my toothed wheel with three encoders and planned update if I ever get around to it.
 
 
Last edit: 1 year 7 months ago by jtrantow.

Please Log in or Create an account to join the conversation.
More
1 year 7 months ago #323433 by jtrantow
Replied by jtrantow on topic Lathe spindle index only?
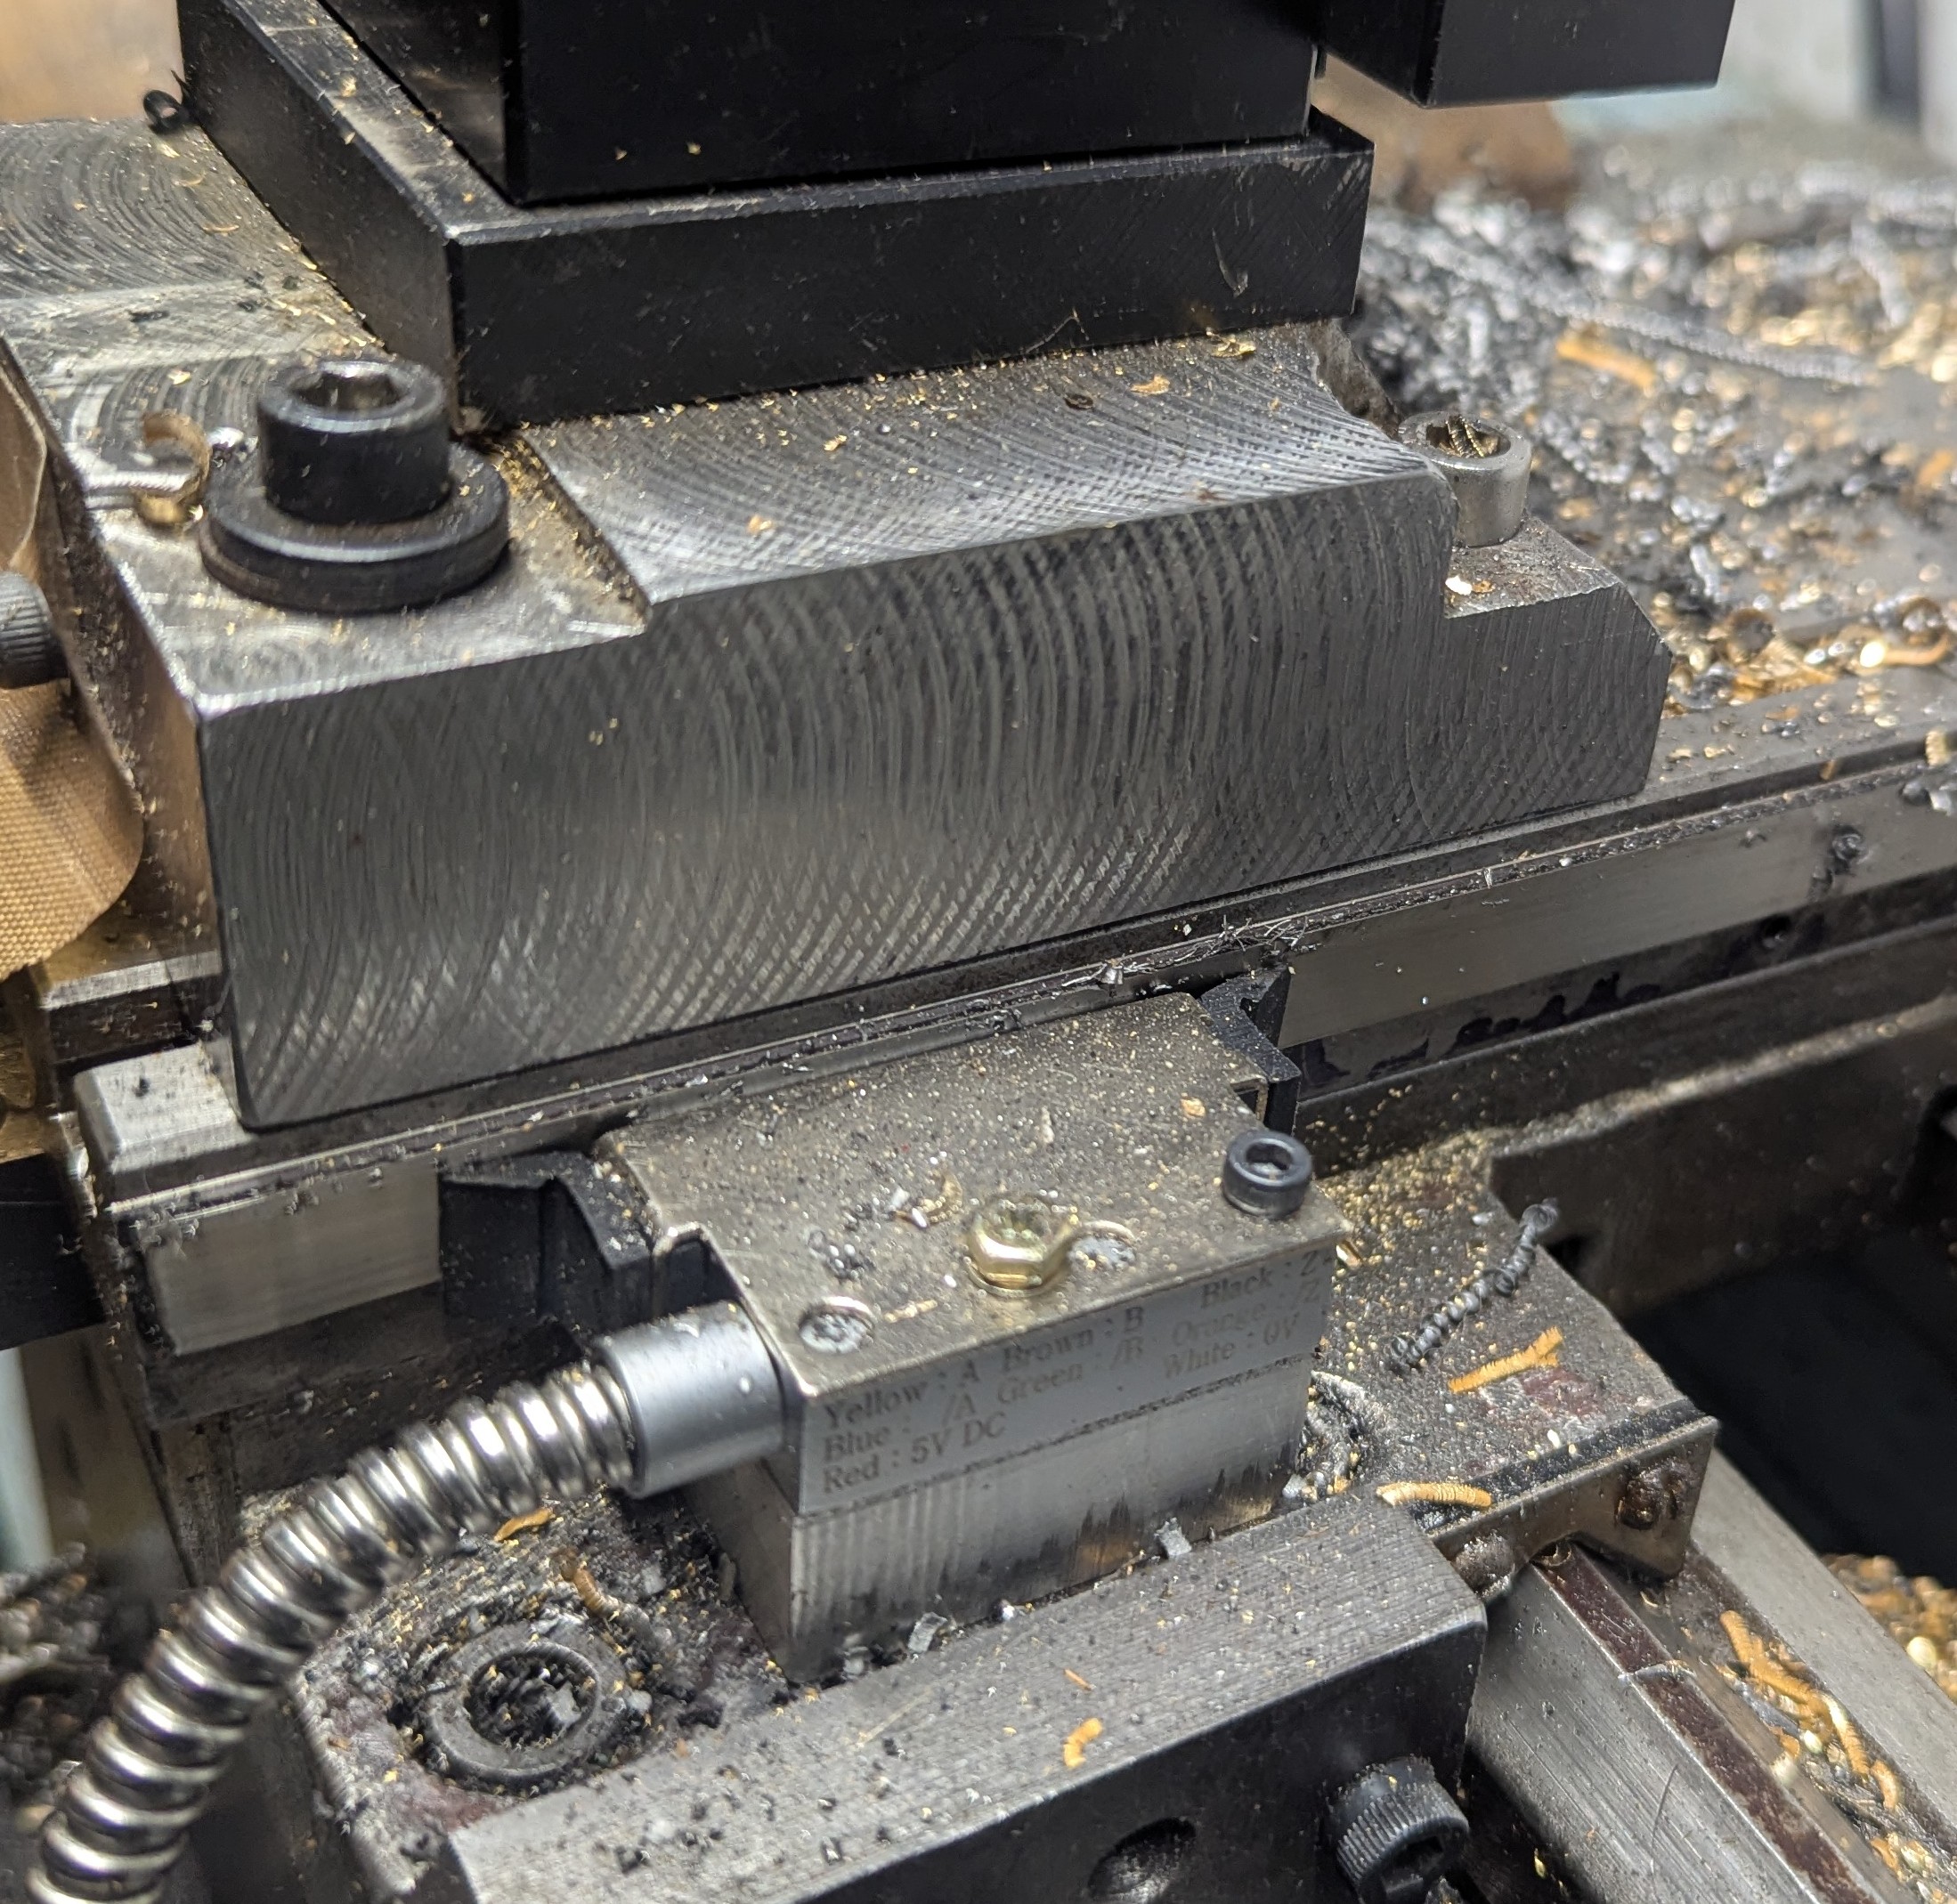
The problem I had was fitting the x ballnut under the cross slide. I ordered a 8mm ballscrew (AliExpress) and still ended up grinding off part of the nut and milling the cross slide. If you grind a ballnut with plastic ball returns use cooling or you can melt the returns...
   

After some trial and error, I settled on 1u magnetic encoder for x.


Photo also shows crude but effective solid tool post. You can sell all your now unnecessary lathe parts on eBay. You will never go back to change gears or manual dials. No regrets selling my compound. Use the $ for x encoder and tooling.

Finally get Andy's lathe macros working and I use the wired Logitech keypad on all my machines for jogging.

Please Log in or Create an account to join the conversation.

More
1 year 7 months ago #323444 by 109jb
Replied by 109jb on topic Lathe spindle index only?
Thanks again. Initially I plan to do this using a Raspberry Pi using software stepping through GPIO, so I am a bit concerned about the Pi being able to keep up with encoder pulses. If it doesn't work on just the Pi, I will get a 7C81 Mesa board for it, but want to try using just the Pi first.

I don't ever see needing to use the spindle as a dividing head. I have a 4th axis on my mill if I need that, so I think two encoders, one for index and one for pulses would work okay for what I need. We will see.

Looking at your picture, that is almost exactly what I was picturing for the slot sensor mounting. I may try a 3d printed slot wheel. We'll see if it flys apart, but I generally don't run too high speeds and think it will be fine. I'll print it at 100% infill and make an aluminum hub to sanwich behind the pulley.

What brought this about is that the threading nut setup on the lathe broke last time I needed to thread a part and I figured it was time to convert to CNC. I plan to include 2 MPG handwheels mounted on the carriage so that I can mimick a manual machine for times when I just want to do simple turning. I have that worked out on the Pi already. I use a handheld wireless MPG on my mill but am thinking about adding 3 handweels and eliminating the wireless MPG. I've had a few loss of connection issues with it in the past.

This is a long term project so things won't happen too fast. I have access to a friends 13" Clausing lathe if I need one and he is only about 3minutes away. I have another big project I'm working on and this one is a fill in for times when I need a break from that one. Thinking about the basic X-Z conversion, the Z axis looks like a piece of cake, and if that 12mm ballscrew I got fits, the X axis cross slide won't be too bad either.

Thanks again.

Please Log in or Create an account to join the conversation.

Time to create page: 0.529 seconds
Powered by Kunena Forum
