
- Posts: 71
- Thank you received: 4
Spindle speed sensor for a Bridgeport 2J head
- rogerfries
- Offline
- Senior Member
-

Less
More
6 years 3 weeks ago #185075
by rogerfries
Replied by rogerfries on topic Spindle speed sensor for a Bridgeport 2J head
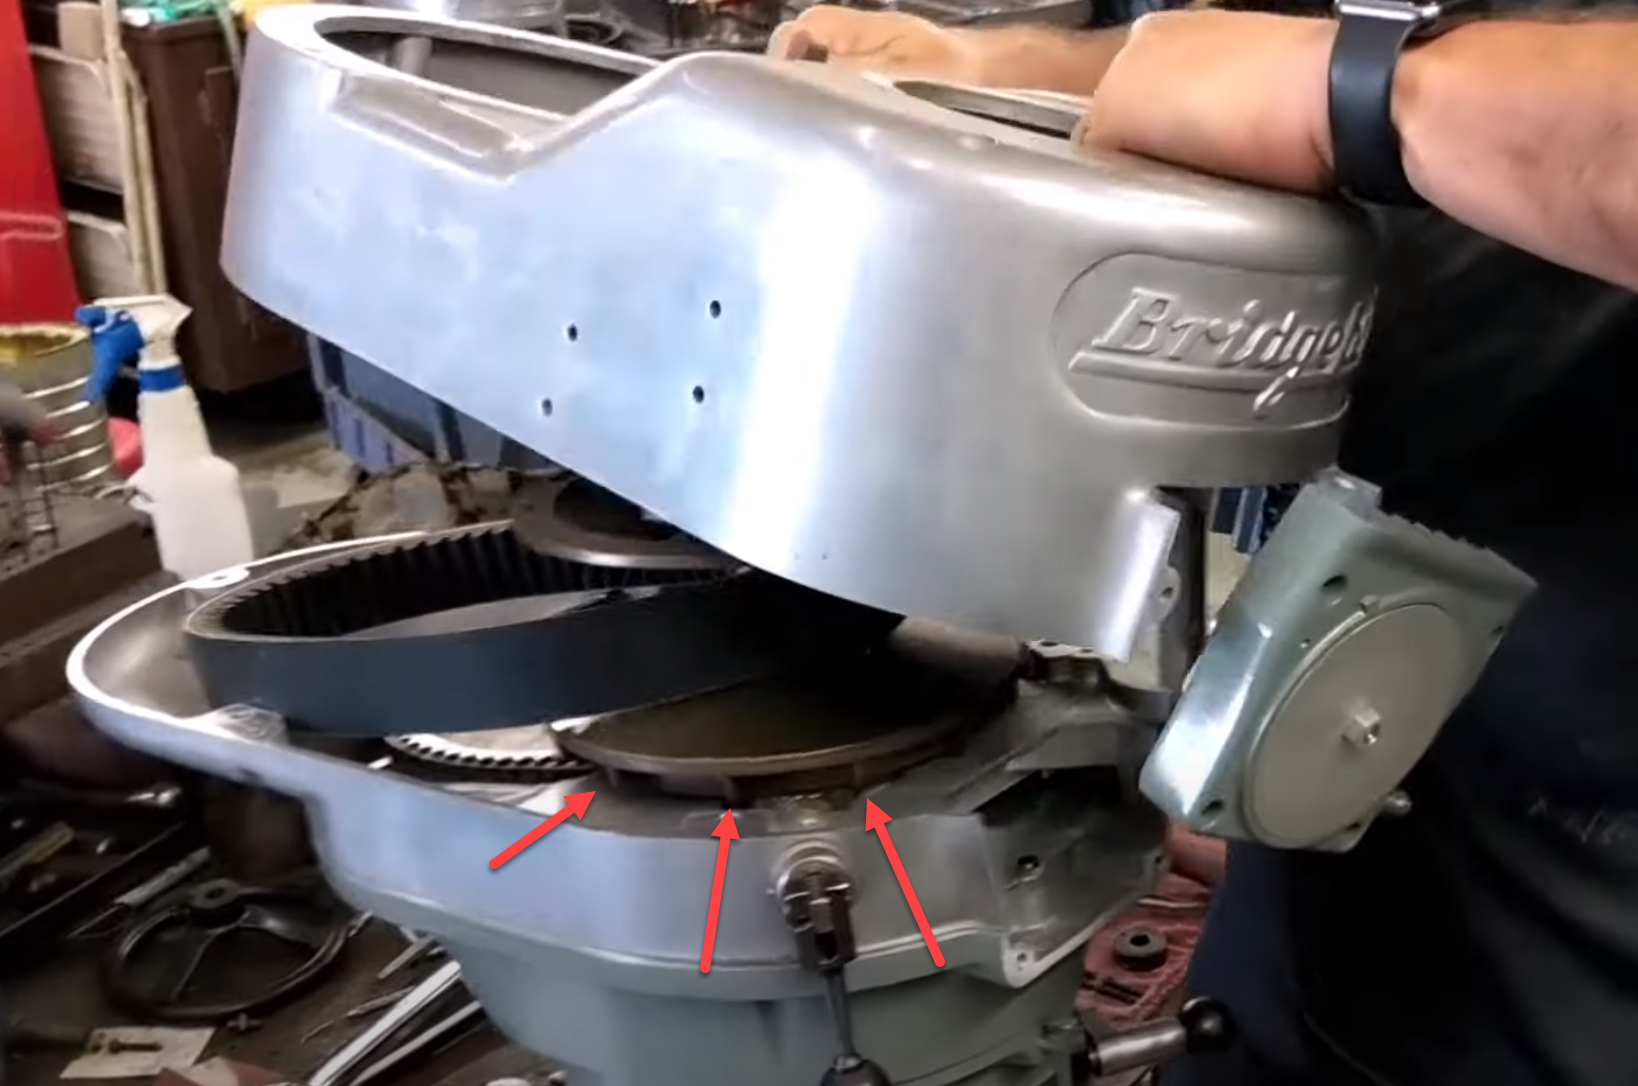
I wounder if I could read these supports on the bottom of the Vari-speed belt? Or better press a reluctor wheel (if that's the correct term) on it?
Please Log in or Create an account to join the conversation.
- rootboy
- Offline
- Senior Member
-
Less
More
- Posts: 76
- Thank you received: 25
6 years 3 weeks ago #185540
by rootboy
Replied by rootboy on topic Spindle speed sensor for a Bridgeport 2J head
Those spots should be no problem. And since it is steel that your sensor will be reading you won't have to get as close to them with the sensor.
But is twelve pluses per revolution going to suffice? Do you need to know direction as well?
But is twelve pluses per revolution going to suffice? Do you need to know direction as well?
Please Log in or Create an account to join the conversation.
- rogerfries
- Offline
- Senior Member
-
Less
More
- Posts: 71
- Thank you received: 4
6 years 3 weeks ago #185603
by rogerfries
I think 12 pulses per rev would be enough for a simple speed indicator, but If I'm going to tear into this I'd like to get a full encoder so perhaps I can try some rigid tapping.
What if I took this part and machined off some or all of the 12 ridges so I can press on a custom made gear tooth ring?
www.machinerypartsdepot.com/product/1561
I'd buy a new part to try it out os so I can revert to back stock ahould this idea turn into a horror show.
This raises the question, How much resolution is needed to do this right? how small can I make the teeth so the sensor can pick them up acurately? Can I achieve sufficiant resolution on this reletively small wheel to do thinks like rigid tapping?
What do you guys think? Thanks!
Replied by rogerfries on topic Spindle speed sensor for a Bridgeport 2J head
rootboy wrote: Those spots should be no problem. And since it is steel that your sensor will be reading you won't have to get as close to them with the sensor.
But is twelve pluses per revolution going to suffice? Do you need to know direction as well?
I think 12 pulses per rev would be enough for a simple speed indicator, but If I'm going to tear into this I'd like to get a full encoder so perhaps I can try some rigid tapping.
What if I took this part and machined off some or all of the 12 ridges so I can press on a custom made gear tooth ring?
www.machinerypartsdepot.com/product/1561
I'd buy a new part to try it out os so I can revert to back stock ahould this idea turn into a horror show.
This raises the question, How much resolution is needed to do this right? how small can I make the teeth so the sensor can pick them up acurately? Can I achieve sufficiant resolution on this reletively small wheel to do thinks like rigid tapping?
What do you guys think? Thanks!
Please Log in or Create an account to join the conversation.
- OT-CNC
- Offline
- Platinum Member
-

Less
More
- Posts: 617
- Thank you received: 75
6 years 3 weeks ago #185611
by OT-CNC
Replied by OT-CNC on topic Spindle speed sensor for a Bridgeport 2J head
If you modify the vari-disk, make sure it stays balanced also I believe those supports act as fans to pull air through the openings on the speed change housing.
Keep in mind that if you go off the vari disk or the top mount like I did, you will get accurate rpm only in normal gear. Back gear will be a different ratio and will mess with the index.
Do you have any exploded views of your spindle? I'm curious on the section that houses the z drive where the stepper is. I'm picturing hanging an encoder off the side driving it with a thin timing belt off the splined shaft. Maybe there is enough room?
Please Log in or Create an account to join the conversation.
- Mike_Eitel
- Offline
- Platinum Member
-
Less
More
- Posts: 1051
- Thank you received: 183
6 years 3 weeks ago #185615
by Mike_Eitel
Replied by Mike_Eitel on topic Spindle speed sensor for a Bridgeport 2J head
If you can fix it additonal on that, you can use a ring, drill lots of tiny holes and fill/glue them with small magnets. Just saw yesterday a 6x6x6 cube of 2mm ones.
Please Log in or Create an account to join the conversation.
- rootboy
- Offline
- Senior Member
-
Less
More
- Posts: 76
- Thank you received: 25
6 years 3 weeks ago #185622
by rootboy
Before I modded the lower pulley half, I would put the tooth ring on the top pulley and mount the sensors through the top cover looking down. Take a look at the video that you provided at about the 11 minute mark. Looks to be plenty of room available to you, and little to no machining for you to have to do.
Drill and tap a second hole inside of the ring and mount a bolt in it. Add a sensor for this, and this can now be used as your marker pulse.
As for resolution, I guess the answer would be how tight of a tolerance do you need to keep the thread cutting to? I'm no machinist, but I can't imagine 5 - 10 degrees making all that much difference.
And rather than worrying about a ton of teeth on the tooth ring, put a second sensor halfway between the teeth. This will in effect give you double the amount of teeth for the price of a sensor.
It should, but wouldn't have to be, mounted as precisely as possible to the midway point between the teeth. Simply run the finished setup, and calculate the trigger point of the midway tooth compared to the primary sensor. Then it's a matter of adding an offset that will in effect "center" the sensor on the tooth for you.
Put another sensor offset from the first sensor by half a tooth and you will get direction as well.
The four sensors can be wired to an Arduino to create the finished encoder pulses for you.
Replied by rootboy on topic Spindle speed sensor for a Bridgeport 2J head
rogerfries wrote:
rootboy wrote: Those spots should be no problem. And since it is steel that your sensor will be reading you won't have to get as close to them with the sensor.
But is twelve pluses per revolution going to suffice? Do you need to know direction as well?
I think 12 pulses per rev would be enough for a simple speed indicator, but If I'm going to tear into this I'd like to get a full encoder so perhaps I can try some rigid tapping.
What if I took this part and machined off some or all of the 12 ridges so I can press on a custom made gear tooth ring?
www.machinerypartsdepot.com/product/1561
I'd buy a new part to try it out os so I can revert to back stock ahould this idea turn into a horror show.
This raises the question, How much resolution is needed to do this right? how small can I make the teeth so the sensor can pick them up acurately? Can I achieve sufficiant resolution on this reletively small wheel to do thinks like rigid tapping?
What do you guys think? Thanks!
Before I modded the lower pulley half, I would put the tooth ring on the top pulley and mount the sensors through the top cover looking down. Take a look at the video that you provided at about the 11 minute mark. Looks to be plenty of room available to you, and little to no machining for you to have to do.
Drill and tap a second hole inside of the ring and mount a bolt in it. Add a sensor for this, and this can now be used as your marker pulse.
As for resolution, I guess the answer would be how tight of a tolerance do you need to keep the thread cutting to? I'm no machinist, but I can't imagine 5 - 10 degrees making all that much difference.
And rather than worrying about a ton of teeth on the tooth ring, put a second sensor halfway between the teeth. This will in effect give you double the amount of teeth for the price of a sensor.
It should, but wouldn't have to be, mounted as precisely as possible to the midway point between the teeth. Simply run the finished setup, and calculate the trigger point of the midway tooth compared to the primary sensor. Then it's a matter of adding an offset that will in effect "center" the sensor on the tooth for you.
Put another sensor offset from the first sensor by half a tooth and you will get direction as well.
The four sensors can be wired to an Arduino to create the finished encoder pulses for you.
Please Log in or Create an account to join the conversation.
Time to create page: 0.839 seconds