THC plasma configs, with HOW TO.

More
8 years 3 months ago - 8 years 3 months ago #115181 by jawneelogik
tommylight, This is my first post on this forum. I have been lurking for quite a few months, but I have not yet taken the plunge into LinuxCNC so I thought it best to keep my mouth shut and just listen for now.

I do have a question regarding the Proma 150 that I'm hoping you will help me with. Can you share with me what are your recommended settings on the Proma 150 THC controller (Hysteresis, Delay, etc.) as well as your recommended Z parameters (velocity and acceleration) while under THC control.

I am now using a UCCNC controller. I needed to replace Mach3 and another forum member recommended it. I have also been told I should get something better than the Proma 150, but I'm not ready to give up on it yet (it's paid for!). Most of the material I cut is between 1/4" and 1/2" and some times up to 3/4". The material is normally quite flat/straight, but in my limited experience, I see that these tables can never maintain perfect alignment between the gantry and the material surface. They are NOT milling machines. The support slats are constantly getting chewed up badly which changes the material support surface over the length and width of the table, so, I believe, reliable THC is needed to maintain proper cut height for best quality and consumable life.

My table is 4'x8'. It will move at up to 700 ipm in all axes and my acceleration is currently set at 300 ips/s.
Last edit: 8 years 3 months ago by jawneelogik.

Please Log in or Create an account to join the conversation.

More
8 years 3 months ago - 8 years 3 months ago #115184 by Grotius
@Tommy,

That looks kind of cool. Gmoccapy has cool colors...
I changed the color theme to adwaita dark in Gmoccapy, but added button's are not changing into dark. I am using Debian 9.
Hmm. something to think about. I think i have to add some orginal python code back to the files, then it will follow the theme.

Do you want to use Gmoccapy in future for your plasma machine's? Or do you want to stay at the Axis screen?

Please find the Toma schematics.
After that I will look for a option to enable float switch and the float switch area option is also a time saving option.
Last edit: 8 years 3 months ago by Grotius.
The following user(s) said Thank You: tommylight

Please Log in or Create an account to join the conversation.

More
8 years 3 months ago - 8 years 3 months ago #115206 by tommylight

jawneelogik wrote: Can you share with me what are your recommended settings on the Proma 150 THC controller (Hysteresis, Delay, etc.) as well as your recommended Z parameters (velocity and acceleration) while under THC control.
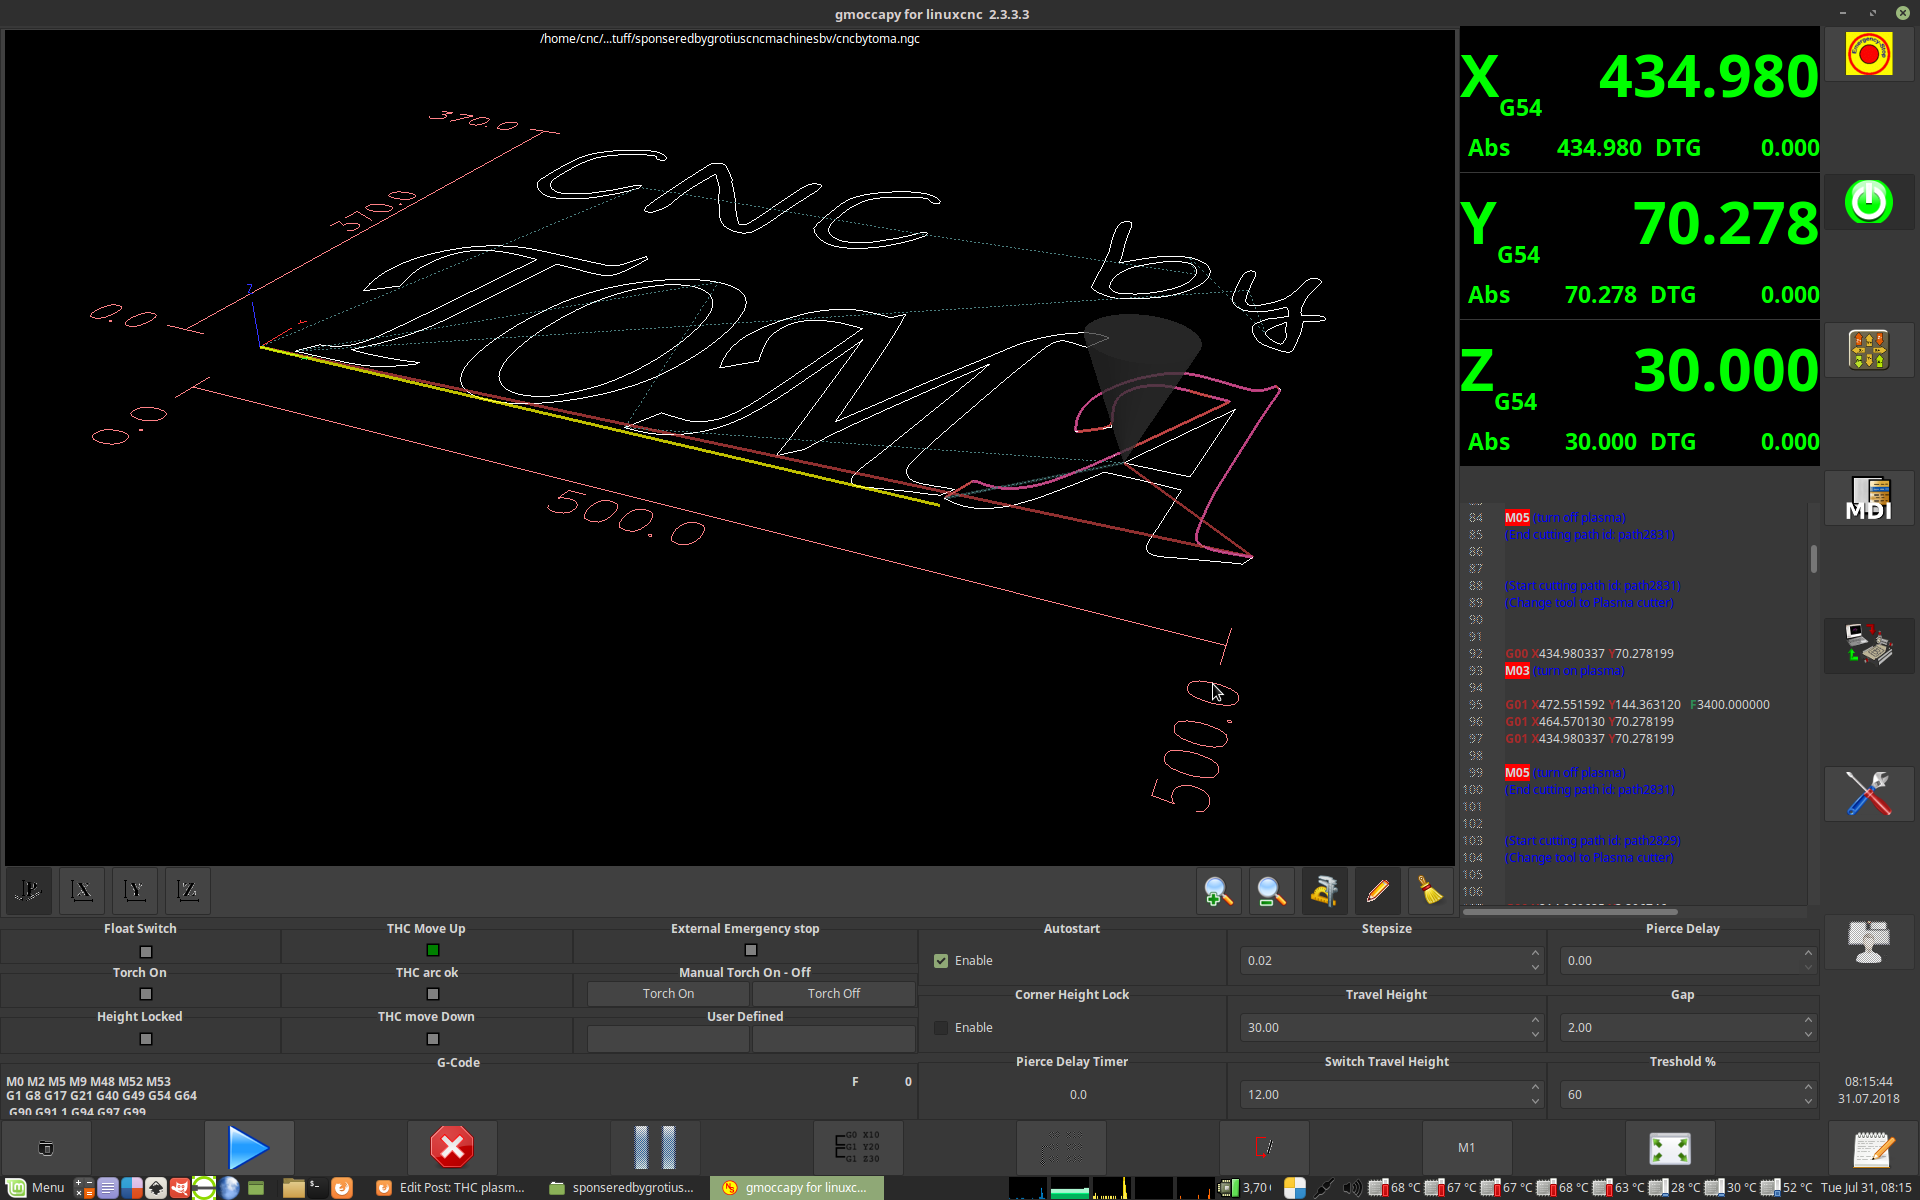
I have all of them set to the fastest reaction time, so Hysteresis is at 2V i think and delay is at 0.1.
If you use the toma config you can set everything in Linuxcnc. For what you need it, Proma 150 will do nicely, even for much more.

BTW here it is on one of the computers i use daily at 1920X1200,


Those LED's really need to be much bigger, and i see no velocity anywhere while the machine is moving, that is a must when plasma cutting.
Last edit: 8 years 3 months ago by tommylight.

Please Log in or Create an account to join the conversation.

More
8 years 3 months ago #115218 by bevins
Hi Tommylight,

Would this be easily setup for 5i25-7i76 stepper system with no FB? I noticed some FB in the thc hal.

Thanks, nice work.

Please Log in or Create an account to join the conversation.

More
8 years 3 months ago #115221 by tommylight
It should be fairly easy, but i sold my 7i76E so i can not test it.
I did set up a 6i25 with stepgens so it should be similar, but i had not time to test it yes.
The following user(s) said Thank You: bevins

Please Log in or Create an account to join the conversation.

More
8 years 3 months ago #115224 by jawneelogik
tommylight, thx for your reply.

Cool screens. Almost makes me regret my decision to choose UCCNC instead of LinuxCNC. However, I needed something that I could comfortably implement out-of-the-box without too steep a learning curve and UCCNC met that criteria (It seems like a "cleaned-up" clone of Mach3.). I do intend to explore LCNC going forward, but I have contract obligations to maintain a level of production in my shop.

Regarding your screen, I don't see anywhere a setting for Z response velocity under THC control? Is there no need for this parameter within LinuxCNC?

Please Log in or Create an account to join the conversation.

Moderators: snowgoer540
Time to create page: 0.457 seconds
Powered by Kunena Forum
