
- Posts: 1943
- Thank you received: 338

tommylight wrote: It should be fairly easy, but i sold my 7i76E so i can not test it.
I did set up a 6i25 with stepgens so it should be similar, but i had not time to test it yes.
Please Log in or Create an account to join the conversation.
bevins wrote:
Just have to figure out which THCad, 10v or 300v.....
Bob
Please Log in or Create an account to join the conversation.
rodw wrote:
bevins wrote:
Just have to figure out which THCad, 10v or 300v.....
Bob
Bob, I'd recommend the 300v version if you don't have a voltage divider and 10v if you do. (unless you have a > 130 amp plasma cutter that produces > 300 volts!
Also mount the THCAD on or in your plasma cutter as the frequency signal will be much more immune to noise on its trip to the control box....
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
 Topic Author

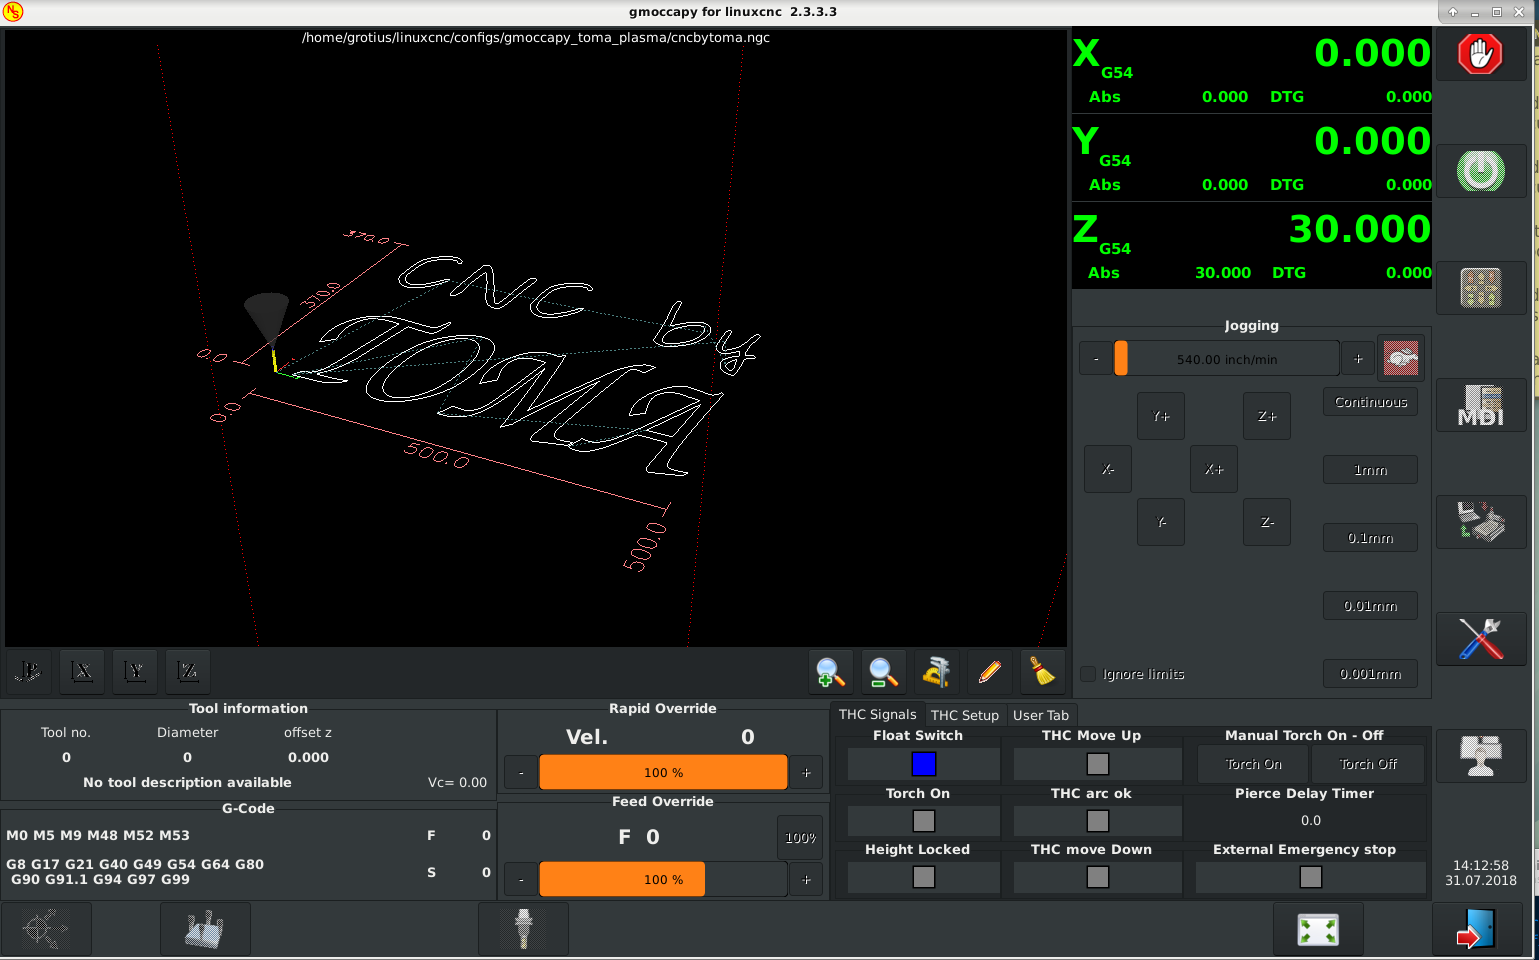
Velocity is set in the ini file at the maximum Z axis can handle, and on screen you have "step size" to adjust how much it will move when commanded from THC.jawneelogik wrote: Regarding your screen, I don't see anywhere a setting for Z response velocity under THC control? Is there no need for this parameter within LinuxCNC?
Please Log in or Create an account to join the conversation.
Just have to figure out which THCad, 10v or 300v.....
Please Log in or Create an account to join the conversation.