5 Axis TCP Simultaneous Kinematics Fusion 360 setup Mesa 7i76e

More
3 years 6 months ago - 3 years 6 months ago #269602 by rodw
<quote>Thank you RodW.
I'll see what PCs I have lying around that could fit the bill. Version 2.9 isn't listed, that's the current build? I'll look through your notes. I really appreciate you sharing them with me.
Do you have direct experience with 5 axis continuous machining? Or do you know anyone who does? I'd love to pick somebody's brain regarding what I'm trying to accomplish.
</quote>
Version 2.8 is the current release version and is pretty long in the tooth. 2.9 has been hived off pending release. 2.10 is the current development branch (master). Linuxcnc was accepted into the Debian repsitories last year but it is only by perodic snapshots of version 2.9. The last one was in about November.

There is an unofficial buildbot of 2.9 and 2.10 so updates are available for bookworm on an ongoing basis. I need to experiment with it and update my instructions.

I have no experience with 5 axis. Aceira is the expert with the kinematics mathematics. I have enough trouble moving from 2D plasma cutting to a 3 Axis CNC Mill I converted. But 2.9/2.10 have some really nice kinematics modules using a method called switchkins which allows swapping between conventional 5 axis cnc mode and 5 axis TCP mode which is cool... 

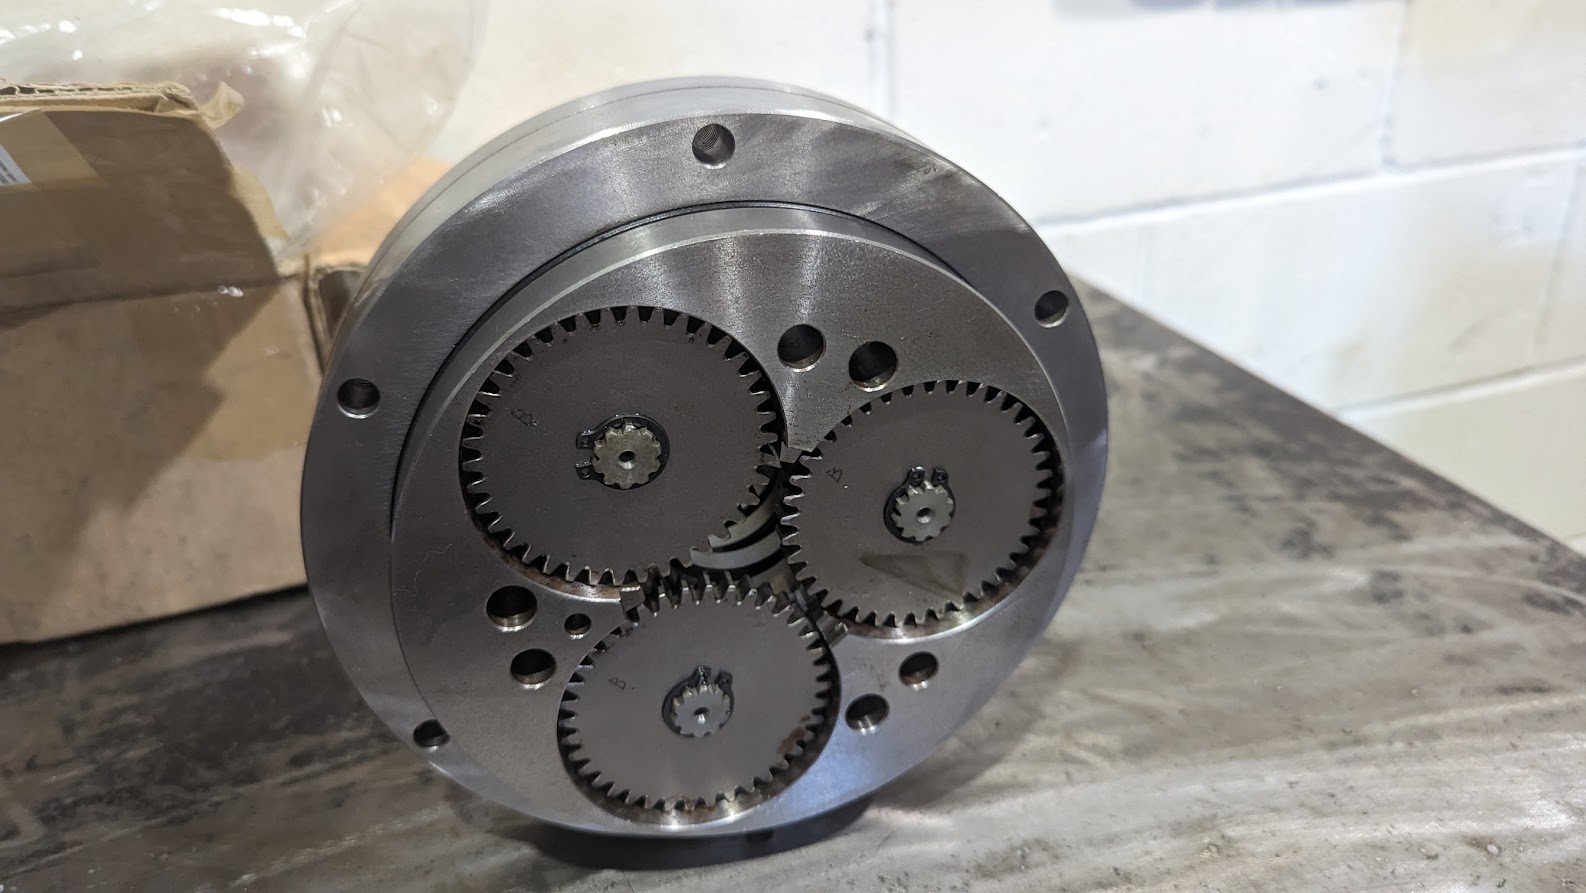
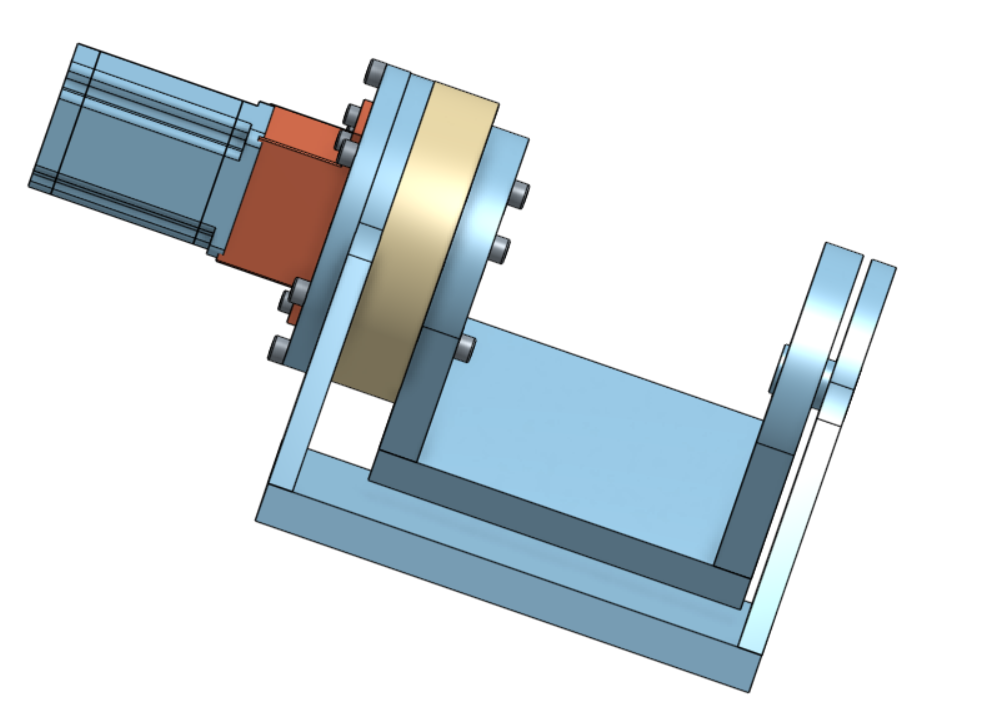
But somebody gave me a High precision rotary gearbox recently. Fortunately, I have a good gear shop who has been making parts for me for years so they are making the missing input shaft (The manufacturer had full specs.) And I have done a bit of work in Onshape. I was planning on using flat parts laser cut from 16mm or 25mm steel. Then bolt or weld together. Welding would require normalisation and machining... 

Its not really a trivial project. This baby needs a 6000 rpm 1 kW servo motor to output 40 rpm. I think that is in the ballpark. What do you think/
I'm not sure where this will take me.... 


Last edit: 3 years 6 months ago by rodw.

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #269608 by wiremonkey
This is very useful information. I hadn't quite understood the joint vs axis concept. Also, thanks for the heads up regarding the limits. As you say, I'm hoping that any potential collisions will be vetted during the CAM process.
Thanks again.

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago - 3 years 6 months ago #269609 by wiremonkey
OK, now I can do the deep dive on switchkins! I appreciate the input.
Looks like you've got a very beefy cycloidal drive there! It seems a bit overkill unless you're trying to mill steel on a regular basic. I plan on starting with a somewhat inexpensive AC setup, around $600, and learn my way around 5 axis machining using very forgiving materials. I'm really curious how accurate I can get. With 3 axis machining, belt driven, I'm living in the ±0.05mm accuracy range. I'd love to be able to achieve this in 5 axis continuous land without breaking the bank, but I don't know how realistic it is.
Good luck with your project. You can't find a replacement shaft from the manufacturer of that gear box?
T-
Last edit: 3 years 6 months ago by wiremonkey.

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #269630 by wiremonkey
OK, so I ordered the AC rotary table in my initial post. I'll do some testing and get back to everyone. Thanks so much for the help!

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #269638 by JPL

... Its not really a trivial project. This baby needs a 6000 rpm 1 kW servo motor to output 40 rpm. I think that is in the ballpark. What do you think...

 
If you go with a used servo motor you will need recent model as the older one have a hard time going above 3 to 5k rpm. For example,  I've recently bought a used  Kollmorgen AKM24F. Max rpm is 8000. Constant torque is 1.8Nm  This is an 830W motor but watts rating can be misleading since what you really need is torque.

So,  your gear reduction appear to be 75  (6000 rpm -> 40 rpm). , Considering an efficiency of 90% your final torque will be around 121.5 Nm with such a motor. Hummm, that seems to be a lot of torque.

Please Log in or Create an account to join the conversation.

More
3 years 6 months ago #269646 by rodw
The gearbox ratio is 153:1. 6000/153 =  39.2 rpm
That seemed to be in the ballpark of some commercial 5th axis units I researched.
Yes I did look at motor requirements. There is a minimum required input torque but its not excessive, I don't think output torque will be a problem!
I really was more interested in the maximum expected torque while cutting as that has an impact on backlash/accuracy.
I probably would use a new servo as I would use 220v AC ethercat...
An alternative use could be to tun a 30 cow rotary dairy on a dairy farm!
In answer to an earlier question, the Japanese manufacturer lists a part number but never replied..
I think in a lot of use cases, custom input shafts are required and they give very detailed specs and drawings
There were 4 of these units given to us and they have been shared around among a group of Aussie users so the cost of the custom shafts for a run of 4 is quite reasonable. I just happened to know the right guys to make them..

Please Log in or Create an account to join the conversation.

Time to create page: 0.296 seconds
Powered by Kunena Forum