
- Posts: 1635
- Thank you received: 595
Retrofitting a 1986 Maho MH400E
- RotarySMP
- Offline
- Platinum Member
-

Less
More
9 years 3 weeks ago #99995
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Good shot with the USB stick down the elevator gap. Couldn't do it again if you tried 
Whn you talk of "Spindle at speed" signal, was this signal generated from that encoder, or frm the VFD, or is it just an assumed value based on the worst case time for the spindle to accelerate. The MAHO set up can't generate that signal as built can it?
Mark
Whn you talk of "Spindle at speed" signal, was this signal generated from that encoder, or frm the VFD, or is it just an assumed value based on the worst case time for the spindle to accelerate. The MAHO set up can't generate that signal as built can it?
Mark
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-

Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago #99998
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
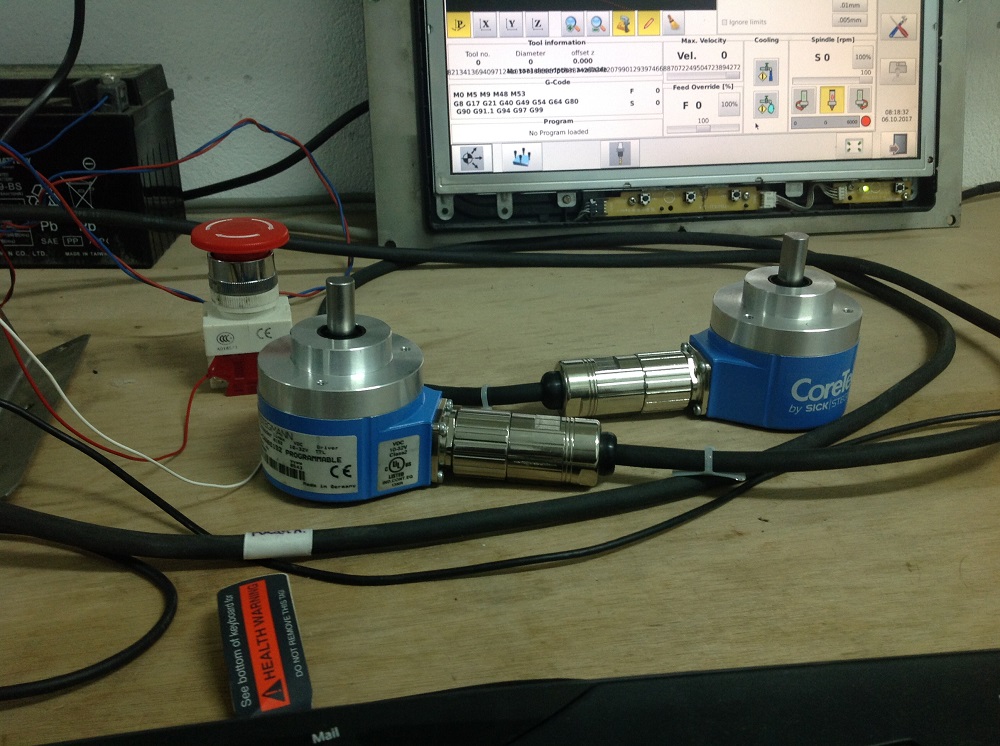
Those are the encoders for the servos.
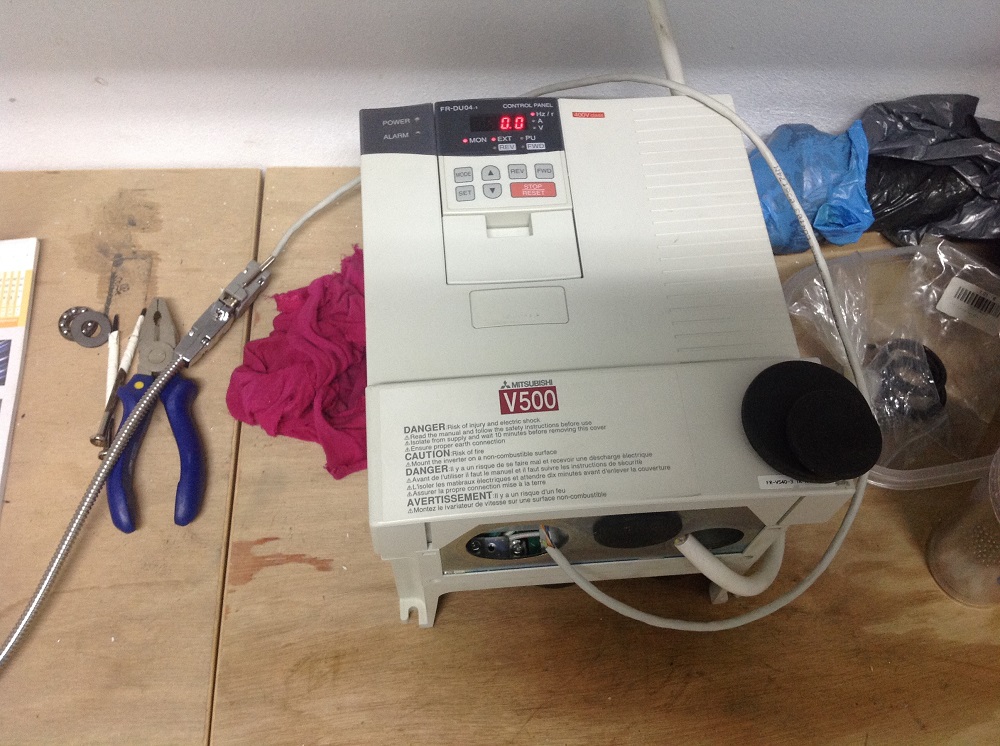
This is the vector drive for the spindle motor
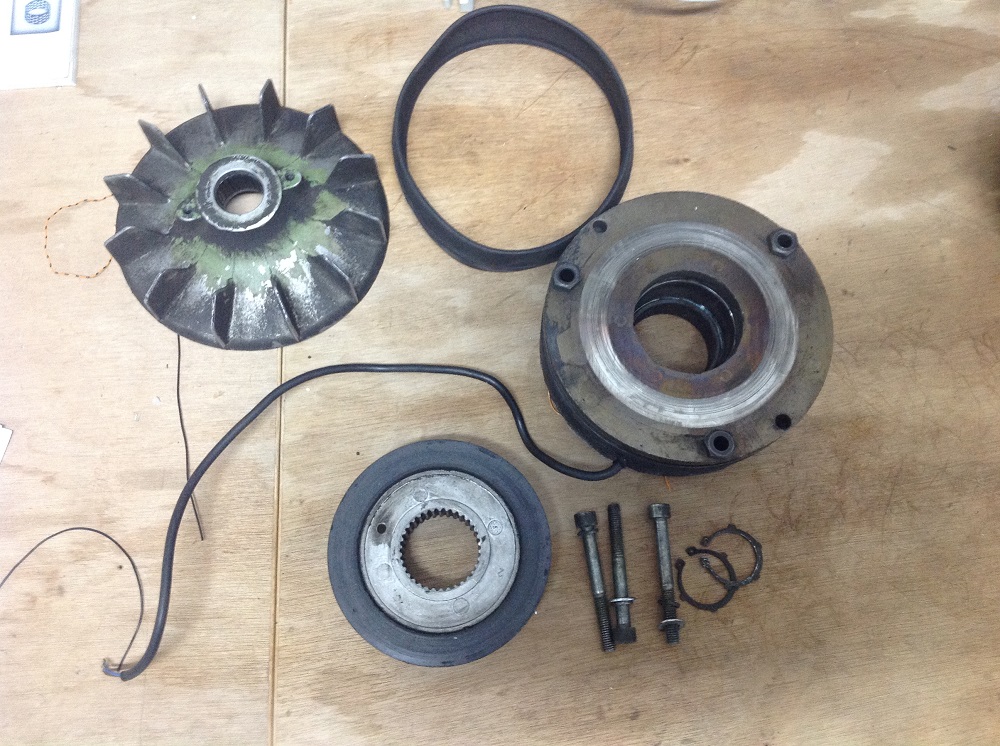
And the brake of the spindle motor
This is the vector drive for the spindle motor
And the brake of the spindle motor
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago - 9 years 3 weeks ago #100000
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
Spindle at speed is an control input to LinuxCnc it is binary (1 or 0) if it is 0 than the LinuxCnc holds the feeds on all axis, if it is 1 than the motion is continued again. The encoder is fed directly to LinuxCnc, and LinuxCnc synchronizes the motion for every job that needs sinc motion with spindle.
John
John
Last edit: 9 years 3 weeks ago by drimaropoylos.
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago - 9 years 3 weeks ago #100001
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
The VFD has a relay output spindle at speed, I can connect it to mesa and connect the two signals with “and” in hall file, or in ladder. The maho originally I don’t think that it had speed at speed, I think it had timers on the controller.
Last edit: 9 years 3 weeks ago by drimaropoylos.
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago - 9 years 3 weeks ago #100003
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
I think that Spindle at speed is intended to be connected like this (to vfds), so LinuxCnc knows that the vfd has reached the commanded speed.
Last edit: 9 years 3 weeks ago by drimaropoylos.
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago - 9 years 3 weeks ago #100013
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
www.linuxcnc.org/docs/2.4/html/examples_...cha:Spindle-Feedback
loadrt encoder num_chan=1
addf encoder.update-counters base-thread
addf encoder.capture-position servo-thread
setp encoder.0.position-scale 100
net spindle-position encoder.0.position => motion.spindle-revs
net spindle-velocity encoder.0.velocity => motion.spindle-speed-in
net spindle-index-enable encoder.0.index-enable <=> motion.spindle-index-enable
net spindle-phase-a encoder.0.phase-A
net spindle-phase-b encoder.0.phase-B
net spindle-index encoder.0.phase-Z
net spindle-phase-a <= parport.0.pin-10-in
net spindle-index <= parport.0.pin-11-in
Can I put on the setp encoder.0.position-scale instead of a number, a signal that is connected to an output off ladder to scale correct the selected gear. And not connect the index
John
Last edit: 9 years 3 weeks ago by drimaropoylos.
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 2.193 seconds