
- Posts: 1635
- Thank you received: 595
Retrofitting a 1986 Maho MH400E
- RotarySMP
- Offline
- Platinum Member
-

Less
More
9 years 3 weeks ago #100034
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Thanks for the photos. Reminds me that I should also use my camera instead of the phone to post decent photos.
Why add encoders to the axis motors? Are you throwing out the Indramat?
If we need a spindle at speed signal to make the gearbox changing work, I'll just use a worst case time delay to simulate that, as I really dont want to get into replacing the MAHO relay based motor contro with a VFD at this time. Maybe down the road.
Mark
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-

Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago #100042
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
Say that we cut something and while the g code is running we estimate that the spindle speed is to low or to hi, and we move the spindle slider on the Gmoccapy. The ladder will see change in the commanded speed, and it will start gear change immediately. If the controller won’t stop feed on all axis and stop the motor, then either the gear box will be destroyed because the speed is very hi for gear change, or the tool will break because the spindle is not rotate to remove material.
When the slider for commanded speed is moved or a spindle speed commanded from the gcode than we have to ensure that the spindle will slow down to a stop and none of the axis is moving. I believe this is “what spindle at speed” signal is doing, it pause the program until the “spindle at speed” is true again. So when the ladder sees a change in commanded spindle speed, it makes the “spindle at speed” false wait for the estimated time needed for the spindle to come to a full stop, make the gear change and make the “spindle at speed” true again for the program to continue.
John
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago #100044
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
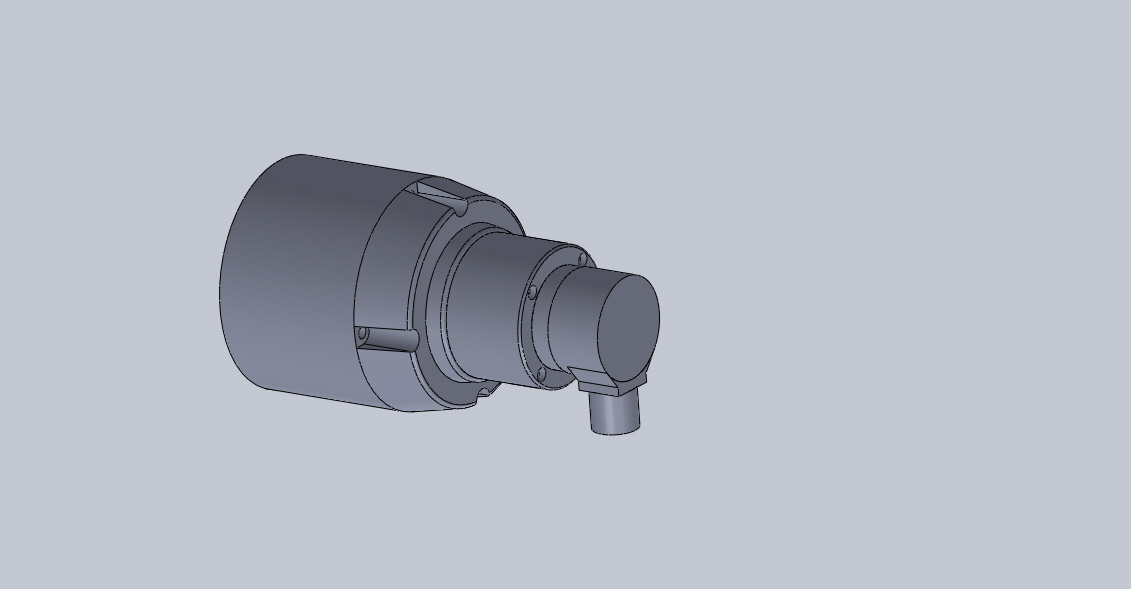
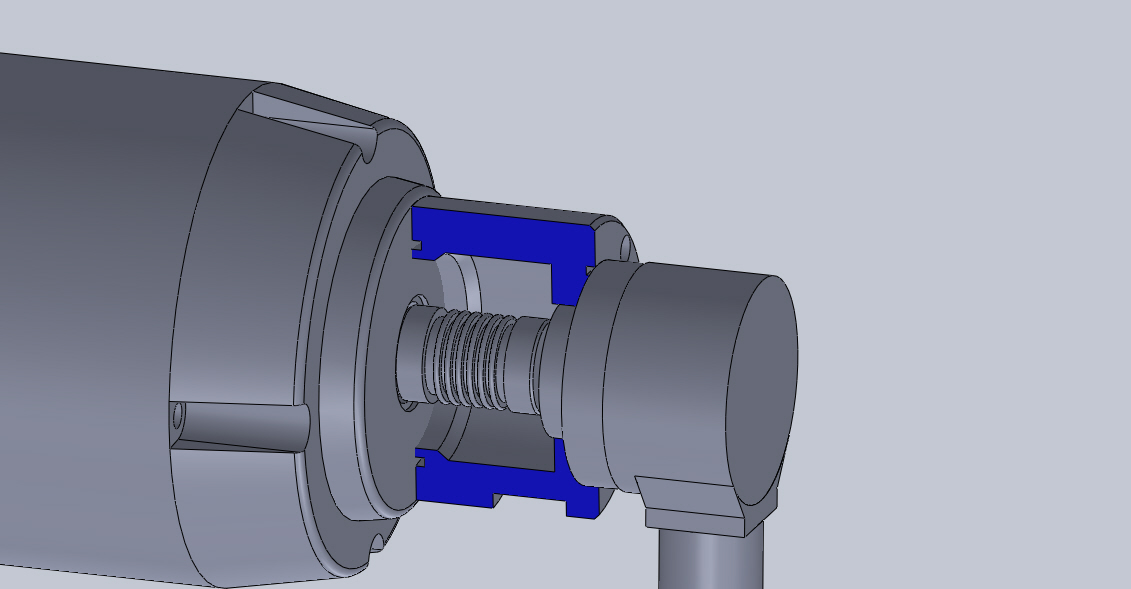
I will keep the indramat servo motors and driver. I will not remove the tachometers, I will connect the encoders like on the picture below.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
9 years 3 weeks ago - 9 years 3 weeks ago #100050
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Does your machine not have the Heidenhain LS403's and EXE? I heard that some MAHO's also have Phillips glass scales for which no one has yet produced a suitable A/D signal processor.
As long as I don't have a VFD installed, I was not going to activate LinuxCNC's spindle override capablity. If the spindle speed is wrong for a feature, I will only have the option of compensating with feed override, or pausing, backing out to a safe Z and changing gear.
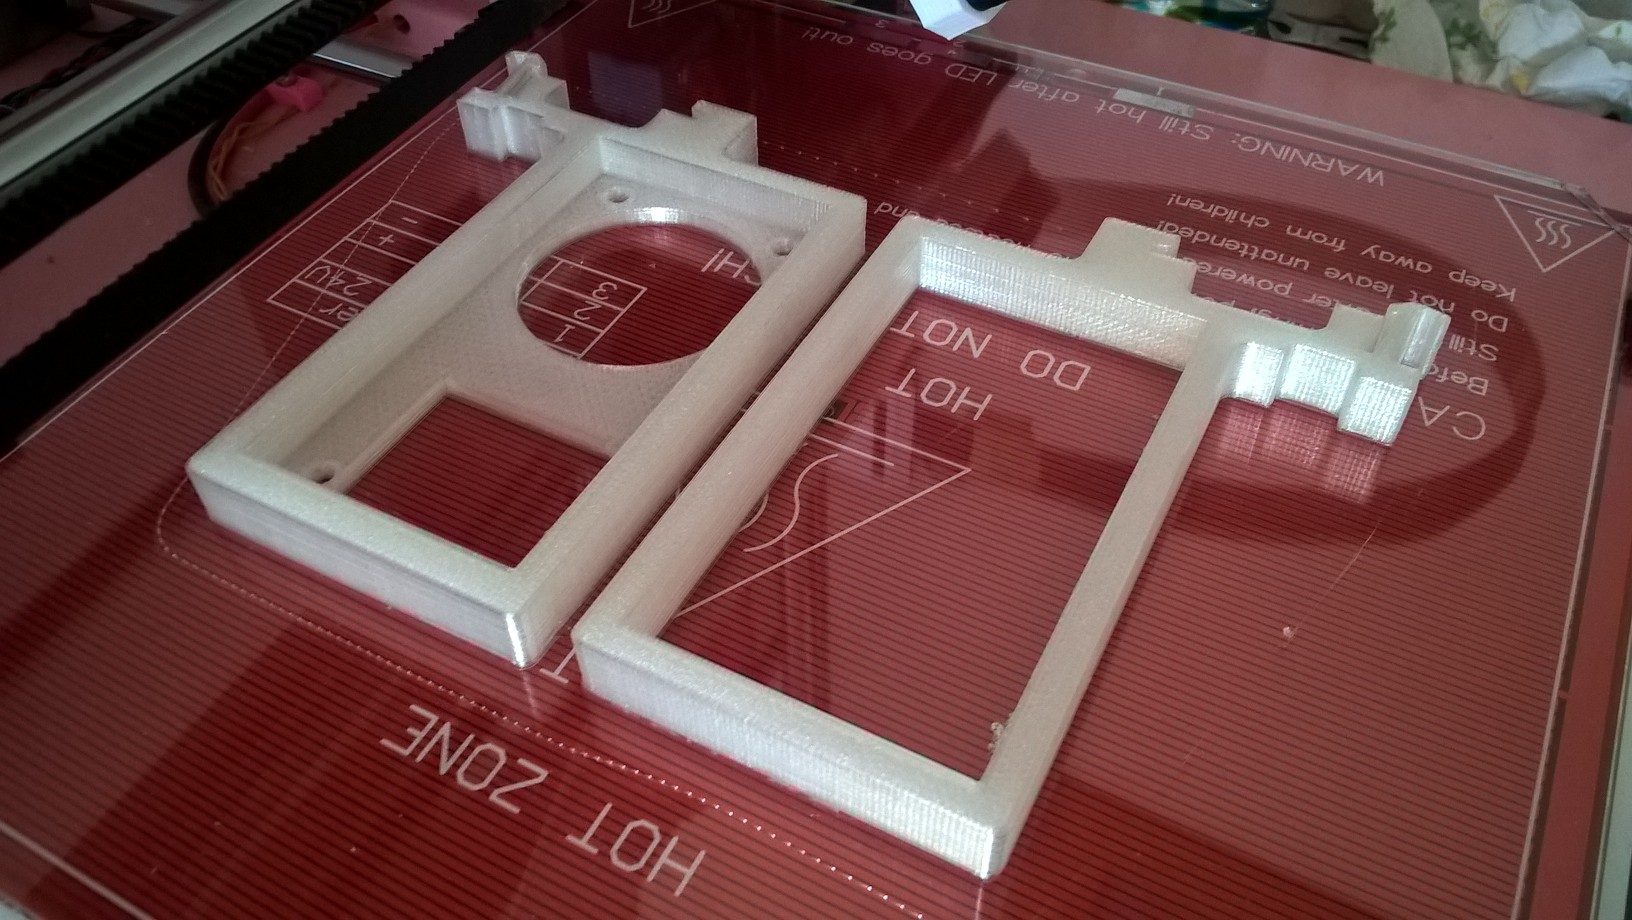
I printed out some brackets to mount the ITX PSU to DIN rail, but screwed up a couple of measurements and will have to print them again.
Mark
As long as I don't have a VFD installed, I was not going to activate LinuxCNC's spindle override capablity. If the spindle speed is wrong for a feature, I will only have the option of compensating with feed override, or pausing, backing out to a safe Z and changing gear.
I printed out some brackets to mount the ITX PSU to DIN rail, but screwed up a couple of measurements and will have to print them again.
Mark
Last edit: 9 years 3 weeks ago by RotarySMP.
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago #100051
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
I don’t know what scales had from the manufacturer, the previous owner had start the retrofit end had placed new scales with quadrature output.
John
John
Please Log in or Create an account to join the conversation.
- drimaropoylos
- Offline
- Elite Member
-
Less
More
- Posts: 265
- Thank you received: 40
9 years 3 weeks ago #100053
by drimaropoylos
Replied by drimaropoylos on topic Retrofitting a 1986 Maho MH400E
3d printer… nice thing to have.
John
John
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 1.533 seconds