
- Posts: 1635
- Thank you received: 595
Retrofitting a 1986 Maho MH400E
- RotarySMP
- Offline
- Platinum Member
-

Less
More
6 years 9 months ago #153794
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
I am pretty sure all of the various modern DRO's, whether chinese or Mitutoyo etc use TLL square wave signals, so the output of the EXE should work fine with any. My three axis EXE boards needed +12V supply as well as +5V. DRO head units will only supply the 5V, you will need an addition PSU, but a 12V wall wart would probably work fine. I wired 12V off the Linux PC's PSU to the EXE's. The standard alone 602 EXE's I used on two axis did not need the 12V.
Mark
Mark
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
6 years 9 months ago #153919
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
The Boley 4LV lathe face plate is now finished...
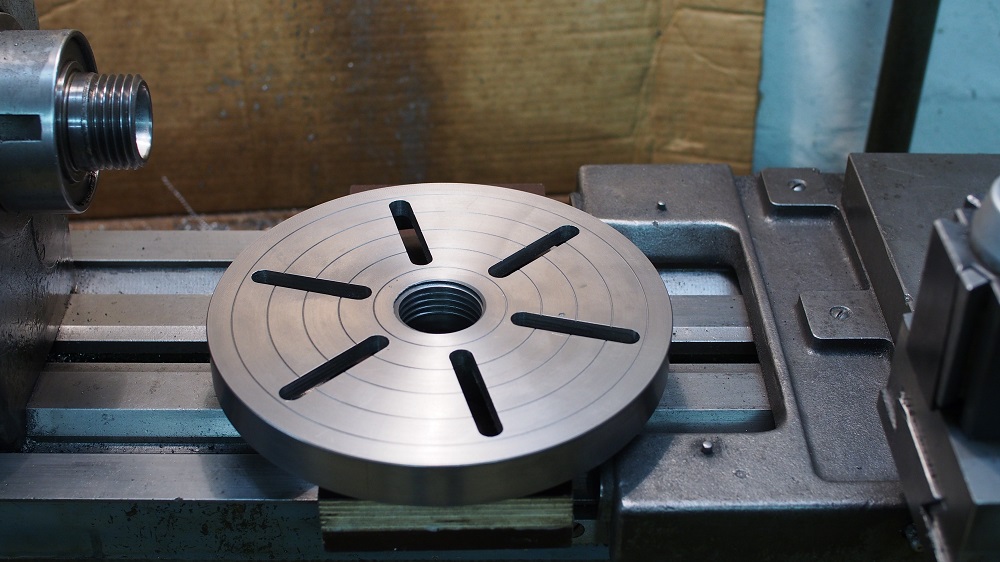
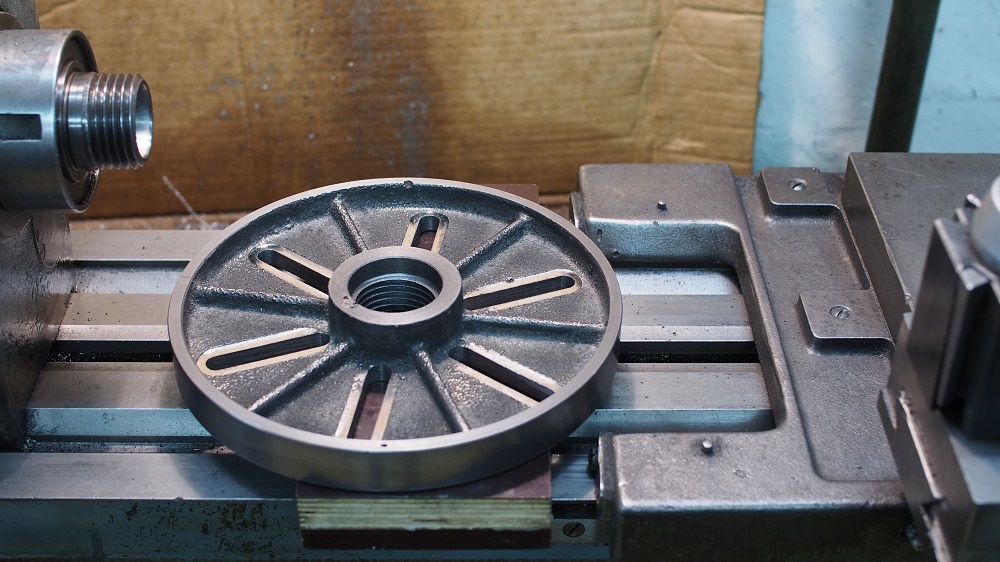
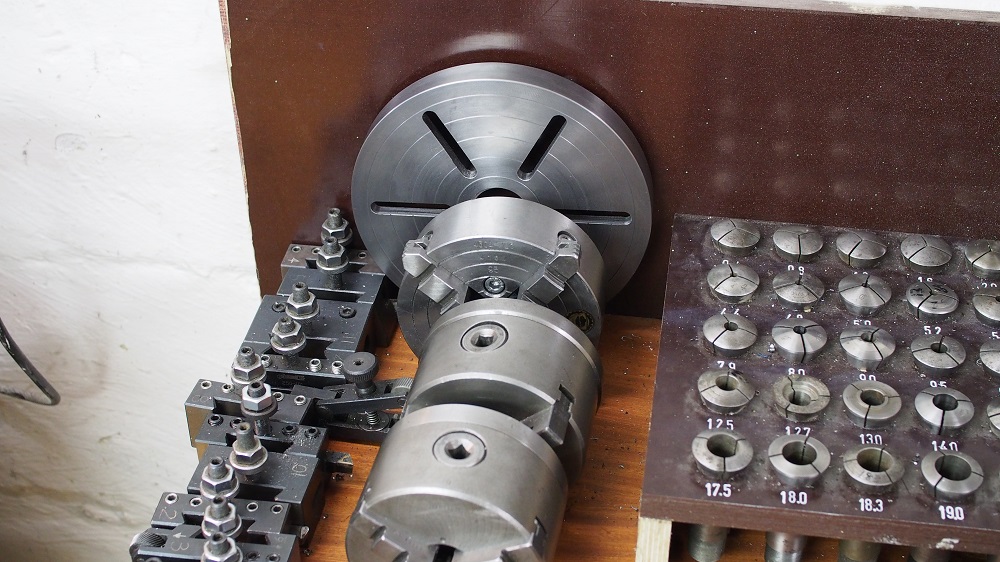
...also a video of the machining (including some MAHO LinuxCNC machining, so it is relevant) can be found here.
Mark
...also a video of the machining (including some MAHO LinuxCNC machining, so it is relevant) can be found here.
Mark
The following user(s) said Thank You: J Green
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
6 years 9 months ago #154324
by andypugh
Very much so. I don't have a foundry of my own, but I have quite a few things cast (to be honest, the commercial prices are such that I don't have much incentive to make my own foundry).
These parts: photos.app.goo.gl/jyLq2pMEzpLpT7V96
Are referred to on this receipt: photos.app.goo.gl/2F5R83N9brvAfAmAA
The large parts were fairly expensive, but then the £150 one weighed 90 kg before machining.
These are 3D printed patterns for a lathe steady: photos.app.goo.gl/MJMGsath5RZkAfpN8
Note the black part, a backup / packer to use during ramming that was trivial to CAD and print, but would have been a real job of work in wood.
And the parts: photos.app.goo.gl/Y7uJkLFqjPFMQFTV9
One tip if printing patterns, leave a hole to put a dowel in (let the CAD package find the centre of gravity...) for the foundry to put a screw in to remove the pattern from the sand. Screws do not take well in low-fill 3D print.
Replied by andypugh on topic Retrofitting a 1986 Maho MH400E
J Green wrote: No offence to any wood workers ,but CAD systems an 3-D printers have really removed a huge problem of coming up with a quick pattern for casting. Even multi part patterns or incorporation of curves or art-nouveau/deco styling should be easy compared to making them from expensive wood.
Very much so. I don't have a foundry of my own, but I have quite a few things cast (to be honest, the commercial prices are such that I don't have much incentive to make my own foundry).
These parts: photos.app.goo.gl/jyLq2pMEzpLpT7V96
Are referred to on this receipt: photos.app.goo.gl/2F5R83N9brvAfAmAA
The large parts were fairly expensive, but then the £150 one weighed 90 kg before machining.
These are 3D printed patterns for a lathe steady: photos.app.goo.gl/MJMGsath5RZkAfpN8
Note the black part, a backup / packer to use during ramming that was trivial to CAD and print, but would have been a real job of work in wood.
And the parts: photos.app.goo.gl/Y7uJkLFqjPFMQFTV9
One tip if printing patterns, leave a hole to put a dowel in (let the CAD package find the centre of gravity...) for the foundry to put a screw in to remove the pattern from the sand. Screws do not take well in low-fill 3D print.
The following user(s) said Thank You: J Green
Please Log in or Create an account to join the conversation.
- Glemigobles
- Offline
- Elite Member
-

Less
More
- Posts: 201
- Thank you received: 18
6 years 9 months ago #154331
by Glemigobles
Replied by Glemigobles on topic Retrofitting a 1986 Maho MH400E
That's a nice face plate Mark! Did you chamfer the edges on the slots on the Maho? It's a great thing to have the CNC do for you if you make parts in CAD/CAM, and not really that difficult to program by hand either since it's just 2D contours. My hand filed chamfers often look like a rough mess and cast iron seems a bit hard on my little Noga scraper.
Please Log in or Create an account to join the conversation.
- RotarySMP
- Offline
- Platinum Member
-
Less
More
- Posts: 1635
- Thank you received: 595
6 years 9 months ago #154351
by RotarySMP
Replied by RotarySMP on topic Retrofitting a 1986 Maho MH400E
Those are some really nice castings Andy. There are no job foundries left around Vienna. There used to be plenty, even in the inner city districts, but were all gone by the 80's. If I need anything heavier than about 18kg cast, I'd probably get a friend to search for a foundry in Bratislava. But for me casting is a challenge I wanted to learn. Now I have the MAHO, I could have just bought a slab of Cast iron and hogged it out of the whole.
Using the 3D printer to also print followers is a technique I only just picked up on.
I didn't chamfer the face plate slots on the MAHO, as I cut the inner edge too close to the hub, and would not have had clearance for the chamfer tool. Also the face side was down during that op.
I changed the INI to reflect the recommendations of Todd and Norbert in this thread, and uploaded a short video showing the tool sensor behaviour now. Still have an error, but it no longer tries to dive through the table.
Mark.
The following user(s) said Thank You: J Green
Please Log in or Create an account to join the conversation.
- hanmon
- Offline
- Senior Member
-

Less
More
- Posts: 73
- Thank you received: 23
6 years 9 months ago #154841
by hanmon
Replied by hanmon on topic Retrofitting a 1986 Maho MH400E
Hi there,
so many interesting things going on here.
I continued work on my A-Axis, a pendant and many smaller parts.
I noticed some issues I'm not so happy with.
The Table drops 0.02mm on the 400mm from left to right (X) which is ok for me.
The drop in Y-direction is 0.05 on the short distance of 250mm.
Also the Main-Spindle seems to be not so happy with a 50mm cutter head.
It doesn't make noise, but the bearings need some readjustment, I guess.
The ballscrew in X is worn. The backlash is 0.3mm. It makes much more noise than the other ballscrews.
I will disassamble the table, remove the ballsrew and try to adjust the Y-drop,
which is very likely caused by play in the ledge.
I will probably replace the ballscrew if there is no simple fix.
I'll keep you up to date.
Cheers
Hanno

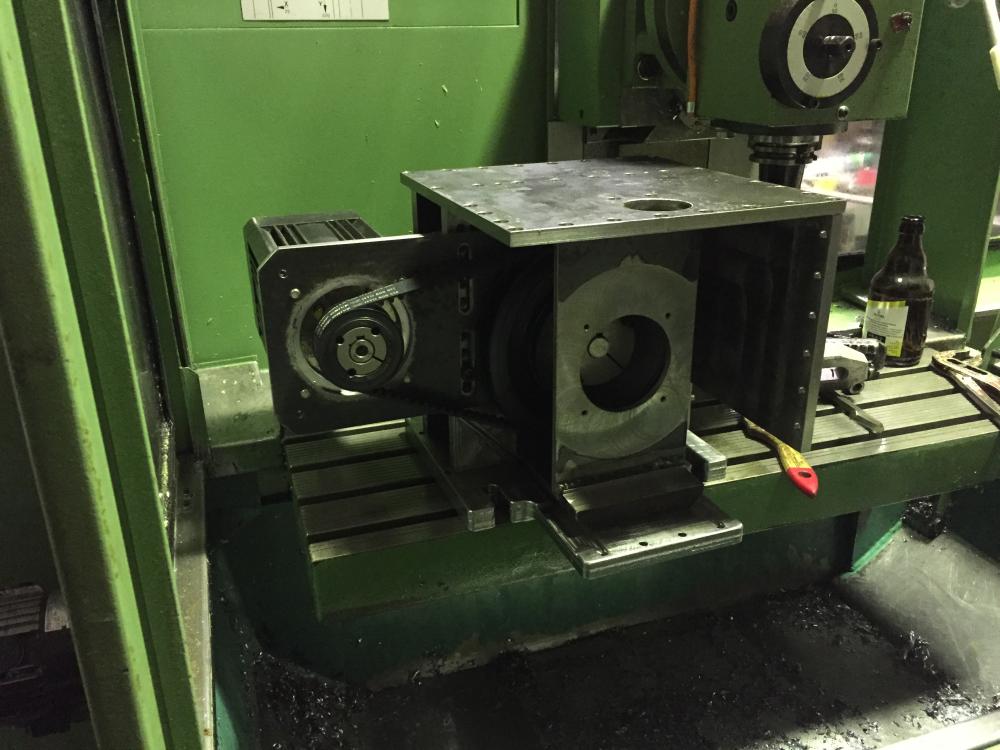
so many interesting things going on here.
I continued work on my A-Axis, a pendant and many smaller parts.
I noticed some issues I'm not so happy with.
The Table drops 0.02mm on the 400mm from left to right (X) which is ok for me.
The drop in Y-direction is 0.05 on the short distance of 250mm.
Also the Main-Spindle seems to be not so happy with a 50mm cutter head.
It doesn't make noise, but the bearings need some readjustment, I guess.
The ballscrew in X is worn. The backlash is 0.3mm. It makes much more noise than the other ballscrews.
I will disassamble the table, remove the ballsrew and try to adjust the Y-drop,
which is very likely caused by play in the ledge.
I will probably replace the ballscrew if there is no simple fix.
I'll keep you up to date.
Cheers
Hanno
The following user(s) said Thank You: J Green
Please Log in or Create an account to join the conversation.
Moderators: piasdom
Time to create page: 0.329 seconds