
- Posts: 959
- Thank you received: 489

Hi,Hello
I'd like to use Remora as a pru for a bridgeport style milling machine.
I'm using a r-pi4 2gb and a btt skr 1.4
Motors are closed loop steppers, with a simple step+dir style command,
for pru and linuxcnc they appear as open-loop.
Before trying Remora I tried the basic hardware with marlin 2 on the skr and is working ok.
Now with remora I have 2 problems:
1- home switches:
I'd like to logically invert the signal coming from remora, but the option "Invert" for digital pin seem to have no effect.
I solved this using a "not" in hal but, anyway since it is in remora config I'd like to know if I'm making some mistake
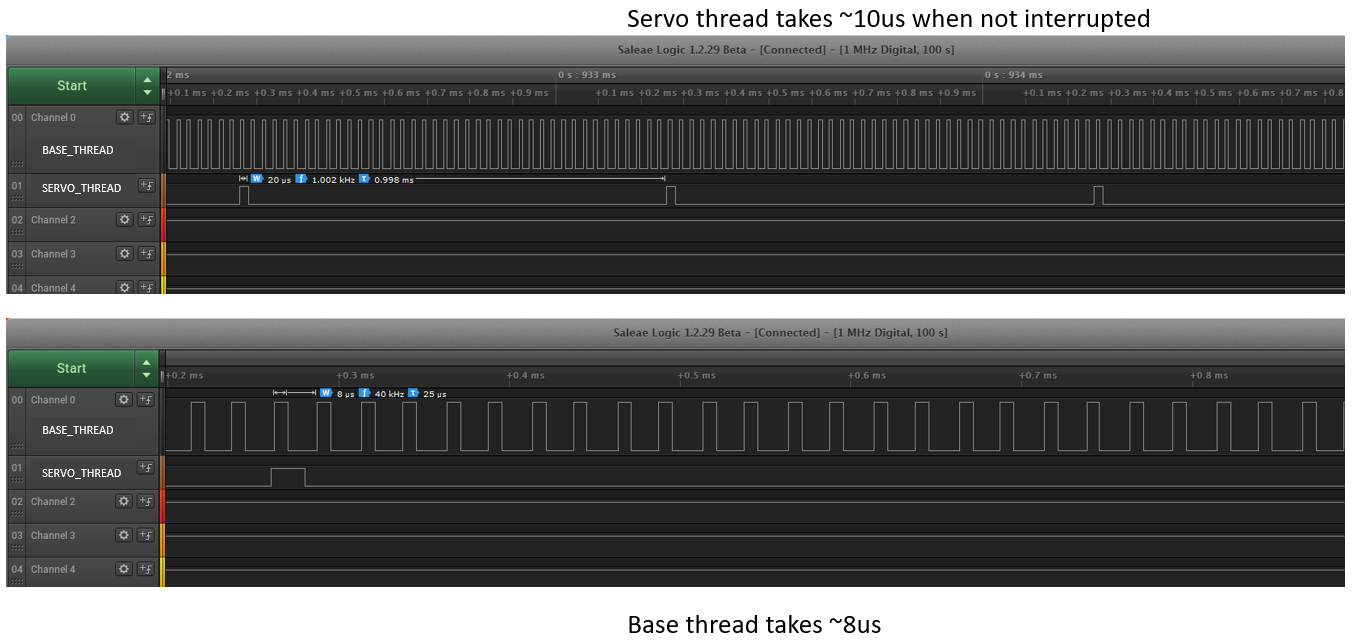
2- what is step generator maximum step rate?
I'm having problems at rates higher than approx 18000-20000 steps per second.
I have 8000step per mm on Z axis, and the driver is happy up to about 140-150mm/min,
at higher speeds remora feedback start to lag behind the command significantly.
Is this normal? Maybe I'm doing somehing wrong, since marlin on the same hw
is able to go happily up to 1800mm/min (also if the machine is not happy to go that fast image missing /media/kunena/emoticons/dizzy.png
Please Log in or Create an account to join the conversation.
Thanks for contributing to the documentation. I need to pull my finger out and get the 3D printer stuff documented.I have started adding hal code clips into the remora docs.
remora-docs.readthedocs.io/en/latest/software/hal-examples.html
If you guys have any interesting or unique code in your hal if you could copy paste it here i can easily add it.
Would be nice if you could give it s short write up so a user can just copy paste the code and have a basic idea of why.
Please Log in or Create an account to join the conversation.
Hi Rommel,I hit a few snags.
1. My neighbour doesn't understand my obsession with this
2. I think I killed my X axis driver.
I finally made a crappy vid Aircut ( streamable.com/5yszzq )
Warning it's headache inducing, bandwidth consuming.
I think it's not bad for a bent X axis leadscrew with a .5" pitch, atleast I think I have the scale correct.
In any case it's just a proof that the controller works, pretty stable too.
Oh and this jscut.org/ is a good start for a newbie it imports svg from inkscape .
@Scott I bump the PRU_BASEFREQ to 200kHz just to see what happens, the video is the result.
But after re-run for a couple of times the x axis driver is dead. I just realized that there's no configurable option to
change the step pulse width. The TB6600 I'm using apparently has a minimum pulse of 5 uSec probably more.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.
Please Log in or Create an account to join the conversation.


