
- Posts: 56
- Thank you received: 1
G33.1 right hand tapping weird behavior H E L P !
- tkamsker
- Offline
- Senior Member
-

Less
More
11 years 7 months ago #56820
by tkamsker
Replied by tkamsker on topic G33.1 right hand tapping weird behavior H E L P !
Hi,
I have an question
I have switched of count of course
have connected A and Z and B is extra so one Revolution of the spindle brings
A and Z
then B
and next revolution the same
And i think that brings me in trouble ,..
I can get Speed rps rpm fine but then revs is 0 -1 or 1
so do i have to attach an encoder which gives AB AB AB AB and so on and only 1 Z per revolution ?
It seems they revs start after 2nd revolution
When i switch counter on and use A and Z (z then on former B ) to have an 90° offset i get everything
but revs keep on counting (when i do G33.1 it starts nice then reverses the spindle but ,... )
So if anybody has some experience with tha minimized setup it would be nice
The bridgeport has done ist somehow by one Pin anyway ,..
but that is another story
thx
thomas
Please Log in or Create an account to join the conversation.
- PCW
- Offline
- Moderator
-

Less
More
- Posts: 18115
- Thank you received: 5334
11 years 7 months ago - 11 years 7 months ago #56828
by PCW
Replied by PCW on topic G33.1 right hand tapping weird behavior H E L P !
Rigid tapping requires a full A/B/IDX encoder, in addition it needs one with fairly good resolution
in order to accurately "gear" the Z axis to the spindle rotation. One pin is fine for getting
spindle velocity, no so fine for determining exactly when reversal occurs
in order to accurately "gear" the Z axis to the spindle rotation. One pin is fine for getting
spindle velocity, no so fine for determining exactly when reversal occurs
Last edit: 11 years 7 months ago by PCW.
The following user(s) said Thank You: tkamsker
Please Log in or Create an account to join the conversation.
- tkamsker
- Offline
- Senior Member
-
Less
More
- Posts: 56
- Thank you received: 1
11 years 7 months ago #56833
by tkamsker
Replied by tkamsker on topic G33.1 right hand tapping weird behavior H E L P !
Hi PCW ,
thank you for you answer i hoped that i can do it without big changes on the bridgeport
my idea was (because on the original
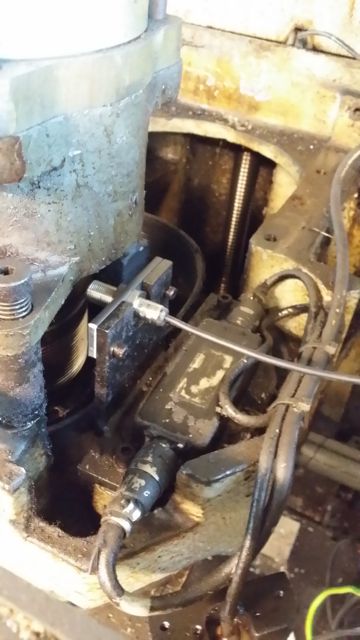 here my adaption ) to use only one "ping"
i now learned that this is not enough
So Plan "B" i build an test on my mill
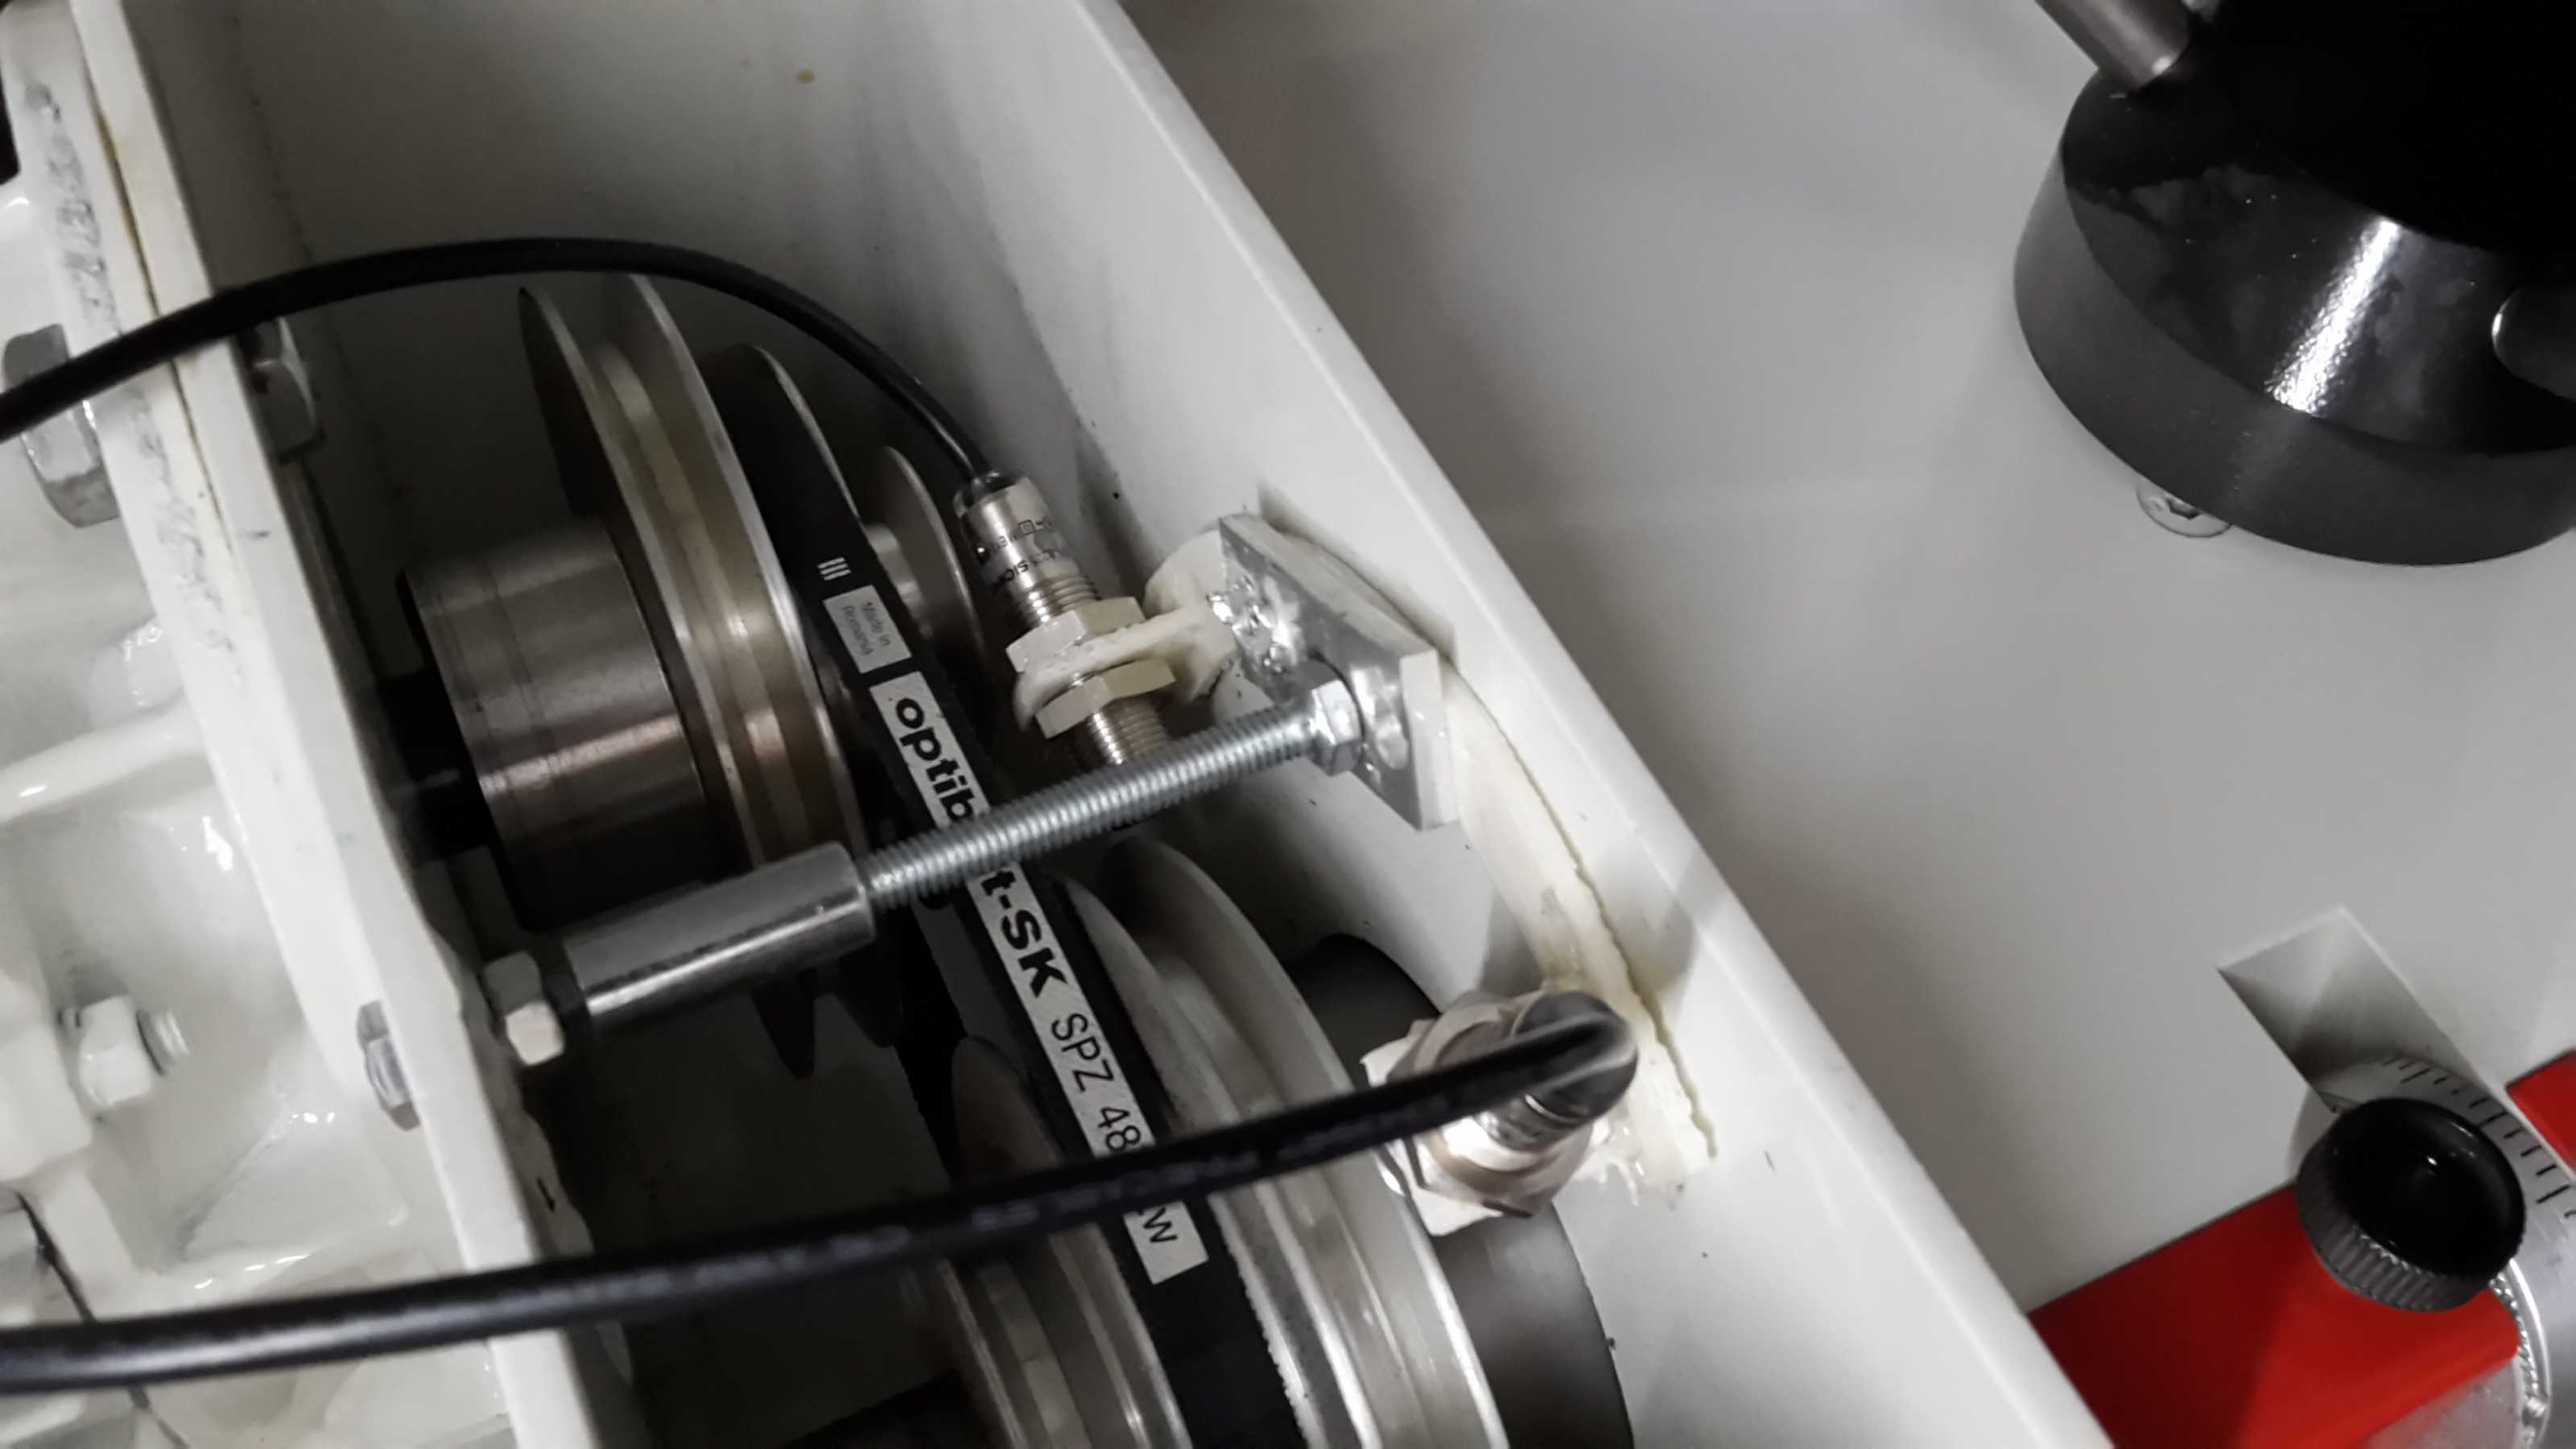 where 2 "Probes" are 90° separated and only 1 steel plate is doing the signal so i hoped to get an A/ B Signal (which i do ) which gives me perfect speed .
but revs are not counted !!! i denn put the index signal to A and later to b signal then the revs never get bigger than 1 or -1
So my conclusion would be to put more metal plates (just for test ) on the spindle to get lets say 4 a/b per revolution and i add an longer metal plate and mount a 3rd "probe" to get the index signal
this would lead to an poor mans encoder ,..
so if someone had done ist similar i would go that route because i have everything at hand (but time)
or if you say encoder i have some AMT 101 Encoders on stock ( www.digikey.at/product-detail/en/AMT102-V/102-1307-ND/827015 ) but the mount on the Bridgeport will be very complicated ( on my lathe i am on the way to do that but that is next task )
So if someone can lead me in the right direction this would help me big times
last resort would be to go the Encoder route
thanx
thomas kamsker
thank you for you answer i hoped that i can do it without big changes on the bridgeport
my idea was (because on the original
i now learned that this is not enough
So Plan "B" i build an test on my mill
but revs are not counted !!! i denn put the index signal to A and later to b signal then the revs never get bigger than 1 or -1
So my conclusion would be to put more metal plates (just for test ) on the spindle to get lets say 4 a/b per revolution and i add an longer metal plate and mount a 3rd "probe" to get the index signal
this would lead to an poor mans encoder ,..
so if someone had done ist similar i would go that route because i have everything at hand (but time)
or if you say encoder i have some AMT 101 Encoders on stock ( www.digikey.at/product-detail/en/AMT102-V/102-1307-ND/827015 ) but the mount on the Bridgeport will be very complicated ( on my lathe i am on the way to do that but that is next task )
So if someone can lead me in the right direction this would help me big times
last resort would be to go the Encoder route
thanx
thomas kamsker
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
11 years 7 months ago #56834
by andypugh
You probably want more than 4 pulses. Home-made encoders normally have 50+ slots and commercial ones have 1000+
Do you know what the response time of you sensors is? At high speeds they may start missing edges.
Replied by andypugh on topic G33.1 right hand tapping weird behavior H E L P !
tkamsker wrote: So my conclusion would be to put more metal plates (just for test ) on the spindle to get lets say 4 a/b per revolution and i add an longer metal plate and mount a 3rd "probe" to get the index signal
You probably want more than 4 pulses. Home-made encoders normally have 50+ slots and commercial ones have 1000+
Do you know what the response time of you sensors is? At high speeds they may start missing edges.
The following user(s) said Thank You: tkamsker
Please Log in or Create an account to join the conversation.
- tkamsker
- Offline
- Senior Member
-
Less
More
- Posts: 56
- Thank you received: 1
11 years 7 months ago #56835
by tkamsker
Replied by tkamsker on topic G33.1 right hand tapping weird behavior H E L P !
Hi,
as always you are right
right now they are
at.rs-online.com/web/p/induktive-naherun...743D3730313832323526
Product code 7018225 which says 2000Hz !
So the spindle can do 4000 hz (which will not be used ) but theoretical i am already in trouble ,..
So i will then use the AMT102 which are rated to 7500 or 15k rpm and i can choose the pulses per revolution by dip switches
I have no idea how to mount them but that has to be done i hoped to get it by not doing it the maximum efford
thank you so much thomas
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-
Less
More
- Posts: 19899
- Thank you received: 4655
11 years 7 months ago #56840
by andypugh
You may be confusing Hz and RPM. 2000Hz = 120,000 rpm.
But if you had a 50 slot code-wheel then the 2000Hz only gives you 2400 rpm.
(This might not matter, you wouldn't rigid-tap at 2000 rpm)
Are there any gears on the spindle? They can make good code-wheels.
pico-systems.com/bridge_spindle.html
Replied by andypugh on topic G33.1 right hand tapping weird behavior H E L P !
tkamsker wrote: Product code 7018225 which says 2000Hz !
So the spindle can do 4000 hz (which will not be used ) but theoretical i am already in trouble
You may be confusing Hz and RPM. 2000Hz = 120,000 rpm.
But if you had a 50 slot code-wheel then the 2000Hz only gives you 2400 rpm.
(This might not matter, you wouldn't rigid-tap at 2000 rpm)
Are there any gears on the spindle? They can make good code-wheels.
pico-systems.com/bridge_spindle.html
Please Log in or Create an account to join the conversation.
Time to create page: 0.260 seconds