
- Posts: 542
- Thank you received: 241
Gcode went wrong
- MaHa
- Offline
- Platinum Member
-

Less
More
7 years 10 months ago #122818
by MaHa
Replied by MaHa on topic Gcode went wrong
If you look at the sketch, there must have been a crash at X-2 Y-2 with the G0 Z-10 move, without cutter compensation. There was no report about. Probably touch off was done with the tool to sides of the block. T without M6 only prepares tool.
Since cutter compensation in linuxcnc is kind of ¿?¿ ,it`s good advice to read this part of the manual.
Since cutter compensation in linuxcnc is kind of ¿?¿ ,it`s good advice to read this part of the manual.

Please Log in or Create an account to join the conversation.
- mane
- Offline
- Senior Member
-

Less
More
- Posts: 46
- Thank you received: 1
7 years 10 months ago #122822
by mane
Replied by mane on topic Gcode went wrong
Thanks to all your comments. I thought it´s easier to run a simple program. I will check all suggestions in the next days.
Merry Christmas.
Mane
Merry Christmas.
Mane
Please Log in or Create an account to join the conversation.
- jbraun
- Offline
- Senior Member
-
Less
More
- Posts: 65
- Thank you received: 15
7 years 10 months ago #122833
by jbraun
Replied by jbraun on topic Gcode went wrong
Here's an attached png to clarify what I posted earlier.
The red is your file with no tool loaded and no D in the G41 line. You need one or the other for linuxcnc to read the tool table.
The white is a compensated path with a lead-in, notice how it rolls around corners.
It's not hard programming if you follow the rules.
Merry Christmas to you as well.
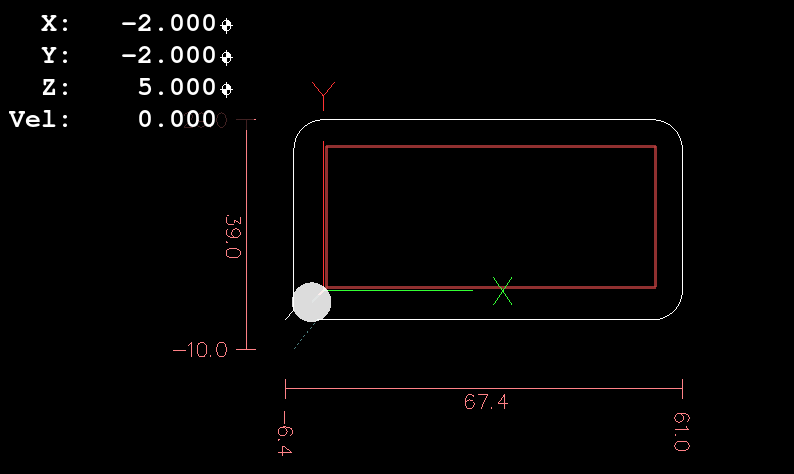
The red is your file with no tool loaded and no D in the G41 line. You need one or the other for linuxcnc to read the tool table.
The white is a compensated path with a lead-in, notice how it rolls around corners.
It's not hard programming if you follow the rules.
Merry Christmas to you as well.
Please Log in or Create an account to join the conversation.
- mane
- Offline
- Senior Member
-
Less
More
- Posts: 46
- Thank you received: 1
7 years 10 months ago - 7 years 10 months ago #122920
by mane
Replied by mane on topic Gcode went wrong
I changed line 5 to G41 D10 and did not use the tool table. Homed the machine and touched left lower corner of the workpiece with G54. Then i loaded the program below with error "Length of cutter compensation entry move is not greater than the tool radius".
To have no problem with tool cutter entry i added line 4 to be far away from the corner. But this does not help.
The error comes right after loading the program, in the status line bottom i have no tool loaded. And G54 DRO view does not change the values when i jog around the axis by keyboard.
To have no problem with tool cutter entry i added line 4 to be far away from the corner. But this does not help.
The error comes right after loading the program, in the status line bottom i have no tool loaded. And G54 DRO view does not change the values when i jog around the axis by keyboard.
Code:
1. G21 G17 G40 G49 G61 G90 G54
2. F56
3. G0 Z5
4. G0 X-20 Y-20
5. G41 D10
6. G1 Z1
7. G1 X0.5 Y0.5
8. G1 X0.5 Y24.5
9. G1 X56.5 Y24.5
10. G1 X56.5 Y0.5
11. G1 X0.5 Y0.5
12. M30
Last edit: 7 years 10 months ago by mane. Reason: additional info added
Please Log in or Create an account to join the conversation.
- andypugh
- Offline
- Moderator
-

Less
More
- Posts: 19899
- Thank you received: 4655
7 years 10 months ago #122928
by andypugh
Replied by andypugh on topic Gcode went wrong
Try an XY move after the G41.
Please Log in or Create an account to join the conversation.
- jbraun
- Offline
- Senior Member
-
Less
More
- Posts: 65
- Thank you received: 15
7 years 10 months ago #122935
by jbraun
Replied by jbraun on topic Gcode went wrong
Hi Mane
It's as Andy said, a minor change gets rid of the error.
The difference between G61 and G64 it may a good read. My apologies if you're already aware of those codes.
While the rest of the household was watching the Die Hard marathon I did a little blog post on cutter comp.
I am not an expert on the topic but maybe there's something useful there.
steppingintocnc.blogspot.com/2018/12/eas...er-compensation.html
*moderators: if linking to a personal blog is out of bounds removing the link causes no hard feelings
It's as Andy said, a minor change gets rid of the error.
Code:
G21 G17 G40 G49 G61 G90 G54
F56
G0 Z5
G0 X-20 Y-20
G1 Z1
G41 D10
G1 X0.5 Y0.5
G1 X0.5 Y24.5
G1 X56.5 Y24.5
G1 X56.5 Y0.5
G1 X0.5 Y0.5
M30
While the rest of the household was watching the Die Hard marathon I did a little blog post on cutter comp.
I am not an expert on the topic but maybe there's something useful there.
steppingintocnc.blogspot.com/2018/12/eas...er-compensation.html
*moderators: if linking to a personal blog is out of bounds removing the link causes no hard feelings
Please Log in or Create an account to join the conversation.
Time to create page: 1.039 seconds